GF3012: Overview
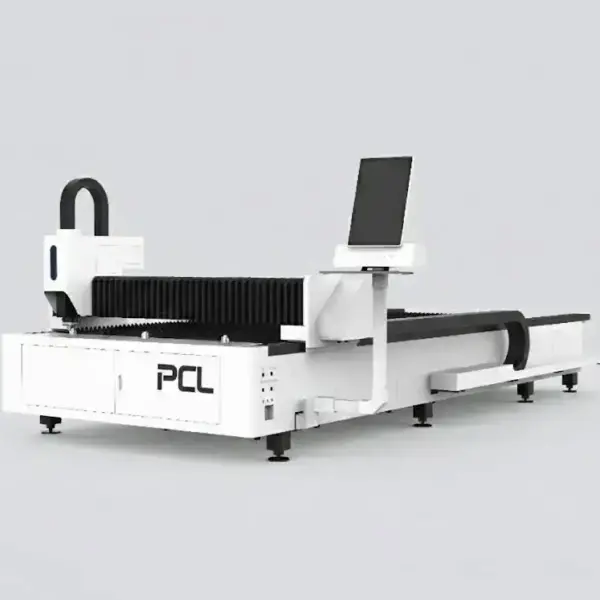
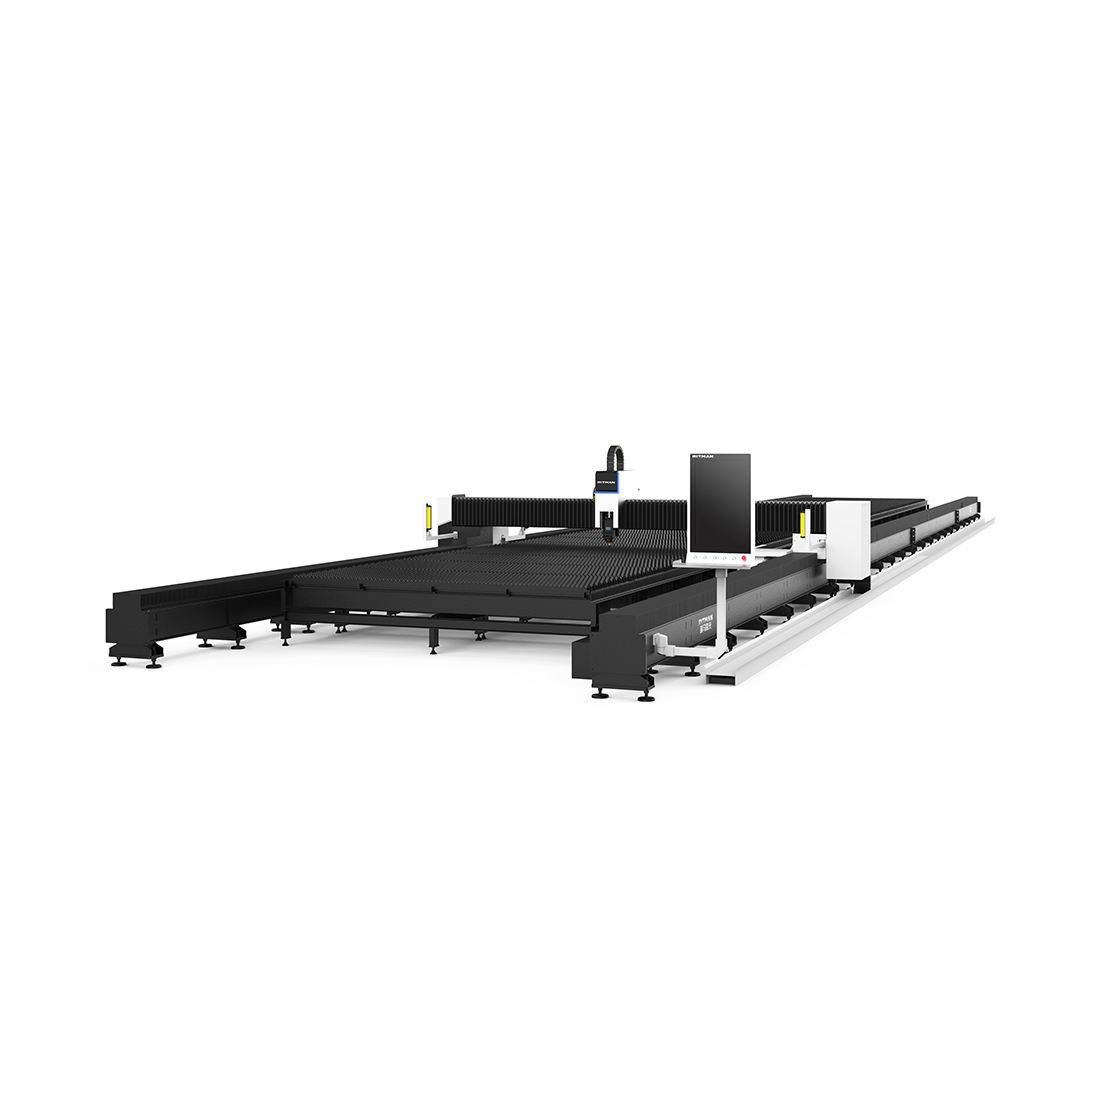
The GF3012 puts a high-power fiber source, from 6 kW up to 60 kW, on a compact 3000 × 1200 mm bed. It is for shops that cut thick plate into small and medium parts and want the power without the floor space of a 4020 or 6020 machine. The motion is built around an auto-focus head, Yaskawa or Fuji servo drives and Hiwin rails.

Technical Specifications
| Working area | 3000 × 1200 mm |
|---|---|
| Laser power | 6–60 kW fiber |
| X/Y positioning accuracy | ±0.03 mm |
| Max linkage speed | 100 m/min |
| Cutting head | Raytools or WSX auto-focus |
| Drive | Yaskawa or Fuji servo motors, Hiwin linear rails |
| File formats | AI, BMP, PLT, DXF, DST and others |
| Materials | Carbon steel, stainless steel, aluminium, brass |
| Certification | CE, ISO 9001 |
| Warranty | 24 months on the whole machine (consumables excluded) |
What the Power Options Cut
Typical maximum thickness from 1 kW to 60 kW; the last column marks the powers this machine can carry. Treat the figures as the ceiling, not the daily working range. At these powers the GF3012 is a thick-plate machine. On thin sheet the extra kilowatts add little, because acceleration sets the pace there.
| Laser power | Carbon steel (O₂) | Stainless (N₂) | Aluminium (N₂) | Brass (N₂) | This model |
|---|---|---|---|---|---|
| 1 kW | 10 mm | 5 mm | 3 mm | 3 mm | – |
| 1.5 kW | 16 mm | 6 mm | 4 mm | 3 mm | – |
| 2 kW | 20 mm | 8 mm | 6 mm | 5 mm | – |
| 3 kW | 22 mm | 10 mm | 8 mm | 6 mm | – |
| 4 kW | 25 mm | 12 mm | 10 mm | 8 mm | – |
| 6 kW | 25 mm | 20 mm | 16 mm | 12 mm | ✓ |
| 8 kW | 40 mm | 30 mm | 30 mm | 16 mm | ✓ |
| 12 kW | 40 mm | 40 mm | 40 mm | 16 mm | ✓ |
| 20 kW | 80 mm | 100 mm | 60 mm | 20 mm | ✓ |
| 60 kW | 200 mm | 150 mm | – | – | ✓ |
Maximum thickness is a ceiling, cut slowly and with a rougher edge. Plan daily production a few millimetres below it, and confirm with the cutting chart of the exact source and head in your quotation.
Typical Cutting Speeds
| Thickness | 6 kW | 12 kW |
|---|---|---|
| 3 mm | 3.5–4.2 | – |
| 4 mm | 3.3–3.8 | – |
| 6 mm | 2.7–3.2 | – |
| 8 mm | 2.2–2.5 | – |
| 10 mm | 2.0–2.3 | 2.0–2.3 |
| 12 mm | 1.9–2.1 | 3.0–3.5 |
| 16 mm | 1.2–1.4 | 2.8–3.0 |
| 20 mm | 0.6–0.7 | 1.5–1.6 |
| 25 mm | 0.4–0.5 | 0.8–1.0 |
| Thickness | 6 kW | 12 kW |
|---|---|---|
| 1 mm | 40–50 | 50–60 |
| 2 mm | 25–30 | 40–45 |
| 3 mm | 15–18 | 30–35 |
| 5 mm | 7–8 | 15–18 |
| 6 mm | 6–7 | 13–15 |
| 8 mm | 3.5–3.8 | 8–10 |
| 10 mm | 1.6–2.0 | 6.5–7.5 |
| 12 mm | 1.0–1.2 | 5.0–5.5 |
| 16 mm | 0.5–0.6 | 2.0–2.3 |
| 20 mm | 0.2–0.35 | 1.2–1.4 |
Speeds in m/min. Typical values for good-quality cutting; edge requirements, material grade, gas purity and the head change them. Your quotation includes the chart for the exact configuration.
High Power on a Compact Bed
Thick-plate parts such as flanges, brackets, base plates and machine parts are often small. Cutting them on a 3012 bed gives you the source power without paying for and housing a 4 m or 6 m machine. Three things scale with the power, not with the bed: the chiller, the electrical supply and the gas supply. Plan them for the source you choose, and plan a crane for heavy plate.
The 1200 mm width takes 1250 × 2500 mm plates directly. If you buy 1500 × 3000 mm plates, look at the LFP3015 or the 4020 machines.
Why Auto-Focus Matters on Thick Plate
Thick plate is pierced in stages, each with its own focus and height, and oxygen cutting moves the focus further up as the plate gets thicker. The auto-focus head takes these values from the cutting program, so the operator does not reset lenses for each job, and pierces and cuts come out the same every time.
Where It Sits in the PCL Laser Range
| Model | Working area | Power | Best for |
|---|---|---|---|
| GF3012 (this machine) | 3000 × 1200 mm | 6–60 kW | High power on a compact bed |
| LFP3015 | 3000 × 1500 mm | 1–12 kW | Open single table; standard sheets |
| LFP4020 | 4000 × 2000 mm | 1–30 kW | Dual exchange table for volume |
| LFH4020 | 4000 × 2000 mm | 1–30 kW | High-power plate on a plate-welded bed |
| LFP6020 | 6000 × 2000 mm | 1.5–3 kW | Long sheets at lower investment |
| LFH6020 | 6000 × 2000 mm | 1–12 kW | Large-format production |
| 2-in-1 sheet & tube | 3015 or 4020 + tubes Ø20–220 mm | 1–12 kW | Sheet and tube on one machine |
Common Problems and How to Fix Them
| Problem | Usual cause | What to do |
|---|---|---|
| Pierce blow-out on thick plate | Single-step pierce on heavy plate | Use staged piercing and let the plate cool between pierces |
| Heavy dross under thick carbon steel | Speed too high, oxygen pressure low, focus too negative, nozzle partly blocked | Reduce speed by 5–8 %; keep oxygen at 0.5–0.7 bar; set focus +3 to +4 mm; check the nozzle |
| Not cutting through | Pierce not finished, focus not positive enough on oxygen cuts, dirty protective window | Let all pierce stages finish; raise focus in 1 mm steps; clean or replace the window |
| Dross under stainless or aluminium | Speed too high, nitrogen pressure too low or focus not deep enough | Lower the speed or raise pressure; move the focus down (negative) as thickness grows |
What Decides the Price
| Item | Options | Effect |
|---|---|---|
| Laser source | Brand (Raycus, IPG, Max) and power | The largest single item; higher power costs more and needs a bigger chiller and supply |
| Cutting head | Raytools or WSX auto-focus | Auto-focus and protection against collisions |
| Drive | Servo brand, rails and racks | Accuracy over the years |
| Power | 6–60 kW | The source is most of the price; higher power also needs a larger chiller, power supply and gas supply |
The GF3012 is quoted on request.
From Inquiry to Production
- Parts and samples. Send your thickest parts and materials; we cut samples on the power you are considering.
- Configuration. We fix the source, head, table and options, and send a layout with floor space, power, gas and extraction connections.
- Build and test. The machine is assembled and tested before shipment; lead time is confirmed in the quotation.
- Site preparation. Level floor, power supply, assist gas and compressed air, and fume extraction ready before arrival.
- Installation and training. Quoted with the machine; operators learn nesting, cutting parameters, daily checks and simple fault finding.
- Support. 24-month warranty on the whole machine, consumables excluded.
Before You Order
- Thickest plate and the thickness you cut most hours.
- Crane for loading heavy plate.
- Power supply, chiller and gas supply for the chosen source.
- Plate sizes: the bed takes 1250 × 2500 mm directly.
Maintenance
| When | What |
|---|---|
| Daily | Check and clean the protective window; check nozzle condition and centring; check gas pressures. |
| Weekly | Remove slag; clean slats and rails; check the height sensor. |
| Periodically | Replace slats; lubricate rails and racks; change chiller water and extraction filters. |
Safety
Laser light reflected from the sheet is invisible and can injure eyes, so the cutting area must be enclosed or fenced off and the door interlocks must stay working. Keep the extraction running and its filters clean; dust in the bed and filters can catch fire, especially after aluminium. Keep oxygen equipment free of oil and grease, and secure gas cylinders.
GF3012 FAQ
What is the working area of the GF3012?
3000 × 1200 mm.
Which power options are there?
Fiber sources from 6 kW up to 60 kW.
How thick can it cut?
Typical maximums are 25 mm carbon steel and 20 mm stainless at 6 kW, about 40 mm of both at 12 kW, and far more at 20–60 kW. Daily production runs a few millimetres below the maximum.
Which files can it read?
AI, BMP, PLT, DXF and DST among others.
Why put high power on a 3012 bed?
Thick-plate parts are often small. The compact bed gives you the source power without the cost and floor space of a 4 m or 6 m machine.
What does high power need on site?
A larger power connection, a chiller matched to the source and a gas supply for high consumption; the layout drawing lists them for your configuration.
Compare all fiber laser cutting machines side by side in our selection guide.
Send your thickest parts and material. We suggest the source power and quote the GF3012.
Get a quote