

Robot Welding Workstation: Overview
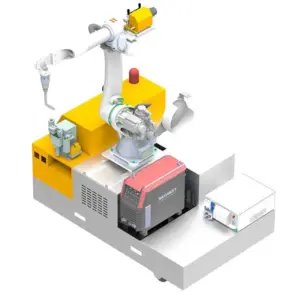
A robot welding workstation combines a 6-axis welding robot with a positioner that turns the part, so every seam is welded in the best position, usually flat or horizontal. It is the standard choice for repeat parts, from small automotive brackets to heavy structural assemblies of several tonnes.
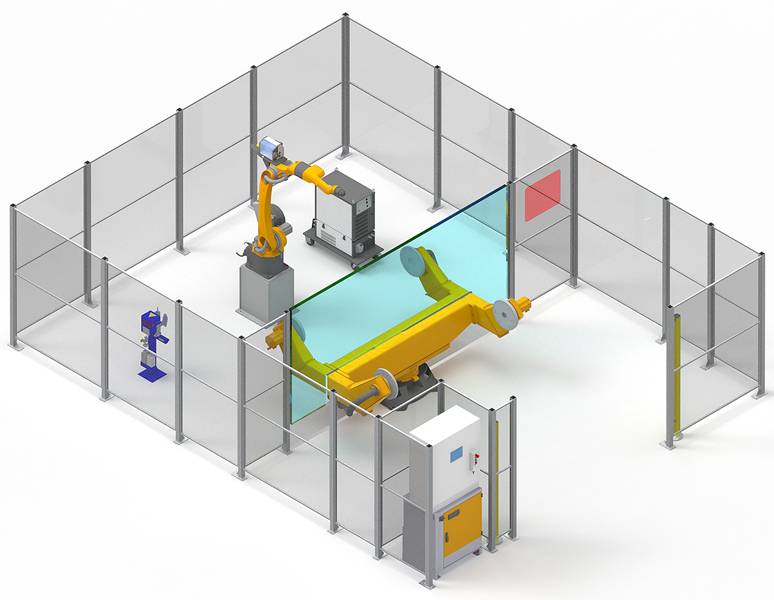
The positioner is synchronized with the robot controller, so the part rotates while the robot welds. Round seams are welded in one continuous pass, and multi-side parts are welded without re-clamping.
Robot Welding Workstation in Action
The positioner turns the part while the robot welds.
Technical Specifications
| Robot | 6-axis welding robot |
|---|---|
| Positioner types | Single-axis, L-type (two-axis) or C-type |
| Positioner capacity | 500–5000 kg and above |
| Positioner drive | RV reducers, synchronized with the robot controller |
| Ground rail | Optional, for longer parts |
| Programming | Offline programming or teaching-free, depending on the application |
| Seam finding | Laser seam tracking or arc tracking (options) |
| Welding processes | MIG / MAG / TIG; solid and flux-cored wire |
| Welding power source | Aotai, Megmeet, Panasonic, Lincoln Electric, Miller or others on request |
| Welding standards | Procedures can be qualified to ISO, AWS D1.1 and classification-society rules (ABS, LR, CCS) |
| Certification | CE, ISO 9001 |
| Lead time | 20–45 days depending on configuration |
| Warranty | 24 months on the whole machine (consumables excluded) |
Choosing the Positioner
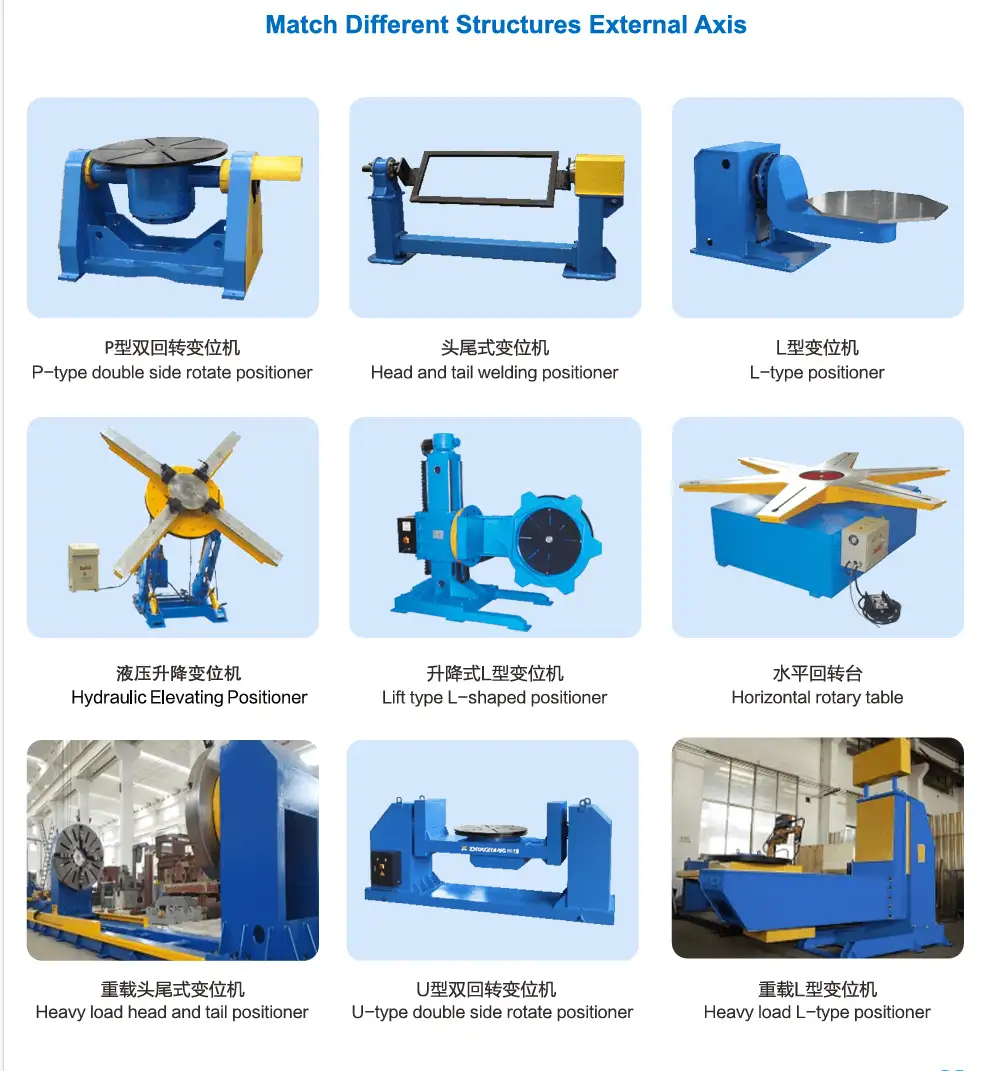
| Type | Movement | Typical parts |
|---|---|---|
| Single-axis | Turns the part around one horizontal axis | Long parts such as beams, frames and shafts |
| L-type (two-axis) | Tilts and rotates the part | Boxes, brackets and parts with seams on several faces |
| C-type | Rotates the part inside a C-shaped frame | Parts that need full access around their length, such as frames and booms |
How a Workstation Runs
- Clamp the part in a fixture. Repeat parts use a fixture on the positioner, so every part sits in the same place.
- Program once. Create the program offline from the model, or with the teaching-free function where the application allows.
- Weld in the best position. The positioner turns the part so the robot welds flat or horizontal, which gives better penetration and bead shape.
- Repeat. For every following part the operator only loads, clamps and starts the cycle.
Typical Workpieces and Industries
Workpieces
- Automotive brackets and small assemblies
- Construction-machinery booms and frames
- Agricultural machinery parts
- Structural steel assemblies up to several tonnes
- Shafts, pipes and round parts
Why a workstation
- Best welding position for every seam
- Continuous circumferential welds
- Fast cycle on repeat parts
- Fixtures keep part position consistent
- Compact footprint compared with gantry systems
How It Compares with Other Welding Robots
| System | Strength | Choose it when |
|---|---|---|
| Cantilever welding robot CWR500A | Open front and back for crane loading; 3.5 m reach | Long plate units, H-beams and box girders loaded by crane |
| Gantry welding robot | Covers a full rectangular area, e.g. 12 m × 4 m | Very wide parts such as ship sections and trailer frames |
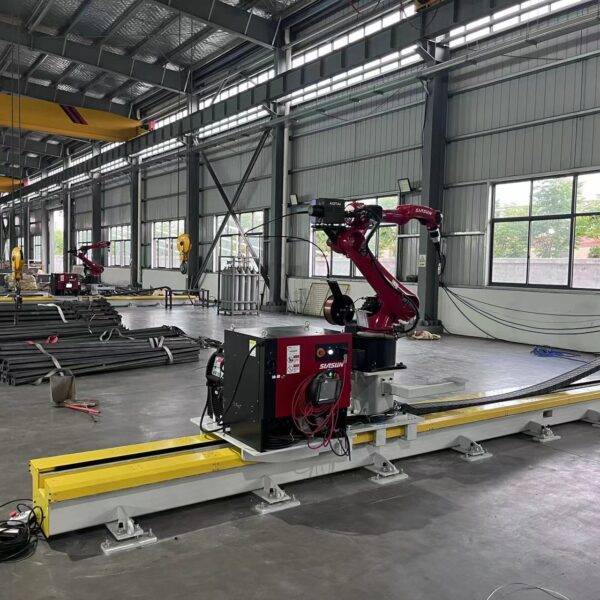
| Rail-mounted 7-axis welding robot | Compact single-robot line with 3D scanning | Steel-structure members of similar size |
| Mobile welding robot | Drives to the workpiece; no rail needed | Parts too large or heavy to move to any station |
| Robot welding workstation (this machine) | Positioner turns the part to the best welding angle | Repeat parts up to several tonnes in batches |
| Cobot welding station | Hand-guided teaching, no fence after risk assessment | Small, mixed parts and frequent changeovers |
What Determines the Price of a Robot Welding Workstation
Most workstations fall in the USD 18,000–30,000 range (FOB Qingdao). Where a configuration sits depends on:
| Cost factor | Options | How it affects the price |
|---|---|---|
| Positioner | Single-axis, L-type or C-type; 500–5000 kg+ | Higher capacity and more axes cost more |
| Ground rail | With or without | Extends reach for longer parts |
| Seam finding | Laser seam tracking, arc tracking | Needed when fit-up varies |
| Programming | Offline or teaching-free | Teaching-free reduces programming time on new parts |
| Welding power source | Aotai, Megmeet, Panasonic, Lincoln Electric, Miller | Imported brands cost more; local brands are easier to service in some regions |
| Fixtures | Per part family | Designed to your parts; quoted separately |
| Service | On-site installation and training | Quoted separately, usually about one week on site |
For a quote, send drawings or photos of your parts, their weight, the material and the expected annual quantity.
Delivery, Installation and Support
- Configuration and drawings. Our engineers choose the positioner, fixtures and process from your parts.
- Production and factory test. Lead time is 20–45 days depending on the configuration. The system is assembled and test-welded before shipment.
- Site preparation. Prepare a level floor, the electrical supply and shielding gas, and plan the safety fencing around the cell.
- Installation and training. On-site installation and operator training usually take about one week and are quoted separately. Operators learn programming, daily operation and routine maintenance.
- After-sales support. 24-month warranty on the whole machine, consumables excluded, with remote technical support for software and process questions.
Fixture Design Tips
In a workstation, the fixture decides weld quality as much as the robot does. Good fixtures follow a few rules:
- Locate every part on the same datum features that the drawing uses.
- Keep clamps out of the torch path and away from the arc.
- Make loading quick and foolproof, so a part can only go in one way.
- Design for consistent fit-up gaps; the robot repeats exactly what the fixture gives it.
- Allow access for the torch at the best welding angle after the positioner turns.
Common Problems and How the Workstation Handles Them
Repeat-part welding is where a workstation shines, but only if these points are handled:
| Problem | Typical cause | How the system handles it |
|---|---|---|
| Weld position is never ideal | Part is fixed on a flat table | The positioner turns the part so seams are welded flat or horizontal |
| Fit-up varies between batches | Upstream cutting and bending tolerances | Fixtures fix the position; laser seam tracking or arc tracking corrects the rest |
| Round seams show start-stop marks | Re-positioning by hand | The positioner rotates in sync with the robot for one continuous weld |
| Positioner struggles with a heavy part | Centre of gravity far from the rotation axis | Capacity is selected for both weight and centre-of-gravity offset |
| Robot waits during loading | Single-station layout | A two-station layout lets one part be loaded while the other is welded |
Before You Buy: A Workstation Checklist
These answers decide the positioner, fixture and layout:
- Part drawings, weight and centre of gravity.
- Annual quantity and batch sizes.
- Target cycle time per part.
- Seams that need the part turned: round, multi-face or vertical-up seams.
- Whether one or two stations are needed.
- Available floor space for the fenced cell.
- Electrical supply, shielding gas and fume extraction.
Daily and Periodic Maintenance
| Interval | Task |
|---|---|
| Every shift | Clean the nozzle and remove spatter; check the contact tip and replace it when the bore is worn; check the wire feed and wire stock; confirm shielding-gas flow |
| Weekly | Check torch cables and hoses for wear; check gas connections for leaks; clean the torch cleaning station or anti-spatter unit if fitted |
| Monthly | Clean spatter from fixtures and locating pins; check the positioner ground connection; check clamp wear |
| Yearly | Service the positioner reducers and the robot as specified by the manufacturers |
Follow the robot and power-source manufacturers' manuals for reducer grease and battery replacement intervals. Back up robot programs and welding procedures after every change.
Safety
- Enclose the cell with fencing and interlock the doors with the robot controller.
- Use light curtains at the loading side if operators load while the robot welds at the other station.
- Protect operators from arc light with screens at the loading area.
- Fit fume extraction above or behind the positioner.
Typical Cell Layouts
| Layout | How it works | Best for |
|---|---|---|
| Single positioner | One positioner in front of the robot; load, weld, unload | Long weld times per part or low volumes |
| Two stations | Two positioners or tables; the robot welds at one while the other is loaded | Repeat parts where loading takes a large share of the cycle |
| Positioner with ground rail | The robot travels on an optional ground rail to reach longer parts | Long frames and booms that exceed the robot reach |
Advantages and Limitations
Advantages
- Every seam in the best welding position
- Fastest cycle for repeat parts
- Handles parts from small brackets to several tonnes
- Within the typical price range of USD 18,000–30,000
Limitations
- Needs fixtures for each part family
- Parts longer than the positioner and rail are better on a gantry or cantilever welding robot
- For very small batches with frequent changes, a cobot welding station is quicker to set up
- Needs a fenced cell
Wire Size Reference for MAG Welding
Typical current windows for solid-wire MAG welding. The process library selects parameters automatically, but this table helps when you plan wire stock and plate thickness.
| Wire Ø | Short-circuit (A) | Globular (A) | Spray (A) | Typical plate |
|---|---|---|---|---|
| 0.8 mm | 40–120 | 120–170 | 170–200 | 0.8–4.0 mm |
| 1.0 mm | 60–140 | 140–190 | 190–300 | 2.0–8.0 mm |
| 1.2 mm | 80–180 | 180–240 | 240–400 | from about 4 mm |
| 1.6 mm | 130–220 | 220–280 | 280–500 | from about 8 mm |
Short-circuit transfer runs at about 14–22 V, globular transfer at about 22–26 V (the spatter zone to avoid), and spray transfer above 26 V.
Robot Welding Workstation FAQ
Which positioner do I need?
Single-axis positioners suit long parts such as beams and shafts; L-type positioners suit boxes and multi-face parts; C-type positioners give full access around frames and booms. Capacity ranges from 500 kg to over 5000 kg.
Does the positioner move while the robot welds?
Yes. The positioner is synchronized with the robot controller, so circumferential and curved seams are welded in one continuous pass.
How much does a robot welding workstation cost?
Most configurations are between USD 18,000 and 30,000, FOB Qingdao, depending on the positioner, rail and seam-finding options.
Is it suitable for small batches?
It is best for repeat parts. For very small batches with frequent changes, a cobot welding station is quicker to program.
Can the welds meet AWS D1.1 requirements?
Welding procedures can be qualified to ISO, AWS D1.1 and classification-society rules such as ABS, LR and CCS, for your specific joints and materials.
What is the lead time?
Lead time is 20–45 days depending on the configuration. Installation and training take about one week on site and are quoted separately.
Do I need a two-station layout?
A two-station layout lets operators load one part while the robot welds the other, which keeps the robot welding. It needs more floor space and a second positioner or table; we recommend it when loading takes a large share of the cycle.
How is the positioner capacity chosen?
By the part weight and by how far its centre of gravity sits from the rotation axis. A heavy part with a large offset needs more turning torque than its weight alone suggests.
See all welding robots to compare cantilever, gantry, mobile, workstation and cobot systems side by side.
Send us drawings or photos of your parts. We will recommend the positioner and fixture concept, and quote FOB Qingdao.
Get a configuration and quote