2-in-1 Sheet and Tube Laser: Overview
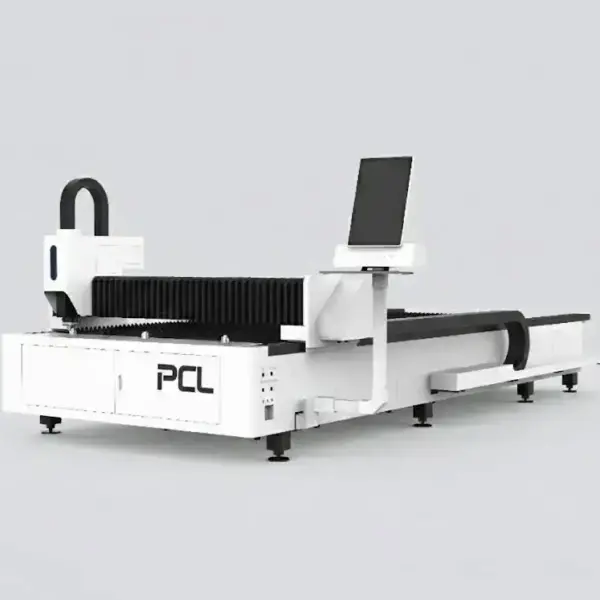
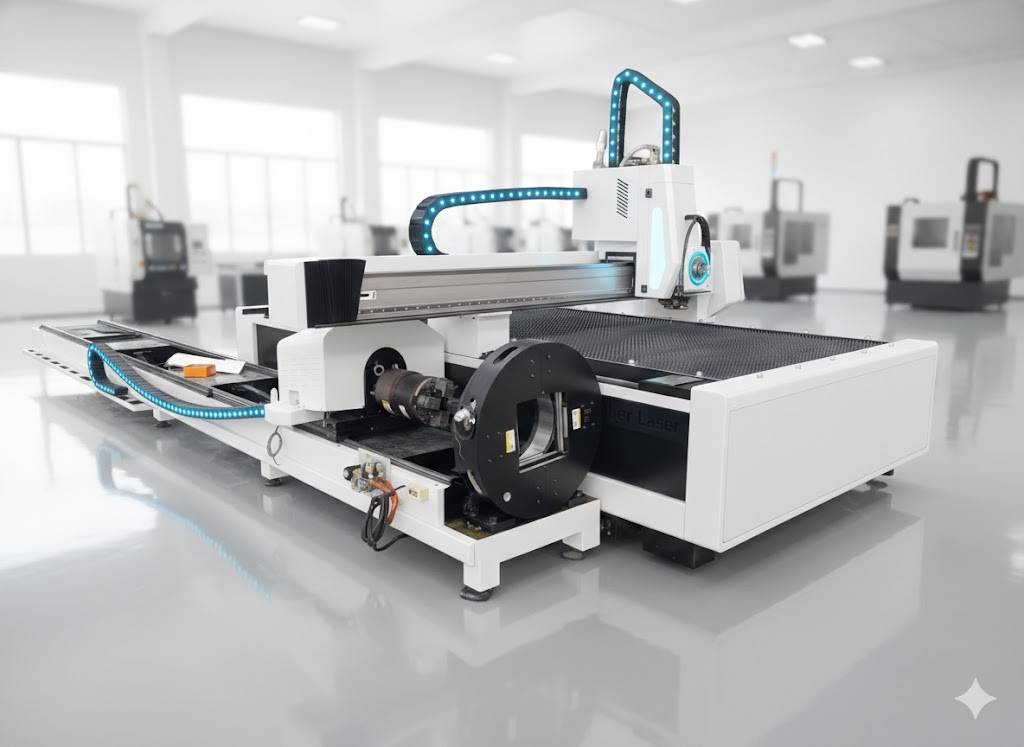
The 2-in-1 machine has a flatbed for sheet and a pneumatic chuck for tubes, sharing one source and one controller. It suits shops that cut mostly sheet and some tube, and do not want to buy and staff a second machine.
Technical Specifications
| Flatbed | 3000 × 1500 mm or 4000 × 2000 mm |
|---|---|
| Tubes | Ø20–220 mm, 6000 mm long; round, square, rectangular, oval |
| Laser source | 1–12 kW; Raycus or IPG |
| Positioning accuracy | ±0.03 mm |
| Max acceleration | 1.0–1.2 G |
| Tube clamping | Pneumatic chuck |
| Certification | CE, ISO 9001 |
| Warranty | 24 months on the whole machine (consumables excluded) |
What the Power Options Cut
Typical maximum thickness from 1 kW to 60 kW; the last column marks the powers this machine can carry. Treat the figures as the ceiling, not the daily working range.
| Laser power | Carbon steel (O₂) | Stainless (N₂) | Aluminium (N₂) | Brass (N₂) | This model |
|---|---|---|---|---|---|
| 1 kW | 10 mm | 5 mm | 3 mm | 3 mm | ✓ |
| 1.5 kW | 16 mm | 6 mm | 4 mm | 3 mm | ✓ |
| 2 kW | 20 mm | 8 mm | 6 mm | 5 mm | ✓ |
| 3 kW | 22 mm | 10 mm | 8 mm | 6 mm | ✓ |
| 4 kW | 25 mm | 12 mm | 10 mm | 8 mm | ✓ |
| 6 kW | 25 mm | 20 mm | 16 mm | 12 mm | ✓ |
| 8 kW | 40 mm | 30 mm | 30 mm | 16 mm | ✓ |
| 12 kW | 40 mm | 40 mm | 40 mm | 16 mm | ✓ |
| 20 kW | 80 mm | 100 mm | 60 mm | 20 mm | – |
| 60 kW | 200 mm | 150 mm | – | – | – |
Maximum thickness is a ceiling, cut slowly and with a rougher edge. Plan daily production a few millimetres below it, and confirm with the cutting chart of the exact source and head in your quotation.
Typical Cutting Speeds
| Thickness | 1.5 kW | 3 kW | 6 kW | 12 kW |
|---|---|---|---|---|
| 2 mm | 5.0 | 3.8–4.2 | – | – |
| 3 mm | 3.6 | 3.2–3.6 | 3.5–4.2 | – |
| 4 mm | 2.5 | 3.0–3.2 | 3.3–3.8 | – |
| 6 mm | 1.4 | 2.2–2.5 | 2.7–3.2 | – |
| 8 mm | 1.2 | 1.8–2.2 | 2.2–2.5 | – |
| 10 mm | 1.0 | 1.0–1.3 | 2.0–2.3 | 2.0–2.3 |
| 12 mm | 0.8 | 0.9–1.0 | 1.9–2.1 | 3.0–3.5 |
| 16 mm | 0.5 | 0.6–0.7 | 1.2–1.4 | 2.8–3.0 |
| 20 mm | – | 0.5–0.55 | 0.6–0.7 | 1.5–1.6 |
| 25 mm | – | – | 0.4–0.5 | 0.8–1.0 |
| Thickness | 1.5 kW | 3 kW | 6 kW | 12 kW |
|---|---|---|---|---|
| 1 mm | 20 | 28–35 | 40–50 | 50–60 |
| 2 mm | 7 | 18–24 | 25–30 | 40–45 |
| 3 mm | 4.5 | 7–10 | 15–18 | 30–35 |
| 5 mm | 1.5 | 3.0–3.6 | 7–8 | 15–18 |
| 6 mm | 0.8 | 2.0–2.7 | 6–7 | 13–15 |
| 8 mm | – | 1.0–1.2 | 3.5–3.8 | 8–10 |
| 10 mm | – | 0.5–0.6 | 1.6–2.0 | 6.5–7.5 |
| 12 mm | – | – | 1.0–1.2 | 5.0–5.5 |
| 16 mm | – | – | 0.5–0.6 | 2.0–2.3 |
| 20 mm | – | – | 0.2–0.35 | 1.2–1.4 |
Speeds in m/min. Typical values for good-quality cutting; edge requirements, material grade, gas purity and the head change them. Your quotation includes the chart for the exact configuration.
The Honest Trade-Off
One source and one operator for two jobs is efficient as long as tube work is the smaller share. The machine does one thing at a time, though: while it cuts tube, the flatbed waits, and the other way round. Once tube cutting fills whole shifts, or you need tubes above 220 mm or longer than 6 m, a dedicated tube laser is the better investment.

Where It Sits in the PCL Laser Range
| Model | Working area | Power | Best for |
|---|---|---|---|
| GF3012 | 3000 × 1200 mm | 6–60 kW | High power on a compact bed |
| LFP3015 | 3000 × 1500 mm | 1–12 kW | Open single table; standard sheets |
| LFP4020 | 4000 × 2000 mm | 1–30 kW | Dual exchange table for volume |
| LFH4020 | 4000 × 2000 mm | 1–30 kW | High-power plate on a plate-welded bed |
| LFP6020 | 6000 × 2000 mm | 1.5–3 kW | Long sheets at lower investment |
| LFH6020 | 6000 × 2000 mm | 1–12 kW | Large-format production |
| 2-in-1 sheet & tube (this machine) | 3015 or 4020 + tubes Ø20–220 mm | 1–12 kW | Sheet and tube on one machine |
Common Problems and How to Fix Them
| Problem | Usual cause | What to do |
|---|---|---|
| Tube parts out of position | Tube bow or twist not compensated | Run edge-finding before cutting; check chuck jaws |
| Dross under stainless or aluminium | Speed too high, nitrogen pressure too low or focus not deep enough | Lower the speed or raise pressure; move the focus down (negative) as thickness grows |
| Not cutting through | Pierce not finished, focus not positive enough on oxygen cuts, dirty protective window | Let all pierce stages finish; raise focus in 1 mm steps; clean or replace the window |
| Parts tip up and hit the head | Small parts falling between slats | Leave micro-joints; replace worn slats; cut small parts last |
What Decides the Price
| Item | Options | Effect |
|---|---|---|
| Laser source | Brand (Raycus, IPG, Max) and power | The largest single item; higher power costs more and needs a bigger chiller and supply |
| Cutting head | Raytools or WSX auto-focus | Auto-focus and protection against collisions |
| Drive | Servo brand, rails and racks | Accuracy over the years |
| Bed | 3015 or 4020 | Larger bed for larger sheets |
| Tube unit | Pneumatic chuck, Ø20–220 mm × 6 m | Adds tube cutting without a second machine |
The 2-in-1 machine is quoted on request.
From Inquiry to Production
- Parts and samples. Send typical sheet parts and tube parts with sizes and materials.
- Configuration. We fix the source, head, table and options, and send a layout with floor space, power, gas and extraction connections.
- Build and test. The machine is assembled and tested before shipment; lead time is confirmed in the quotation.
- Site preparation. Level floor, power supply, assist gas and compressed air, and fume extraction ready before arrival.
- Installation and training. Quoted with the machine; operators learn nesting, cutting parameters, daily checks and simple fault finding.
- Support. 24-month warranty on the whole machine, consumables excluded.
Before You Order
- Share of sheet work and tube work in your hours.
- Largest tube and its length.
- Space along the machine for 6 m tubes.
- Who will program sheet and tube parts.
Maintenance
| When | What |
|---|---|
| Daily | Check and clean the protective window; check nozzle condition and centring; check gas pressures. Check the chuck jaws. |
| Weekly | Remove slag; clean rails, racks and the chuck; drain the air filter. |
| Periodically | Replace slats; lubricate rails and racks; check chuck air seals; change chiller water. |
Safety
Laser light reflected from the sheet is invisible and can injure eyes, so the cutting area must be enclosed or fenced off and the door interlocks must stay working. Keep the extraction running and its filters clean; dust in the bed and filters can catch fire, especially after aluminium. Keep oxygen equipment free of oil and grease, and secure gas cylinders.
2-in-1 Laser FAQ
What tubes can it cut?
Ø20–220 mm, up to 6000 mm long, in round, square, rectangular and oval sections.
Which flatbed sizes are there?
3000 × 1500 mm or 4000 × 2000 mm.
Can it cut sheet and tube at the same time?
No. It switches between flatbed and chuck.
When is a separate tube laser better?
When tube work fills most shifts, or tubes are larger than 220 mm or longer than 6 m.
Does switching between sheet and tube take long?
The machine switches between flatbed and chuck mode; most of the time goes into loading the tube or the sheet.
Is the tube accuracy the same as on a tube laser?
Positioning accuracy is ±0.03 mm; for high tube volumes a dedicated tube laser handles loading and long tubes better.
Compare all fiber laser cutting machines side by side in our selection guide.
Tell us your sheet and tube mix. We work out whether a 2-in-1 or two machines pays off better.
Get a quote