H-Beam Production Line with Magnetic Crawler for Wind Tower fabrication
In this article
Optimizing H-Beam Fabrication for Wind Tower Internals
In the fabrication of wind turbine towers, the structural integrity of internal platforms, ladders, and cable supports relies heavily on the precision of H-beam processing. These components must adhere to the strict tolerances required for circular shell integration. The introduction of a magnetic crawler Plasma Cutting system into the H-Beam Production Line addresses the specific geometric challenges posed by these large-scale structures. Unlike stationary CNC lines, the magnetic crawler offers a mobile, high-stability platform that maintains constant contact with the workpiece, ensuring that thermal cutting operations remain precise even across long spans of structural steel.
From an industrial engineering perspective, the throughput of a wind tower facility is often throttled by the manual rework required when beams do not fit the curvature of the tower sections. By automating the plasma cutting process with a crawler mechanism, facilities can achieve repeatable dimensional accuracy that minimizes secondary grinding and manual fit-up.
Maximizing Intersection Accuracy in Complex Geometries
One of the most critical aspects of wind tower H-beam fabrication is the intersection where the beam meets the inner diameter of the tower shell. These are rarely simple 90-degree cuts. The intersection profile must account for the radius of the tower, requiring a sophisticated saddle or complex curve cut.
Geometric Mapping and Path Control
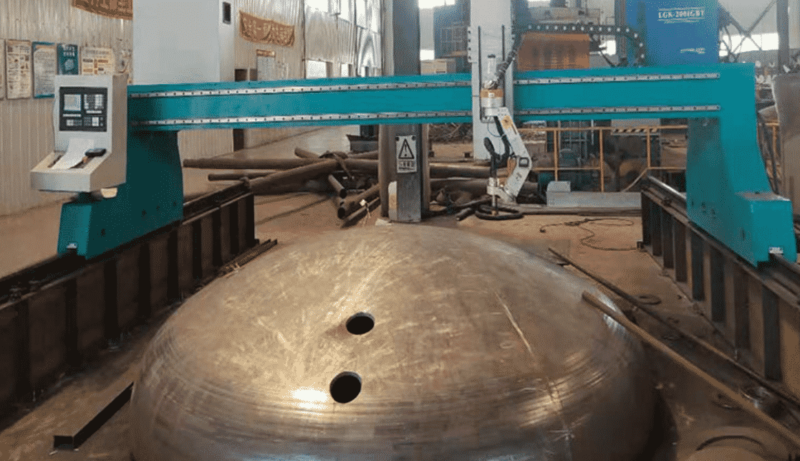
Magnetic crawlers equipped with multi-axis plasma heads utilize localized encoders and path-following software to map the H-beam’s flange and web positions. This allows for real-time adjustments to the torch path. Intersection accuracy is maintained by calculating the exact kerf compensation needed for the specific thickness of the H-beam. When the crawler moves along the beam, the magnetic adhesion eliminates the vibrations that typically plague wheeled systems, ensuring that the plasma arc remains steady as it transitions from the web to the flange.
Mitigating Thermal Distortion
Thermal management is essential for maintaining accuracy. Plasma cutting generates a localized heat-affected zone (HAZ). Industrial engineers favor magnetic crawlers because they allow for synchronized travel speeds that optimize the heat input. By maintaining a constant standoff distance via arc voltage height control (AVHC), the system prevents the dimensional deviations that occur when the torch-to-plate distance fluctuates. This precision ensures that the H-beam’s final length and profile match the 3D CAD model within tolerances of +/- 1.0mm, a prerequisite for efficient wind tower assembly.
Advanced Beveling for High-Strength Structural Joints
Wind tower internals are subjected to constant vibration and dynamic loading. Consequently, the weld preparations on H-beams must meet stringent deep-penetration requirements. Automated plasma beveling integrated into a magnetic crawler system allows for the creation of V, Y, K, and X-shaped bevels without moving the beam to a separate workstation.
Multi-Angle Torch Manipulation
The crawler’s plasma torch head is often mounted on a motorized tilt-and-rotate assembly. This configuration enables the system to perform bevel cuts on both the flanges and the web of the H-beam. For wind tower applications, where the H-beam might serve as a primary load-bearing mezzanine support, the ability to produce a clean, dross-free bevel is paramount. The plasma arc is capable of handling the heavy wall thicknesses typical of structural H-beams, providing a consistent edge preparation that is ready for immediate assembly.
Edge Quality and Metallurgical Integrity
Modern high-definition plasma power sources used in these lines produce a constricted arc with higher energy density. This results in a narrower kerf and a perpendicularity that meets ISO 9013 Range 3 or 4 standards. For the industrial engineer, this means the metallurgical properties of the H-beam are preserved, and the risk of edge cracking or porosity during subsequent joining processes is significantly reduced.
Low Maintenance Requirements in Heavy Industrial Environments
Maintenance downtime is a critical KPI in any H-beam production line. Plasma cutting systems are inherently robust, designed to operate in the dusty, high-temperature environments typical of steel fabrication shops. Unlike more sensitive optical systems, plasma components are built for high duty cycles and ease of service.
Consumable Life and Component Durability
The primary maintenance focus in a plasma-based H-beam line is the management of consumables—nozzles, electrodes, and swirls. Modern plasma cutting technology incorporates “long-life” electrode designs that increase the number of pierces and the total linear meters of cut per set. Because the magnetic crawler operates on a simple mechanical rail or directly on the steel surface, it lacks the complex rack-and-pinion systems or sensitive linear guides that require frequent lubrication and protection from metallic dust.
Modular System Design
Industrial engineers prioritize systems where the power source and the motion controller are modular. In a magnetic crawler setup, if the torch head or a motor driver requires service, the components can be swapped out in minutes. This modularity ensures that the H-beam production line maintains a high OEE (Overall Equipment Effectiveness) rating. Furthermore, the lack of complex mirrors or gas-tight delivery tubes reduces the specialized training required for the maintenance staff, allowing for faster internal troubleshooting.
Strategic Implementation in Wind Tower Workflows
Integrating a magnetic crawler into the H-beam production line shifts the fabrication bottleneck from cutting to assembly. By utilizing H-beam production automation, manufacturers can feed the wind tower shell assembly stations with perfectly prepped components just-in-time.
Streamlining Material Handling
Traditional H-beam processing requires heavy cranes to move beams between cutting, beveling, and cleaning stations. The magnetic crawler brings the machine to the work. Once the H-beam is placed on the conveyor or support bed, the crawler performs all necessary cuts and bevels in a single pass. This reduction in material handling not only increases safety but also decreases the risk of mechanical damage to the beams.
Data Integration and Traceability
In the wind energy sector, traceability is mandatory. Plasma cutting systems integrated with CNC crawlers can log cutting parameters, timestamps, and operator IDs for every H-beam processed. This digital footprint is essential for quality assurance audits and ensures that every component used in the wind tower meets the engineering specifications for the project’s design life.
Conclusion
The application of magnetic crawler plasma cutting in H-beam production lines represents a focused, high-efficiency solution for Wind Tower fabrication. By concentrating on intersection accuracy, the system ensures perfect fit-up against curved tower walls. The ability to perform complex beveling in situ reduces the need for secondary processing, while the robust nature of plasma technology ensures that maintenance remains a minor operational footnote rather than a production hurdle. For the industrial engineer, this technology provides the necessary balance between precision, durability, and throughput, directly contributing to the lower cost of energy in the wind sector.





