Beam Processing Center with Arc Voltage Control for for Wind Tower fabrication
In this article
- Optimization of Wind Tower Structural Components via Plasma Processing
- The Role of Arc Voltage Control (AVC) in Dimensional Stability
- Mechanical Principles of AVC Integration
- Achieving High Intersection Accuracy for Complex Geometries
- H-Beam Low Maintenance and Operational Reliability
- Non-Contact Processing Advantages
- Debris Management and Slag Control
- Advanced Beveling Capabilities for Weld Preparation
- Conclusion: Systematic Throughput Gains
Optimization of Wind Tower Structural Components via Plasma Processing
In the sector of utility-scale wind energy, the structural integrity of tower internals and foundation supports relies on the precision of heavy-duty steel processing. A Beam Processing Center designed for Wind Tower fabrication must address the challenges of handling large-scale H-beams, channels, and heavy plates with high repeatability. The transition from manual layout and mechanical cutting to automated Plasma Cutting environments has redefined the throughput capacities of modern fabrication facilities.
Industrial engineers prioritize systems that minimize material handling and maximize “arc-on” time. For wind tower components—such as internal platforms, ladder supports, and flange reinforcements—the accuracy of the cut determines the efficiency of the subsequent assembly phases. By implementing a centralized processing hub, manufacturers can execute complex geometries in a single pass, eliminating the need for secondary grinding or manual corrections.
The Role of Arc Voltage Control (AVC) in Dimensional Stability
One of the most critical technical features in high-definition plasma systems is Arc Voltage Control. In the context of wind tower fabrication, raw material is rarely perfectly flat or uniform. Long-span H-beams and thick plates often exhibit slight camber, sweep, or surface irregularities. Without real-time compensation, the distance between the plasma torch and the workpiece—the standoff distance—would fluctuate, leading to inconsistent kerf widths and degraded cut quality.
Mechanical Principles of AVC Integration
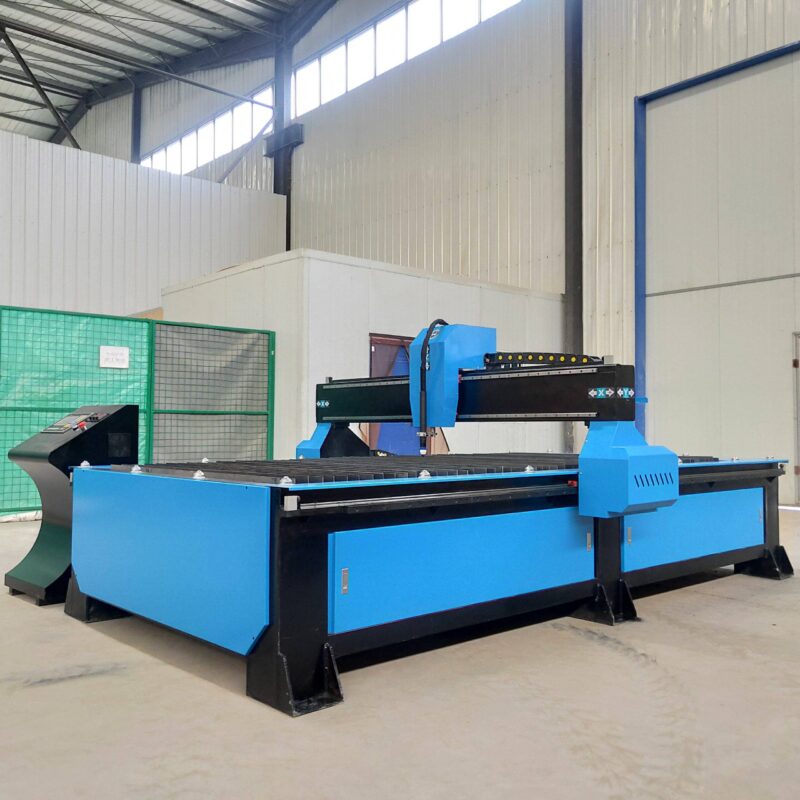
AVC operates by monitoring the electrical potential between the electrode and the material. As the physical distance changes due to material warping, the voltage varies proportionally. The beam processing center’s CNC logic interprets these voltage shifts and instantly adjusts the Z-axis height. This continuous modulation ensures that the plasma arc remains at its optimal focal point. For wind tower components, this results in a uniform heat-affected zone (HAZ) and consistent edge squareness, which are vital for meeting stringent structural codes.
Achieving High Intersection Accuracy for Complex Geometries
The internal architecture of a wind tower requires numerous structural intersections where beams must interface with curved shell surfaces or other structural members. Achieving high intersection accuracy is a primary requirement for ensuring the load-bearing capacity of the tower. Automated plasma centers utilize multi-axis robotic heads or specialized gantry systems to navigate these complex 3D paths.
When cutting holes or coping beam ends for interlocking joints, the software must account for the beam’s dimensional tolerances. By utilizing laser probing or mechanical sensing in conjunction with AVC, the system maps the actual profile of the H-beam before the cut begins. This data-driven approach ensures that bolt holes are perfectly aligned and that saddle cuts for pipe-to-beam intersections fit with zero-gap tolerances. This precision reduces the volume of filler metal required during assembly and ensures that the structural load is distributed according to the original engineering specifications.
H-Beam Low Maintenance and Operational Reliability
From an operational expenditure (OPEX) perspective, H-beam low maintenance is a significant advantage of plasma-based processing centers over traditional mechanical methods. Mechanical drilling and sawing systems involve high-wear components such as drill bits, saw blades, and coolant systems that require frequent replacement and calibration.
Non-Contact Processing Advantages
Plasma cutting is a non-contact thermal process. Because there is no physical force exerted on the tool, the system experiences significantly less mechanical stress. The primary wear items are limited to the nozzle, electrode, and swirl ring, which can be replaced in minutes without complex recalibration. In a high-volume wind tower production line, this translates to higher machine uptime and lower labor costs associated with tool maintenance. Furthermore, the absence of cutting fluids simplifies the workspace and reduces the environmental footprint of the fabrication facility.
Debris Management and Slag Control
Modern beam centers are engineered with integrated fume extraction and slag collection systems. By containing the byproducts of the thermal cut, the internal mechanical components of the gantry—such as linear rails and ball screws—are protected from abrasive dust. This engineering focus on component protection ensures that the machine maintains its precision over a multi-decade service life, even in the harsh environments typical of heavy steel fabrication.
Advanced Beveling Capabilities for Weld Preparation
Wind tower components are subjected to extreme fatigue and rotational loads, necessitating full-penetration welds on many structural joints. Automated plasma beveling is essential for creating the V, Y, X, and K-shaped profiles required for these high-strength connections.
Precision Beveling with Multi-Axis Heads
The integration of a tilt-rotator head allows the plasma torch to deviate from the vertical plane, cutting angles up to 45 or 50 degrees. During these maneuvers, the Arc Voltage Control system remains active, compensating for the increased distance the arc must travel when the torch is tilted. This ensures that the bevel angle remains constant throughout the entire length of the cut, regardless of any material deformation.
Surface Quality and Secondary Operations
High-definition plasma systems produce a surface finish that often requires no further preparation before assembly. By controlling the gas flow (typically oxygen or nitrogen mixtures) and the cutting speed, the system minimizes dross formation. For wind tower manufacturers, the ability to produce a clean, beveled edge directly on the beam processing center eliminates the need for manual grinding stations, which are both labor-intensive and prone to human error.
Conclusion: Systematic Throughput Gains
The implementation of a beam processing center equipped with AVC represents a strategic investment in technical efficiency for Wind Tower fabrication. By prioritizing Plasma Cutting for its versatility and speed, and leveraging the precision of automated voltage monitoring, manufacturers can achieve levels of intersection accuracy that were previously unattainable with manual methods. The shift toward low-maintenance H-beam processing ensures that production schedules remain consistent, while advanced beveling capabilities provide the foundational quality required for high-performance structural components in the renewable energy sector.






