H-Beam Production Line with Magnetic Crawler for Steel Structure
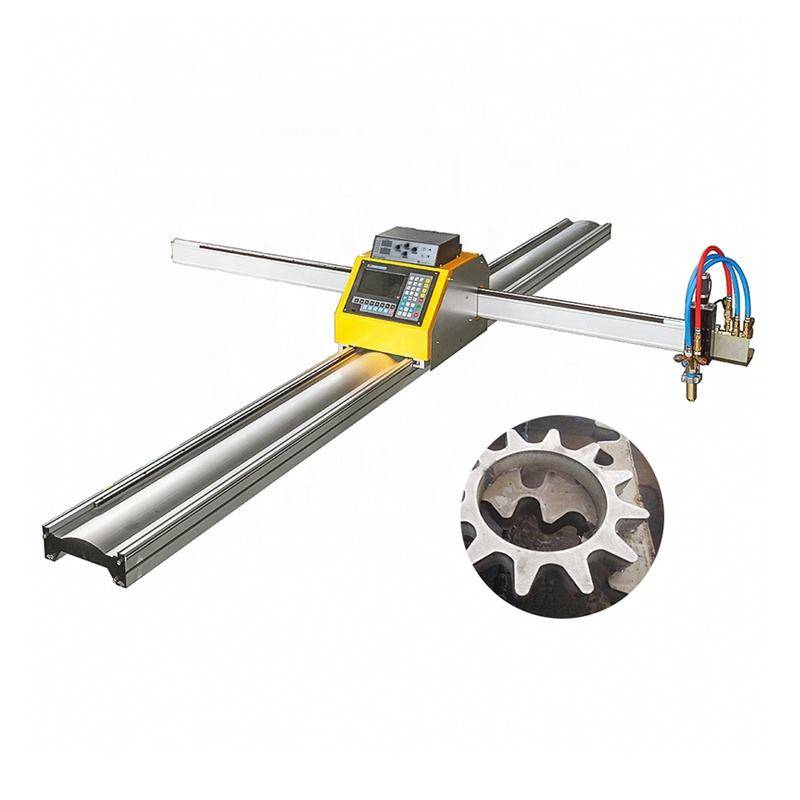
In this article
- The Engineering Logic of Magnetic Crawlers in H-Beam Fabrication
- Mechanical Stability and Thermal Management
- Precision in Plasma Intersection and Geometric Accuracy
- Automated Beveling for High-Strength Joints
- Operational Efficiency and Low Maintenance Requirements
- Consumable Life and System Durability
- Data Integration and Workflow Optimization
- Conclusion: The Future of Structural Steel Processing
The Engineering Logic of Magnetic Crawlers in H-Beam Fabrication
In the domain of structural steel fabrication, the H-beam serves as the primary load-bearing element. Transitioning from manual layout to automated production lines requires a sophisticated approach to torch movement. The implementation of a magnetic crawler system represents a significant shift in how plasma torches interact with large-scale workpieces. Unlike traditional gantry systems that rely on external rails, a magnetic crawler utilizes high-strength permanent magnets or electromagnets to adhere directly to the flange or web of the H-beam.
From an industrial engineering perspective, this direct adhesion eliminates the vibration and mechanical backlash often associated with long-distance rail travel. The crawler provides a localized, stable platform for the plasma head, ensuring that the distance between the nozzle and the steel surface remains constant. This stability is the foundation for achieving high-level plasma intersection accuracy, particularly when performing complex cuts across the varying planes of the beam.
Mechanical Stability and Thermal Management
Plasma Cutting generates significant thermal energy. When processing thick-walled H-beams, the localized heat can cause minor material expansion. A magnetic crawler, by virtue of its physical connection to the beam, moves in concert with the workpiece. This synchronization minimizes the risk of torch-to-plate collisions and maintains the integrity of the arc. The system’s design focuses on high-torque stepper motors and precision gearboxes that translate electronic commands into fluid, linear motion, which is essential for maintaining the narrow kerf widths required in industrial specifications.
Precision in Plasma Intersection and Geometric Accuracy
The primary challenge in H-beam processing is the intersection between the web and the flanges. Traditional cutting methods often struggle with the radius or “root” of the beam, where the thickness increases. Modern plasma systems integrated with Magnetic Crawlers utilize multi-axis rotation to navigate these transitions. By calculating the exact position of the torch relative to the beam’s center line, the system ensures that cope cuts, blocks, and flange thinnings are executed within tolerances of +/- 0.5mm.
Optimizing the Kerf and Heat-Affected Zone
To maximize H-beam structural integrity, the cutting process must minimize the Heat-Affected Zone (HAZ). High-definition plasma systems use constricted arc technology to increase energy density. When combined with the steady travel speed of a magnetic crawler, the resulting cut surface is cleaner, with less dross and minimal metallurgical alteration. This is critical for structural steel that must undergo rigorous non-destructive testing (NDT) after fabrication.
Automated Beveling for High-Strength Joints
Structural steel designs frequently require beveled edges for full-penetration butt welds. The magnetic crawler facilitates automated beveling cycles by allowing the plasma torch to tilt at precise angles—typically ranging from 0 to 45 degrees—while maintaining a consistent travel path. This eliminates the need for secondary grinding or manual edge preparation.
Types of Bevels Achieved via Magnetic Crawler Systems
- V-Type Bevels: Standard preparation for single-sided welding on web sections.
- Y-Type Bevels: Providing a root face to control penetration and reduce filler material consumption.
- K-Type and X-Type Bevels: Applied to heavy flanges to ensure balanced stress distribution across the joint.
The integration of CNC (Computer Numerical Control) allows the crawler to adjust the bevel angle dynamically as it moves along the profile of the H-beam. This is particularly useful for complex architectural steel where the geometry of the intersection changes along the length of the member.
Operational Efficiency and Low Maintenance Requirements
One of the strongest arguments for plasma-based magnetic crawlers in an H-Beam Production Line is the reduction in long-term maintenance. Unlike mechanical cutting tools or complex optical systems, plasma components are designed for high-uptime environments. The magnetic crawler itself is a ruggedized piece of equipment, built to withstand the sparks, dust, and heat inherent in a steel mill or fabrication shop.
Consumable Life and System Durability
Plasma torches used in these lines are engineered for longevity. The electrodes and nozzles are cooled via specialized liquid systems or high-velocity air, extending their operational life even during continuous multi-shift operations. Because the magnetic crawler has fewer moving parts than a full-scale bridge gantry, the mechanical wear points are limited to the drive wheels and the torch height control (THC) mechanism. This results in a lower Mean Time To Repair (MTTR) and higher overall equipment effectiveness (OEE).
Dust and Debris Management
In a production line environment, steel dust and slag can compromise precision machinery. Magnetic crawlers are typically equipped with scrapers and shielded drive components to prevent metallic particles from interfering with the magnetic grip or the internal electronics. This “industrial hardening” ensures that the magnetic crawler integration remains a reliable asset over years of heavy use.
Data Integration and Workflow Optimization
Modern H-beam production lines operate on a “file-to-factory” workflow. Building Information Modeling (BIM) data, typically in DSTV or STEP formats, is fed directly into the crawler’s control system. The software translates the 3D model into specific plasma cutting paths. The crawler executes these paths with high repeatability, ensuring that every beam produced is an exact replica of the digital model.
Throughput Analysis
By streamlining the cutting and beveling into a single station, the production line reduces the amount of material handling required. Each time an H-beam is moved, there is a risk of damage or misalignment. By bringing the magnetic crawler to the beam—or moving the beam through a stabilized crawler station—the process becomes more linear. The time saved on setup and manual measurement contributes directly to a faster return on investment (ROI) for the facility.
Conclusion: The Future of Structural Steel Processing
The reliance on plasma cutting technology within an H-beam production line, supported by the stability of magnetic crawler systems, addresses the dual needs of precision and productivity. By focusing on intersection accuracy and automated beveling, engineers can ensure that the steel members meet the stringent safety codes required for modern infrastructure. The low maintenance profile of these systems ensures that the production line remains active, minimizing downtime and maximizing the output of high-quality structural components.





