H-Beam Production Line with Magnetic Crawler for Oil & Gas Tanks
In this article
- Advanced Plasma Integration in H-Beam Production
- Achieving Superior Intersection Accuracy
- Kinematic Control and Path Optimization
- Magnetic Crawler Technology for Precision Guidance
- Stability in Heavy Industrial Environments
- High-Precision Beveling for Heavy-Walled Structures
- Low Maintenance and Industrial Durability
- Process Efficiency and Throughput Analysis
- Conclusion on Structural Integrity
Advanced Plasma Integration in H-Beam Production
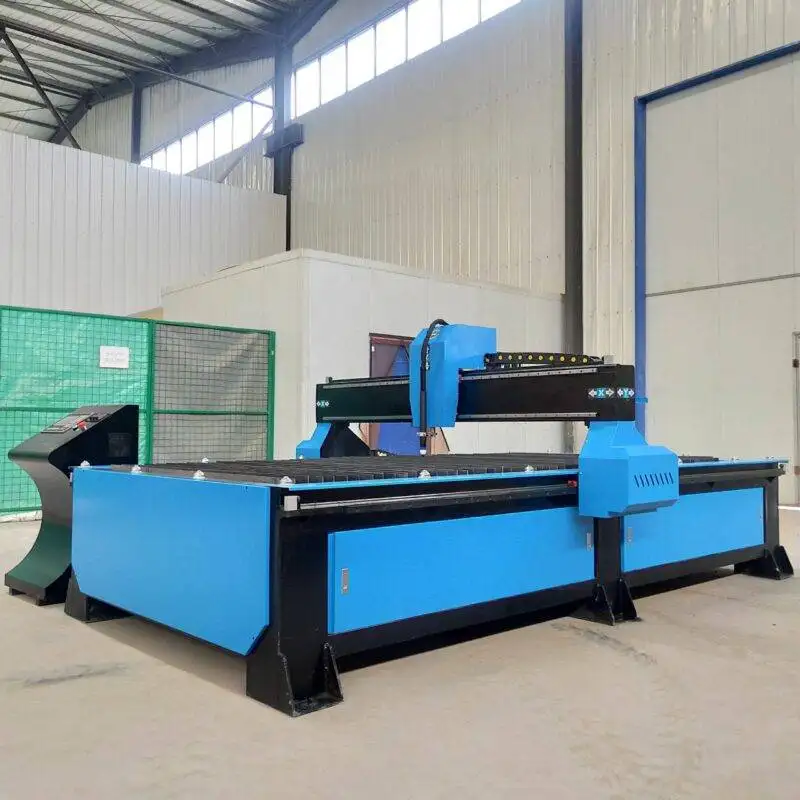
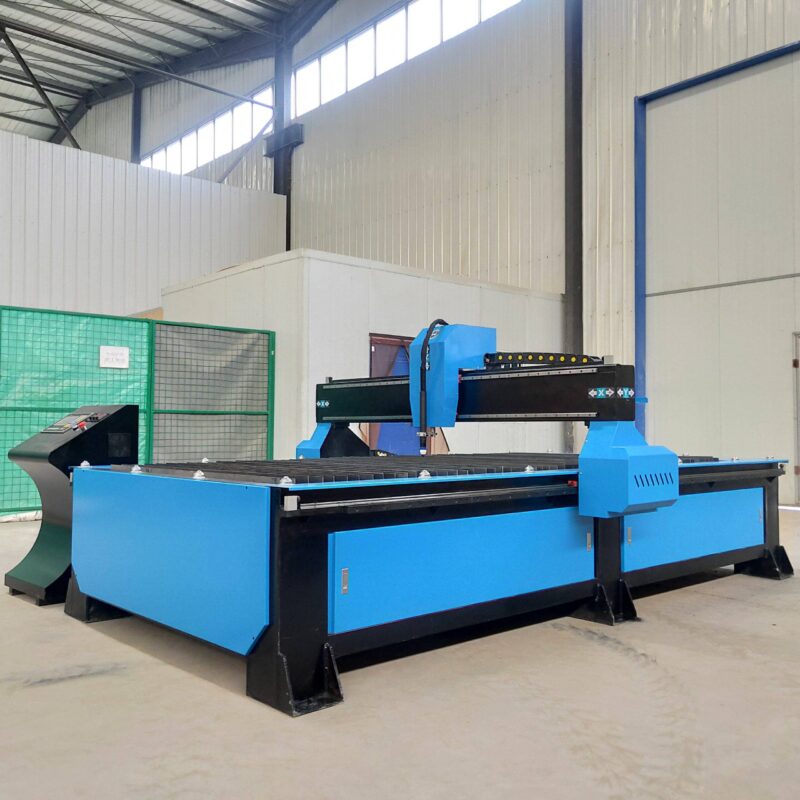
In the heavy fabrication sector, specifically for Oil & Gas tank construction, the H-beam serves as a foundational structural element. The efficiency of a production line is measured by its ability to process these beams with high repeatability and tight tolerances. Utilizing Plasma Cutting technology within these lines offers a robust solution for thick-walled carbon steel and alloy sections. Unlike mechanical shearing or sawing, plasma provides the flexibility to perform complex 3D cuts and intersections necessary for tank saddles and reinforcing rings.
The industrial engineering focus here is on the plasma cutting duty cycle and its interaction with high-tensile structural steel. By employing high-definition plasma power sources, the production line can maintain continuous operation under heavy loads. The process relies on a constricted ionized gas arc that melts the material, while a high-velocity gas stream removes the molten metal. This allows for rapid processing of H-beam webs and flanges with minimal heat input, reducing the risk of structural warping that could compromise the tank’s circularity or support alignment.
Achieving Superior Intersection Accuracy
Oil & Gas tanks require precise fit-up between structural supports and the cylindrical shell. This necessitates complex intersection cuts where the H-beam meets a curved surface. Standard 2D cutting is insufficient for these geometries. The production line incorporates multi-axis plasma heads capable of articulating around the beam’s profile. This 3D capability ensures that the cut path accounts for the radius of the tank shell, resulting in a gap-less fit that facilitates superior structural integrity.
Kinematic Control and Path Optimization
The accuracy of these intersections is driven by advanced CNC algorithms that calculate the kerf compensation and torch angle in real-time. For an H-beam, the transition from cutting the flange to the web requires seamless motion control to prevent dross accumulation at the corners. High-speed processors in the control unit synchronize the movement of the beam through the conveyor with the plasma torch’s lateral and vertical displacement. This synchronization ensures that the intersection profile remains consistent across hundreds of identical components, minimizing manual rework.
Magnetic Crawler Technology for Precision Guidance
A critical component in the modern H-beam line for tank fabrication is the magnetic crawler. This device is engineered to navigate the surface of the H-beam or the tank shell with high stability. In the context of plasma cutting, the crawler serves as a mobile platform for the torch, providing a consistent standoff distance. Maintaining a constant arc voltage is paramount for edge quality; even slight fluctuations in torch-to-workpiece distance can lead to bevel angle deviations or increased slag.
Stability in Heavy Industrial Environments
The magnetic crawler utilizes high-force permanent magnets or electromagnets to lock onto the steel surface. This is particularly advantageous when cutting large-scale H-beams where traditional gantry systems might reach their physical limits or experience vibration. By mounting the plasma torch on a crawler, the production line gains a localized precision tool that is immune to the slight misalignments of long-travel rail systems. The crawler follows the actual contour of the beam, compensating for any inherent mill camber or sweep in the structural steel.
High-Precision Beveling for Heavy-Walled Structures
In Oil & Gas applications, structural joints must often be prepared with specific bevel profiles to allow for full penetration. Plasma cutting is uniquely suited for this task. The production line can be configured to perform V, Y, and K-style bevels on H-beam ends and web penetrations. The ability to bevel during the primary cutting phase eliminates the need for secondary edge milling, significantly reducing the total man-hours per ton of steel.
Bevel Angle Consistency and Gas Selection
To achieve a consistent beveling angle, the plasma system must manage the arc’s natural tendency to taper. Modern high-definition systems use specialized nozzle designs and secondary shielding gases to constrict the arc, resulting in a square edge or a precisely controlled bevel. For carbon steels typical of tank construction, an oxygen-based plasma gas is used to increase cutting speeds and provide a clean surface finish. For stainless steel components, nitrogen or H35 (hydrogen-argon mix) is preferred to prevent oxidation and ensure the edge is ready for subsequent processing steps.
Low Maintenance and Industrial Durability
One of the primary reasons industrial engineers specify plasma systems for H-beam lines in the energy sector is their low maintenance profile. These production environments are often dusty, subject to extreme temperature fluctuations, and operate 24/7. Plasma torches and power supplies are designed for this ruggedness. Unlike sensitive optical systems that require clean-room conditions for their internal components, plasma systems are relatively simple: they consist of power electronics, gas delivery solenoids, and consumable copper electrodes and nozzles.
Optimizing Consumable Life
Maintenance schedules in a high-volume H-beam line are built around consumable replacement. Engineering the gas flow to include a “soft start” and “soft stop” sequence preserves the electrode’s hafnium insert, extending its life by up to 30%. Modern systems also feature self-diagnostic sensors that monitor coolant flow and gas pressure, alerting operators before a component failure occurs. This predictive maintenance approach ensures that the production line remains active, avoiding the costly downtime associated with more delicate cutting technologies.
Process Efficiency and Throughput Analysis
From a workflow perspective, integrating plasma cutting with magnetic guidance creates a continuous throughput model. The H-beam enters the station, is scanned for dimensional accuracy, and is then processed by the plasma-equipped crawler. The speed of plasma cutting—often exceeding 100 inches per minute on half-inch plate—outpaces traditional oxy-fuel methods by a factor of three or four. This speed, combined with the reduction in secondary cleanup, allows for a leaner manufacturing process.
Furthermore, the integration of nesting software allows the production line to optimize material usage. By calculating the most efficient layout for intersection cuts and holes on the H-beam, scrap rates are minimized. In large-scale tank projects where thousands of tons of steel are used, even a 2% improvement in material utilization represents a significant cost saving. The plasma system’s narrow kerf width contributes to this efficiency, allowing for tighter nesting of complex parts.
Conclusion on Structural Integrity
The ultimate goal of using these advanced technologies is the structural integrity of the Oil & Gas tank. The precision of the plasma-cut H-beam intersections ensures that loads are distributed evenly across the tank’s foundation and support structure. By eliminating fit-up gaps through 3D accuracy and providing clean, beveled edges for joint preparation, the production line delivers components that meet the stringent requirements of API (American Petroleum Institute) standards. The combination of plasma’s reliability, the crawler’s precision, and the CNC’s accuracy represents the pinnacle of current industrial engineering in structural steel fabrication.





