H-Beam Production Line with Magnetic Crawler for LNG Projects
In this article
- Structural Integrity in LNG Infrastructure: The H-Beam Requirement
- Precision Engineering of Intersection Geometries
- Thermal Management and Kerf Compensation
- Advanced Beveling for Full Penetration Requirements
- Operational Efficiency: The Low-Maintenance Advantage
- Reduced Mechanical Wear and Calibration Needs
- Integration into the Digital Workflow
Structural Integrity in LNG Infrastructure: The H-Beam Requirement
Liquefied Natural Gas (LNG) projects represent some of the most demanding environments for structural steel. The support frames for cryogenic tanks, regasification modules, and pipe racks must withstand not only massive static loads but also significant thermal stresses. The H-beam is the fundamental building block of these structures. However, the standard off-the-shelf H-beam rarely meets the precise dimensional requirements for complex LNG plant layouts. This necessitates a production line capable of sophisticated modifications, specifically in the realm of plasma arc stability and geometric preparation.
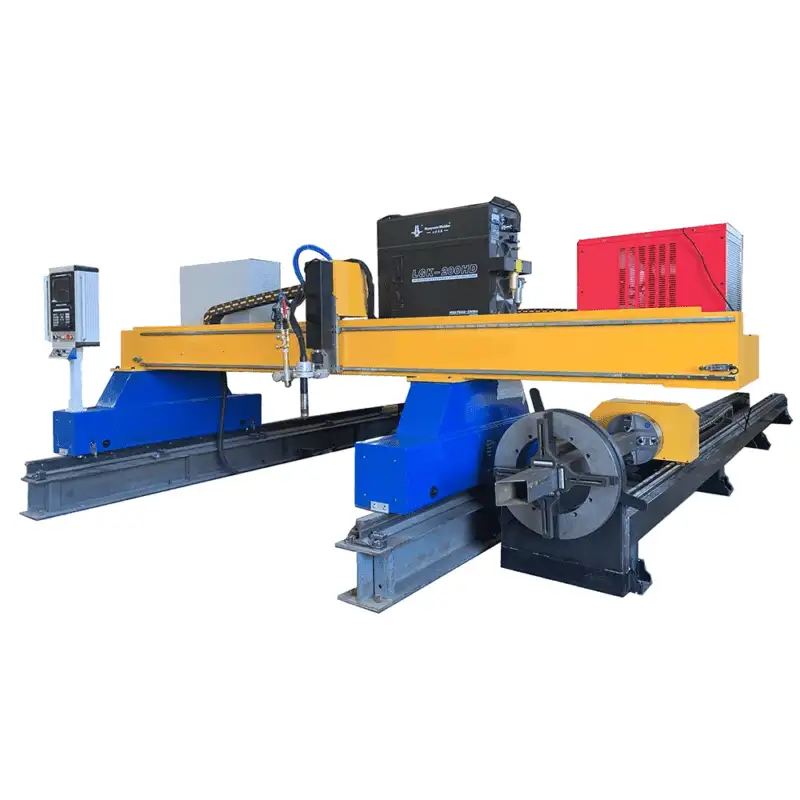
Traditional gantry-based cutting systems often struggle with the sheer scale and the variable surface profiles of heavy-duty H-beams. The introduction of the magnetic crawler represents a paradigm shift in how Plasma Cutting is delivered to the workpiece. By utilizing high-intensity permanent magnets or electromagnets, the crawler adheres directly to the web or flange of the H-beam. This eliminates the vibration and mechanical backlash associated with long-reach gantry arms, providing a stable platform for high-definition plasma torches.
Precision Engineering of Intersection Geometries
One of the primary challenges in LNG structural fabrication is the intersection of secondary beams with the main headers. In a typical pipe rack or module frame, H-beams meet at various angles, requiring complex “bird-mouth” cuts or circular penetrations for piping pass-throughs. The accuracy of these intersections determines the overall structural integrity of the facility. If the fit-up gap exceeds 2mm, the subsequent welding processes face increased risk of burn-through or excessive residual stress.
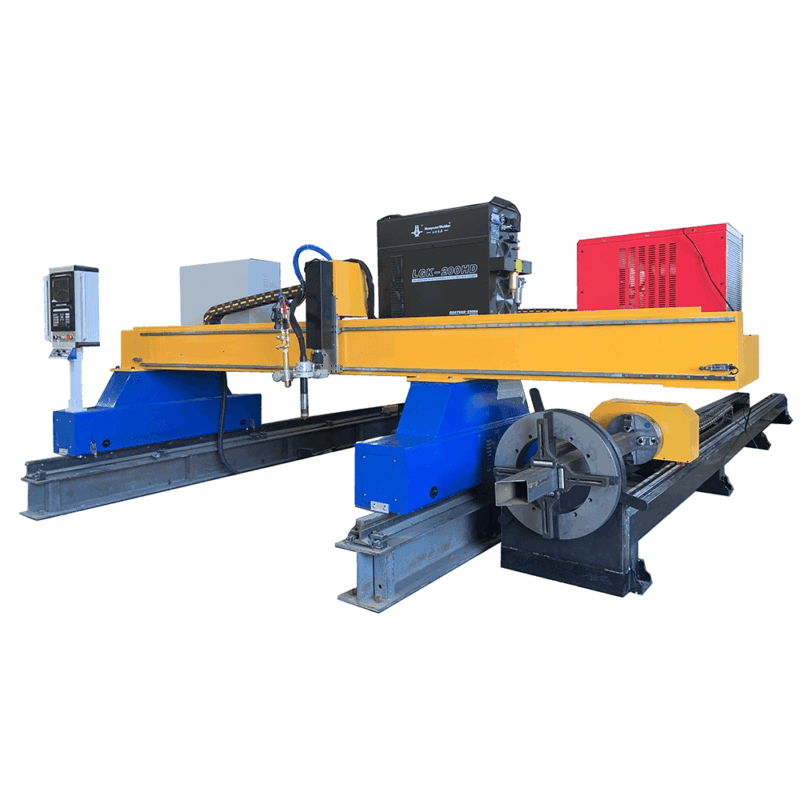
The magnetic crawler system, coupled with multi-axis CNC software, calculates the intersection geometry in real-time. Unlike manual marking and cutting, the plasma torch on a crawler follows a mathematically derived path that accounts for the beam’s actual dimensions rather than theoretical nominal sizes. This is critical because hot-rolled H-beams often exhibit slight flange tilt or web eccentricity. The crawler’s ability to reference the actual surface of the steel ensures that the plasma stream remains perpendicular or at the prescribed bevel angle relative to the material surface at every point of the cut.
Thermal Management and Kerf Compensation
High-definition plasma cutting in H-beam lines requires sophisticated kerf compensation. As the plasma arc melts through the thick carbon steel typical of LNG projects (often ranging from 20mm to 50mm in flange thickness), the width of the removed material—the kerf—must be precisely managed. The CNC controller on the magnetic crawler adjusts the torch path based on the arc voltage and the consumable orifice size. This level of control ensures that the final dimensions of the H-beam intersections are within sub-millimeter tolerances, facilitating rapid assembly in the field without the need for on-site grinding or mechanical adjustments.
Advanced Beveling for Full Penetration Requirements
In LNG structural design, fillet welds are often insufficient for primary load-bearing joints subjected to seismic or thermal cycling loads. Design codes frequently mandate complete joint penetration (CJP) welds. Achieving a CJP weld requires precise edge preparation, specifically V-groove, Y-groove, or K-groove bevels. The magnetic crawler excels in this application by providing a stable, constant-velocity motion that is essential for uniform beveling parameters.
The plasma torch mounted on the crawler is typically equipped with a tilt-and-rotate mechanism (often referred to as a 3D or 5-axis head). As the crawler moves along the flange of the H-beam, the torch can incline up to 45 or 60 degrees. Because the crawler is physically coupled to the beam via magnetic force, the “torch-to-work” distance remains constant even if the beam has slight longitudinal bowing. This constancy is vital; even a 1mm deviation in torch height can significantly alter the bevel angle and the land thickness of the cut, leading to inconsistencies that would fail NDT (Non-Destructive Testing) ultrasonic inspections.
Optimizing the Heat Affected Zone (HAZ)
For LNG applications, the metallurgical properties of the steel near the cut edge are under intense scrutiny. High-speed plasma cutting with oxygen or nitrogen shielding gases minimizes the residence time of the heat source. By maintaining high travel speeds facilitated by the magnetic crawler’s traction, the Heat Affected Zone is kept to a minimum. This ensures that the base metal retains its toughness and ductility—properties that are essential for resisting brittle fracture at low ambient temperatures or in the event of cryogenic liquid exposure.
Operational Efficiency: The Low-Maintenance Advantage
Industrial engineers prioritizing throughput in LNG fabrication facilities favor plasma systems primarily for their robust reliability. Unlike other high-energy beam processes, plasma cutting systems are remarkably resilient to the dusty, high-vibration environments of a structural steel shop. The magnetic crawler itself is a masterpiece of mechanical simplicity. By reducing the number of moving parts compared to a massive bridge gantry, the maintenance requirements are shifted from complex rail alignments to simple consumable management.
The magnetic crawler precision is maintained through rugged drive wheels and high-torque stepper motors that are sealed against metallic dust and slag. In a high-volume H-Beam Production Line, downtime is the primary enemy of profitability. Plasma systems offer a high duty cycle, often capable of 100% operation at maximum amperage. The consumables—nozzles, electrodes, and swirl rings—are designed for rapid change-out, often taking less than 60 seconds. This allows the production line to maintain a continuous flow of prepared H-beams, feeding the assembly and welding stations without bottlenecking.
Reduced Mechanical Wear and Calibration Needs
A significant hidden cost in structural steel fabrication is the recalibration of heavy machinery. Gantry systems can fall out of square due to floor settling or accidental impact. In contrast, a magnetic crawler is “self-aligning” in the sense that its frame of reference is the workpiece itself. This localized approach to machining means that as long as the H-beam is positioned on the conveyors, the crawler will execute the programmed cut with absolute fidelity to the beam’s geometry. The absence of long drive belts, rack-and-pinion systems spanning 20 meters, and complex cable carriers significantly reduces the annual maintenance budget and the requirement for specialized calibration technicians.
Integration into the Digital Workflow
Modern LNG projects utilize BIM (Building Information Modeling) and TEKLA structures for detailing. The H-beam production line integrated with a magnetic crawler can ingest these DSTV or NC1 files directly. The software translates the 3D model into plasma cutting paths, including all necessary bolt holes, copes, and weld preparations. This digital-to-physical transition is seamless. The magnetic crawler acts as the final link in a highly automated chain, ensuring that the engineer’s intent is translated into the steel with zero manual intervention.
In conclusion, the deployment of a magnetic crawler-based plasma cutting system offers a strategic advantage for LNG project contractors. By focusing on the precision of intersections, the consistency of multi-axis beveling, and the inherent low-maintenance nature of the hardware, industrial engineers can guarantee a production line that meets the most stringent international standards. This technological synergy not only reduces the cost per ton of fabricated steel but also significantly enhances the structural reliability of the global energy infrastructure.






