H-Beam Production Line with Laser Seam Tracking for Bridge Trusses
In this article
Advancing Infrastructure Fabrication: The Plasma-Centric H-Beam Line
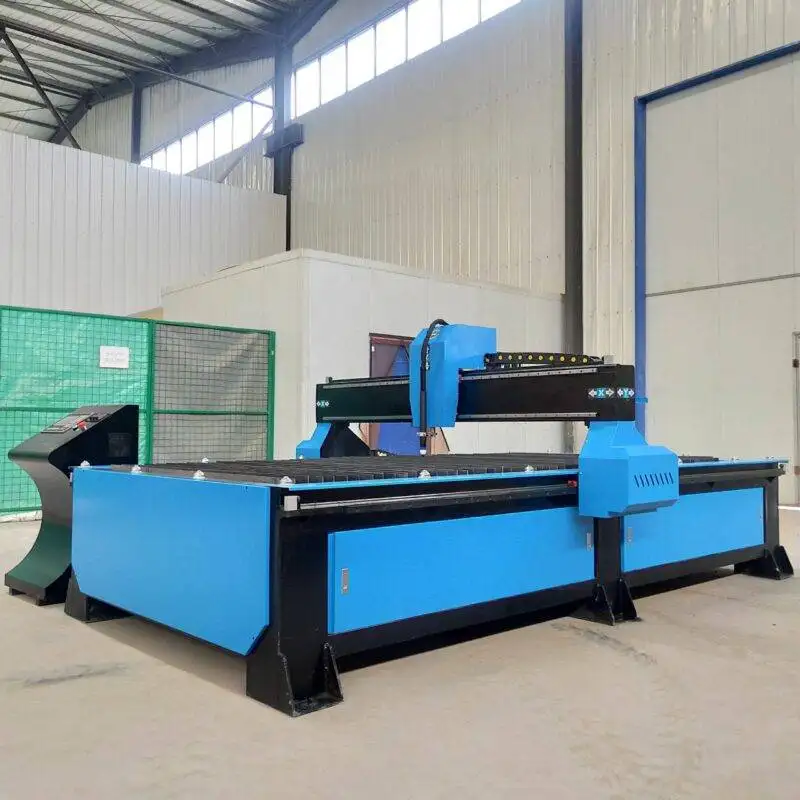
In the domain of heavy structural engineering, the production of H-beams for Bridge Trusses demands a rigorous adherence to dimensional tolerances and metallurgical integrity. The transition toward fully automated H-beam production lines has necessitated a shift in how raw materials are processed, particularly concerning the preparation of structural members that must withstand massive dynamic loads. By centering the production line on high-definition Plasma Cutting technology, engineers can achieve a synergy between high-speed material removal and the surgical precision required for complex truss intersections.
The selection of plasma as the primary cutting medium in bridge fabrication is driven by its ability to handle thick-plate structural steel with significant efficiency. Unlike mechanical sawing or oxygen-fuel processes, modern plasma systems provide a narrower kerf and a significantly reduced heat-affected zone (HAZ), which is critical for maintaining the fatigue resistance of the steel used in bridge chords and diagonals.
Precision Intersection Accuracy in Complex Truss Geometries
Bridge trusses often feature intricate geometries where multiple H-beams converge at specific nodes. The accuracy of these intersections is paramount; even a two-millimeter deviation can result in significant secondary stresses during assembly or, worse, structural failure under load. Plasma cutting systems equipped with multi-axis CNC heads allow for the precise contouring of H-beam webs and flanges to match the exact profile of the mating component.
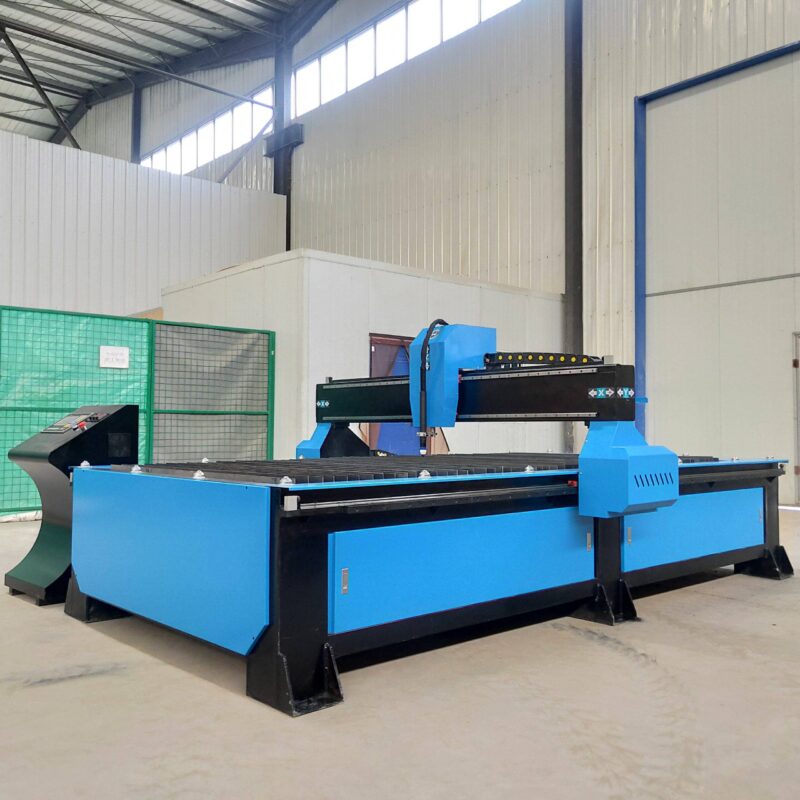
To achieve this level of intersection accuracy, the production line utilizes advanced kinematic algorithms that compensate for the physical dimensions of the plasma arc. The software calculates the lead-in and lead-out paths to ensure that the corners of the H-beam intersections are crisp and free of dross. This precision eliminates the need for manual grinding or secondary fit-up adjustments, directly increasing the throughput of the fabrication shop and ensuring that the structural load paths are aligned exactly as specified by the bridge designers.
Laser Seam Tracking: Mitigating Thermal Distortion
One of the primary challenges in heavy-duty plasma cutting is the management of thermal expansion. As the plasma torch delivers intense heat to the steel, the beam can undergo localized deformation, causing the intended cutting path to drift. To counteract this, industrial-grade laser seam tracking systems are integrated directly into the cutting carriage. These sensors project a laser line or dot onto the surface of the H-beam, scanning the topography in milliseconds.
The data from the laser sensor is fed back to the CNC controller in real-time. If the sensor detects that the flange of the H-beam has bowed due to residual stresses or thermal input, the system automatically adjusts the torch height and lateral position to maintain the correct focal distance and path alignment. This closed-loop feedback loop is essential for long-span bridge trusses where H-beams may exceed 12 meters in length. Without such tracking, the cumulative error over the length of the beam would render the component useless for high-precision bridge assembly.
Advanced Beveling for Full-Penetration Structural Joints
In bridge construction, joints are rarely simple 90-degree cuts. Most structural specifications require V, X, or K-profile bevels to facilitate full-penetration butt welds between the H-beam sections. The ability to perform high-speed beveling within the primary cutting cycle is a significant advantage of plasma-based lines. By utilizing a 5-axis or 6-axis robotic arm or a specialized tilting torch head, the system can chamfer the edges of thick flanges at precise angles (typically 30 to 45 degrees) while simultaneously cutting the profile.
The quality of these bevels is superior to manual oxy-fuel cutting. The plasma arc provides a smoother surface finish, which is a prerequisite for ultrasonic testing (UT) and radiographic testing (RT) of the final welds. By automating the beveling process, the bridge truss fabrication workflow removes the variability of human operators, ensuring that every joint across the entire bridge span meets the same stringent quality standards. Furthermore, the accuracy of the automated bevel ensures a consistent root gap, which is the most critical factor in achieving a defect-free structural connection.
Operational Efficiency and Low Maintenance Architecture
From an industrial engineering perspective, the “uptime” of a production line is as important as its precision. Plasma systems have evolved into highly robust units characterized by low maintenance requirements. Unlike mechanical cutting tools, there are no blades to sharpen or break. The primary consumables—electrodes and nozzles—are designed for quick-change operations, often taking less than two minutes to replace, thereby minimizing downtime.
The design of the H-Beam Production Line incorporates heavy-duty dust collection and slag management systems. Because plasma cutting generates significant particulate matter, integrated downdraft tables or water-injection systems are used to protect the mechanical components of the CNC gantry and the laser tracking sensors. This protective engineering ensures that the sensitive optics of the laser tracking system remain clear of debris, maintaining 24/7 operational capability in harsh fabrication environments.
Optimized Consumable Management and Duty Cycle
Modern plasma power sources utilize “LongLife” oxygen technology, which significantly extends the lifespan of the copper consumables. For an industrial engineer, this translates to lower cost-per-cut and fewer interruptions in the production cycle. In the context of a bridge project requiring thousands of cut meters, the cumulative savings in consumable costs and labor hours are substantial. The high duty cycle of these power sources (often 100% at maximum output) allows the line to run continuously, matching the high-volume requirements of large-scale infrastructure projects.
Integration with CAD/CAM for End-to-End Workflow
The final pillar of a high-performance H-beam line is the seamless integration between the design office and the shop floor. Structural BIM (Building Information Modeling) data is exported directly to the plasma line’s nesting software. This digital thread ensures that the exact dimensions, hole locations, and bevel angles conceived by the bridge engineers are executed by the plasma torch without manual data entry errors. This “digital-to-physical” accuracy is what allows modern bridge trusses to be assembled with the precision of a Swiss watch, despite their massive scale and weight.
By focusing on the precision of plasma technology, the real-time correction capabilities of laser tracking, and the robustness of the mechanical design, industrial engineers can deliver H-beam production lines that redefine the benchmarks for bridge fabrication. The result is a faster construction timeline, lower maintenance costs for the fabrication facility, and, most importantly, a safer and more reliable public infrastructure.





