H-Beam Production Line with 5-Axis Beveling for Pressure Vessels
In this article
Optimizing H-Beam Production Lines for Pressure Vessel Fabrication
In the specialized field of pressure vessel manufacturing, the structural integrity of support skids and saddles is as critical as the vessel shell itself. Industrial engineering workflows now prioritize the automation of H-beam fabrication to ensure that these supports can handle the static and dynamic loads of pressurized systems. The transition from manual layout and mechanical sawing to integrated 5-axis Plasma Cutting lines represents a fundamental shift in throughput capacity and dimensional tolerance management.
The primary challenge in utilizing H-beams for vessel supports involves the complex geometry of intersections. Where a structural H-beam meets the cylindrical curvature of a pressure vessel, a simple straight cut is insufficient. It requires a precise, contoured interface that accounts for both the beam’s profile and the vessel’s radius. Plasma cutting technology, specifically when mounted on a multi-axis robotic or CNC gantry system, provides the necessary degrees of freedom to execute these cuts without the need for manual templates or extensive rework.
The Mechanics of 5-Axis Plasma Beveling
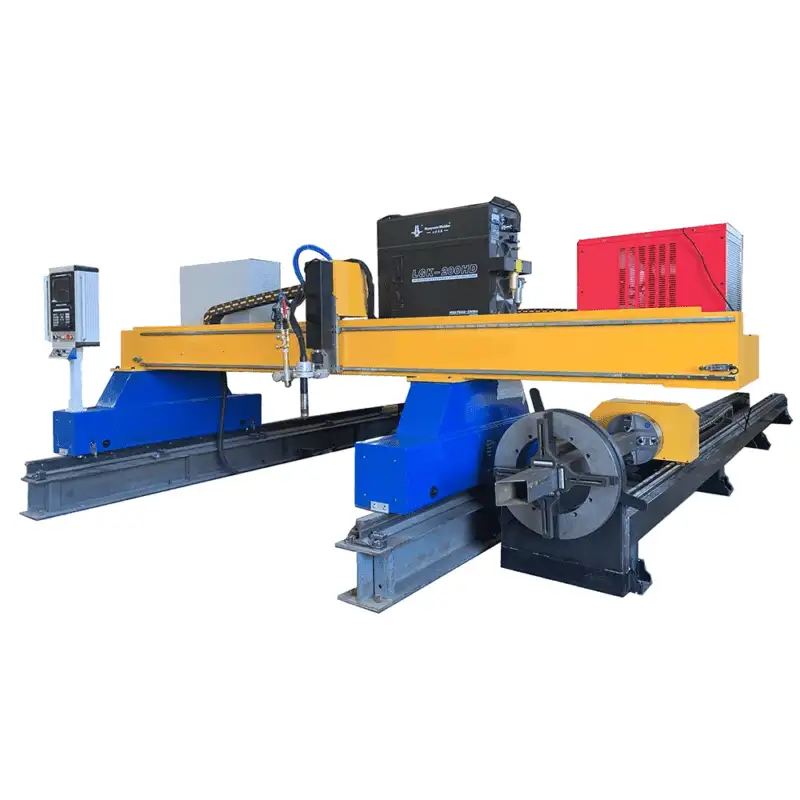
A 5-axis plasma cutting system introduces two rotational axes (typically A and C) to the standard X, Y, and Z linear movements. In the context of H-beam processing, this allows the plasma torch to tilt and rotate around the flange and web sections simultaneously. For pressure vessel manufacturers, this is vital for creating weld preparations (bevels) on the fly. Instead of cutting a beam to length and then using a handheld grinder or a secondary beveling machine to create a V or K-groove, the 5-axis head performs the profile cut and the beveling in a single pass.
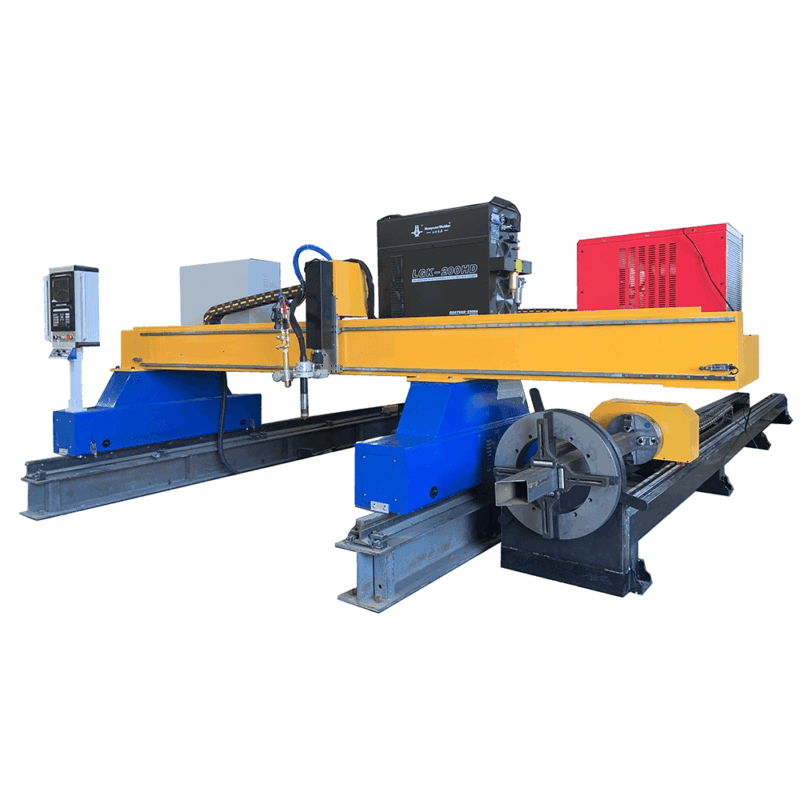
The kinematic software governing these machines must calculate the “true” path of the plasma arc. Because the plasma arc is a localized high-temperature ionized gas stream, its behavior changes when tilted. Advanced CNC controllers compensate for the kerf width variations that occur during angular cutting, ensuring that the root face of the bevel remains consistent across the entire cross-section of the H-beam. This consistency is a prerequisite for the high-quality penetration required in pressure-critical applications.
Achieving High-Precision Intersection Accuracy
When an H-beam serves as a saddle or a longitudinal support for a vessel, the beveling accuracy of the cut determines the quality of the subsequent weld. If the gap between the beam and the vessel wall is inconsistent, the risk of weld defects such as burn-through or lack of fusion increases. High-definition plasma systems utilize sophisticated Torch Height Control (THC) to maintain a constant distance between the nozzle and the beam surface, even if the beam has slight mill-scale irregularities or minor dimensional deviations.
The intersection accuracy is further enhanced by the use of laser sensing or mechanical probing prior to the cut. The system maps the actual position of the H-beam on the conveyor line, adjusting the cutting program to account for any “camber” or “sweep” inherent in the raw material. This ensures that the 5-axis head executes the saddle cut precisely centered on the beam’s neutral axis, which is essential for uniform load distribution in the final pressure vessel assembly.
Thermal Management and Material Integrity
A common concern in industrial engineering is the Heat Affected Zone (HAZ) created during thermal cutting. In H-beam production for Pressure Vessels, the material is often high-strength carbon steel or specialized alloys. Modern plasma power sources use constricted, high-velocity arcs that minimize the heat input into the surrounding material. By optimizing the cutting speed and gas flow (typically using Oxygen or Nitrogen-Hydrogen mixes), the width of the HAZ is kept within acceptable limits, preventing the embrittlement of the H-beam flanges.
Furthermore, the localized nature of plasma cutting prevents the global distortion of the beam. Since the H-beam is a rigid structural member, uneven heating can lead to twisting. However, the speed of 5-axis plasma systems allows the heat to dissipate rapidly through the mass of the beam, maintaining the straightness required for modular skid construction where multiple beams must align perfectly over long distances.
Low Maintenance Requirements in Continuous Operations
From an operational standpoint, the pressure vessel manufacturing environment demands equipment with high “up-time.” Plasma systems are inherently robust due to their lack of complex optical components or high-precision mechanical friction points found in other cutting technologies. The primary consumables—electrodes, nozzles, and swirl rings—are designed for rapid replacement, often taking less than two minutes to swap out. This ensures that the H-beam production line remains active during multi-shift operations.
The maintenance of the 5-axis head itself is streamlined through the use of brushless AC servo motors and sealed planetary gearboxes. In a heavy industrial setting where metal dust and slag are prevalent, these sealed systems prevent contamination. Modern plasma lines also feature automated slag collection and localized fume extraction, reducing the wear and tear on the linear guides and rack-and-pinion drives. This low-maintenance profile translates to a lower Total Cost of Ownership (TCO) compared to mechanical milling or waterjet systems for heavy-duty beam processing.
Integration with Structural Steel CAD/CAM Software
Efficiency in an H-beam production line is not solely dependent on the hardware; the software interface plays a pivotal role. Industrial engineers utilize specialized software that can import 3D models of pressure vessels and automatically generate the cutting paths for the supporting H-beams. This “art-to-part” workflow eliminates manual data entry errors and ensures that the complex 5-axis movements are optimized for the shortest cycle time.
The software handles the nesting of multiple components on a single H-beam, minimizing scrap rates. For pressure vessel skids, which often require varied lengths and different bevel profiles on each end, the ability to sequence these cuts automatically while maintaining traceability of the heat numbers is a significant regulatory advantage. Every cut performed by the 5-axis plasma can be logged, providing a digital twin of the fabrication process for quality assurance audits.
Economic and Technical Synergy
The synergy between 5-axis plasma cutting and H-beam processing creates a lean manufacturing environment. By consolidating cutting, coping, and beveling into a single station, the footprint of the production line is minimized. This reduction in material handling—moving heavy H-beams between different machines—not only saves time but also significantly reduces the risk of workplace injuries associated with overhead crane usage.
In conclusion, for the industrial engineer focused on pressure vessel support structures, the implementation of a 5-axis plasma-based H-beam line is a strategic necessity. The combination of high-precision intersection geometry, minimal maintenance requirements, and the ability to produce weld-ready bevels directly from CAD data ensures that the final assembly meets the rigorous safety and performance standards of the pressure vessel industry. By focusing on the specific strengths of plasma technology, manufacturers can achieve a level of repeatability and efficiency that manual methods simply cannot match.





