Beam Processing Center with Offline Programming for Steel Structure
In this article
Optimizing Structural Steel Workflows via Plasma Beam Processing
In the current industrial landscape, the efficiency of structural steel fabrication is no longer dictated solely by raw cutting speed, but by the seamless integration of data and mechanical execution. A Beam Processing Center equipped with Plasma Cutting capabilities represents the pinnacle of this integration. Unlike traditional manual layouts that rely on soapstone marking and hand-held torches, modern CNC systems utilize 3D environments to execute complex geometries with mathematical precision. The shift toward automated plasma systems addresses the primary bottlenecks in H-beam fabrication: layout errors, slow coping speeds, and the high cost of rework during field assembly.
The Architecture of Offline Programming
The operational efficiency of a beam processing center begins long before the first arc is struck. Offline programming (OLP) serves as the digital backbone of the system. By extracting data directly from BIM software such as Tekla Structures or SDS/2, the OLP software generates NC1 or DSTV files that contain every hole coordinate, cope geometry, and bevel requirement. This eliminates the need for manual data entry at the machine controller, effectively decoupling the programming phase from the production phase.
From an industrial engineering perspective, OLP minimizes machine downtime. While the plasma system is processing a current batch of H-beams, the programming suite is nesting the next sequence, simulating torch paths to prevent collisions, and calculating the most efficient scrap utilization. This “zero-gap” workflow ensures that the plasma cutting unit maintains a high duty cycle, maximizing the return on capital investment. Furthermore, OLP allows for the detection of design inconsistencies—such as bolt hole interferences or impossible cope radii—prior to the material reaching the conveyor, preventing costly material waste.
Achieving Superior Intersection Accuracy
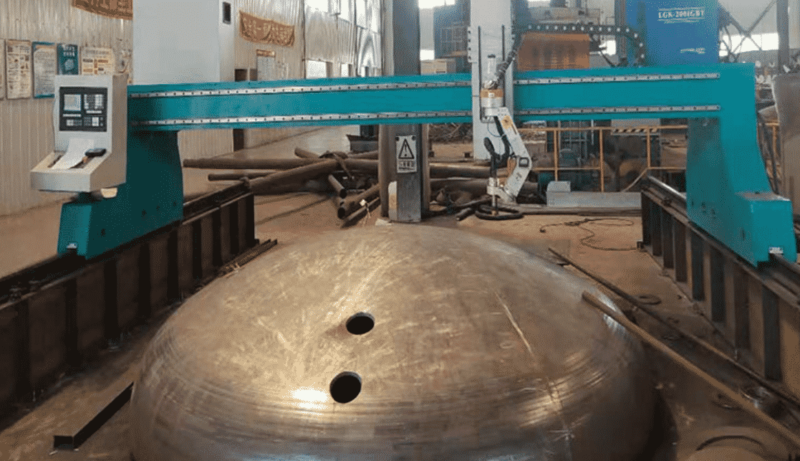
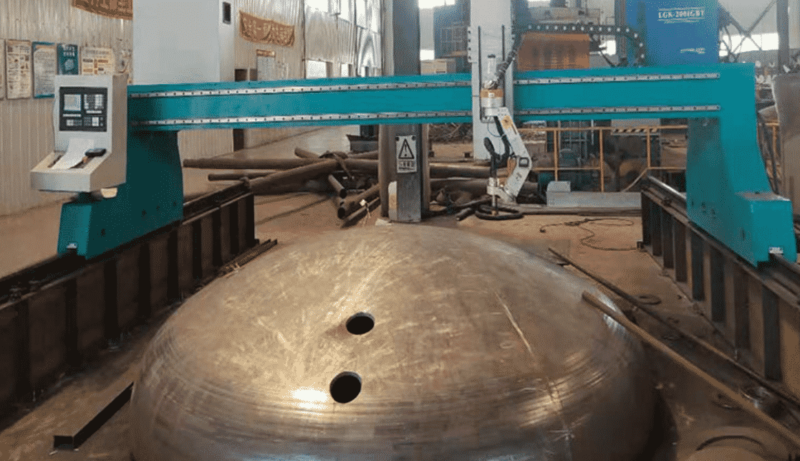
One of the most critical metrics in structural steel is intersection accuracy. In complex braced frames or multi-story assemblies, the fit-up between a primary girder and a secondary beam must be tight to ensure structural integrity and facilitate efficient joining. Plasma-based beam processors utilize multi-axis robotic arms or specialized gantry systems to navigate the flange and web surfaces of H-beams, channels, and hollow structural sections (HSS).
The precision of these intersections is governed by the system’s ability to compensate for material deviations. Structural steel is rarely perfectly straight; mill tolerances allow for slight camber, sweep, and flange out-of-squareness. Advanced plasma processing centers utilize mechanical probes or laser sensors to “map” the actual profile of the beam before cutting. The CNC controller then adjusts the cutting path in real-time. This ensures that a cope or a block-out is cut relative to the actual position of the flange, rather than the theoretical model. This level of intersection accuracy reduces the need for “gap-filling” during assembly and ensures that the structural load paths are maintained as designed.
Bolt Hole Precision and Slotting
Modern high-definition plasma systems have bridged the gap between thermal cutting and mechanical drilling. Through optimized gas flow and specialized power supply cycles, plasma torches can now produce bolt holes with minimal taper that meet AISC (American Institute of Steel Construction) standards for hole quality. This allows a single machine to handle both the perimeter coping and the internal bolt hole patterns in a single pass. The elimination of a separate drilling station reduces material handling time—a major “non-value-added” cost in the fabrication shop.
Low Maintenance Requirements for H-Beam Systems
Reliability is a cornerstone of lean manufacturing. When comparing various thermal cutting technologies for the heavy-duty environment of a steel service center, plasma cutting stands out for its H-beam low maintenance profile. The mechanical components of a plasma beam processor are designed for high-dust, high-vibration environments. Unlike mechanical cutting tools that suffer from tool wear, breakage, and the need for constant lubrication, a plasma torch is a non-contact process.
The primary maintenance requirements for plasma systems are centered on consumables—nozzles, electrodes, and shields—which can be replaced in seconds. The absence of high-torque mechanical forces on the machine frame means that the structural alignment of the gantry remains stable over longer periods. Furthermore, modern plasma power sources feature self-diagnostic modules that monitor coolant flow, gas pressure, and arc stability, allowing for predictive maintenance rather than reactive repairs. For a facility running multiple shifts, this reliability translates to predictable throughput and lower overhead costs per ton of processed steel.
Beveling and Weld Preparation Efficiency
For structural members subjected to high stress, such as moment connections, weld preparation is mandatory. Traditionally, beveling the flanges of an H-beam required manual grinding or the use of portable track torches, both of which are labor-intensive and prone to inconsistency. A 3D plasma beam processing center integrates beveling directly into the cutting sequence.
By utilizing a 5-axis or 6-axis torch head, the system can execute V, Y, X, and K-cuts on the flanges and webs. This capability is vital for creating full-penetration weld preparations. The OLP software calculates the necessary kerf compensation for the angled torch, ensuring that the root face and bevel angle are consistent across the entire length of the cut. This precision not only speeds up the subsequent joining processes but also reduces the volume of filler metal required, as the joint geometry is optimized to the design specifications. The ability to perform complex beveling on the fly transforms the beam processor from a simple “cutting machine” into a comprehensive fabrication hub.
Material Handling and Flow Optimization
Integrating a beam processing center into a facility requires a focus on material flow. The center usually features automated infeed and outfeed conveyors, equipped with cross-transfers to minimize crane dependency. When a beam is loaded, the system automatically detects the leading edge and initiates the programmed sequence. As the plasma torch executes the copes and holes, the outfeed system can mark the piece with part numbers or assembly marks using the plasma arc at a lower amperage. This integrated marking ensures traceability throughout the galvanizing or painting process, completing the digital-to-physical loop initiated by the offline programming software.
Data-Driven Throughput and Future Readiness
The transition to an automated plasma beam processing center is a strategic move for any industrial engineering department. By focusing on the high-definition capabilities of plasma and the robust nature of the machinery, shops can handle heavier profiles and more complex designs without a proportional increase in labor costs. The data generated by the OLP software also provides management with accurate estimates of processing time per ton, allowing for more competitive bidding and better project scheduling. As the steel industry continues to move toward more complex architectural geometries, the flexibility and accuracy of 3D plasma cutting remain the most viable solution for high-volume, high-precision structural fabrication.





