Beam Processing Center with Offline Programming for for Bridge Trusses
In this article
- Optimizing Bridge Truss Fabrication through Advanced Beam Processing
- The Role of Offline Programming in Structural Workflows
- Achieving High-Precision Intersection Accuracy
- Kinematic Calibration and Volumetric Precision
- Geometric Complexity in Truss Joints
- Mechanical Advantages of Plasma Cutting for Heavy Sections
- Low Maintenance Requirements for H-Beam Processing
- Slag Management and Heat Dissipation
- Advanced Plasma Beveling for Weld Preparation
- Multi-Axis Beveling Geometry
- Quality Control and Edge Preparation
- Operational Efficiency and Throughput
- Minimizing Material Handling
Optimizing Bridge Truss Fabrication through Advanced Beam Processing
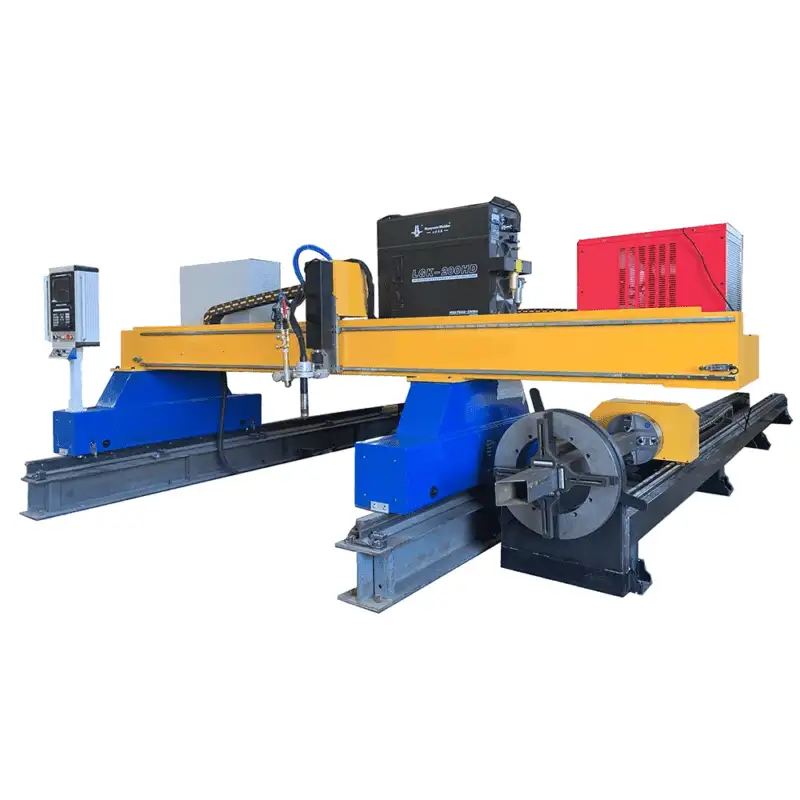
In the domain of structural engineering, particularly concerning large-scale bridge trusses, the transition from manual layout to automated Beam Processing Center technology represents a critical shift in production efficiency. Bridge trusses require extreme tolerances to ensure load distribution follows theoretical models. Any deviation in member length or joint geometry introduces secondary stresses that can compromise the long-term fatigue life of the structure. This analysis focuses on the role of automated Plasma Cutting and offline programming in achieving these stringent requirements.
The Role of Offline Programming in Structural Workflows
The efficiency of a beam processing center is not measured solely by its cutting speed, but by its uptime. Offline Programming (OLP) allows engineers to generate toolpaths, verify collisions, and simulate the cutting process in a virtual environment while the machine remains operational on another task. By importing IFC or TEKLA models directly into the OLP environment, the risk of human error during manual data entry is eliminated.
OLP software calculates the exact kerf compensation and torch lead-ins required for complex geometries. for Bridge Trusses, where diagonal members often intersect chords at acute angles, OLP ensures that the developed surfaces of the H-beams or channels match the mating surfaces with sub-millimeter precision. This digital continuity ensures that the physical output reflects the engineer’s intent without the need for shop-floor adjustments.
Achieving High-Precision Intersection Accuracy
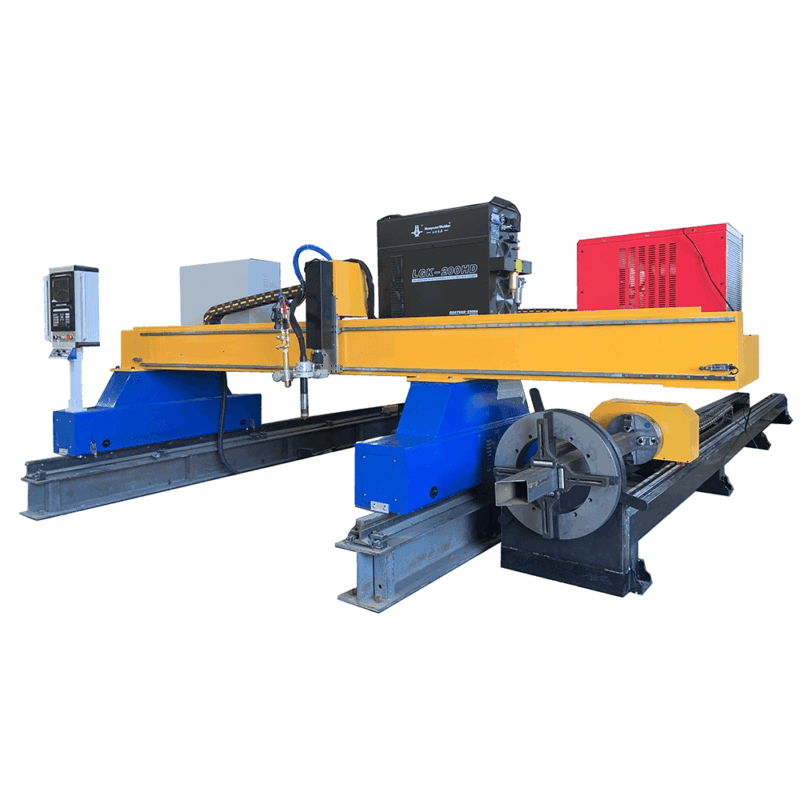
The structural integrity of a truss depends on the fit-up of its components. In traditional fabrication, gaps at intersections are often filled with weld metal, which increases the Heat Affected Zone (HAZ) and potential for distortion. Modern plasma-based beam centers utilize robotic arms or multi-axis gantry systems to navigate the contours of H-beams, ensuring that the Intersection Accuracy is maintained across all planes.
Kinematic Calibration and Volumetric Precision
To achieve high-accuracy cuts, the system must account for the mechanical tolerances of the beam itself. Structural steel is rarely perfectly straight. Advanced beam centers employ probing systems or laser sensors to map the actual profile of the beam before cutting begins. The OLP-generated toolpath is then dynamically adjusted to the “as-is” geometry of the steel. This process ensures that copes, notches, and bolt holes are placed relative to the actual flange and web positions, rather than a theoretical centerline.
Geometric Complexity in Truss Joints
Bridge trusses often involve complex bird-mouth cuts and double-miter joints. Plasma cutting heads with five or six axes of motion can execute these geometries in a single pass. The ability to maintain a constant standoff distance while rotating the torch around the flanges of an H-beam is essential for maintaining a clean cut surface and consistent edge quality, which directly impacts the subsequent assembly phase.
Mechanical Advantages of Plasma Cutting for Heavy Sections
While various thermal cutting methods exist, plasma remains the industrial standard for heavy-duty structural steel due to its robustness and cost-to-performance ratio. When processing large H-beams for bridge infrastructure, the equipment must withstand a harsh environment characterized by dust, scale, and high thermal loads.
Low Maintenance Requirements for H-Beam Processing
One of the primary drivers for selecting plasma technology in a beam processing center is the H-beam Low Maintenance profile. Plasma torches are designed for high duty cycles in industrial environments. Unlike more sensitive optical cutting systems, plasma components are relatively inexpensive to replace and are less susceptible to the vibration and debris common in structural steel shops. The robust nature of the power supply and the simplified gas delivery systems mean that maintenance intervals are extended, and the technical skill required for routine servicing is manageable for standard plant maintenance crews.
Slag Management and Heat Dissipation
Modern plasma systems incorporate advanced gas flow controls that minimize dross or slag accumulation on the underside of the cut. For bridge fabricators, this reduces the man-hours required for secondary grinding. Furthermore, the high energy density of modern high-definition plasma concentrates the heat in a very narrow area, which limits structural warping—a critical factor when maintaining the straightness of long-truss chords.
Advanced Plasma Beveling for Weld Preparation
Bridge trusses are subject to dynamic loading, necessitating full-penetration welds in many critical joints. Preparing these edges manually is a labor-intensive process prone to inconsistency. An automated beam processing center integrates Plasma Beveling directly into the cutting cycle.
Multi-Axis Beveling Geometry
By utilizing a robotic tilting head, the system can produce V, X, K, and Y-style bevels. These preparations are programmed through the OLP software to match the specific welding procedure specifications (WPS). The precision of the plasma bevel ensures a uniform root gap and land, which is essential for automated or semi-automated welding processes that follow. The ability to vary the bevel angle along a single cut path allows for the creation of complex transitions required in skewed bridge connections.
Quality Control and Edge Preparation
The quality of a plasma-cut edge in bridge fabrication is governed by standards such as AWS D1.5. High-definition plasma systems produce an edge with minimal taper and a surface finish that often requires no further machining. By controlling the gas chemistry—using oxygen or nitrogen blends depending on the material thickness—the system can produce a metallurgically sound edge that is ready for welding, ensuring that the final truss assembly meets all NDT (Non-Destructive Testing) requirements.
Operational Efficiency and Throughput
The integration of a beam processing center into a bridge production line fundamentally changes the throughput calculations for a fabrication shop. By combining multiple operations—length cutting, hole drilling (via plasma marking or high-speed spindles), and beveling—into a single workstation, the material handling overhead is significantly reduced.
Minimizing Material Handling
Every time a heavy H-beam is moved via overhead crane, production stops and safety risks increase. A centralized beam center takes raw stock at one end and outputs a finished, bolt-ready, or weld-ready component at the other. The OLP software also facilitates nesting, which optimizes the use of raw material and reduces scrap, a vital consideration given the high cost of structural steel.
Summary of Engineering Benefits
- Reduction in manual layout errors through direct BIM-to-Machine data transfer.
- Enhanced structural performance due to tighter joint fit-up and accurate beveling.
- Lower operational costs through reduced maintenance and consolidated processing steps.
- Increased safety by minimizing the manual handling of large structural sections.
In conclusion, the deployment of a beam processing center equipped with multi-axis plasma cutting and offline programming is a prerequisite for modern bridge truss fabrication. The focus on intersection accuracy and the mechanical reliability of plasma systems ensures that fabricators can meet the rigorous demands of infrastructure projects while maintaining a competitive edge in production efficiency.





