Beam Processing Center with Narrow Gap welding for for Pressure Vessels
In this article
Integrating Plasma Cutting in Pressure Vessel Beam Processing
In the realm of heavy-duty fabrication, the efficiency of a Beam Processing Center is measured by its ability to deliver precise geometries that facilitate downstream automation. For pressure vessel manufacturing, where structural integrity and weld quality are non-negotiable, the front-end preparation of H-beams and cylindrical supports dictates the success of the entire assembly. While various thermal cutting methods exist, plasma cutting remains the industrial benchmark for thick-walled section processing due to its balance of speed, cost-effectiveness, and metallurgical compatibility with carbon and stainless steels.
The transition to automated Narrow Gap Welding (NGW) necessitates a level of fit-up accuracy that manual layout cannot achieve. In these specialized welding processes, the groove angles are significantly reduced to minimize the volume of filler metal and the total heat input into the base material. Consequently, the plasma cutting system must provide exceptional edge squareness and dimensional consistency. This article examines the mechanical and operational parameters that make high-definition plasma cutting the preferred choice for these high-stakes industrial environments.
Optimization of Intersection Accuracy
Intersection accuracy refers to the precision with which the cutting head manages the transition between different planes of an H-beam or the complex curvature of a vessel shell. In a robotic beam processing center, the software must calculate the kerf compensation in real-time as the torch moves across the web and flanges. For pressure vessel supports, these intersections often involve saddle cuts or offset pipe-to-beam joints that require 4-axis or 5-axis motion control.
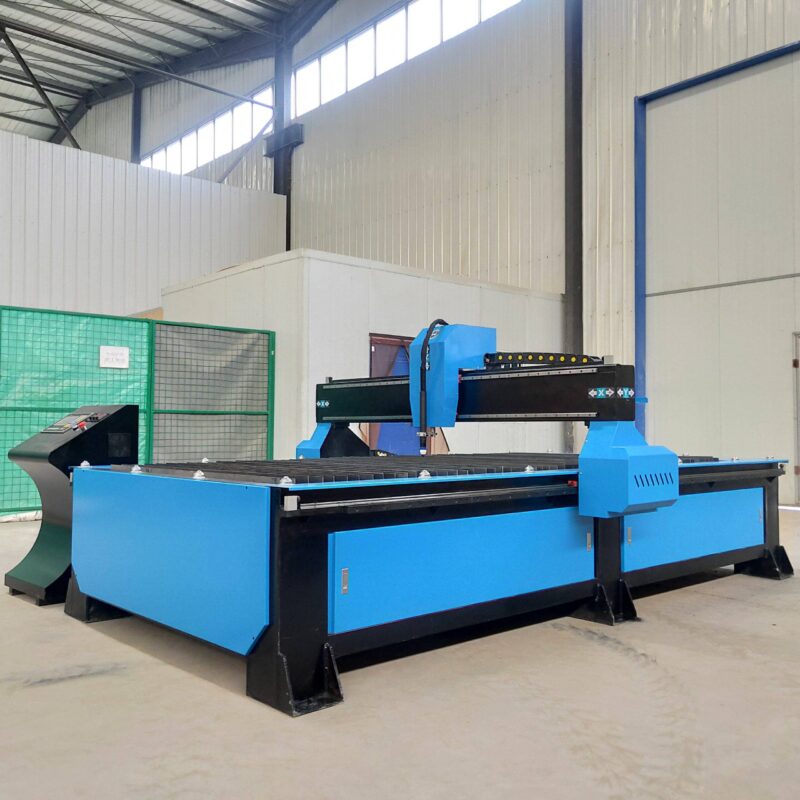
The mechanical rigidity of the gantry and the resolution of the servo drives are critical. When the plasma arc penetrates a thick flange, any vibration or deviation in the torch path results in a “gouging” effect that ruins the fit-up for Narrow Gap Welding. Modern CNC controllers use advanced algorithms to maintain a constant torch-to-workpiece distance via voltage sensing, ensuring that the arc remains stable even when encountering the metallurgical variations common in rolled structural sections. This precision eliminates the need for manual grinding, which is often a hidden bottleneck in vessel fabrication shops.
Low Maintenance H-Beam Handling and Durability
From an industrial engineering perspective, the Total Cost of Ownership (TCO) of a processing line is heavily influenced by the maintenance requirements of the cutting medium. Plasma systems are inherently rugged. Unlike complex optical systems that require clean-room environments and sensitive alignment, plasma torches are designed for the grit and heat of a heavy fabrication floor.
For H-Beam Processing Center operations, the primary wear components are limited to electrodes, nozzles, and swirl rings. These consumables can be replaced in minutes by shop floor operators, ensuring that the machine stays in the “green” or productive zone for the majority of the shift. Furthermore, the absence of sensitive mirrors or fiber delivery systems means that the mechanical vibrations associated with moving heavy structural beams through conveyors do not degrade the cutting quality over time.
The robust nature of plasma also extends to its tolerance of surface contaminants. While other methods might struggle with mill scale, light rust, or primers commonly found on structural H-beams, high-definition plasma penetrates these layers with minimal impact on arc stability. This reduces the pre-processing requirements, allowing raw material to move directly from storage to the cutting bed, streamlining the internal logistics of the manufacturing facility.
Beveling for Narrow Gap Preparation
The core requirement for narrow gap welding is the production of deep, steep-angled bevels. Conventional V-grooves typically require 60 to 70-degree included angles, but narrow gap preparations often reduce this to 10 degrees or less, sometimes employing J-groove geometries. Achieving these profiles on thick-walled beams requires a plasma head capable of high-angle tilting without losing arc density.
Advanced Weld Prep Accuracy is achieved through multi-pass plasma cutting or single-pass beveling using high-amperage power sources. When preparing the longitudinal or circumferential joints of a vessel’s structural frame, the plasma system must maintain a consistent “land” or root face. If the land thickness varies by even a millimeter, the automated welding head may experience burn-through or lack of fusion. Therefore, the beam processing center must integrate sophisticated material mapping, using touch probes or laser scanners to account for any slight camber or sweep in the H-beam before the cut begins.
Thermal Management and Heat Affected Zone (HAZ)
A common concern in pressure vessel fabrication is the Heat Affected Zone (HAZ) created during thermal cutting. Industrial engineers must balance cutting speed with the metallurgical properties of the steel. High-definition plasma systems utilize secondary gases—such as oxygen or nitrogen—to constrict the arc, resulting in a narrower kerf and a significantly smaller HAZ compared to oxy-fuel cutting.
For NGW applications, a small HAZ is beneficial as it minimizes the risk of hydrogen-induced cracking and maintains the mechanical properties of the grain structure near the weld interface. By optimizing the cutting speed and gas flow, the beam processing center produces a metallurgical edge that is often weld-ready. This synergy between the cutting process and the final welding stage is the hallmark of an efficient production line, reducing the secondary handling of heavy components.
Throughput and Productivity Gains
The integration of plasma cutting into a centralized beam processing workflow yields substantial productivity gains. By combining hole-punching (via plasma marking or small-hole technology), coping, and beveling into a single CNC-controlled operation, the facility reduces the number of “touches” per part. In the context of large-scale pressure vessel projects, where hundreds of structural supports may be required, the cumulative time savings are significant.
Furthermore, the reliability of the plasma arc allows for “lights-out” or semi-autonomous operation. Once the H-beam is loaded onto the infeed conveyor, the system can execute complex nested programs that maximize material utilization. The data generated by the CNC controller also provides valuable insights for industrial engineers to track cycle times, consumable life, and overall equipment effectiveness (OEE).
Conclusion on System Selection
For manufacturers specializing in pressure vessels, the choice of a beam processing center must be driven by the specific requirements of heavy-wall fabrication and narrow gap welding. The focus should remain on systems that offer superior intersection accuracy and the ability to produce consistent, high-angle bevels. By prioritizing plasma technology, shops benefit from a low-maintenance, high-durability solution that survives the rigors of the structural steel environment while delivering the precision of a laboratory tool.
In conclusion, the successful marriage of plasma cutting and narrow gap welding represents the pinnacle of modern structural engineering. It allows for the construction of safer, more reliable pressure vessels at a lower cost and with higher throughput. As the industry continues to move toward greater automation, the role of the precision-cut beam will only become more central to the manufacturing lifecycle.





