Beam Processing Center with Arc Voltage Control for for Steel Structure
In this article
Optimizing Structural Steel Fabrication with Beam Processing Centers
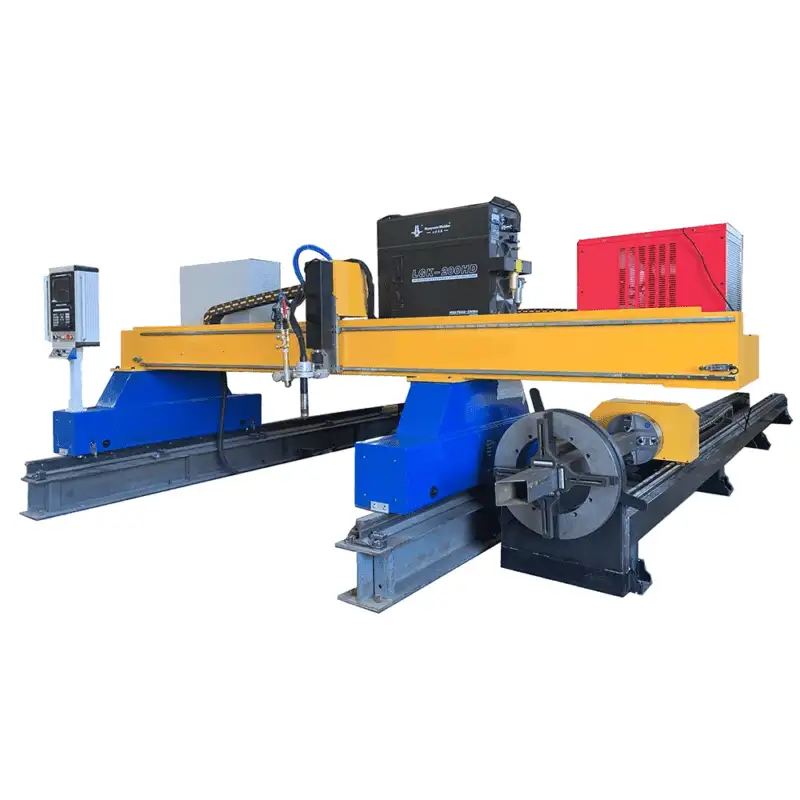
In the field of heavy structural steel fabrication, the Beam Processing Center (BPC) represents the primary hub for multi-axis material reduction and preparation. Unlike traditional manual layout methods, these automated systems leverage Plasma Cutting technology to execute complex geometries on H-beams, I-beams, and channels. The core challenge in processing large-scale structural members lies in the inherent variability of the material. Steel beams often exhibit mill tolerances including camber, sweep, and flange tilt. To maintain engineering precision, the integration of Arc Voltage Control (AVC) is a mandatory requirement for modern industrial operations.
The Engineering Logic of Arc Voltage Control
Arc Voltage Control is a closed-loop feedback mechanism that regulates the distance between the plasma torch tip and the workpiece surface. In plasma physics, the voltage of the arc is directly proportional to the length of the arc. As the distance between the torch and the steel beam increases, the voltage increases; as the distance decreases, the voltage drops.
For a Beam Processing Center, the AVC system continuously monitors these fluctuations at millisecond intervals. When the system detects a change in voltage—indicating a deviation in the beam’s surface height—it signals the Z-axis motor to adjust the torch position. This ensures a constant standoff distance, which is critical for maintaining the plasma arc’s energy density. Without AVC, a torch would either collide with a warped beam or move too far away, leading to excessive dross, wider kerfs, and compromised edge quality.
Maximizing Intersection Accuracy in Complex Copes
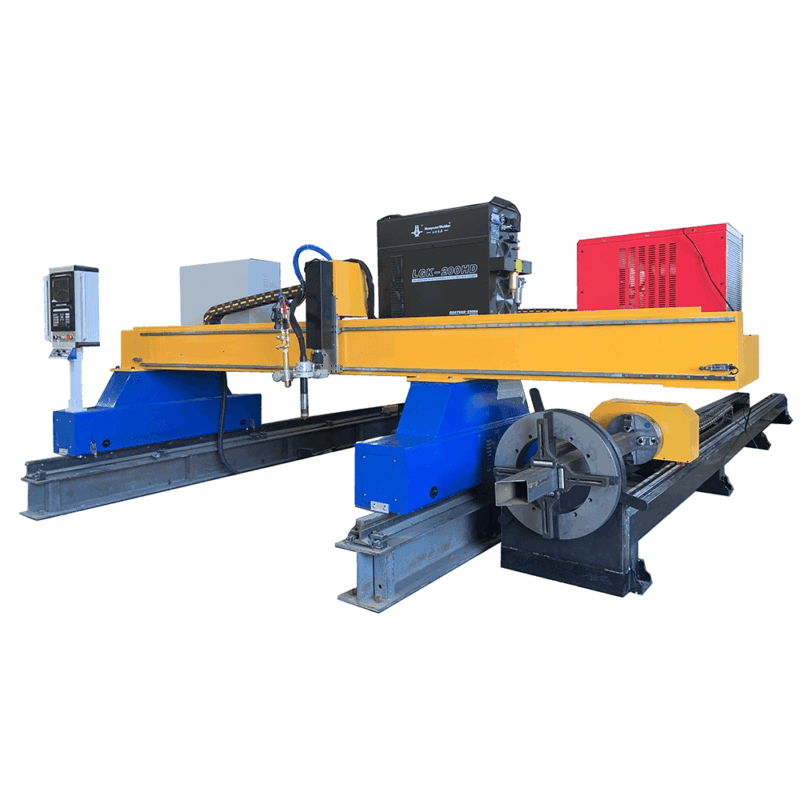
Structural integrity in steel skeletons depends heavily on the fit-up of beam-to-beam and beam-to-column connections. These intersections often require intricate “copes,” “rat holes,” and bolt-hole patterns. Intersection accuracy is the primary metric by which a Beam Processing Center is evaluated.
When cutting through the web of an H-beam toward the flange, the plasma torch must transition between different material thicknesses and orientations. The AVC ensures that as the torch navigates these transitions, the focal point of the plasma jet remains optimized. In high-definition plasma systems, this results in bolt holes that meet AISC (American Institute of Steel Construction) standards for circularity and taper, and copes that require zero secondary grinding before assembly.
Achieving Precision in Multi-Axis Beveling
Welded connections in heavy structural steel demand specific edge preparations, typically V, Y, or K-cut bevels. A multi-axis Beam Processing Center utilizes a robotic or tilt-rotate head to achieve these angles. However, beveling introduces a geometric complexity: the distance from the torch to the plate changes as the torch tilts.
Sophisticated AVC algorithms compensate for this “slant” distance. By calculating the trigonometric offset of the tilted torch, the Arc Voltage Control maintains the correct effective arc length. This precision allows for the production of weld-ready edges on both the flanges and webs of H-beams, significantly reducing the labor hours typically spent on manual beveling with handheld torches or track cutters.
H-Beam Maintenance and Operational Longevity
From a facility management perspective, the choice of plasma technology within a BPC is driven by the need for H-beam low maintenance and high uptime. Mechanical processing methods, such as drilling or sawing, involve significant consumable costs in the form of bits and blades, and they subject the machine frame to high vibration and mechanical stress.
Plasma systems are non-contact. Because the cutting force is delivered via an ionized gas stream, there is no tool pressure exerted on the machine’s gantry or robotic arm. This reduces the wear and tear on bearings, rails, and drive motors. Modern plasma power sources are designed with “long-wear” consumable kits that optimize the life of electrodes and nozzles through controlled ramp-up and ramp-down of gas flows and current. In a high-volume steel service center, this translates to fewer mid-shift interventions and a lower total cost per ton of processed steel.
Material Handling and Surface Sensing
Effective beam processing begins before the arc is even struck. Most high-end centers utilize a combination of mechanical probing and initial height sensing (IHS) to map the beam’s actual dimensions versus the theoretical CAD model. Once the Beam Processing Center establishes the physical start point, the AVC takes over for the duration of the cut.
This dual-layer approach is essential because structural steel is rarely perfectly straight. Thermal expansion during the cutting process can also cause the material to move or “oil-can.” The AVC’s ability to react to these dynamic changes in real-time prevents the torch from losing the arc or sustaining damage, which is vital for maintaining the continuous flow of the production line.
Environmental and Efficiency Considerations
Industrial engineers also prioritize the efficiency of the cutting process. Plasma cutting at high amperages requires robust fume extraction. Integrated BPCs often feature localized extraction hoods that follow the torch, ensuring that the particulates generated during the vaporization of the steel are captured immediately. This not only protects the machine’s precision components from dust accumulation but also ensures compliance with workplace safety standards.
Furthermore, the speed of plasma cutting on heavy-walled H-beams is significantly higher than oxy-fuel alternatives. While oxy-fuel relies on a chemical reaction (oxidation) that is limited by the speed of heat transfer, plasma uses high-velocity thermal energy. This allows for faster feed rates across all sections of the beam, maximizing the throughput of the shop.
Conclusion: The Path to Automated Precision
The implementation of a Beam Processing Center equipped with Arc Voltage Control represents a strategic investment in technical accuracy and operational lean-ness. By focusing on the precision of plasma intersections, the versatility of automated beveling, and the low-maintenance profile of non-contact cutting, steel fabricators can achieve tolerances that were previously impossible at scale. As structural designs become more complex, the reliance on real-time feedback loops like AVC ensures that the final product remains within the tight constraints required for modern engineering and construction.






