Beam Processing Center with Arc Voltage Control for for Pressure Vessels
In this article
- Optimizing Pressure Vessel Structural Fabrication via Beam Processing Centers
- The Engineering Mechanics of Arc Voltage Control
- Closed-Loop Feedback for Z-Axis Modulation
- Precision Intersection and Saddle Cuts
- Achieving Mathematical Accuracy in 3D Space
- H-Beam Processing: The Low Maintenance Advantage
- Advanced Plasma Beveling for Weld Preparation
- Automated Beveling Cycles
- Throughput and Operational Efficiency
Optimizing Pressure Vessel Structural Fabrication via Beam Processing Centers
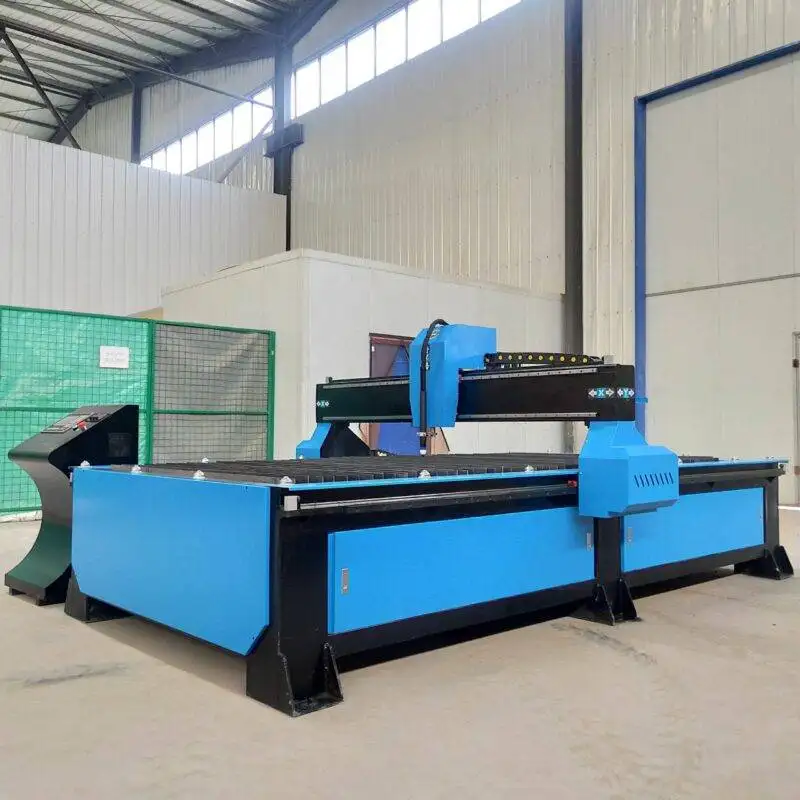
In the heavy industrial sector, specifically within the manufacturing of pressure vessels and associated support structures, the demand for dimensional precision is absolute. A Beam Processing Center serves as the primary hub for transforming raw H-beams, channels, and heavy-walled profiles into finished components. When these structures are destined for high-pressure environments, the tolerance for error in fit-up vanishes. The implementation of Plasma Cutting systems integrated with sophisticated sensor arrays represents the current gold standard for achieving these rigorous engineering specifications.
The Engineering Mechanics of Arc Voltage Control
The core challenge in automated plasma cutting of large structural profiles is the inherent variability in material geometry. H-beams are rarely perfectly flat or straight; mill tolerances often allow for slight bowing, twisting, or flange variations. Without a dynamic adjustment system, a fixed-height cutting head would either collide with the workpiece or move too far away, resulting in poor kerf quality and lost Intersection Accuracy.
Closed-Loop Feedback for Z-Axis Modulation
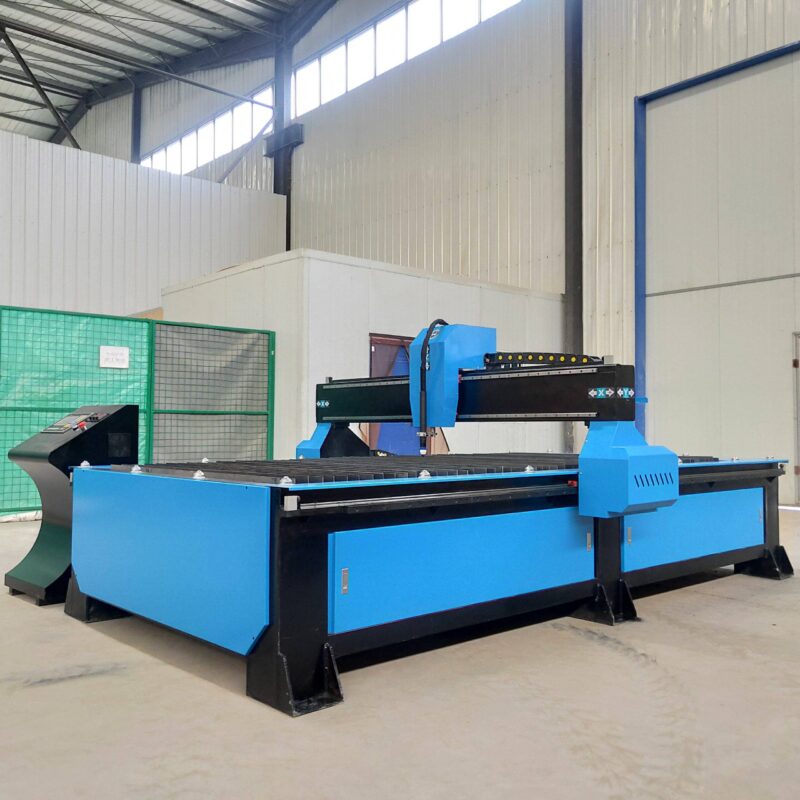
Arc Voltage Control (AVC) functions as a real-time, closed-loop feedback mechanism. The system monitors the electrical potential between the plasma torch electrode and the metallic workpiece. Since the voltage of a plasma arc is directly proportional to the length of the arc, the CNC controller can translate voltage fluctuations into precise Z-axis movements. If the beam flange bows upward, the voltage drops; the AVC instantly signals the torch lift to retract, maintaining a constant standoff distance. This ensures that the plasma stream remains at its optimal focal point, providing a consistent cut width and preventing dross accumulation.
Precision Intersection and Saddle Cuts
Pressure vessel support frames frequently require complex geometry where beams must intersect at non-orthogonal angles or wrap around cylindrical vessel bodies. Traditional mechanical methods struggle with these “saddle cuts” or “cope cuts,” often requiring secondary manual grinding. A plasma-based Beam Processing Center eliminates these bottlenecks through multi-axis motion control.
Achieving Mathematical Accuracy in 3D Space
The intersection of two structural members creates a complex three-dimensional curve. By utilizing plasma torches mounted on robotic or multi-axis gantry systems, the BPC calculates the tool path required to create a perfect fit-up. Because the AVC maintains the exact standoff distance even as the torch rotates to accommodate the flange-to-web transition, the resulting edge is clean and ready for immediate assembly. This level of accuracy is critical for ensuring that load-bearing joints meet the structural integrity requirements mandated by ASME and other regulatory bodies.
H-Beam Processing: The Low Maintenance Advantage
From an industrial engineering perspective, Total Cost of Ownership (TCO) is a primary KPI. Compared to mechanical drilling or sawing lines, plasma-centric beam centers offer a significantly Low Maintenance profile. Mechanical systems rely on physical contact, leading to tool wear, breakage, and the constant need for lubrication and cooling fluids.
Eliminating Consumable Volatility
Plasma cutting is a non-contact process. Beyond the periodic replacement of electrodes and nozzles, there are no mechanical stresses applied to the machine frame or the cutting head. This reduces the frequency of calibration cycles and prevents the catastrophic failures associated with drill bit shearing inside thick-walled sections. Furthermore, modern plasma power supplies are designed for high duty cycles, allowing for continuous operation in 24/7 production environments without the thermal degradation seen in traditional mechanical cutting tools.
Waste Management and Operational Cleanliness
A plasma-based BPC also streamlines the shop floor environment. Unlike saws that produce large volumes of sharp metallic chips and oily coolant runoff, plasma systems utilize integrated dust collection and fume extraction. This centralized waste management reduces the man-hours required for machine cleaning and enhances the longevity of the linear guides and rack-and-pinion drive systems by preventing the ingress of abrasive metallic particles.
Advanced Plasma Beveling for Weld Preparation
In the context of pressure vessels, the strength of the weld is the strength of the vessel. Achieving full penetration welds requires precise edge preparation, commonly known as beveling. Manually grinding bevels on heavy H-beams is not only labor-intensive but introduces human error that can lead to weld failure during X-ray inspection.
Automated Beveling Cycles
The integration of a tilting plasma head allows the Beam Processing Center to perform V, Y, X, and K-style bevels in a single pass. The Plasma Beveling process is synchronized with the AVC to ensure that as the torch tilts, the distance to the material is recalculated to account for the hypotenuse of the angle. This prevents the “rounding” of corners and ensures a sharp, consistent land area for the root pass of the weld.
Thermal Input and Metallurgical Integrity
Industrial engineers often scrutinize the Heat Affected Zone (HAZ) created by plasma cutting. Modern high-definition plasma systems utilize narrow-kerf technology and high-speed motion to minimize thermal input. By optimizing the cutting speed through the CNC interface, the BPC ensures that the metallurgical properties of the H-beam are preserved, preventing embrittlement at the critical junction where the vessel support will be fused. This precision reduces the need for post-cut heat treatment and ensures compliance with metallurgical standards for pressure-retaining structures.
Throughput and Operational Efficiency
The ultimate goal of implementing an AVC-equipped Beam Processing Center is the compression of the production timeline. By combining cutting, coping, and beveling into a single automated station, the “dwell time” between fabrication stages is virtually eliminated. Material handling—often the largest hidden cost in structural fabrication—is minimized as the beam only needs to be loaded and indexed once.
Data-Driven Fabrication
Modern BPCs integrate directly with Building Information Modeling (BIM) and CAD/CAM software. This allows for the seamless transfer of “Tekla” or “SDS/2” files directly to the cutting floor. The AVC ensures that what was designed in the digital twin is exactly what is produced in the physical world, regardless of the minor imperfections in the raw steel. This digital-to-physical fidelity is the cornerstone of modern industrial engineering in the pressure vessel sector, ensuring that every beam is a precision component rather than a rough-cut approximation.






