Beam Processing Center with Arc Voltage Control for for Pressure Vessels
In this article
Optimizing Pressure Vessel Fabrication via Advanced Beam Processing
In the heavy industrial sector, the fabrication of pressure vessels demands rigorous adherence to geometric tolerances and structural integrity standards. The transition from manual layout and handheld thermal cutting to an automated Beam Processing Center represents a significant shift in production efficiency. For industrial engineers, the primary objective is to eliminate variability in the cutting phase, ensuring that every penetration and shell intersection aligns perfectly with the engineering design. This analysis focuses on the deployment of high-definition plasma systems equipped with specialized control mechanisms to meet these stringent requirements.
The Role of Arc Voltage Control in Plasma Precision
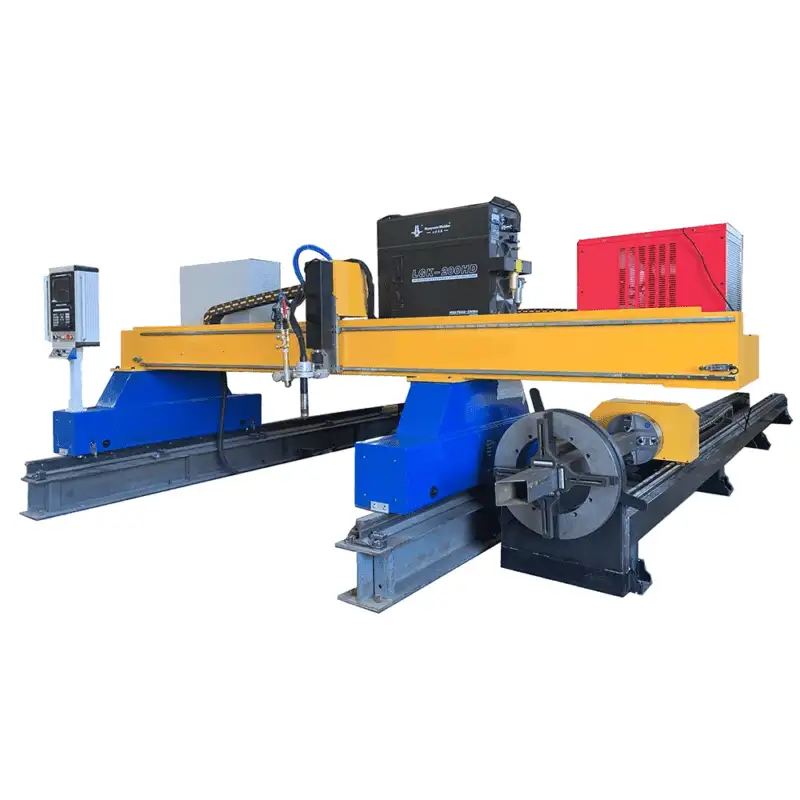
The core of high-performance Plasma Cutting in the pressure vessel industry is Arc Voltage Control (AVC). Unlike flat plate cutting, beam and vessel processing involve navigating irregular surfaces, structural variances, and material deviations. AVC functions as a closed-loop feedback system that monitors the electrical potential between the plasma torch electrode and the workpiece. As the distance between the torch and the material changes, the voltage fluctuates.
The AVC system detects these micro-fluctuations and commands the Z-axis motor to adjust the torch height instantaneously. In the context of pressure vessels, this is critical when cutting through curved shells or along the flanges of structural supports. By maintaining a constant standoff distance, the system ensures a stable plasma arc column. This stability directly impacts the kerf width and the angle of the cut, preventing “dross” accumulation and reducing the need for secondary grinding operations. From a throughput perspective, AVC minimizes the risk of torch collisions and consumable damage, which are common failure points in automated thermal cutting.
Achieving Superior Intersection Accuracy
Pressure vessels often require complex nozzle penetrations and structural attachments where a cylindrical or spherical shell meets another geometric body. Achieving high Intersection Accuracy is not merely a matter of linear movement; it requires a sophisticated 5-axis or 6-axis robotic kinematic model. The beam processing center must calculate the mathematical “unrolling” of the intersection path in real-time.
When cutting a hole for a nozzle, the plasma torch must tilt and rotate to compensate for the thickness of the vessel wall. This ensures that the internal diameter of the cut matches the external diameter of the mating component throughout the entire circumference. Industrial engineers prioritize systems that utilize high-resolution encoders and precision rack-and-pinion drives. This mechanical rigidity, combined with software algorithms that account for the plasma arc’s “lag” at high speeds, allows for tolerances within +/- 0.5mm. Such precision is vital for the subsequent assembly phase, where tight fit-ups are required to satisfy radiographic testing (RT) standards for weld quality.
H-Beam Structural Integrity and Low Maintenance Design
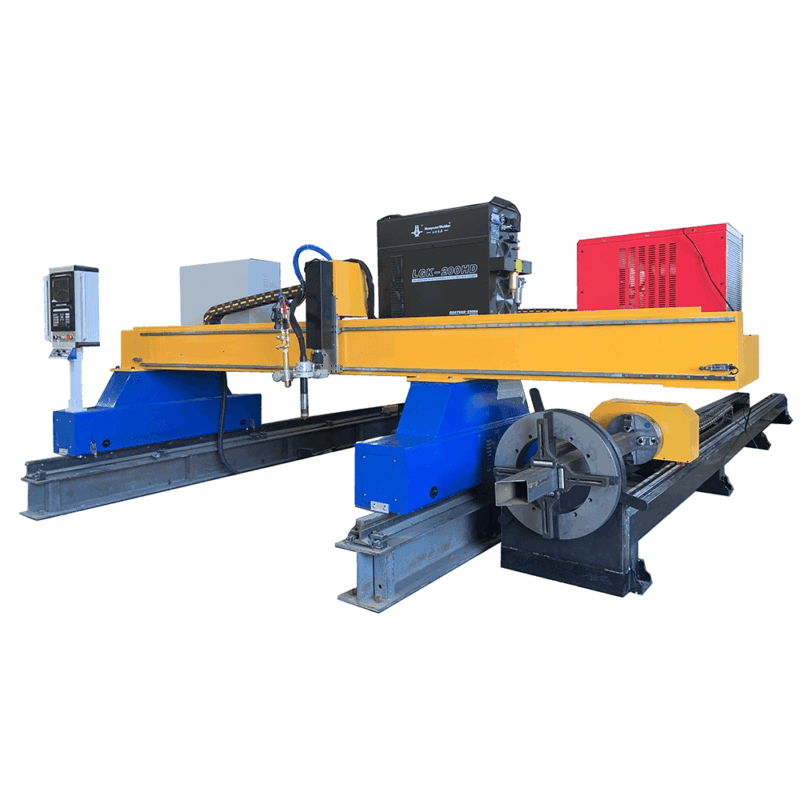
The physical framework of a beam processing center is usually subjected to harsh environments, including metal dust, high temperatures, and heavy vibrations. Utilizing a heavy-duty H-beam construction for the machine bed and gantry provides the necessary dampening characteristics required for high-speed plasma operations. Unlike lighter tubular frames, H-beam structures offer superior torsional rigidity, which prevents “whipping” during rapid directional changes of the cutting head.
From a maintenance standpoint, the engineering focus is on longevity and uptime. Modern centers employ hardened, ground linear ways and pressurized bellows to protect sensitive components from conductive plasma dust. By utilizing oversized H-beam supports, the machine maintains its alignment over years of multi-shift operation. This “over-engineered” approach reduces the frequency of recalibration cycles, allowing the facility to maintain a higher OEE (Overall Equipment Effectiveness) score. For the industrial engineer, low maintenance translates to lower total cost of ownership and more predictable production schedules.
Advanced Plasma Beveling for Weld Preparation
In pressure vessel manufacturing, a square cut is rarely sufficient. Most joints require a specific bevel profile—typically V, Y, or K-cuts—to allow for full penetration welding. Implementing Plasma Beveling within the beam processing center eliminates the need for manual beveling with handheld torches or carbon arc gouging, both of which are labor-intensive and prone to human error.
The integration of a programmable beveling head allows the center to change the torch angle dynamically during the cutting cycle. This is particularly important for “varying bevels” where the angle must change as the torch moves around a contoured surface. The software must automatically calculate the offset for the plasma tip to ensure the root face remains consistent. This consistency is the foundation of a high-quality weld. When the root face is uniform, the heat input during the welding process can be standardized, leading to fewer defects and a reduction in rework costs.
Data-Driven Throughput and Material Optimization
Beyond the mechanical cutting process, the industrial engineering value of an automated beam processing center lies in its integration with CAD/CAM environments. Nesting software optimizes the layout of penetrations and cuts on a single workpiece, minimizing scrap. Furthermore, the digital integration allows for real-time tracking of material usage and cutting time per component. This data provides the basis for accurate job costing and capacity planning.
By automating the plasma cutting process with AVC and multi-axis control, a facility can transition from a “craft-based” shop to an “engineered” production line. The reliance on highly skilled layout personnel is reduced, and the focus shifts to process monitoring and optimization. The result is a standardized output that meets the high-pressure demands of the energy, chemical, and nuclear sectors, where failure is not an option and precision is the primary metric of success.
Conclusion on Thermal Processing Efficiency
The deployment of a Beam Processing Center for Pressure Vessels is a strategic investment in technical precision. By prioritizing Arc Voltage Control, manufacturers ensure that the plasma arc remains optimal regardless of surface irregularities. The structural choice of H-beam frames guarantees long-term accuracy and minimal downtime, while advanced beveling capabilities streamline the path from raw material to a weld-ready component. In the competitive landscape of industrial fabrication, these technical advantages provide the necessary margin for both quality assurance and operational profitability.





