Optimizing LNG Infrastructure Through Advanced Plasma Fabrication
The construction of Liquefied Natural Gas (LNG) facilities demands a level of geometric precision and structural integrity that exceeds standard industrial applications. In the realm of industrial engineering, the focus remains on minimizing material waste and maximizing throughput without compromising the safety standards required for cryogenic environments. A specialized Plasma Cutting Machine equipped with multi-axis capabilities represents the cornerstone of modern pipe and profile fabrication. These machines address the specific challenges of large-scale LNG projects, including the management of thick-walled high-alloy steels and the complex geometries of terminal piping networks.
Precision in Geometric Intersection Accuracy
LNG projects involve miles of piping with intricate branch connections and headers. The primary technical hurdle in these assemblies is Intersection Accuracy. When two pipes meet at an angle, the resulting cut must account for the curvature of both the header and the branch pipe. A CNC plasma system utilizing advanced kinematics ensures that the torch remains perpendicular or at a specific bevel angle relative to the surface throughout the entire cut path.
From an engineering perspective, this precision is vital for maintaining a consistent root gap during the subsequent welding phase. If the intersection cut is inaccurate, the resulting fit-up will have varying gaps, leading to excessive weld metal deposition, increased internal stresses, and potential failure points under cryogenic thermal cycling. High-definition plasma power sources provide a narrow kerf and minimal heat-affected zone (HAZ), which ensures that the metallurgical properties of the specialized alloys used in LNG piping are preserved.
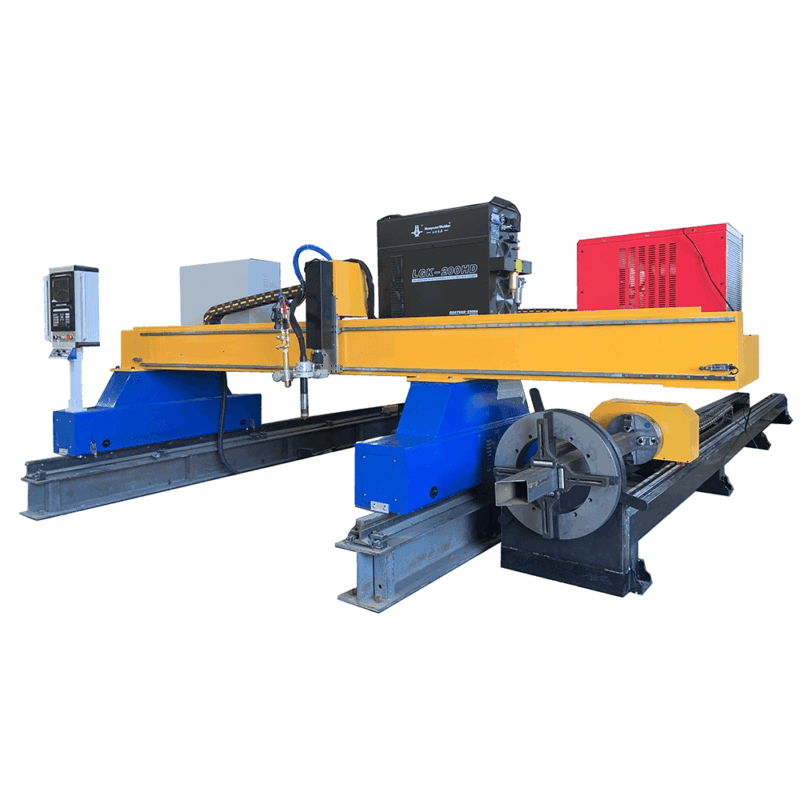
H-Beam Processing and Low Maintenance Operations
The structural skeletons of LNG modules rely heavily on H-beams and I-beams to support heavy liquefaction equipment and storage tanks. In heavy industrial environments, equipment uptime is a critical KPI. Plasma cutting technology offers a distinct advantage in H-beam Processing due to its mechanical robustness and resilience to environmental factors. Unlike systems that rely on sensitive optical components, plasma torches are designed to operate in dusty, vibration-heavy fabrication shops with minimal downtime.
Low maintenance is achieved through the simplicity of the plasma arc delivery system. The consumables—nozzles, electrodes, and swirl rings—are easily replaceable and do not require complex calibration after changeouts. For H-beam processing, the ability to cut through mill scale, rust, and slight surface irregularities without losing arc stability is essential. This reliability ensures that the fabrication of structural supports remains on the critical path of the project schedule, avoiding the bottlenecks associated with more delicate cutting technologies.
Multi-Axis Beveling for Enhanced Weld Preparation
Welding requirements for LNG tanks and piping often specify V, Y, X, or K-style bevels to ensure full penetration. Automated plasma beveling heads, capable of tilting up to 45 or 50 degrees, allow for the completion of complex weld preparations in a single pass. This eliminates the need for secondary grinding or manual beveling, which are labor-intensive and prone to human error.
The integration of a rotating 3D head allows the machine to adjust the bevel angle dynamically as it moves along a contoured cut. This is particularly useful for pressure vessel nozzles where the bevel angle must change constantly relative to the vessel’s radius. By achieving a high-quality surface finish directly from the plasma torch, the facility can move components straight from the cutting table to the assembly jig, significantly reducing the “man-hours per ton” metric that defines project profitability.
The Strategic Role of Offline Programming
In the context of Industry 4.0, the hardware is only as effective as the software driving it. Offline Programming (OLP) is the bridge between the BIM (Building Information Modeling) data and the physical cutting process. In LNG projects, where thousands of unique spools and structural members are required, manual programming at the machine controller is an inefficient use of resources.
OLP software allows engineers to import DSTV or STEP files directly from design platforms like Tekla or SDS/2. The software then automatically generates the toolpaths, nesting configurations, and bevel parameters. This process includes:
1. Automated Collision Detection: Ensuring the torch head does not interfere with the workpiece during complex 3D maneuvers.
2. Optimized Nesting: Reducing scrap rates by strategically placing parts on the raw material, which is critical when dealing with expensive high-nickel steels.
3. Simulation: Visualizing the entire cutting sequence to identify potential issues before any material is consumed.
By moving the programming task to the office environment, the machine remains in constant operation, dedicated solely to cutting. This decoupling of preparation and execution is essential for meeting the aggressive timelines of global energy projects.
Thermal Management and Material Integrity
LNG applications utilize materials like 9% nickel steel or 304/316L stainless steel to maintain ductility at temperatures as low as -196°C. The plasma cutting process must be finely tuned to manage heat input. Industrial engineers specify gas mixtures—such as H35 (35% hydrogen, 65% argon) or nitrogen—to produce clean, dross-free cuts on these alloys. The high travel speeds of modern plasma systems minimize the residence time of the heat source, thereby narrowing the heat-affected zone and preventing the precipitation of carbides that could lead to intergranular corrosion in the field.
Conclusion: Engineering a Seamless Workflow
The implementation of a plasma cutting system with integrated offline programming transforms the fabrication workflow for LNG infrastructure. By focusing on the precision of intersections and the efficiency of structural profile processing, engineers can ensure that every component meets the rigorous safety and quality standards of the energy sector. The reduction in manual labor through automated beveling and the high uptime afforded by low-maintenance plasma hardware create a scalable production model. Ultimately, the synergy between robust mechanical execution and sophisticated digital preparation allows for the delivery of complex LNG modules that are both structurally sound and economically viable.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.