Optimization of Heavy Plate Fabrication in Energy Infrastructure
In the construction of Oil & Gas Tanks, the transition from traditional plate processing to high-definition plasma systems represents a critical shift in production efficiency. The primary engineering challenge in this sector involves managing large-format carbon steel and stainless steel plates, often exceeding 25mm in thickness, while maintaining the tight tolerances required for mechanized joining processes. Unlike standard structural steelwork, tank fabrication demands rigorous adherence to geometric circularity and edge preparation standards. This is where a precision-engineered Plasma Cutting Machine becomes the foundational tool for the entire fabrication workflow.
The synergy between cutting accuracy and subsequent welding stages cannot be overstated. When preparing plates for Narrow Gap Welding, the margin for error in the groove geometry is exceptionally slim. Traditional oxy-fuel methods often leave excessive slag and heat-affected zones (HAZ) that require secondary grinding. Modern high-definition plasma systems, however, utilize sophisticated gas-flow dynamics to produce a constricted arc. This result is a cleaner cut with a reduced HAZ, ensuring that the metallurgical properties of the tank shell remain uncompromised during the primary shaping phase.
The Critical Role of Intersection Accuracy
One of the most complex aspects of oil and gas tank construction is the fabrication of nozzle penetrations, manways, and shell-to-roof connections. These components require Intersection Accuracy that accounts for the curvature of the tank wall. An industrial-grade plasma system equipped with 5-axis motion control can calculate the varying bevel angles required as the torch moves along a 3D intersection path. This eliminates the “gap-and-bridge” issues that typically plague manual fit-ups.
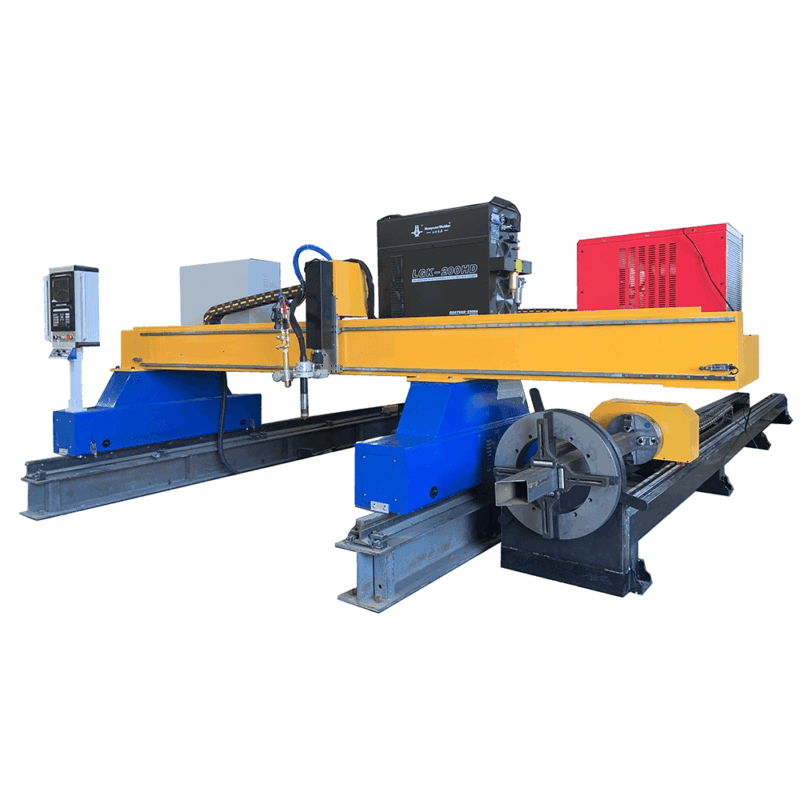
From a mechanical engineering perspective, the intersection of a cylindrical nozzle with a spherical or cylindrical shell requires a non-linear cut path. If the plasma system lacks the necessary motion interpolation, the resulting gap will vary in width, leading to inconsistent weld penetration. High-accuracy plasma cutting ensures that the fit-up is tight enough to support the high-deposition rates of narrow gap processes, where even a 1mm deviation in the root opening can lead to burn-through or lack of fusion. By automating these complex geometries, facilities can reduce the man-hours spent on manual layout and corrective grinding by up to 60%.
Structural Rigidity: H-Beam Frames and Low Maintenance
In heavy industrial environments, the longevity of the cutting platform is directly tied to its structural design. High-end plasma systems for the oil and gas sector utilize heavy-duty H-beam rails and gantry supports. This design choice is not merely about weight capacity; it is about vibration dampening and thermal stability. During high-speed plasma operations, the inertia of the gantry can cause micro-vibrations that translate into “scalloping” on the cut surface. A robust H-beam foundation provides the necessary mass to counteract these forces, maintaining a smooth edge finish.
Furthermore, the focus on low maintenance is a key KPI for industrial engineers. H-beam designs integrated with helical rack-and-pinion drives and oversized linear guideways offer superior resistance to the dust and dross inherent in plasma operations. Unlike lighter aluminum extrusion frames, heavy steel H-beams do not warp under the intense radiant heat generated during long-duration cuts on thick plates. By utilizing self-lubricating blocks and bellows-protected rails, these machines ensure that the “up-time” remains consistent across multi-shift operations. This reliability is vital in large-scale tank farms where a bottleneck at the cutting station can halt the entire assembly line.
Precision Beveling for Narrow Gap Preparation
Narrow gap welding is characterized by a deep, slim groove—typically with an included angle of 1 to 5 degrees—designed to minimize the volume of weld metal required. Achieving this specific geometry requires a plasma head capable of precise beveling. Modern plasma torches can tilt up to 45 or even 50 degrees, allowing for V, Y, X, and K-type joints. However, for narrow gap applications, the machine’s ability to maintain a constant “torching height” via voltage-sensing height control is paramount.
The engineering advantage of using plasma for beveling lies in the speed of the bevel-on-the-fly capability. Rather than cutting a square edge and then performing a second pass for the bevel, the 5-axis plasma head performs the beveling during the initial profile cut. This single-pass approach ensures that the bevel angle is perfectly synchronized with the plate’s perimeter. In the context of oil and gas tanks, where circumferential seams can span dozens of meters, the consistency of this bevel angle determines whether a mechanized narrow gap welding head can travel the entire circumference without manual intervention to adjust for fit-up variances.
Thermal Management and Kerf Compensation
When cutting thick sections for heavy-duty tanks, thermal expansion becomes a variable that engineers must account for. As the plasma arc introduces heat into the plate, the material expands. High-performance CNC controllers integrate real-time kerf compensation and thermal scaling factors. This ensures that the final dimensions of the part, once cooled, match the CAD specifications exactly. For narrow gap welding, where the root face (land) must be consistent to support the first pass of the weld, this level of thermal control is a prerequisite.
The plasma gas chemistry also plays a role in the weldability of the edge. By utilizing oxygen as the plasma gas for carbon steel, the system achieves a faster cut speed and a square edge with minimal dross. For stainless steel applications in the chemical storage segment of oil and gas, H35 (a hydrogen-argon mix) or F5 (nitrogen-hydrogen) gases are used to prevent oxidation of the cut face. This clean, oxide-free edge is essential for narrow gap welding, as it prevents inclusions and porosity in the high-integrity weld beads required by API 650 or ASME Section VIII standards.
Data-Driven Production and ROI
Implementing a high-precision plasma solution is an investment in the entire lifecycle of the tank. By reducing the volume of filler metal through precise narrow gap prep, the cost savings in consumables alone can justify the capital expenditure of the machine. Furthermore, the reduction in arc-on time for welding—enabled by the optimized joint design—leads to faster tank completion. Industrial engineers should evaluate these machines based on their ability to deliver consistent results over thousands of meters of cutting, the rigidity of their H-beam supports, and the sophistication of their nesting software which minimizes plate waste in large-diameter tank projects.
In conclusion, the focus on plasma cutting technology within the oil and gas sector is driven by the need for geometric precision and mechanical reliability. By prioritizing intersection accuracy and robust H-beam construction, fabricators can meet the stringent demands of modern energy infrastructure while maintaining a competitive edge through reduced maintenance and optimized welding preparation.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.