Engineering Precision: 5-Axis Plasma Systems in Oil & Gas
In the heavy fabrication sector of the oil and gas industry, the production of storage tanks and pressure vessels demands a rigorous adherence to structural integrity. The transition from manual layout and cutting to automated Plasma Cutting Machine technology has redefined the throughput capabilities of modern fabrication shops. Specifically, the implementation of 5-axis beveling systems addresses the most critical bottleneck in tank production: the preparation of weld joints for thick-walled steel plates.
Industrial engineers prioritize plasma technology for this application due to its high energy density and ability to maintain consistent cutting speeds across varying plate thicknesses, typically ranging from 10mm to over 50mm. Unlike traditional 2D cutting, 5-axis systems introduce rotational and tilting axes (A and B), allowing the torch to maneuver around complex geometries. This capability is not merely a luxury but a necessity when dealing with the curved surfaces of cylindrical tank shells and dished ends.
Maximizing Intersection Accuracy for Nozzle Fit-ups
One of the most complex challenges in tank fabrication is the creation of openings for nozzles, manways, and piping connections. These intersections require precise holes cut into curved surfaces, often requiring a variable bevel angle to ensure uniform root gaps for the subsequent welding process. This is where intersection accuracy becomes the primary KPI for any industrial engineer evaluating a plasma system.
When a nozzle meets a cylindrical shell, the intersection line is a non-planar curve. A standard 3-axis machine cannot provide the necessary edge preparation because the torch must remain perpendicular to the plate. A 5-axis plasma head, however, utilizes sophisticated algorithms to adjust the torch angle dynamically as it follows the path of the cut. This ensures that the weld prep—whether it be a V, X, or K profile—remains consistent relative to the nozzle’s insertion angle. High intersection accuracy reduces the need for manual back-gouging and excessive filler metal, directly lowering the cost per joint.
The Structural Advantage of H-Beam Gantry Designs
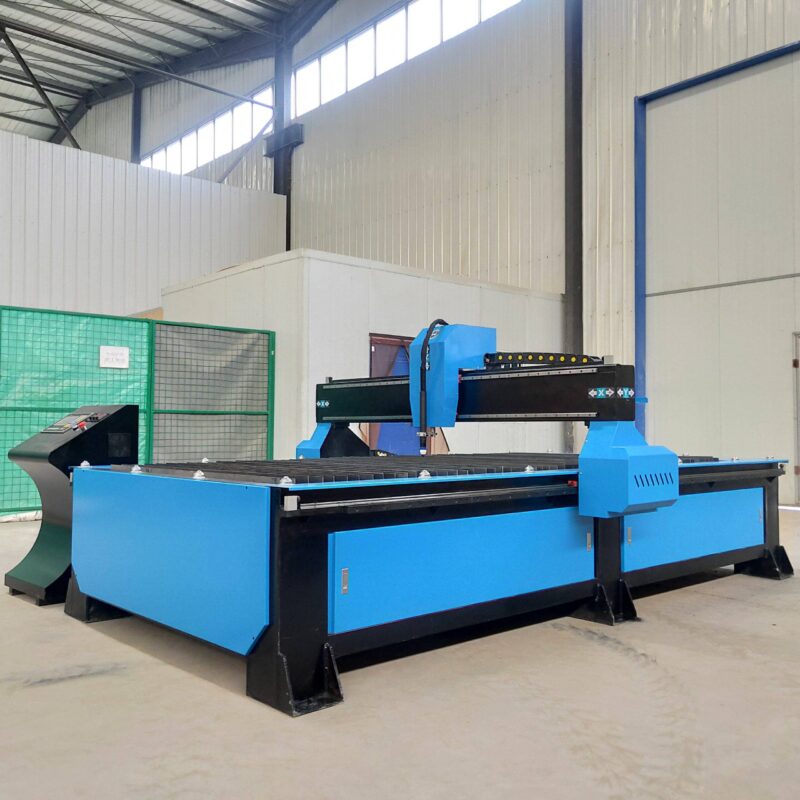
The environment of an oil and gas fabrication facility is harsh, characterized by heavy dust, high temperatures, and the movement of massive steel plates. To maintain long-term precision, the mechanical backbone of the plasma machine must be exceptionally rigid. Industrial engineers favor H-beam low maintenance designs for the gantry and rail systems over lighter alternatives.
Vibration Damping and Rigidity
The H-beam structure provides a high moment of inertia, which is critical for damping the vibrations generated by high-speed torch movements and the rapid acceleration of the 5-axis head. Minimal vibration translates to a smoother cut surface and a smaller heat-affected zone (HAZ). From a maintenance perspective, the heavy-duty nature of H-beam rails means they are less susceptible to deformation under the thermal stress of continuous operation.
Reduced Calibration Frequency
Precision in 5-axis cutting is highly dependent on the alignment of the gantry. Lightweight frames often require frequent recalibration due to the mechanical stresses of supporting a heavy 5-axis bevel head and the umbilical cables for the plasma power supply. The robust H-beam construction ensures that the machine retains its squareness and volumetric accuracy over years of multi-shift operation, leading to lower total cost of ownership (TCO).
Advanced Beveling Profiles and Weld Preparation
In the context of ASME Section VIII or API 650 standards, the quality of the bevel profile is paramount. 5-axis beveling allows for the automation of complex edge preparations that were previously performed by hand-held torches or secondary machining.
Top-Down and Bottom-Up Beveling
The ability to tilt the torch up to 45 or even 50 degrees enables the machine to produce Y-grooves and K-grooves in a single pass or through sequenced multi-pass logic. In oil and gas tanks, where longitudinal and circumferential seams must withstand high internal pressures, the consistency of these bevels ensures deep penetration welds and minimizes the risk of radiographic failure.
Kerf Compensation in 5-Axis Logic
Plasma cutting involves an ionized gas stream that is naturally slightly tapered. To achieve high-precision bevels, the control software must apply complex kerf compensation that accounts for the tilt angle of the torch. Modern 5-axis controllers calculate the offset in real-time, ensuring that the dimensional integrity of the part remains within the tight tolerances required for automated tank assembly.
Optimizing Material Handling and Throughput
Beyond the cut itself, the integration of a plasma machine into a tank production line requires a focus on workflow efficiency. Large-format tables, often exceeding 3 meters in width and 12 meters in length, allow for the nesting of multiple shell plates. When combined with a 5-axis head, the machine can cut the perimeter of the plate to size and apply the necessary bevels for the girth seams in one continuous program.
This consolidation of processes eliminates the “work-in-progress” (WIP) lag time associated with moving plates to a separate beveling station. By performing the 5-axis beveling on the same table where the initial profile is cut, the industrial engineer maximizes the duty cycle of the plasma power source and optimizes the footprint of the fabrication hall.
Conclusion: The ROI of Automated Plasma Beveling
For the fabrication of oil and gas tanks, the move toward automated 5-axis plasma cutting is a strategic investment in quality and scale. By focusing on machines that offer high intersection accuracy and utilize an H-beam low maintenance architecture, facilities can achieve a level of precision that meets the most demanding regulatory codes. The reduction in manual labor for weld preparation, combined with the decreased consumption of welding consumables due to tighter fit-ups, provides a clear and rapid return on investment. In the competitive landscape of energy infrastructure, the ability to produce high-integrity vessels with minimal secondary processing is the ultimate operational advantage.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.