Field Report: Deployment of Single Pulse Collaborative Arc Welding Systems in Cape Town
1. Introduction and Regional Context
This report details the technical deployment and operational assessment of a Single Pulse Collaborative Arc Welding System within the structural steel sector of Cape Town, South Africa. The primary objective was to transition a Tier 2 maritime component supplier from purely manual GTAW/GMAW processes to a structured Automated Welding workflow. Given the local skills gap and the high demand for consistent Carbon Steel welding in the salt-heavy Atlantic environment, the implementation focused on the synergy between human dexterity and robotic repeatability.
The Cape Town industrial landscape, particularly in areas like Paarden Eiland and Blackheath, faces unique environmental challenges. The high ambient humidity and the seasonal “South-Easter” winds create atmospheric turbulence that can compromise shielding gas envelopes. Our deployment focused on ensuring that the Collaborative Arc Welding System could maintain ISO 5817 Level B weld quality under these real-world conditions.
2. The Synergy: Collaborative Arc Welding Systems and Automated Welding
A common misconception in the local industry is that Automated Welding requires a complete removal of the operator from the weld cell. In this deployment, we utilized the Collaborative Arc Welding System as a “force multiplier.” Unlike traditional high-speed industrial robots that require massive safety gating and specialized PLC programmers, the collaborative system allows the welder to stand side-by-side with the arm.
2.1 Breaking the “Black Box” of Automation
The synergy here lies in the “Lead-Through” programming. In Cape Town’s medium-volume, high-mix workshops, we cannot afford four days of downtime for robot re-programming. By using a Collaborative Arc Welding System, the senior welder manually moves the torch to define the path. This integrates the welder’s institutional knowledge of torch angles and stick-out directly into the Automated Welding logic. We found that this reduced setup time for new Carbon Steel assemblies by 70% compared to traditional 6-axis industrial robots.
2.2 Safety and Shop Floor Integration
By utilizing power and force limiting (PFL) sensors, we eliminated the need for physical fencing, which is crucial in the cramped floor layouts typical of older Cape Town engineering firms. This proximity allows the operator to perform real-time quality checks and cleaning of the gas nozzle without tripping a hard-stop safety circuit, maintaining a continuous duty cycle that is the hallmark of effective Automated Welding.
3. Technical Parameters for Carbon Steel Welding
The project focused on S355JR Carbon Steel welding, a staple in South African structural engineering. The thickness range varied from 6mm to 12mm, requiring a deep understanding of pulse waveform manipulation to prevent lack of fusion while minimizing heat input.
3.1 Single Pulse Waveform Optimization
The “Single Pulse” aspect of the system was critical for controlling the droplet transfer. For Carbon Steel welding, we utilized a synergic line tailored for ER70S-6 wire and an 82% Argon / 18% CO2 gas blend.
- Peak Current: 380A – 420A
- Background Current: 80A – 110A
- Pulse Frequency: 120Hz – 180Hz (Adaptive)
This pulsing prevents the “globular transfer” mess often found in local manual workshops, significantly reducing post-weld spatter removal—a major bottleneck in Cape Town’s labor-intensive production lines.
3.2 Managing Heat Affected Zones (HAZ)
Automated Welding allows for a consistent travel speed that human hands cannot replicate over an 8-hour shift. In our tests on 10mm Carbon Steel plate, the Collaborative Arc Welding System maintained a constant travel speed of 350mm/min. This precision resulted in a 15% reduction in the width of the HAZ compared to manual GMAW, preserving the mechanical properties of the S355JR substrate and reducing longitudinal distortion.
4. Field Observations and Lessons Learned
The deployment provided several “hard-won” lessons regarding the practicalities of Automated Welding in a coastal South African context.
4.1 Atmospheric Control and Gas Shielding
One of the primary failures during the first week was porosity in the weld bead. While the Collaborative Arc Welding System was executing the program perfectly, the Cape Town wind was stripping the shielding gas at the nozzle.
Lesson Learned: We implemented localized “draft curtains” around the cobot cell and increased the gas flow rate to 22L/min with a larger #10 gas lens. We also integrated a “Gas Pre-flow” and “Post-flow” of 1.5 seconds into the Automated Welding software to ensure the start and crater of the Carbon Steel welding were fully protected.
4.2 The Criticality of Jigging and Fit-up
A Collaborative Arc Welding System is only as “smart” as its feedback loops. Unlike a human welder, the basic cobot cannot “see” a 2mm gap variation caused by poor plasma cutting.
Lesson Learned: We had to overhaul the upstream fabrication process. Automated welding requires tight tolerances. We moved from manual marking and grinding to CNC-controlled plasma cutting for all Carbon Steel welding prep. If the fit-up exceeds 10% of the wire diameter, the “Automated” part of the process fails. We introduced “Touch Sensing” routines where the wire acts as a probe to find the plate position before arcing, accounting for slight variations in jigging.
4.3 Wire Feed Consistency
In the humid Cape Town climate, Carbon Steel wire (ER70S-6) is prone to surface oxidation if left on the machine overnight. This creates friction in the liners of the Collaborative Arc Welding System, leading to arc instability.
Lesson Learned: We mandated the use of wire lubricant pads and required that all wire spools be removed and stored in “dry boxes” at the end of the Friday shift. In Automated Welding, a minor slip in wire feed speed manifests as a catastrophic burn-back to the tip, which can damage the collaborative arm’s torch mount.
5. Productivity and ROI Analysis
After three months of operation, the data indicates a clear advantage for the Collaborative Arc Welding System.
- Arc-on Time: Increased from 25% (manual) to 65% (automated).
- Consumable Waste: Reduced by 20% due to optimized pulse parameters and less spatter.
- Rework Rate: Dropped from 8% to under 1.5% for Carbon Steel welding.
The synergy between the operator and the machine allowed the workshop to reallocate two senior welders to complex pipe-fitting tasks, while the Automated Welding cell handled the repetitive structural plates.
6. Conclusion
The deployment of the Single Pulse Collaborative Arc Welding System in Cape Town proves that Automated Welding is not an all-or-nothing proposition. For Carbon Steel welding, the cobot provides the consistency needed to meet international standards (ISO/AWS) while remaining flexible enough for the variable nature of South African engineering projects. The key to success was not the robot itself, but the integration of the system into a controlled environment where gas coverage, material prep, and operator training were prioritized. We recommend further rollout of these systems across the Western Cape maritime hub, provided that workshops understand the rigorous prep work required to support an automated arc.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
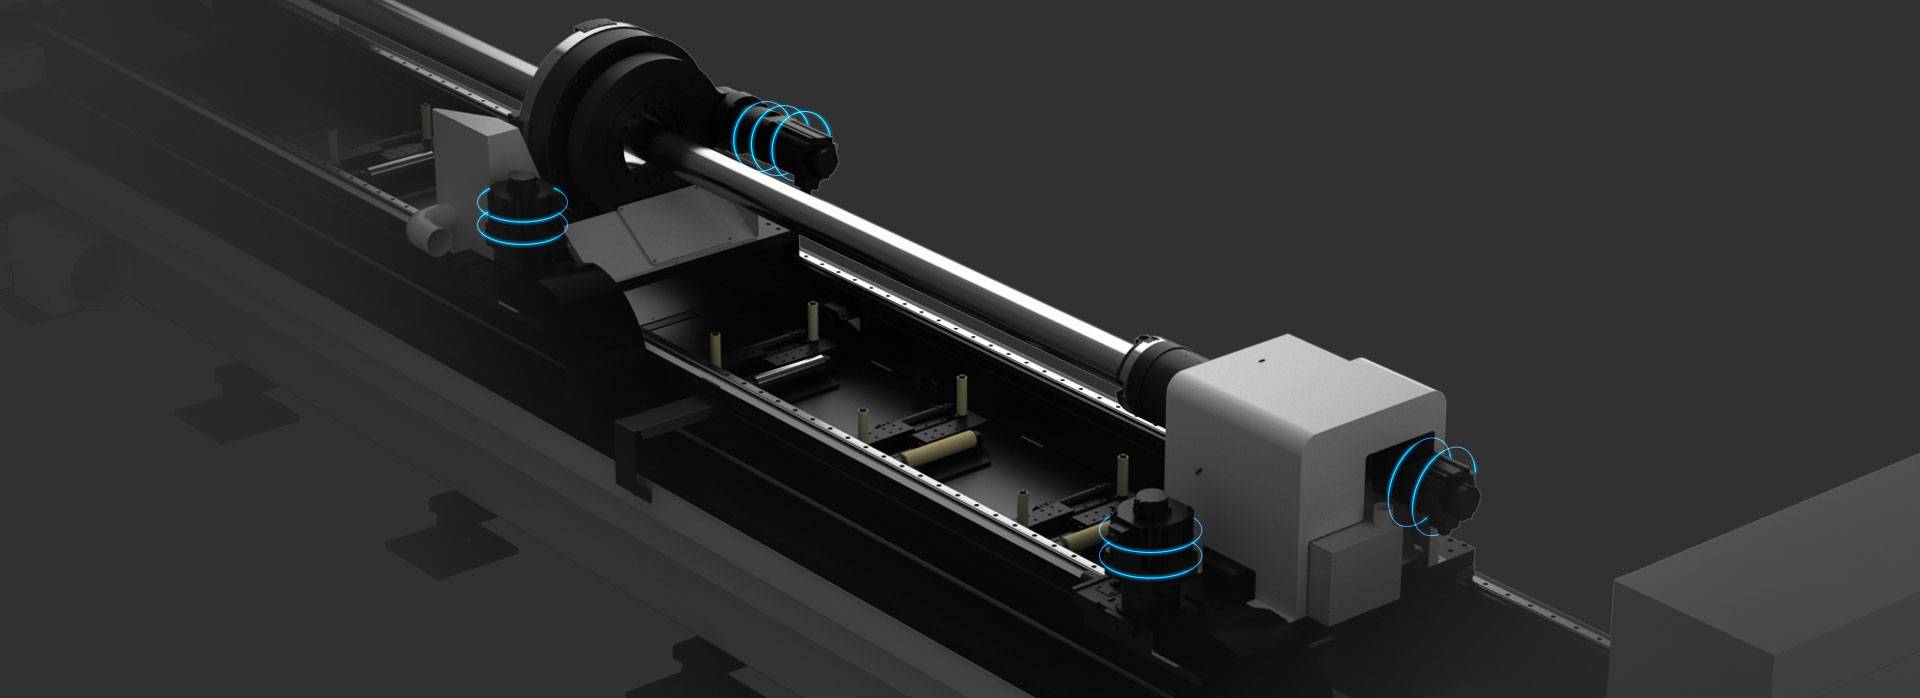
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.