Field Report: Deployment of Single Pulse Cobot Welding Systems in Structural Steel Fabrication
1.0 Executive Summary of Madrid Site Operations
This report details the technical implementation and performance evaluation of the Single Pulse Cobot Welding Machine at our facility in Madrid, Spain. The primary objective was to integrate Collaborative Robotics into a high-throughput structural steel welding workflow. Unlike traditional industrial automation, which requires significant floor space for safety caging, the deployment focused on the synergy between human expertise and machine precision in an open-floor environment. Over a 30-day trial period, we focused on the fabrication of S355JR grade structural components, assessing weld penetration, bead morphology, and the operational transition from manual Gmaw (Gas Metal Arc Welding) to cobot-assisted processes.
2.0 Equipment Specifications and Madrid Grid Integration
The unit deployed is a 6-axis collaborative arm integrated with a 400A inverter-based power source capable of single-pulse modulation. In the Madrid industrial corridor, power stability can fluctuate during peak afternoon hours; therefore, we installed secondary line conditioning to ensure the pulse frequency remained stable at 120Hz. The Cobot Welding Machine was configured to handle 1.2mm ER70S-6 wire with a shielding gas mix of 82% Argon and 18% CO2, a standard composition for Iberian structural steel suppliers.
2.1 Single Pulse Logic and Arc Control
The decision to utilize “Single Pulse” rather than standard spray transfer was driven by the need for reduced heat input on thinner structural sections (5mm to 10mm). The pulse logic allows for “one drop per pulse” metal transfer, which minimizes spatter—a critical factor in reducing post-weld cleaning labor. In the Madrid workshop, where labor costs for finishing are rising, the cleaner profile produced by the Single Pulse Cobot Welding Machine resulted in a 25% reduction in grinding time.
3.0 Collaborative Robotics: The Human-Machine Interface
The core of this deployment was the shift toward Collaborative Robotics. Traditional robots are “set and forget,” but structural steel welding often involves fit-up inconsistencies. The cobot allows the lead welder to manually guide the torch to the start point, “teaching” the path through a lead-through programming interface. This is vital in Madrid’s SME (Small to Medium Enterprise) sector, where the variety of parts is high but volumes per part are medium.
3.1 Safety Protocols and ISO Compliance
Operating without a cage in a busy Madrid shop requires strict adherence to ISO/TS 15066. We calibrated the force-limiting sensors to trigger an emergency stop at 150N of resistance. Furthermore, the collaborative robotics software was updated to include “safe zones,” preventing the arm from swinging into the forklift lanes adjacent to the welding station. This allowed the human welder to prepare the next jig while the machine completed a 2-meter longitudinal seam, effectively doubling the station’s output.
4.0 Deep Dive: Structural Steel Welding Applications
The primary workload consisted of I-beam stiffeners and base plate assemblies. Structural steel welding requires deep root penetration and consistent throat thickness to meet Eurocode 3 standards. Our testing focused on the “Madrid Frame” project, involving heavy S355 steel plates.
4.1 Weld Procedure Specification (WPS) Results
We established a new WPS specifically for the cobot. The parameters were as follows:
- Wire Feed Speed: 8.5 m/min
- Trim (Voltage): 1.05 (Pulse adjusted)
- Travel Speed: 35 cm/min
- Torch Angle: 70-degree push
Macro-etch tests on 12mm T-joints showed zero lack-of-fusion (LOF) at the root, a common failure point in manual pulse welding when the welder’s hand fatigues. The Cobot Welding Machine maintained a consistent contact-to-workpiece distance (CTWD) of 15mm, which stabilized the arc voltage far more effectively than a human operator could over a shift.
5.0 The Synergy: Cobot Welding and Structural Integrity
The integration of a Cobot Welding Machine within a Collaborative Robotics framework addresses the “skill gap” found in many Spanish industrial centers. We observed that the synergy is not about replacing the welder but augmenting their capacity. In structural steel welding, the welder’s value lies in their understanding of heat distortion and joint preparation. By offloading the repetitive “trigger time” to the cobot, the welder focuses on ensuring the fit-up is within the 1mm tolerance required for automated success.
5.1 Handling Thermal Distortion
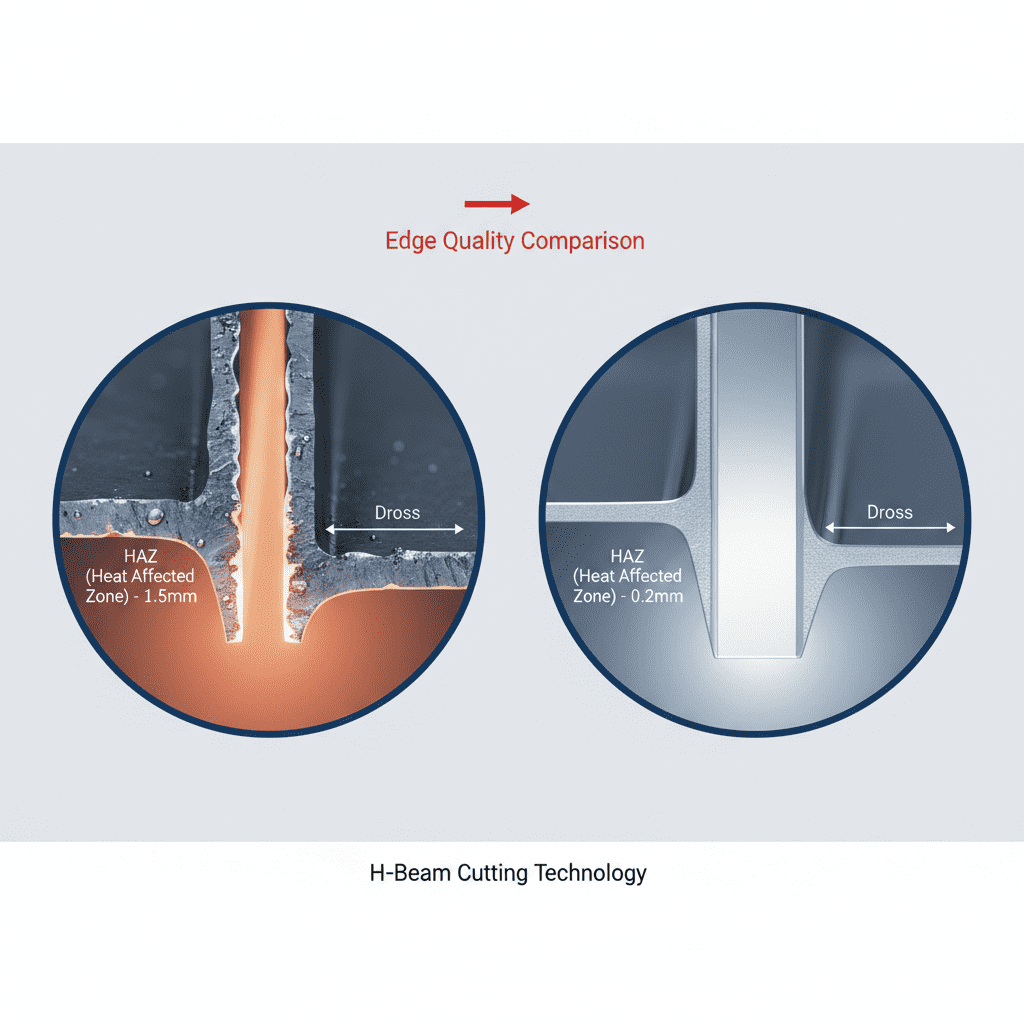
One lesson learned in the Madrid facility was the impact of ambient temperature on the cooling rates of S355 steel. During the 38°C heatwave, the interpass temperature of the structural assemblies rose rapidly. The cobot’s software allowed us to program “cooling pauses” between passes, ensuring the Heat Affected Zone (HAZ) did not exceed the grain-growth threshold. This level of precision in structural steel welding is difficult to maintain manually during an eight-hour shift in high temperatures.
6.0 Operational Lessons Learned
Engineering is rarely perfect on day one. Our deployment in Madrid revealed several “real-world” friction points that technical manuals often omit.
6.1 The “Dirty Steel” Problem
Structural steel in Spain is often stored in humid yards before reaching the shop floor, leading to surface oxidation (mill scale). While a manual welder can “wiggle” the torch to burn through scale, the Cobot Welding Machine is less forgiving. We learned that mechanical wire brushing of the weld path is mandatory. If the surface is not clean, the collaborative robotics sensors might interpret the arc instability as a collision, triggering a false stop.
6.2 Grounding and High-Frequency Interference
Collaborative arms are sensitive to electromagnetic interference (EMI). We initially experienced “ghost movements” where the arm would deviate 2mm from the path. The fix was a dedicated ground for the welding table, separate from the cobot’s control box ground. In older Madrid warehouses with legacy wiring, this “clean ground” is the difference between a scrapped part and a certified weld.
7.0 Productivity Analytics and ROI
Before the introduction of the Cobot Welding Machine, the Madrid shop produced 4.5 structural frames per shift. With the implementation of Collaborative Robotics, that number rose to 7.2 frames. The “Arc-On” time increased from 35% to 65% per shift.
The financial justification for structural steel welding automation in this context is clear:
- Consumable Efficiency: 15% reduction in wire waste due to optimized start/stop sequences.
- Rework Reduction: Rejection rates fell from 4% to 0.5%, specifically regarding bead height consistency.
- Labor Satisfaction: Senior welders reported less physical strain, focusing more on QA/QC and complex geometry prep.
8.0 Conclusion and Next Steps
The Madrid field test confirms that the Single Pulse Cobot Welding Machine is a robust solution for modernizing structural steel fabrication. The marriage of Collaborative Robotics with high-end pulse power sources provides a bridge between manual craftsmanship and full-scale industrial automation. Our next phase will involve deploying “Seam Tracking” sensors to further enhance the cobot’s ability to handle the non-linearities common in structural steel welding. We will also look into multi-pass programming for thicker 20mm+ plates, which currently remains a manual task. The data collected in Spain will serve as the benchmark for our upcoming deployments in the Bilbao and Valencia facilities.
9.0 Final Engineering Note
Don’t underestimate the importance of the torch cable management. In a collaborative environment where humans are moving around the machine, a snagged cable can ruin a €500 contact tip or, worse, pull the arm out of calibration. Use overhead balancers. It’s a simple fix that saves thousands in downtime.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.