Engineering Review: Multi-pass Welding Robotic Arm Welder – Pune, India
In this article
- Field Report: Multi-pass Integration for Robotic Arm Welder Systems
- Location: Industrial Hub, Pune, India
- 1. Synergy: Robotic Arm Welder and Industrial Automation
- 2. Technical Challenges in Thin Metal Sheet Welding
- 3. Implementation Data and Parameter Tuning
- 4. Lessons Learned: The Pune Field Experience
- Addressing Voltage Fluctuations
- Managing Dust and Wire Feed
- The “Human” Element of Automation
- 5. Precision in Multi-pass Programming
- 6. Quality Assurance and Throughput Metrics
- 7. Concluding Technical Summary
Field Report: Multi-pass Integration for Robotic Arm Welder Systems
Location: Industrial Hub, Pune, India
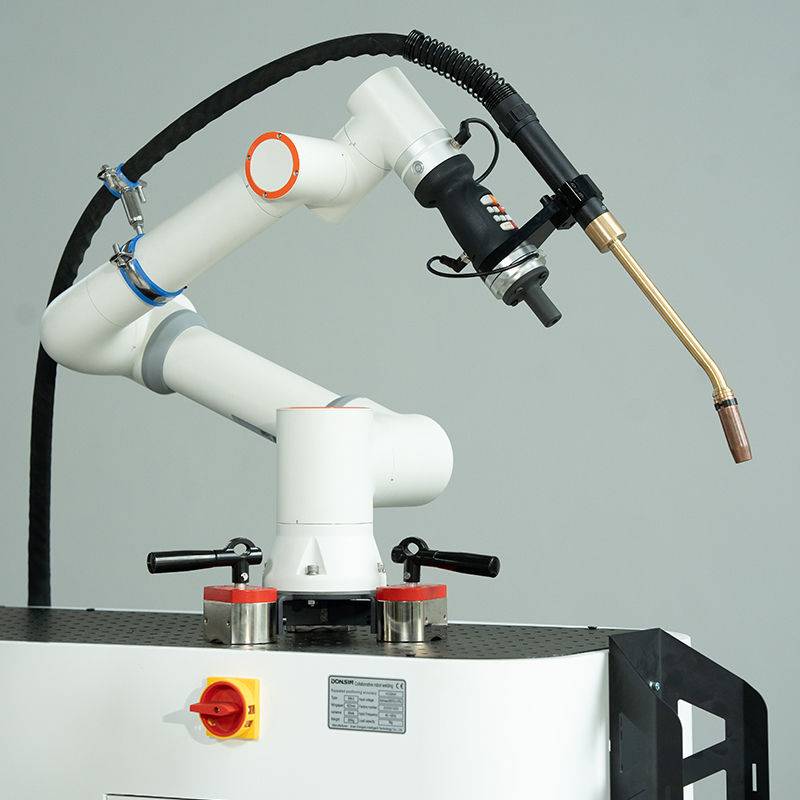
This report outlines the technical deployment and optimization of a 6-axis Robotic Arm Welder within a high-throughput manufacturing facility in Pune. The project’s objective was to transition a manual multi-pass welding station for thin-walled pressure vessels into a fully realized **Industrial Automation** cell.
In the Pune region, environmental factors—specifically high ambient humidity during the monsoon and significant dust ingress—necessitate a specific approach to hardware maintenance and shielding gas integrity. The primary challenge addressed here is the application of multi-pass techniques to Thin Metal Sheet welding (2.5mm to 4.0mm thickness), where thermal distortion is the primary cause of rejection.
1. Synergy: Robotic Arm Welder and Industrial Automation
The integration of a Robotic Arm Welder is often misunderstood as a simple replacement for a manual operator. In the context of Industrial Automation, the robot is merely the executioner; the success of the cell depends on the “ecosystem”—the jigs, the synchronized positioners, and the programmable logic controllers (PLCs) that manage the cycle time.
In our Pune installation, we utilized a FANUC ARC Mate series integrated with a Lincoln Electric Power Wave source. The synergy here is found in the communication speed between the power source and the arm’s motion controller. When we speak of Industrial Automation, we are referring to the ability of the system to adjust wire feed speed and voltage in real-time based on the robot’s TCP (Tool Center Point) velocity.
In a manual environment, an operator in a Pune workshop might compensate for a slightly off-center seam by eye. In an automated environment, we implemented laser-touch sensing. The Robotic Arm Welder probes the joint before the arc ignition, updating its path coordinates to account for any upstream fabrication tolerances. This is where automation moves from “blind repetition” to “intelligent execution.”
2. Technical Challenges in Thin Metal Sheet Welding
Thin Metal Sheet welding presents a narrow window for error. Unlike heavy plate welding, where heat soak is managed by the sheer mass of the substrate, thin sheets (specifically the 3mm CRCA steel used in this project) are prone to:
1. Burn-through: Excessive heat input localized in one area.
2. Warpage: Differential cooling causing the sheet to “oil-can” or twist.
3. Inconsistent Penetration: Often caused by the rapid travel speeds required to keep heat input low.
To combat this, we moved away from the traditional single-pass high-amperage approach. Instead, we programmed the Robotic Arm Welder for a dual-pass strategy, despite the material’s thinness.
The Multi-pass Strategy for Thin Gauges
The first pass (Root Pass) was executed at a lower travel speed with a pulsed-MIG (Metal Inert Gas) waveform to ensure 100% penetration without blowing through the gap. The second pass (Cap Pass) utilized a weave pattern—specifically a “crescent” motion programmed into the Robotic Arm Welder—to distribute the heat across a wider surface area, effectively normalizing the stresses introduced by the first pass.
3. Implementation Data and Parameter Tuning
During the commissioning phase in Pune, we identified that standard European or North American weld settings failed due to local variations in power stability and gas purity. We recalibrated the Industrial Automation software to the following parameters for the 3mm joints:
* Wire: 0.8mm ER70S-6.
* Gas: 80% Argon / 20% CO2 (Flow rate increased to 18L/min to compensate for shop-floor drafts).
* Travel Speed (Root): 450 mm/min.
* Travel Speed (Cap): 600 mm/min with a 1.5mm weave frequency.
* Voltage Offset: +0.5V to account for the impedance in the extended cable runs required by the cell layout.
The use of Industrial Automation allowed us to log every “Arc-On” second. We discovered that by using a Robotic Arm Welder, we could maintain a duty cycle of 85%, compared to the 30% achieved by manual welders who required frequent breaks due to the intense Pune heat and ergonomic strain.
4. Lessons Learned: The Pune Field Experience
Addressing Voltage Fluctuations
One of the most critical lessons learned in the Pune industrial belt (specifically the Chakan zone) is the impact of “brownouts” and voltage spikes on sensitive Industrial Automation components. Even with a dedicated transformer, we saw logic errors in the Robotic Arm Welder controller.
* Lesson: Always install a high-capacity Servo Stabilizer and an active power filter specifically for the robot controller and the welding power source. Do not share the ground with heavy stamping presses.
Managing Dust and Wire Feed
The Pune environment is notoriously dusty. In Thin Metal Sheet welding, any particulate matter dragged into the weld pool results in immediate porosity.
* Lesson: We moved from open wire spools to enclosed wire drums with “Quick-Connect” liners. This ensured that the wire remained pristine from the drum to the torch neck of the Robotic Arm Welder, significantly reducing contact tip wear and arc instability.
The “Human” Element of Automation
A common mistake in Pune’s manufacturing sector is the belief that a Robotic Arm Welder eliminates the need for a skilled welder.
* Lesson: The most successful operators were our former manual welders who were trained in basic G-code and pendant navigation. They understood the “puddle” and could identify when the Industrial Automation was drifting due to a worn contact tip or a clogged gas nozzle before the sensors even tripped.
5. Precision in Multi-pass Programming
The “Multi-pass” logic in thin-sheet applications requires a deep understanding of the Heat Affected Zone (HAZ). If the Robotic Arm Welder returns for the second pass too quickly, the accumulated heat will cause the thin sheet to lose its structural integrity.
We programmed a “cooling offset” into the Industrial Automation cycle. While the robot finished the root pass on Part A, it would immediately move to Part B for its root pass, allowing Part A to cool below 150°C before returning for the cap pass. This “Interpass Temperature Management” is impossible to do consistently with manual labor at scale, but it is a native strength of a programmed Robotic Arm Welder.
6. Quality Assurance and Throughput Metrics
Post-implementation, the results for the Thin Metal Sheet welding line were quantified over a 30-day period:
* Defect Rate: Dropped from 12% (manual) to 1.5% (automated).
* Consumable Efficiency: 22% reduction in shielding gas waste due to precision solenoid timing in the Industrial Automation suite.
* Post-Weld Grinding: Virtually eliminated. The consistency of the Robotic Arm Welder produced a “stack of dimes” aesthetic that met automotive standards without secondary finishing.
7. Concluding Technical Summary
The deployment of a Robotic Arm Welder for Thin Metal Sheet welding in Pune has proven that the limitations of the material are not an obstacle if the Industrial Automation is configured correctly. The key is not just the robot, but the holistic management of heat, environment, and power stability.
For future installations, we recommend a “Modular Fixture” approach. As the Pune market shifts toward EV (Electric Vehicle) components, the ability to rapidly swap jigs while using the same Robotic Arm Welder programs will be the deciding factor in ROI. We have laid the groundwork here for a system that is not only productive today but adaptable for the lighter-gauge aluminum alloys we expect to see in the coming quarters.
End of Report.
Prepared by:
*Lead Welding Engineer (Robotics & Automation)*







