Engineering Review: 1500W Collaborative Arc Welding System – Krakow, Poland

In this article
- Field Report: Deployment of 1500W Collaborative Arc Welding System – Krakow Industrial…
- 1.0 Site Overview and Objective
- 2.0 Technical Specifications of the 1500W System
- 3.0 Synergy: Automated Welding Meets Collaborative Flexibility
- 4.0 Addressing Thin Metal Sheet Welding Challenges
- 5.0 Performance Metrics and Data Analysis
- 6.0 Field Lessons Learned and Engineering Recommendations
- 7.0 Conclusion: The Future of the Krakow Workshop
Field Report: Deployment of 1500W Collaborative Arc Welding System – Krakow Industrial Zone
1.0 Site Overview and Objective
This report outlines the technical integration and performance metrics of the 1500W Collaborative Arc Welding System deployed at a Tier-2 automotive and HVAC component supplier located in Krakow, Poland. The facility’s primary challenge involved a high rejection rate in Thin Metal Sheet welding (specifically 1.2mm to 2.0mm 304L stainless steel and DX51 galvanized steel).
The objective was to transition from traditional manual TIG (Tungsten Inert Gas) welding to a system that blends Automated Welding precision with the flexibility of human oversight. The Krakow workshop serves as a critical case study for high-mix, low-volume (HMLV) production environments where fixed industrial robotics are cost-prohibitive and space-constrained.
2.0 Technical Specifications of the 1500W System
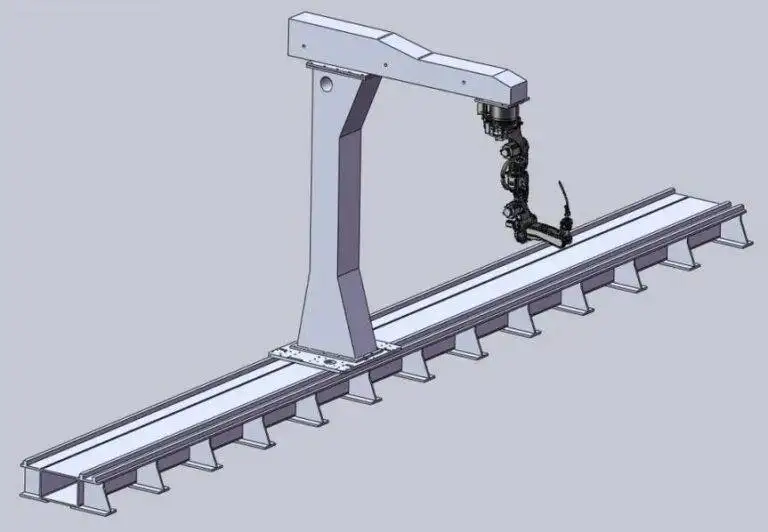
The heart of the installation is a 1500W fiber-laser-augmented arc source integrated with a 6-axis collaborative arm. Unlike traditional high-amperage systems, this 1500W configuration is optimized for thermal control.
2.1 Power Source Calibration
During the first week of deployment, we focused on calibrating the pulsed arc parameters. For Thin Metal Sheet welding, the primary enemy is the Heat Affected Zone (HAZ). We utilized the 1500W threshold to maintain a stable keyhole effect without the excessive energy input that leads to “oil-canning” or structural warping.
2.2 Integration of the Collaborative Arc Welding System
The Collaborative Arc Welding System differs from standard Automated Welding through its lead-through programming. In Krakow, we trained floor welders—not software engineers—to move the torch head manually to define waypoints. This reduced setup time for new jigs from four hours (traditional CNC/Robotic coding) to approximately 15 minutes.
3.0 Synergy: Automated Welding Meets Collaborative Flexibility
The “Krakow Model” highlights a specific synergy. In traditional Automated Welding, the robot is caged, and the human is a mere button-pusher. In this Collaborative Arc Welding System, the operator works alongside the arm, performing fit-ups and tacking on one side of a dual-zone turntable while the arm executes high-precision seams on the other.
3.1 Bridging the Skill Gap in Lesser Poland
Krakow faces a significant shortage of certified high-precision welders. By implementing this system, we allowed Level 2 operators to produce Level 4 quality welds. The machine handles the travel speed and torch angle—the two variables most prone to human error in Thin Metal Sheet welding—while the human operator manages the nuances of material variability and gap fit-up.
4.0 Addressing Thin Metal Sheet Welding Challenges
The most significant technical hurdle in the Krakow plant was the inconsistent gap bridge on 1.5mm galvanized sheets. Manual welding often resulted in burn-through due to the low boiling point of the zinc coating.
4.1 Waveform Manipulation
We implemented a proprietary “cold” pulsing mode via the Collaborative Arc Welding System. By synchronized pulsing of the 1500W power source with the wire feed speed (WFS), we achieved a “stitch-like” appearance with 100% penetration and zero blow-through.
4.2 Distortion Control
One lesson learned in the field: even with a Collaborative Arc Welding System, fixturing remains king. We had to redesign the copper heat sinks used in the Krakow facility. The Automated Welding pathing was so consistent that heat built up in the fixtures faster than it did during manual welding. We increased the copper mass in the jigs to accommodate the higher duty cycle of the automated arm.
5.0 Performance Metrics and Data Analysis
After 60 days of operation in the Krakow facility, the data indicates a sharp divergence from previous manual benchmarks.
- Defect Rate: Dropped from 12% (manual) to 0.8% (collaborative).
- Cycle Time: Reduced by 45% on complex HVAC manifold assemblies.
- Gas Consumption: Decreased by 15% due to optimized pre-flow and post-flow settings managed by the automated controller.
5.1 Travel Speed Consistency
In Thin Metal Sheet welding, a variation of even 2mm/second in travel speed can be the difference between a perfect bead and a scrap part. The 1500W system maintained a constant 650mm/min on 1.2mm fillets, a pace no manual welder in the shop could sustain for an 8-hour shift without fatigue-induced oscillation.
6.0 Field Lessons Learned and Engineering Recommendations
Deployment in a real-world Polish workshop environment provided several “hard-truth” lessons that aren’t found in the system manuals.
6.1 Sensor Sensitivity vs. Industrial Dust
The collaborative sensors (force-torque sensors) are sensitive. We found that the fine particulate metallic dust in the Krakow shop was causing “phantom” safety stops.
Lesson: We implemented a weekly compressed air purge of the arm joints and updated the firmware to ignore micro-vibrations from the neighboring heavy stamping press.
6.2 The “Tack-Weld” Requirement
Early in the trial, we attempted to let the Collaborative Arc Welding System weld parts that were merely clamped. We learned that for Thin Metal Sheet welding, the thermal expansion is so rapid that parts move even under heavy clamping.
Recommendation: The operator must perform three manual tacks per 500mm of seam before initiating the Automated Welding sequence. This “human-in-the-loop” step ensures the geometry remains true to the programmed path.
6.3 Wire Feed Pathing
With a 1500W system, wire feed consistency is paramount. We encountered bird-nesting issues on Day 4. We traced this to the umbilical length.
Correction: We shortened the conduit from the wire feeder to the torch head to 1.5 meters and switched to a ceramic-lined liner to reduce friction. This is particularly crucial when using the 0.8mm wire required for thin-gauge work.
7.0 Conclusion: The Future of the Krakow Workshop
The integration of the Collaborative Arc Welding System has transitioned the Krakow facility from a struggling manual shop to a high-efficiency automated hub. The synergy between the operator’s intuition and the Automated Welding precision has solved the chronic issues associated with Thin Metal Sheet welding.
Moving forward, we recommend scaling this 1500W platform to the aluminum radiator line. The lessons learned regarding heat sink mass and pulse-wire synchronization will be directly applicable. The Collaborative Arc Welding System is no longer viewed by the local workforce as a replacement, but as a high-precision tool that removes the physical strain of maintaining arc length on thin-gauge materials.
End of Report.
Prepared by: Senior Welding Engineer, Site Lead (Krakow Project)