Beam Processing Center with Narrow Gap welding for for Steel Structure
In this article
- Technical Integration of Plasma Cutting in Modern Steel Structure Fabrication
- Precision Intersection Accuracy for Complex Structural Nodes
- H-Beam Production Efficiency and Low Maintenance Architecture
- Advanced Beveling for Narrow Gap Weld Preparations
- Optimizing the Workflow: From Plasma Cut to Finished Weld
Technical Integration of Plasma Cutting in Modern Steel Structure Fabrication
In the current landscape of heavy industrial fabrication, the efficiency of a Beam Processing Center is measured by its ability to facilitate downstream assembly with minimal rework. The adoption of Narrow Gap welding has placed unprecedented demands on the primary cutting stage. Unlike traditional weld preparations, narrow gap processes require extremely tight tolerances in groove geometry to ensure consistent penetration and fusion. This necessitates a transition from manual or basic mechanical cutting to advanced thermal processing systems that prioritize dimensional stability and repeatable accuracy.
Precision Intersection Accuracy for Complex Structural Nodes
The integrity of a Steel Structure often hinges on the fit-up at complex intersections, particularly where H-beams meet at oblique angles or where web-copes are required for clearance. In an industrial engineering context, intersection accuracy is not merely about the final dimension but the consistency of the kerf throughout the depth of the cut.
High-definition Plasma Cutting systems utilize sophisticated arc voltage control and motion interpolation to maintain a perpendicular torch angle relative to the beam’s surface. When processing heavy-walled H-beams, the system must compensate for the natural variance in flange thickness and web centering. Modern beam lines utilize laser probing or mechanical touch-sensing to map the actual geometry of the beam before the first arc is struck. This data is then fed into the CNC controller to adjust the tool path in real-time, ensuring that intersections are cut with a tolerance of +/- 0.5mm. This level of precision is critical for narrow gap preparations, where a gap deviation of even 1mm can lead to excessive weld volume or lack of fusion.
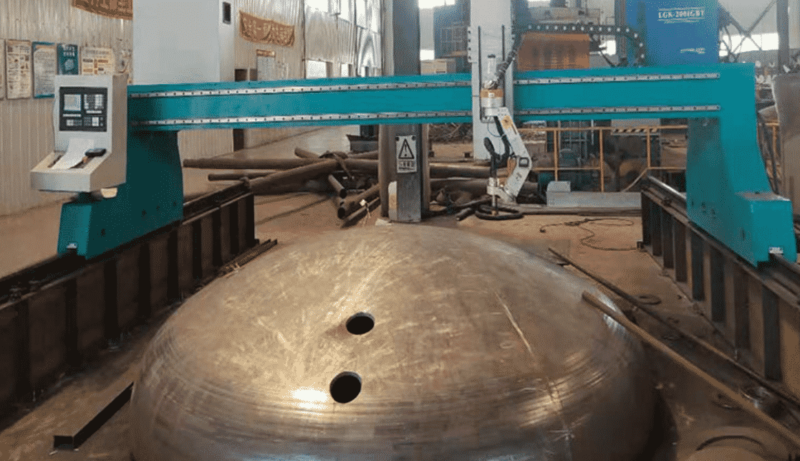
Dynamics of Thermal Kerf Compensation
Achieving high intersection accuracy requires a deep understanding of plasma physics and gas dynamics. The “kerf”—the width of the material removed during the cut—is not constant; it fluctuates based on cutting speed, amperage, and gas pressure. For a beam processing center to remain efficient, the software must employ dynamic kerf compensation. This ensures that the physical part dimensions match the CAD model exactly, regardless of whether the torch is traveling through the 12mm web or the 25mm flange. By stabilizing the arc through refined swirl baffle technology and precise secondary gas mixtures, the system minimizes the taper of the cut edge, which is a prerequisite for high-quality narrow gap joint preparation.
H-Beam Production Efficiency and Low Maintenance Architecture
From an operational standpoint, the total cost of ownership (TCO) of a beam line is heavily influenced by maintenance intervals and machine uptime. Industrial engineers prioritize systems that can withstand the harsh environment of a steel mill, characterized by metallic dust, scale, and high ambient temperatures.
Plasma systems offer a distinct advantage in this regard due to their robust and relatively simple mechanical interface compared to complex mechanical sawing or drilling units. The absence of high-speed moving parts in the cutting head—other than the Z-axis lifter—reduces the frequency of mechanical failure. To further lower maintenance requirements, modern centers utilize self-cleaning torch designs and modular consumable kits. These kits are designed for rapid exchange, minimizing the “mean time to repair” (MTTR).
Slag Management and Extraction Systems
A significant challenge in H-beam processing is the accumulation of dross and slag inside the beam flanges. A low-maintenance system addresses this through integrated fume extraction and slag collection trays. By utilizing a downdraft table design or a traveling extraction hood that follows the plasma torch, the system prevents the build-up of abrasive particulates on the linear guides and rack-and-pinion drives. This protection of the motion system is vital for maintaining long-term positioning accuracy, which directly impacts the quality of the narrow gap weld prep.
Advanced Beveling for Narrow Gap Weld Preparations
The transition to narrow gap welding techniques is driven by the desire to reduce the number of weld passes and the amount of filler material used. However, this technique is only viable if the joint preparation is flawless. This is where multi-axis plasma beveling becomes indispensable.
A 3D plasma head, capable of tilting up to 45 or 50 degrees, allows for the creation of complex bevel profiles—such as V, Y, X, and K-cuts—directly on the beam processing line. For narrow gap applications, the system often produces a deep bevel with a very small included angle (often between 5 to 20 degrees). The ability to maintain a consistent root face and a sharp bevel edge over the entire length of a beam flange is a hallmark of a high-end processing center.
Programming and Kinematics of 5-Axis Plasma Heads
The kinematics of a 5-axis plasma head require complex algorithms to maintain the “Tool Center Point” (TCP) during rotation. If the TCP shifts during a bevel cut, the resulting geometry will be inconsistent, leading to “high and low” spots in the weld groove. In a high-performance beam processing center, the CNC integrates the rotary axes with the linear axes flawlessly. This ensures that even during transition cuts—where the torch moves from a flat flange to a beveled web—the arc length and speed remain constant. This thermal consistency results in a smooth, metallurgical surface finish that requires little to no grinding before the welding process begins.
Optimizing the Workflow: From Plasma Cut to Finished Weld
The ultimate goal of integrating these technologies is the creation of a seamless workflow. When the plasma system delivers a perfectly beveled, accurately dimensioned beam to the welding station, the assembly time is drastically reduced. In narrow gap welding, the volume of the weld puddle is smaller and more controlled; therefore, any irregularity in the base metal preparation is magnified.
By focusing on high-definition plasma cutting, industrial facilities can eliminate the “fit-up” stage where gaps are manually filled or edges are ground to fit. The precision of the plasma cut ensures that the heat input during welding is uniform, reducing the risk of thermal distortion in the final Steel Structure. This holistic approach to engineering—prioritizing the accuracy of the initial cut—is the most effective way to improve the overall equipment effectiveness (OEE) of the entire fabrication facility.
Conclusion: The Future of Beam Processing
The shift toward automated beam processing centers equipped with multi-axis plasma capability represents a significant advancement in structural engineering. By mastering intersection accuracy and beveling precision, and by selecting equipment with a focus on low maintenance and high durability, fabricators can meet the rigorous standards required for modern infrastructure. The synergy between high-definition plasma and narrow gap welding is not just a technical preference but a strategic necessity for competing in a high-efficiency, high-quality global market.






