Beam Processing Center with Narrow Gap welding for for Construction Machinery
In this article
Optimizing Beam Processing via High-Definition Plasma Integration
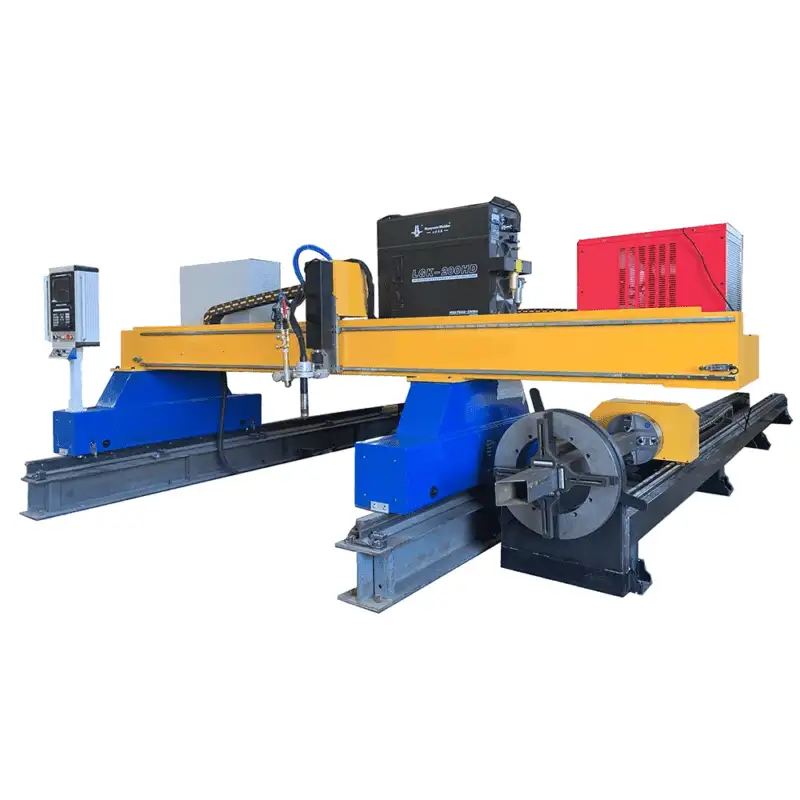
In the fabrication of construction machinery—such as excavator chassis, crane booms, and heavy-duty frames—the structural integrity of H-beams and custom-welded sections is paramount. Industrial engineers are increasingly turning to specialized Beam Processing Centers that prioritize high-definition Plasma Cutting as the primary subtractive method. Unlike traditional mechanical sawing or manual torching, automated plasma systems provide the thermal consistency and geometric precision required for subsequent Narrow Gap Welding (NGW) processes. The efficiency of a production line is measured not just by cutting speed, but by the reduction of secondary operations, making the accuracy of plasma-cut intersections a critical KPI.
Precision Intersection Accuracy for Heavy Structural Loads
The complexity of construction machinery design often involves intersecting beams where flanges and webs must meet at precise angles to distribute stress loads effectively. Plasma Intersection Accuracy is the cornerstone of these assemblies. Automated beam centers utilize multi-axis robotic arms or gantry-mounted plasma torches that compensate for the natural “radius” of the H-beam’s inner corners. When a beam is processed, the software must calculate the kerf compensation and the torch angle dynamically to ensure that the “cope” or the “cut-out” matches the mating beam with tolerances often under 1.0mm.
This level of precision is vital for narrow gap welding. In NGW, the groove angle is significantly reduced to minimize the volume of weld metal used, which in turn reduces heat input and distortion. However, this technique leaves zero room for gaps or misalignment. If the plasma system fails to achieve high-precision intersections, the fit-up will be inconsistent, leading to burn-through or lack of fusion. Therefore, the beam processing center must integrate advanced sensors—such as mechanical probes or laser scanners—to map the actual dimensions of the H-beam, which often vary from theoretical mill specifications, ensuring the plasma arc follows the true centerline of the workpiece.
H-Beam Low Maintenance: Engineering for Reliability
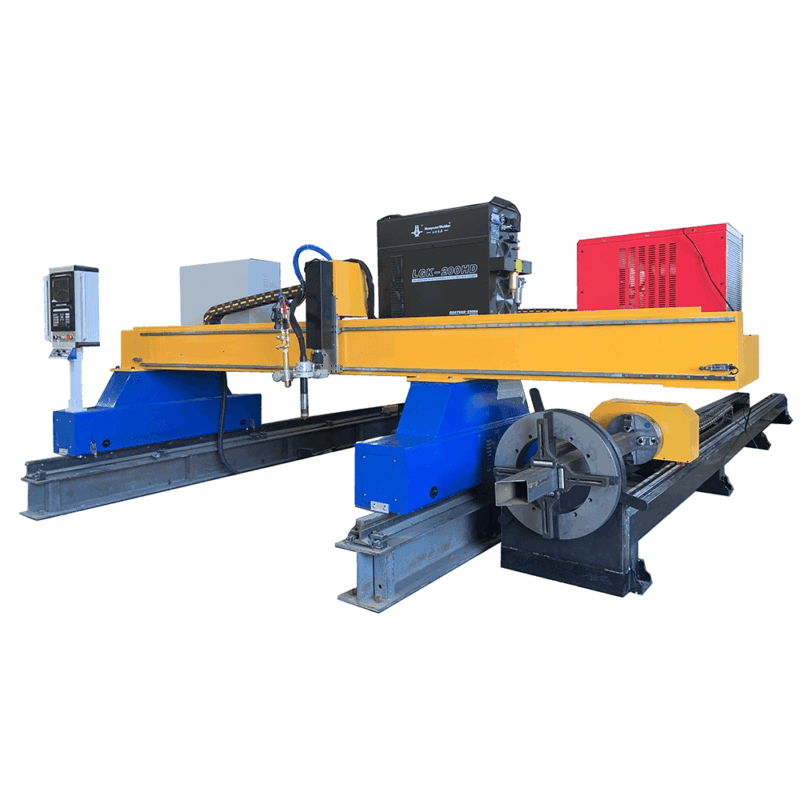
Operational uptime in a heavy machinery plant is dictated by the maintenance cycle of its primary cutting equipment. Modern plasma-based beam centers are engineered for H-Beam Structural Processing with a focus on ruggedness. Traditional mechanical machining centers require constant coolant management and tool sharpening. In contrast, high-definition plasma systems utilize dry cutting or water-shroud technologies that significantly lower the mechanical wear on the machine’s drive system.
To achieve low maintenance, these centers utilize specialized dross management systems and heavy-duty slag conveyors. The plasma torch itself, while a consumable-based tool, features “quick-change” kits that allow operators to swap electrodes and nozzles in under two minutes. From an industrial engineering perspective, the lack of physical contact between the tool (the plasma arc) and the workpiece (the H-beam) eliminates the lateral forces that typically lead to rack-and-pinion wear in milling or sawing centers. This non-contact nature ensures that the structural alignment of the processing center remains calibrated for longer intervals, reducing the Total Cost of Ownership (TCO).
Advanced Beveling for Narrow Gap Preparation
The preparation of weld joints is the most labor-intensive part of construction machinery fabrication. A beam processing center equipped with a 5-axis or 6-axis plasma head can perform Multi-Axis Beveling in a single pass. For narrow gap welding, the bevel profiles—typically deep V, J, or U-grooves—must be executed with extreme consistency along the entire length of the beam flange.
Plasma beveling allows for the creation of complex geometries that would be impossible or prohibitively expensive with mechanical means. By tilting the torch, the system can create a sharp transition from a 0-degree square cut to a 45-degree bevel, facilitating a smooth transition for the welding robot. This capability is particularly useful for heavy-duty box girders used in crane manufacturing. The plasma arc’s ability to maintain a constant standoff distance via voltage control ensures that even if the beam has slight longitudinal warping, the bevel depth remains uniform. This uniformity is the prerequisite for the automated narrow gap welding systems that follow, as they rely on a constant groove geometry to maintain a stable weld pool.
Thermal Management and Material Integrity
A common concern in plasma cutting for heavy machinery is the Heat Affected Zone (HAZ). Industrial-grade beam processing centers mitigate this by using high-current, high-density plasma arcs that move at high travel speeds. This localized heat input ensures that the metallurgical properties of high-strength low-alloy (HSLA) steels, commonly used in construction equipment, are not compromised. By optimizing the gas mix—often using oxygen-plasma for carbon steels—the edge quality is kept free of nitride contamination, which is essential for achieving X-ray quality welds in narrow gap applications.
Digital Integration and Nesting Efficiency
The transition from CAD/CAM designs to a finished beam is managed through integrated software suites that specialize in structural steel. These systems allow for nesting of multiple parts within a single H-beam length, minimizing scrap. The software accounts for the specific characteristics of plasma cutting, such as lead-ins and lead-outs, to ensure that the start and stop points of the cut do not interfere with the critical narrow gap weld prep areas. This digital thread ensures that every hole, notch, and bevel is perfectly positioned relative to the beam’s datum points, eliminating manual layout and the associated human error.
Final Considerations for Implementation
For facilities producing earth-moving and lifting equipment, the shift toward a plasma-centric beam processing center is a strategic move to increase throughput. The synergy between high-precision plasma cutting and narrow gap welding represents the current pinnacle of structural steel fabrication. By focusing on intersection accuracy, the system ensures that complex assemblies are self-fixturing. By reducing maintenance through robust mechanical design and non-contact cutting, the facility ensures consistent production flow. Ultimately, the ability to perform complex beveling automatically transforms the plasma cutter from a simple tool into a sophisticated preparation center for high-value welding operations.






