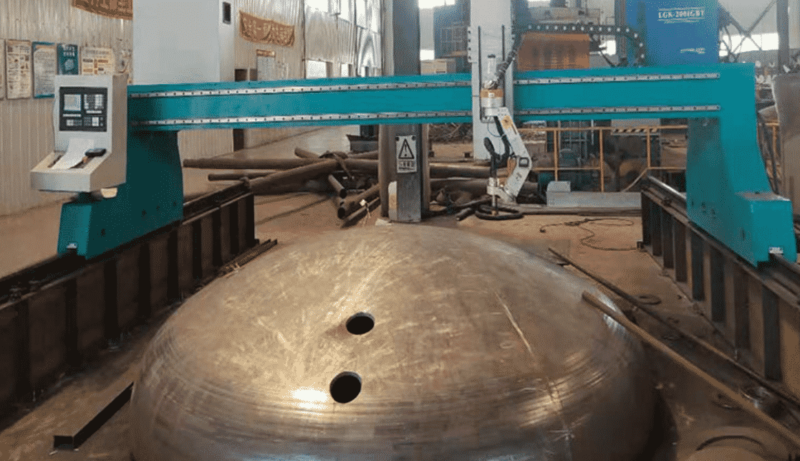
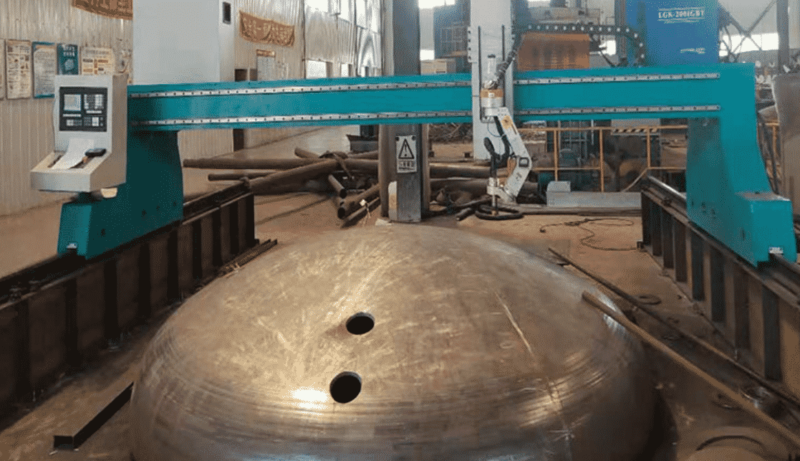
Beam Processing Center with Arc Voltage Control for for LNG Projects
In this article
Technical Optimization of Beam Processing in LNG Infrastructure
The construction of LNG terminals and processing plants involves high-spec structural steel requirements that demand extreme precision and repeatable results. For industrial engineers overseeing these projects, the Beam Processing Center represents the primary pivot point for production efficiency. Unlike standard commercial construction, LNG projects utilize heavy-wall H-beams, channels, and hollow sections that must interface perfectly to ensure the integrity of the cryogenic containment systems and supporting modules.
The shift toward automated Plasma Cutting systems equipped with Arc Voltage Control (AVC) has addressed the inherent challenges of large-scale structural fabrication. By eliminating manual layout and handheld cutting, these centers provide a closed-loop system where geometry and thermal output are synchronized. This analysis focuses on the technical superiority of plasma-based intersection cutting and the mechanical reliability of AVC systems in a high-throughput environment.
The Role of Arc Voltage Control in Precision Processing
In an ideal manufacturing environment, structural steel would be perfectly flat and square. However, mill tolerances for large H-beams often include slight bows, cambers, or flange tilts. When a plasma torch moves along a programmed path, any deviation in the distance between the torch tip and the workpiece—known as the standoff distance—drastically affects the kerf width and the angle of the cut.
Arc Voltage Control functions by measuring the electrical potential between the plasma electrode and the steel beam. Because the voltage of the plasma arc is directly proportional to its length, the AVC system can detect minute changes in distance in real-time. If the flange of an H-beam rises by 2mm due to a mill warp, the AVC system senses the drop in voltage and instantly adjusts the Z-axis motor to maintain the programmed standoff. This constant feedback loop is critical for LNG Projects where even a 1-degree deviation in cut angle can lead to significant gaps during assembly, requiring costly rework or excessive filler metal.
Intersection Accuracy and 3D Geometry Challenges
The complexity of LNG modular frames often requires “saddle cuts” and intricate “cope” geometries where one beam intersects another at a compound angle. Achieving Plasma Cutting Accuracy in these three-dimensional intersections requires advanced motion control. The Beam Processing Center coordinates the rotation of the beam (or the torch) with longitudinal and vertical movement.
When processing the web and flanges of an H-beam, the plasma torch must transition through the “k-zone”—the area where the flange and web meet. This area is typically thicker and contains residual stresses from the rolling process. A high-performance plasma system utilizes specialized nesting software to calculate the exact entry and exit points for the arc. By maintaining a stable arc through AVC, the system ensures that the cut remains perpendicular (or at the specified bevel angle) regardless of the material thickness variations found at the intersection points. This level of accuracy ensures that when modules are lifted into place at the LNG site, the fit-up is seamless, reducing the need for field corrections.
Advanced Beveling for Structural Weld Preparation
For LNG structural components, simple square cuts are rarely sufficient. Most connections require V, Y, or K-style bevels to allow for full-penetration welds, which are necessary to withstand seismic loads and thermal expansion/contraction. The integration of a multi-axis robotic head or a tilting torch carrier allows the Beam Processing Center to perform beveling in a single pass.
Traditional mechanical beveling is time-consuming and often requires secondary handling. Plasma beveling within the automated center utilizes the AVC to ensure that the bevel angle remains consistent even as the torch tilts. This is particularly difficult on the flanges of H-beams, where the surface may not be perfectly horizontal. The AVC system compensates for the “apparent” change in voltage caused by the tilt, maintaining the precise depth of the land and the angle of the bevel. This consistency is a prerequisite for passing non-destructive testing (NDT) in high-pressure LNG environments.
H-Beam Low Maintenance and Operational Reliability
From a maintenance engineering perspective, the plasma-based beam center offers significant advantages over mechanical drilling or sawing lines. Plasma cutting is a non-contact process. There is no tool pressure exerted on the beam, which reduces the wear and tear on the machine’s structural frame and drive motors.
The maintenance cycle of a plasma system is primarily centered on consumables—nozzles, electrodes, and swirl rings. These components can be replaced in minutes, ensuring that the machine’s “uptime” remains above 90% even during double-shift operations. Furthermore, because there are no heavy drill bits to sharpen or saw blades to replace, the logistical footprint of the machine is much smaller. In the context of large-scale LNG projects, where the fabrication yard may be located in a remote area, the simplicity of maintaining a plasma system is a vital operational safeguard. The lack of complex mechanical lubrication systems and hydraulic tool changers further contributes to the long-term reliability of the equipment.
Thermal Management and Material Integrity
A common concern in structural engineering is the Heat Affected Zone (HAZ) created by thermal cutting. Modern high-definition plasma systems used in beam processing minimize the HAZ by utilizing high gas pressures and narrowed arc diameters. This results in a faster cutting speed, which reduces the total heat input into the steel. For the carbon steels and low-alloy steels used in LNG supports, the narrow HAZ produced by an AVC-controlled plasma torch is well within the acceptable limits defined by AWS (American Welding Society) and AISC (American Institute of Steel Construction).
The precision of the AVC also prevents “dross” or slag buildup on the underside of the cut. By keeping the arc at the optimal height, the system ensures that the molten metal is efficiently blown through the kerf. This produces a clean edge that requires little to no grinding before the next stage of fabrication.
Conclusion: Engineering Efficiency through Automation
The deployment of a Beam Processing Center with Arc Voltage Control provides a definitive technical advantage for LNG project fabrication. By prioritizing plasma cutting accuracy and beveling consistency, engineers can ensure that the structural backbone of the facility meets the highest safety and performance standards. The combination of real-time height adjustment via AVC and the low maintenance requirements of the plasma process creates a robust production environment capable of meeting the rigorous timelines and quality benchmarks of the global energy sector. In an industry where precision is non-negotiable, the automation of beam processing is no longer an option but a structural necessity.