Beam Processing Center with Arc Voltage Control for for Wind Tower fabrication
In this article
Advancing Wind Tower Structural Integrity via Automated Beam Processing
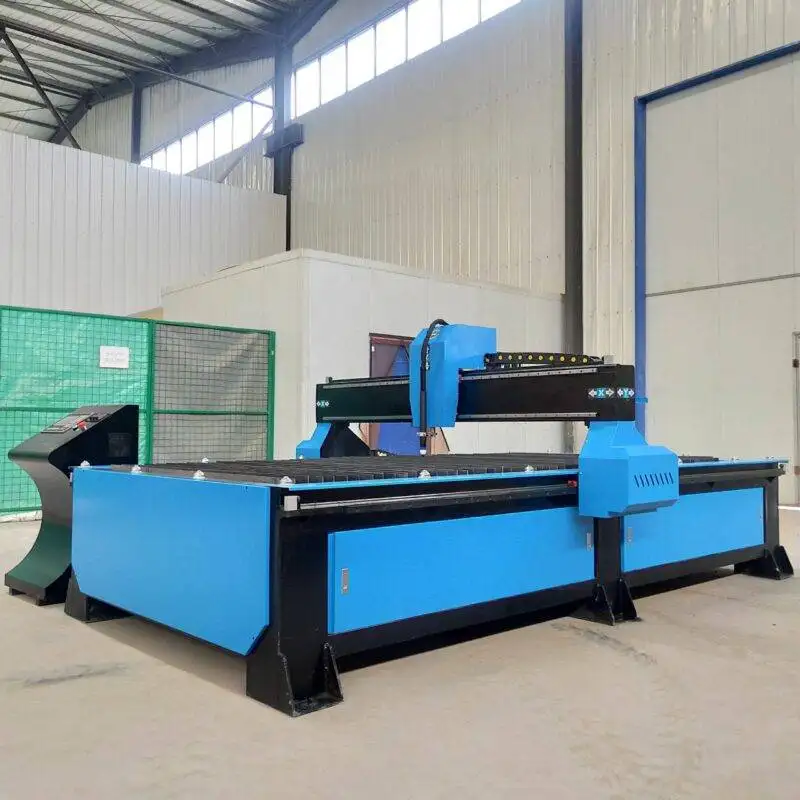
The fabrication of wind tower internal structures—specifically the platforms, ladders, and reinforcement frames—requires a level of geometric precision that traditional manual layout cannot sustain at scale. As tower diameters increase to support larger turbines, the structural components, often comprised of heavy H-beams and channels, must interface perfectly with the curved interior walls of the tower sections. A Beam Processing Center equipped with advanced plasma technology has become the industrial standard for managing these complex requirements, offering a blend of speed, adaptability, and high-tolerance output.
The shift toward automated plasma systems in this sector is driven by the need for repeatability. In wind energy logistics, every millimeter of deviation in an internal support beam can lead to cascading failures during field assembly. By utilizing 3D Plasma Cutting heads, manufacturers can execute complex cope cuts, bolt holes, and flange thinning in a single pass, ensuring that the structural framework supports the massive dynamic loads experienced by the tower during operation.
The Role of Arc Voltage Control in Precision Cutting
In the context of heavy structural steel, material flatness is rarely perfect. H-beams and plates often exhibit slight bows, twists, or surface irregularities resulting from the hot-rolling process or storage. Arc Voltage Control (AVC) acts as the critical sensory feedback loop that maintains the quality of the plasma arc despite these physical variations. AVC technology works by measuring the electrical potential between the plasma torch electrode and the workpiece.
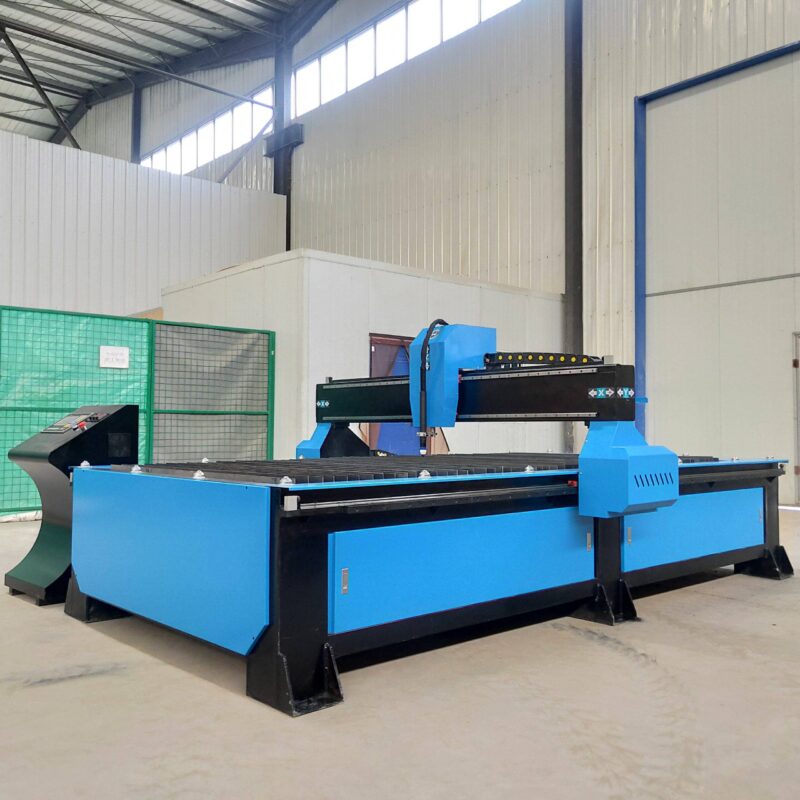
As the distance between the torch and the beam changes due to material warping, the voltage of the arc fluctuates. The AVC system samples this voltage at high frequencies—often thousands of times per second—and communicates with the Z-axis drive to adjust the torch height instantaneously. This constant height maintenance ensures a stable kerf width and prevents the torch from “diving” into the material or pulling too far away, which would otherwise result in excessive dross or a lost arc. For wind tower internals, where long H-beams are processed, AVC is the primary safeguard against consumable damage and part rejection.
Achieving Superior Intersection Accuracy for Cylindrical Fit-Up
One of the most significant challenges in wind tower fabrication is the intersection of linear structural members with the radial profile of the tower shell. A standard square cut on an H-beam is insufficient for a flush fit against a curved surface. This necessitates complex “fish-mouth” or contoured cuts that mirror the tower’s internal radius. Intersection Accuracy is the metric by which these systems are judged.
Modern beam processing centers utilize 6-axis robotic arms or specialized 3D tilting heads to navigate the flange and web of the beam. By integrating CAD/CAM data directly into the controller, the plasma torch follows a calculated path that accounts for the beam’s dimensions and the specific curvature of the tower section it will inhabit. The result is a seamless interface that minimizes gaps. This precision is vital because large gaps require excessive filler metal and increase the risk of heat-induced distortion during the final assembly phases. High intersection accuracy effectively reduces the secondary grinding and fitting labor that typically bottlenecks wind tower production lines.
Plasma Beveling: Optimizing Weld Preparation
Wind tower components are subjected to extreme fatigue cycles. Consequently, the welds connecting internal beams to the shell must be of the highest quality, often requiring full or partial penetration joints. Plasma Beveling allows the beam processing center to create V, Y, X, and K-shaped bevels during the initial cutting phase. Unlike mechanical milling, which is slow and limited to straight edges, a multi-axis plasma head can create a beveled edge on a contoured cut in a single motion.
The ability to bevel the web and flanges of an H-beam simultaneously is a force multiplier for productivity. The plasma arc provides a concentrated heat source that produces a clean, weld-ready edge with a minimal heat-affected zone (HAZ). For the heavy-wall sections common in offshore wind applications, the efficiency of plasma beveling eliminates the need for manual torch work, which is prone to human error and inconsistency. By automating the beveling process, the engineer ensures that every joint meets the stringent welding procedure specifications (WPS) required for renewable energy infrastructure.
Low Maintenance Advantages of H-Beam Plasma Systems
From an operational standpoint, the maintenance profile of a beam processing line is a major factor in total cost of ownership. Mechanical processing centers that rely on drilling, sawing, or milling involve significant “tooling” costs and frequent downtime for bit replacement and lubrication management. In contrast, plasma-based H-beam lines are inherently low maintenance. Because plasma is a non-contact thermal process, there is no mechanical force exerted on the machine frame or the cutting head.
The primary wear items in a plasma system are the electrodes and nozzles, which are inexpensive and can be replaced in minutes. Modern AVC systems further extend consumable life by preventing accidental collisions between the torch and the workpiece. Furthermore, because there are no heavy spindles or coolant systems required for the cutting process, the overall mechanical complexity of the machine is reduced. This leads to higher uptime and a simpler preventative maintenance schedule, which is essential for facilities operating 24/7 to meet global wind energy demands.
Strategic Integration and Industrial Efficiency
Integrating a beam processing center with AVC into a wind tower facility transforms the workflow from a series of disconnected tasks into a continuous manufacturing stream. The software ecosystem surrounding these machines allows for “nesting” of parts, which optimizes material utilization and reduces the scrap rate of expensive H-beam sections. As the industry moves toward larger, more complex tower designs, the reliance on high-speed plasma cutting will only intensify.
In conclusion, the application of plasma cutting technology—buttressed by Arc Voltage Control—provides the precision, versatility, and reliability required for wind tower structural components. By focusing on the mechanical advantages of 3D motion for intersection accuracy and the streamlined nature of plasma beveling, industrial engineers can significantly enhance throughput while maintaining the rigorous safety and quality standards essential for the next generation of wind energy infrastructure. The absence of heavy mechanical contact and the inclusion of intelligent height control make these systems the most resilient choice for modern structural steel fabrication.






