Beam Processing Center with Narrow Gap welding for for Wind Tower fabrication
In this article
Optimizing Structural Integrity in Wind Tower Fabrication
The manufacturing of wind towers requires a sophisticated approach to structural engineering, where the demand for height and load-bearing capacity increases with every generation of turbine. Central to this process is the Beam Processing Center, a dedicated automated system designed to handle the massive H-beams and structural profiles that form the internal frameworks and secondary supports of the tower. For engineers, the primary objective is ensuring that these components meet stringent tolerances to facilitate advanced joining techniques such as Narrow Gap Welding. Unlike traditional welding methods, narrow gap processes require highly specific joint geometries that can only be achieved through precision thermal cutting.
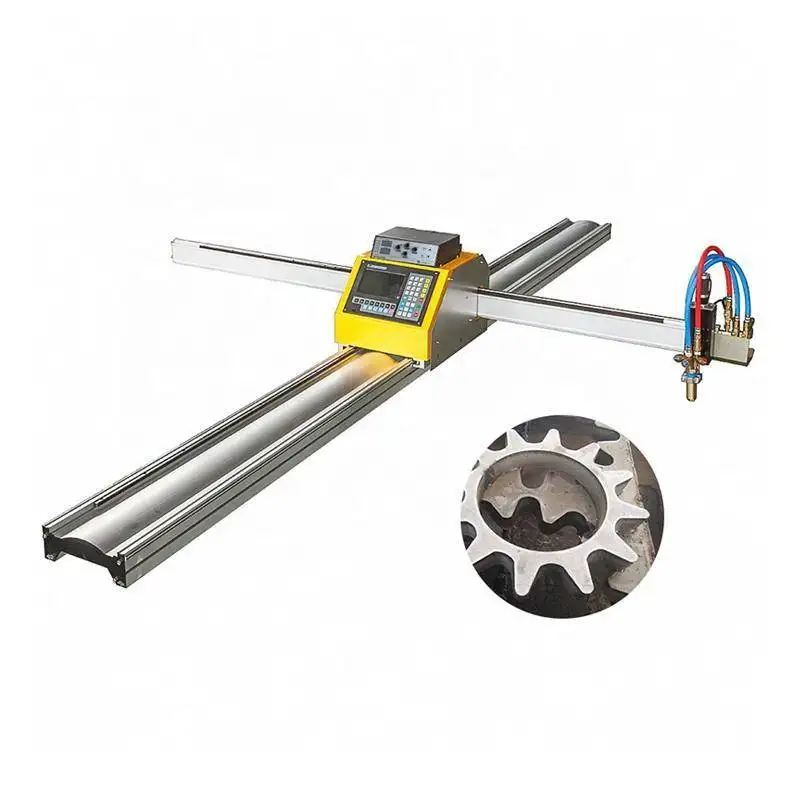
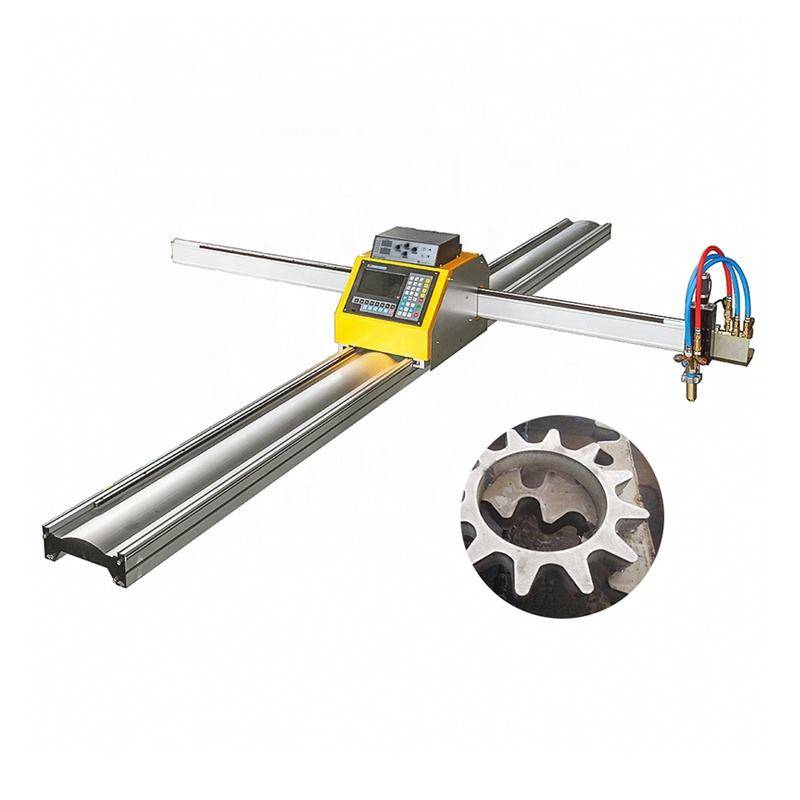
The shift toward Wind Tower Fabrication at scale necessitates a departure from manual layout and cutting. A beam processing center utilizes multi-axis plasma systems to execute complex geometries on structural steel. By automating the material handling and cutting phases, manufacturers eliminate the variability inherent in manual operations. This precision is not merely a matter of aesthetic quality; it is a prerequisite for the mechanical performance of the tower under cyclic loading and extreme environmental stress.
Precision Plasma Cutting and Intersection Accuracy
One of the most critical aspects of beam processing is Intersection Accuracy. In wind tower internals, beams often intersect at oblique angles or meet curved surfaces of the tower shell. Achieving a flush fit-up is essential for maintaining the structural load path. Plasma cutting technology, specifically when integrated into a 5-axis or 6-axis robotic gantry, allows for the dynamic adjustment of the torch angle in real-time. This capability ensures that the cut path accounts for the radius of the beam’s web and the flange thickness simultaneously.
From an industrial engineering perspective, intersection accuracy reduces the “gap volume” that must be filled during the welding phase. When the fit-up is precise, the amount of weld metal required is minimized, which in turn reduces the total heat input into the structural member. This management of the Heat Affected Zone (HAZ) is vital for preserving the metallurgical properties of the high-strength steel typically used in wind energy applications. High-definition plasma systems utilize sophisticated software algorithms to compensate for kerf width, ensuring that the final dimensions of the processed beam match the BIM (Building Information Modeling) data with sub-millimeter precision.
H-Beam Processing with Low Maintenance Requirements
Operational uptime is a key performance indicator (KPI) in any high-volume fabrication facility. Traditional mechanical cutting or older thermal methods often require significant downtime for blade replacement or nozzle cleaning. Modern Plasma Cutting units integrated into beam centers are engineered for high duty cycles with minimal intervention. The H-beam processing environment is inherently harsh, characterized by heavy slag and metallic dust. However, advanced beam centers utilize integrated downdraft tables and slag extraction systems to protect the mechanical components of the machine.
Low maintenance is achieved through the use of long-life consumables and automated torch height control (THC). By maintaining an optimal distance between the plasma electrode and the workpiece, the system prevents “torch crashes” and extends the lifespan of the nozzle and shield. Furthermore, the absence of complex mechanical saws or high-wear abrasive tools means the primary maintenance routine is limited to routine cleaning and the replacement of standardized consumables. This reliability ensures that the beam processing center remains the heartbeat of the production line, providing a steady flow of prepared components to the assembly and welding stations.
Advanced Beveling for Narrow Gap Welding Preparation
The move toward thicker structural sections in offshore wind towers has made Narrow Gap Welding the preferred method for high-efficiency joining. However, the success of NGW is entirely dependent on the quality of the edge preparation. Plasma beveling is the only cost-effective method capable of producing the steep, deep-V or U-groove profiles required for these joints on H-beams. The beam processing center must be capable of executing multi-pass bevels or single-pass compound bevels on both the flanges and the web.
During the beveling process, the plasma torch maintains a consistent angle to create a sharp, clean edge that facilitates deep penetration. Because NGW utilizes a restricted groove width—often less than 10 degrees—the consistency of the bevel angle across the entire length of the beam is paramount. Any deviation in the bevel angle can lead to lack of fusion or slag inclusion during the welding process. By utilizing automated plasma beveling, the fabricator ensures that the root face and the groove angle are perfectly uniform, regardless of the beam’s inherent camber or sweep.
Enhancing Throughput through Automated Workflows
The integration of a beam processing center into the wider wind tower production facility streamlines the transition from raw material to finished sub-assembly. The workflow begins with the loading of H-beams onto a motorized conveyor system, where sensors detect the leading edge and cross-sectional dimensions. The control system then maps the cutting program onto the physical beam, accounting for any mill tolerances or slight deformations in the steel.
Once the plasma cutting cycle begins, the machine executes all necessary bolt holes, copes, and bevels in a single setup. This “one-pass” philosophy is central to industrial efficiency. By eliminating the need to move the beam between separate stations for drilling, sawing, and beveling, the risk of material handling damage is reduced, and the floor space required for work-in-progress (WIP) is significantly minimized. The output is a component ready for immediate fit-up, where the intersection accuracy allows for rapid tack welding and transition to the Narrow Gap Welding station.
Thermal Management and Material Integrity
A common concern in thermal cutting is the introduction of residual stress. Modern high-definition plasma systems mitigate this through high cutting speeds and concentrated arc density. By increasing the travel speed, the total energy delivered to the beam is localized, resulting in a narrow HAZ. For wind tower components, which are subject to high fatigue, maintaining the base metal’s ductility is non-negotiable. The precision control of the plasma arc ensures that the metallurgical transformation at the cut edge is minimal, often requiring only light grinding before the welding process commences.
Furthermore, the software governing the beam processing center can optimize the cutting sequence to distribute heat evenly across the profile. This prevent lateral warping, ensuring that long H-beams remain straight and true after the cutting process is complete. This level of thermal management is essential when preparing components for the tight tolerances of automated narrow gap systems, where even a slight bow in the beam can interfere with the welding head’s tracking sensor.
Conclusion on Technical Integration
The synergy between automated plasma cutting and Narrow Gap Welding represents the pinnacle of modern wind tower fabrication. By focusing on the mechanical advantages of beam processing centers—specifically their ability to deliver superior intersection accuracy and precise beveling—manufacturers can overcome the challenges of thick-material fabrication. The low maintenance profile of plasma systems further ensures that the facility can meet the aggressive delivery schedules required by the global renewable energy market. As tower heights continue to climb, the reliance on these automated, high-precision processing centers will only increase, cementing plasma technology’s role as the primary catalyst for structural steel efficiency.






