Beam Processing Center with Narrow Gap welding for for Steel Structure
In this article
Engineering Efficiency in Beam Processing Centers
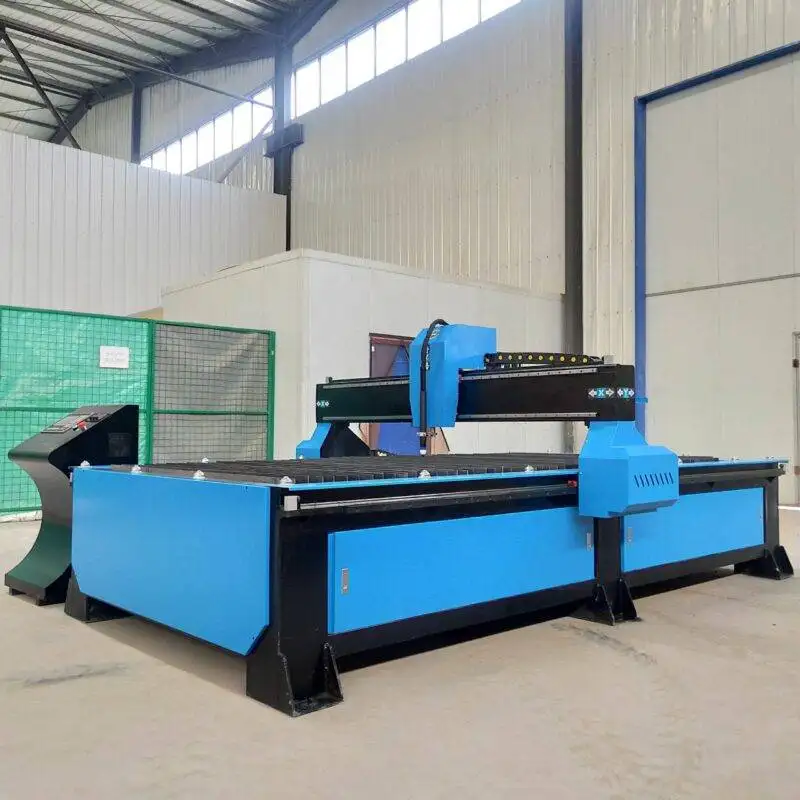
In the sector of heavy structural steel fabrication, the transition from manual layout and cutting to automated plasma profiling marks a significant shift in operational throughput. A Beam Processing Center (BPC) serves as the primary node for transforming raw H-beams, channels, and hollow sections into ready-to-assemble structural components. The engineering objective is to eliminate bottleneck stages in the workshop by consolidating marking, cutting, and beveling into a single CNC-driven workflow. By focusing on plasma technology, engineers can leverage high-energy density arcs to penetrate thick-walled sections with speeds that manual oxygen-fuel systems cannot match.
Intersection Accuracy and Multi-Axis Plasma Profiling
The core requirement for modern steel structures, particularly in high-rise or seismic-resistant frames, is the precision of complex intersections. Whether dealing with pipe-to-beam junctions or web-penetrating utility openings, intersection accuracy determines the ease of fit-up during site erection. Industrial-grade beam processing centers utilize 5-axis or 6-axis robotic gantries to manipulate the plasma torch around the workpiece.
This multi-axis movement allows for real-time compensation of beam camber and sweep. By integrating laser or mechanical probing systems prior to the cut, the CNC controller adjusts the toolpath to match the actual dimensions of the H-beam rather than the theoretical CAD model. This ensures that copes, blocks, and bolt holes are positioned with sub-millimeter tolerances, reducing the need for field adjustments. High-definition plasma power sources further refine this process by providing a constricted arc that minimizes the kerf width and reduces the heat-affected zone (HAZ), preserving the metallurgical properties of the ASTM A36 or A992 structural steel.
Low Maintenance Requirements for H-Beam Production Lines
From an industrial maintenance perspective, the longevity of a beam processing center is predicated on its ability to withstand the harsh environment of a steel mill. Unlike more delicate optical systems, Plasma Cutting hardware is inherently robust. The primary maintenance focus in an H-beam low maintenance configuration revolves around the consumable life of the torch and the mechanical stability of the drive system.
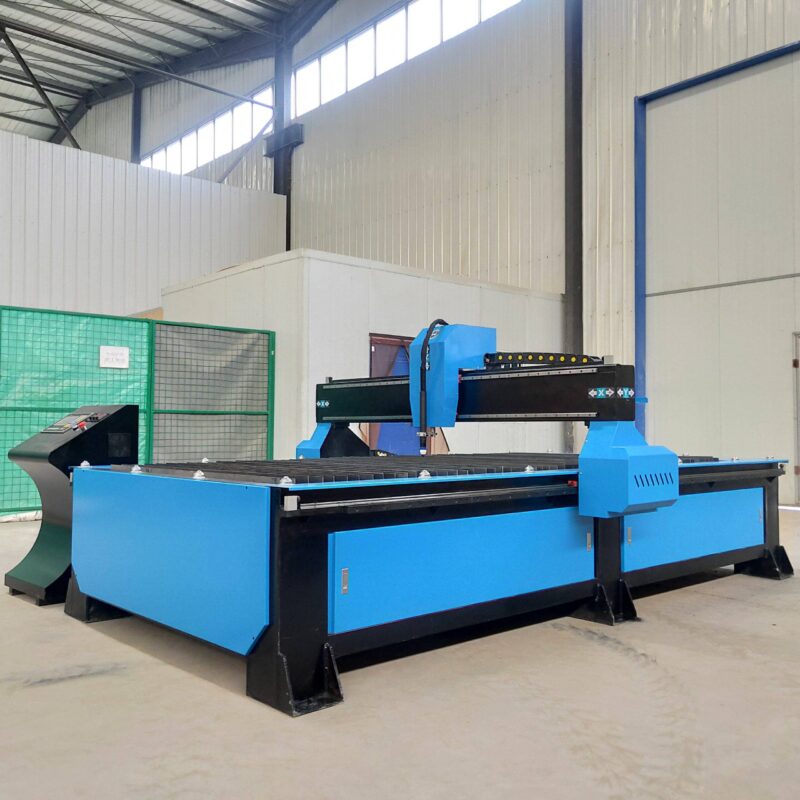
Advanced BPC designs utilize rack-and-pinion drives with pressurized enclosures to prevent the ingress of metallic dust and slag. Since plasma cutting generates significant particulate matter, integrated downdraft tables or water-injection systems are critical. By managing dross through optimized gas flow and torch height control (THC), the machine reduces the mechanical wear on the z-axis drive. Furthermore, modern plasma systems feature “quick-change” torch heads and long-life electrodes that can sustain several hundred pierces before requiring operator intervention. This high duty cycle is essential for maintaining a continuous flow in high-volume fabrication shops.
Plasma Beveling for Narrow Gap Welding Preparation
The shift toward narrow gap welding preparation represents a strategic move to reduce the volume of weld metal required for full-penetration joints. In thick-section H-beams, traditional wide-angle V-grooves require excessive passes, leading to increased thermal distortion and consumable costs. Plasma beveling units integrated into the beam processing center allow for the creation of steep-angle bevels (ranging from 3 to 10 degrees) with high repeatability.
To achieve a successful narrow gap preparation, the plasma torch must maintain a consistent standoff distance and angle relative to the flange or web surface. The BPC achieves this through sophisticated kinematic algorithms that coordinate the motion of the robotic arm with the rotation of the beam. This precise geometry is vital for narrow gap techniques, as even minor deviations in the root gap or face angle can lead to lack-of-fusion defects. By automating this beveling process, the facility ensures that the joint geometry is optimized for high-deposition welding processes, significantly shortening the overall fabrication timeline.
Thermal Management and Kerf Compensation
One of the technical challenges in plasma cutting is managing the thermal expansion of the steel beam during long cuts. Industrial engineers address this by implementing intelligent nesting and sequencing software. The software calculates the heat input and staggers the cutting path to allow for localized cooling, preventing the beam from warping.
Kerf compensation is another critical factor. As the plasma arc is essentially a pressurized column of ionized gas, it naturally tapers. High-definition plasma systems compensate for this by tilting the torch slightly to ensure that the finished edge is perfectly square where required, or at the exact specified angle for a weld prep. This level of control is fundamental when preparing beams for narrow gap welding, where the margin for error in the joint fit-up is extremely slim.
Robotic Integration and Structural Integrity
The integration of robotics within the beam processing center allows for “all-in-one” processing. A beam can be loaded onto the conveyor, scanned for dimensions, and then processed on all four sides without manual flipping. This reduces the risk of mechanical damage to the beam flanges and maintains the integrity of the protective mill scale where cutting is not required.
For the structural engineer, the use of automated plasma cutting ensures that the structural integrity of the member is not compromised by irregular hand-cut notches or gouges. Smooth transitions in copes and radii are essential for fatigue resistance in bridges and industrial cranes. The CNC-controlled plasma arc provides a surface finish that often negates the need for secondary grinding, moving the component directly from the cutting cell to the welding station.
Optimizing Throughput and Return on Investment
The financial justification for a beam processing center with narrow gap beveling capabilities is found in the reduction of “man-hours per ton.” By automating the structural steel throughput, a facility can handle larger contracts with a smaller footprint. The precision of the plasma-cut bevels leads to a direct reduction in the amount of weld wire consumed and the energy required for pre-heating and welding.
Furthermore, the reliability of plasma systems in a 24/7 production environment ensures that the machine remains an asset rather than a maintenance liability. By focusing on the mechanical robustness of the H-beam line and the accuracy of the multi-axis profiling, fabricators can achieve a level of consistency that is unattainable through manual methods. This technical synergy between plasma profiling and narrow gap welding preparation defines the current state of the art in steel structure manufacturing.





