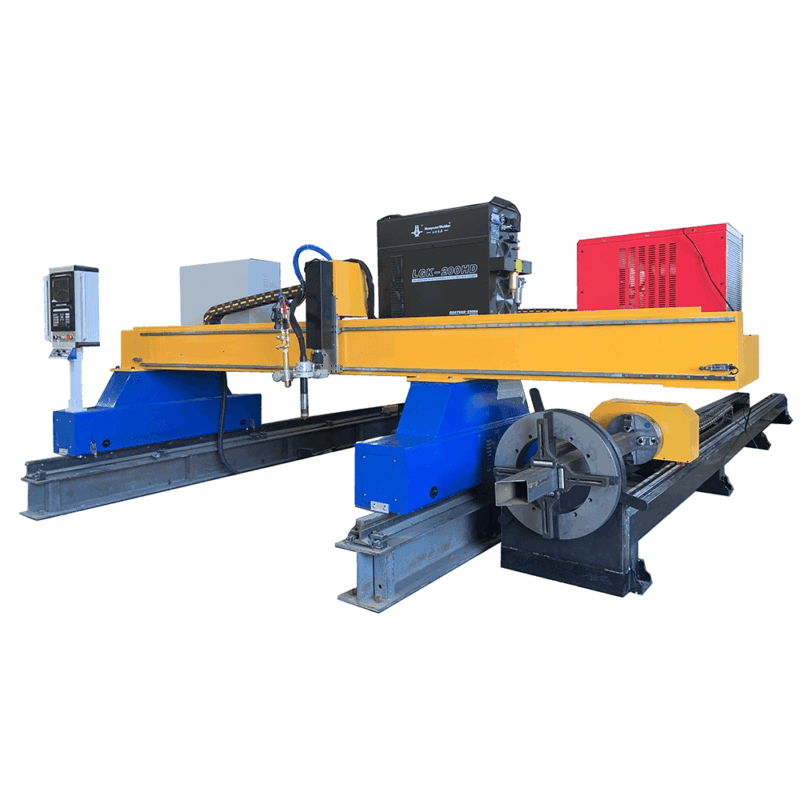
Beam Processing Center with Arc Voltage Control for for Bridge Trusses
In this article
- Precision Engineering in Bridge Truss Fabrication
- The Role of Arc Voltage Control (AVC) in Thermal Cutting
- Achieving Superior Intersection Accuracy
- Optimizing Nodal Geometry
- H-Beam Processing and Low Maintenance Requirements
- Advanced Plasma Beveling for Weld Preparation
- Streamlining Throughput in the Fabrication Shop
- Conclusion
Precision Engineering in Bridge Truss Fabrication
The fabrication of bridge trusses demands a level of structural accuracy that exceeds standard commercial steel building requirements. Bridge components are subjected to dynamic loading, thermal expansion, and rigorous fatigue cycles, necessitating near-perfect fit-up at nodal points. A Beam Processing Center equipped with advanced plasma technology serves as the primary engine for this precision. Unlike traditional mechanical methods, modern plasma systems utilize Arc Voltage Control to maintain a constant distance between the torch tip and the workpiece, ensuring that the thermal energy is applied consistently across varying flange thicknesses and web depths.
In the context of H-beam processing, the primary challenge lies in the inherent inconsistencies of hot-rolled steel. Mill tolerances often result in slight deviations in flange parallelism or web centering. An automated beam processing center compensates for these variances by utilizing touch-sensing and real-time feedback loops. This capability is critical when preparing complex truss geometries where multiple members converge at a single point, requiring precise copes and miters to ensure load paths are correctly aligned according to the structural engineer’s specifications.
The Role of Arc Voltage Control (AVC) in Thermal Cutting
Arc Voltage Control is the cornerstone of high-definition Plasma Cutting in structural steel applications. The system functions by measuring the electrical potential between the plasma electrode and the steel beam. As the physical distance between the torch and the material changes due to beam camber or flange warping, the voltage fluctuates. The CNC controller interprets these fluctuations and adjusts the Z-axis position instantaneously to maintain the programmed standoff distance.
for Bridge Trusses, where material thickness can vary significantly between the web and the flange of a heavy W-shape or H-beam, AVC ensures the plasma arc remains in its most stable and concentrated state. This stability is vital for achieving a narrow kerf and minimizing the heat-affected zone (HAZ). By maintaining the optimal focal point of the plasma jet, the system eliminates “dross” or slag buildup on the underside of the cut, which significantly reduces the labor required for secondary grinding operations.
Achieving Superior Intersection Accuracy
The structural integrity of a bridge truss is heavily dependent on Intersection Accuracy. When diagonal and vertical members are joined to the top and bottom chords, the geometry of the cuts must account for the 3D profile of the receiving member. Plasma-based beam processing centers utilize multi-axis robotic arms or specialized 6-axis gantries to execute these complex volumetric cuts.
Traditional sawing and drilling lines often struggle with complex intersections, particularly when “bird-mouth” cuts or complex copes are required for tubular or H-beam intersections. A plasma system, however, can navigate the internal corners of a flange-web junction with high velocity and directional precision. This allows for a “tight fit” assembly. When the fit-up is accurate to within fractions of a millimeter, the subsequent welding process becomes more predictable, with reduced risk of distortion and a more uniform distribution of stress across the joint.
Optimizing Nodal Geometry
In bridge engineering, the “node” is the point where forces are transferred. If the plasma cut is inaccurate, the resulting gap must be filled with weld metal, which introduces unnecessary heat and potential points of failure. The Beam Processing Center uses sophisticated nesting and CAD/CAM integration to translate 3D models into precise cutting paths. This ensures that every mitered edge and bolt hole aligns perfectly during field erection, drastically reducing the need for “forcing” connections on-site.
H-Beam Processing and Low Maintenance Requirements
From an industrial engineering perspective, the Total Cost of Ownership (TCO) is a critical metric for any fabrication facility. One of the standout advantages of plasma-based beam centers is their H-beam low maintenance profile compared to mechanical cutting alternatives. Mechanical systems, such as circular saws or band saws, rely on physical contact, leading to tool wear, blade breakage, and the constant need for lubrication and cooling fluids.
Plasma cutting is a non-contact process. There is no mechanical force exerted on the beam, which means the machine structure is not subjected to the vibration and stress associated with high-speed sawing. The primary consumables—electrodes and nozzles—are easily replaced and have predictable lifespans based on “arc-on” time. Furthermore, the absence of cutting fluids prevents the accumulation of “sludge” (a mixture of metal chips and oil) that typically plagues mechanical lines. This results in a cleaner work environment and reduces the downtime required for machine cleaning and preventative maintenance.
Advanced Plasma Beveling for Weld Preparation
Weld preparation is perhaps the most labor-intensive aspect of bridge truss fabrication. Standard practice involves creating V, Y, or X bevels on the edges of the steel members to allow for full-penetration welds. A Beam Processing Center equipped with a 3D plasma head automates this process entirely. Plasma Beveling allows the machine to cut the profile and the weld angle simultaneously.
Versatility in Bevel Profiles
The ability to transition from a straight 90-degree cut to a 45-degree bevel in a single continuous motion is a significant efficiency gain. For bridge trusses, where different sections of a single beam may require different weld preparations based on the stress levels at that specific location, the flexibility of a 5-axis or 6-axis plasma head is indispensable. The CNC system can vary the bevel angle dynamically along the cut path, accommodating the varying geometry of the truss nodes.
Thermal Efficiency and Edge Quality
Modern high-definition plasma power sources provide a constricted arc that delivers high energy density. This results in a cut edge that is nearly as smooth as a machined surface. For bridge components, the edge quality is vital because surface irregularities can act as stress risers, potentially leading to fatigue cracking over decades of service. The automated control of travel speed, gas pressure, and arc voltage ensures that the bevel surface meets the stringent requirements of the American State Highway and Transportation Officials (AASHTO) or similar regulatory bodies.
Streamlining Throughput in the Fabrication Shop
Efficiency in a bridge shop is measured by “tons per man-hour.” By consolidating cutting, coping, hole-making, and beveling into a single workstation, the Beam Processing Center eliminates the need for multiple material handlings. In traditional workflows, a beam might move from a saw to a drill line, and then to a manual layout station for beveling. Each move carries the risk of material damage and consumes valuable crane time.
The integration of plasma technology allows for a “raw material in, finished component out” workflow. The automated measurement systems within the center detect the actual length and orientation of the beam, adjusting the cutting program on the fly. This level of automation is particularly beneficial for bridge trusses, which often involve massive sections that are difficult to maneuver. By performing all operations in a single clamping cycle, the center ensures that the spatial relationship between holes, copes, and bevels remains perfectly consistent, adhering to the tight tolerances required for infrastructure projects.
Conclusion
The implementation of a Beam Processing Center with Arc Voltage Control represents a significant leap forward for bridge truss manufacturers. By focusing on the precision of plasma technology, facilities can achieve superior intersection accuracy and high-quality weld preparations while benefiting from the low maintenance requirements of non-contact cutting. As bridge designs become more complex and safety standards more rigorous, the ability to produce highly accurate, beveled H-beams with minimal manual intervention becomes a decisive competitive advantage in the heavy structural steel industry.