Beam Processing Center with Arc Voltage Control for for Construction Machinery
In this article
Technical Optimization of Beam Processing in Construction Machinery
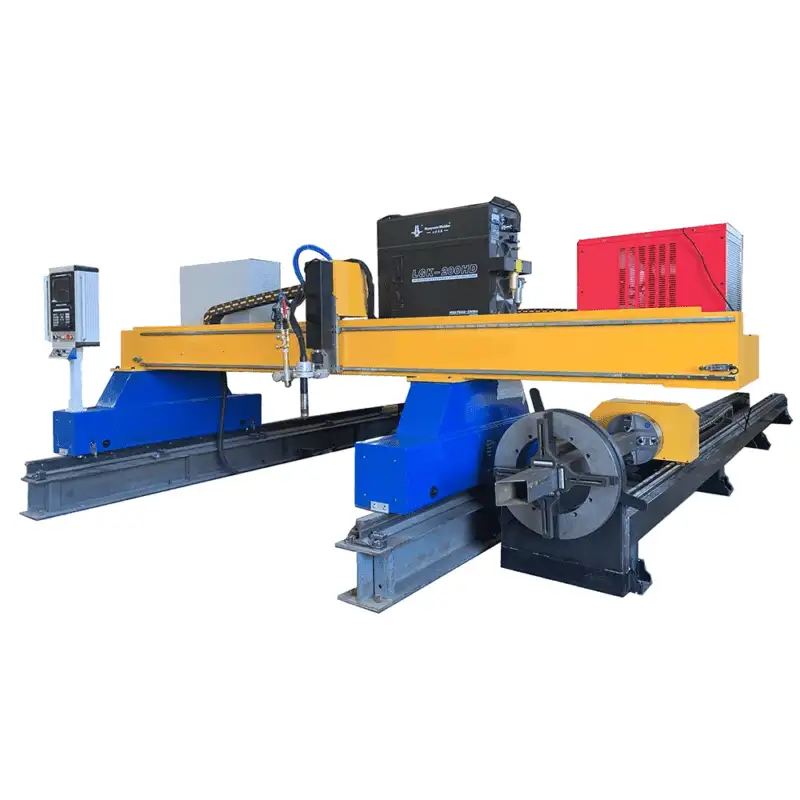
In the production of heavy-duty construction machinery—such as mobile cranes, excavators, and earthmoving chassis—structural integrity depends on the precision of H-beam and I-beam processing. These components often bear extreme dynamic loads, requiring tight tolerances and repeatable geometries. The implementation of a specialized Beam Processing Center utilizing Plasma Cutting technology has become the industry standard for achieving these requirements while maintaining high throughput. Unlike manual layouts, an automated center integrates material handling, measurement, and thermal cutting into a single CNC-controlled workflow.
The primary challenge in structural steel fabrication is the inherent variance in raw materials. Structural beams, particularly long-span H-beams, are rarely perfectly straight. They exhibit “camber,” “sweep,” and “twist” resulting from the rolling process at the mill. To compensate for these geometric deviations, industrial engineers rely on arc voltage control (AVC) systems. This technology ensures the plasma torch maintains a constant standoff distance from the workpiece, which is the foundational requirement for consistent kerf width and angular accuracy.
The Role of Arc Voltage Control in Thermal Cutting
Arc Voltage Control operates on a closed-loop feedback mechanism. During the plasma cutting process, the voltage between the electrode and the workpiece is directly proportional to the distance between the torch tip and the metal surface. As the plasma torch moves across a warped beam, the AVC system samples the arc voltage at high frequencies—often exceeding 1,000 times per second.
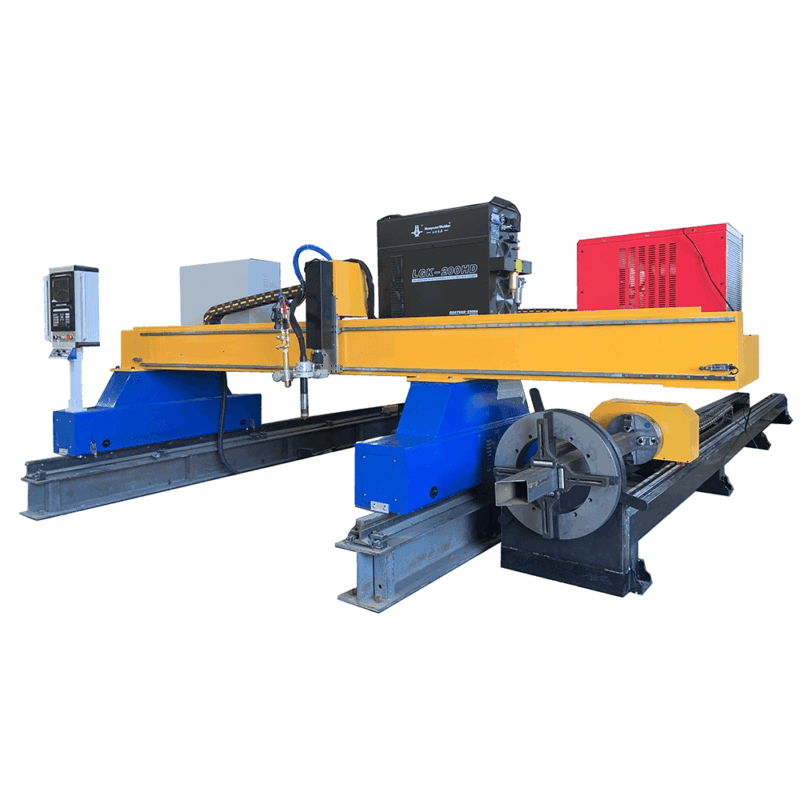
When the system detects a voltage fluctuation, it signals the Z-axis motor to adjust the torch height instantaneously. If the voltage increases, the torch is too far from the plate; if it decreases, the torch is too close. By maintaining a precise “Sweet Spot,” the system prevents dross accumulation and minimizes the Heat Affected Zone (HAZ). for Construction Machinery, where structural fatigue is a primary concern, minimizing the HAZ is critical to preventing crack initiation at the cut edges.
Enhancing Intersection Accuracy for Complex Geometries
One of the most difficult operations in beam processing is the creation of “rat holes,” cope cuts, and flange penetrations where one structural member intersects another. Intersection accuracy is paramount because gaps exceeding 2mm often require excessive filler metal, leading to distortion and increased labor costs during assembly. A beam processing center solves this through 6-axis kinematic control.
High-definition plasma units mounted on robotic or multi-axis gantry systems can navigate the web and flanges of an H-beam simultaneously. The CNC software maps the actual dimensions of the beam using laser or physical probing before the cut begins. By combining this “real-world” map with the AVC data during the cut, the machine can execute complex 3D intersections that fit together with mechanical precision. This eliminates the need for manual grinding and “make-to-fit” adjustments on the shop floor.
Low Maintenance Requirements for H-Beam Lines
From an operational expenditure (OPEX) perspective, plasma-based beam centers offer a distinct advantage in terms of durability. The environment of a structural steel plant is characterized by dust, mill scale, and temperature fluctuations. Plasma systems are inherently robust. Unlike optical-based systems that are sensitive to vibration and environmental particulates, plasma torches are designed for heavy industrial use.
The structural steel fabrication workflow benefits from the “clean-cut” nature of modern high-definition plasma. The consumables—nozzles, electrodes, and swirl rings—are the only significant wear items. Modern centers feature “quick-change” torch heads and automated consumable monitoring, which alerts operators before cut quality degrades. Furthermore, because the plasma arc can pierce through mill scale and light rust common on H-beams, the need for pre-process shot blasting is often reduced, further lowering the total cost of ownership.
Multi-Axis Beveling for Weld Preparation
In construction machinery, most joints are designed for full-penetration or partial-penetration welds. This necessitates beveling the edges of the H-beam web and flanges. Traditional methods involved manual oxy-fuel torches or portable bevellers, both of which are slow and prone to human error. An integrated beam processing center executes V, Y, X, and K-style bevels in a single pass.
The multi-axis plasma head can tilt up to 45 or 50 degrees, allowing for complex chamfering even on the interior sections of the beam. The AVC system remains active during beveling, though the voltage-to-distance ratio is adjusted to account for the angular travel of the arc. This ensures that the bevel angle remains consistent across the entire length of the cut, which is vital for automated fit-up stations. When the bevel is consistent, the volume of weld metal required is predictable, allowing engineers to optimize the welding wire consumption and cycle times.
Process Integration and Throughput Optimization
The efficiency of a beam processing center is not just in the speed of the torch (inches per minute), but in the reduction of material handling. In a traditional shop, a beam must be moved from a saw to a layout station, then to a drill line, and finally to a manual cutting area. Each move introduces potential for error and safety risks.
An automated center consolidates these steps. The beam is loaded onto a conveyor, measured for length and cross-section, and then processed. All holes, copes, slots, and bevels are completed in one setup. For construction machinery manufacturers, this transition to a single-platform solution typically results in a 40% to 60% reduction in man-hours per ton of steel. The precision of the plasma cut also ensures that downstream assembly is faster, as components align perfectly without the need for hydraulic jacks or heavy wedging.
Summary of Engineering Benefits
The transition to a beam processing center with integrated Arc Voltage Control represents a shift toward data-driven manufacturing. By prioritizing intersection accuracy and utilizing the mechanical resilience of plasma systems, manufacturers can achieve a level of structural consistency that manual methods cannot replicate. As construction machinery continues to grow in scale and complexity, the ability to produce high-tolerance, beveled structural components with low maintenance overhead will remain a core competitive advantage for industrial engineers and plant managers alike.






