H-Beam Production Line with Zero-tailing technology for Oil & Gas Tanks
In this article
Optimization of Structural Steel Fabrication for Petrochemical Storage
In the construction of large-scale oil and gas storage tanks, the structural integrity of the supporting H-beam framework is paramount. Industrial engineers are increasingly turning to a specialized H-Beam Production Line that incorporates zero-tailing technology to meet these demands. Unlike traditional fabrication methods that result in significant material scrap, modern plasma-based lines focus on maximizing material utilization while maintaining the tight geometric tolerances required for API-standard tank foundations and skid units.
The transition from manual layout and cutting to automated CNC plasma processing is driven by the need for repeatability and precision. In the oil and gas sector, where environmental factors such as seismic activity and high wind loads are critical variables, the H-beams used for tank saddles and peripheral supports must be processed with absolute consistency. The application of Plasma Cutting in this context is not merely about speed; it is about the controlled delivery of thermal energy to ensure clean edges and precise intersections.
The Mechanics of Zero-Tailing Technology
Zero-tailing technology represents a significant advancement in material handling and software integration. Traditional H-beam cutting systems often require a “clamping zone” or a minimum length of material at the end of the beam that cannot be processed due to the physical limitations of the feeding rollers or carriage. This results in a “tail” of expensive structural steel being relegated to the scrap bin.
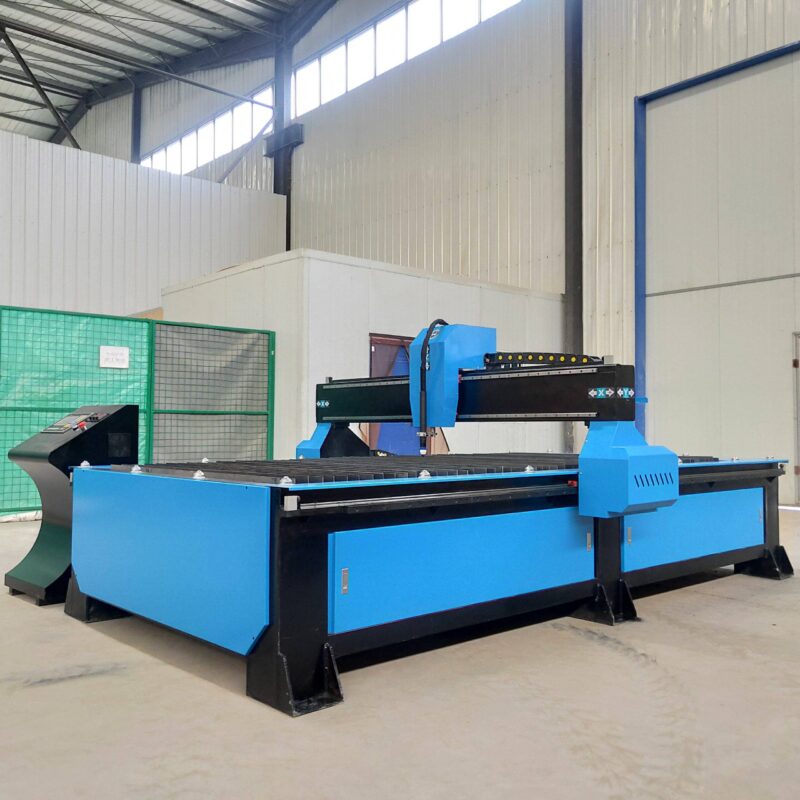
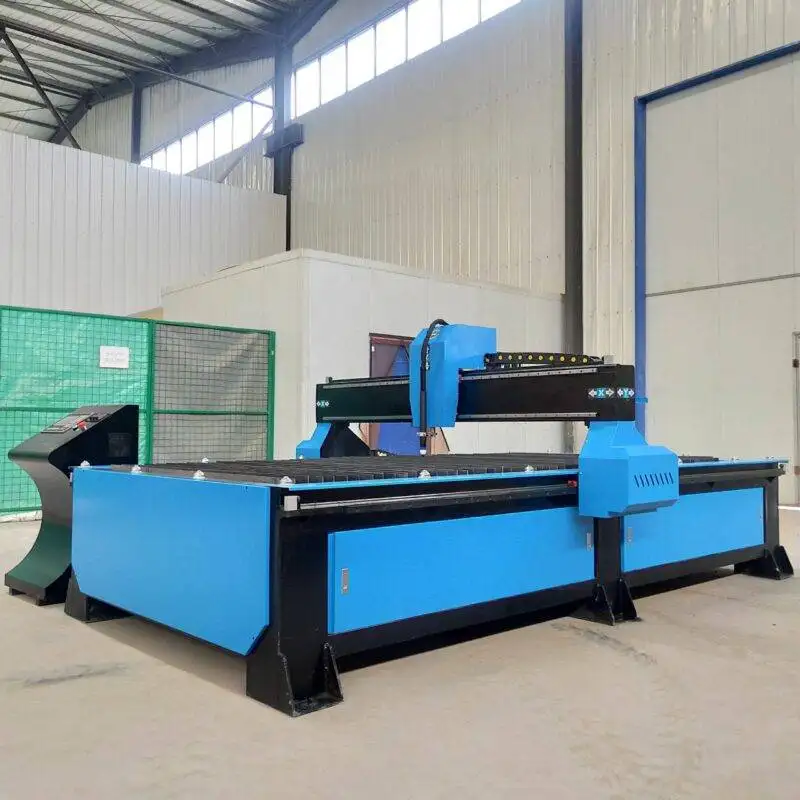
In an engineered zero-tailing technology system, the production line utilizes a dual-chuck or a specialized “pass-through” feeding mechanism. This allows the plasma torch to reach the extreme edge of the raw material. By synchronizing the CNC movement with the material displacement sensors, the system can calculate the exact position of the beam’s end, allowing the cutting head to execute the final profile or bolt hole pattern with less than 5mm of waste. For high-volume tank projects, where thousands of tons of steel are processed, the cumulative reduction in scrap leads to a direct improvement in the project’s bottom line.
Plasma Intersection Accuracy and 3D Profiling
One of the primary challenges in fabricating H-beams for tank structures is the complexity of intersections. Beams often intersect at oblique angles or require cutouts to accommodate piping and secondary bracing. Plasma intersection accuracy is achieved through the use of high-definition plasma power sources paired with 5-axis or 6-axis robotic cutting heads.
These systems utilize sophisticated algorithms to compensate for the beam’s inherent flange-to-web deviations. Structural steel is rarely perfectly straight; it possesses “rolling tolerances” such as camber and sweep. An advanced plasma line uses laser or mechanical probing to map the actual surface of the H-beam in real-time. The CNC then adjusts the torch trajectory to ensure that the intersection profile fits perfectly against the mating surface. This level of precision is critical for oil and gas tanks, where gaps in fit-up can lead to structural weaknesses or excessive weld metal volume, both of which are unacceptable in high-pressure environments.
High-Definition Beveling for Structural Integrity
The preparation of weld joints is a bottleneck in many fabrication facilities. In an H-beam production line, automated beveling integrates the weld preparation process directly into the cutting cycle. For tank support skids, full penetration or partial penetration welds are often specified. This requires the H-beam flanges and webs to be beveled at specific angles (V, Y, or K profiles).
The multi-axis plasma head can tilt up to 45 or 50 degrees, allowing it to perform bevel cuts on the fly. Because the plasma arc is a high-energy density process, it creates a narrow heat-affected zone (HAZ), which preserves the metallurgical properties of the structural steel. This is particularly important for oil and gas applications where the steel may be subject to low-temperature environments (requiring high Charpy V-notch toughness). The precision of the bevel angle ensures that when the beams are assembled on-site, the root gap is consistent, facilitating high-quality welding and reducing the likelihood of UT (ultrasonic testing) or RT (radiographic testing) failures.
H-Beam Low Maintenance Protocols and Uptime
From an industrial engineering perspective, the total cost of ownership (TCO) is a critical metric. A primary advantage of the plasma process in an H-beam line is its mechanical simplicity and robustness. H-beam low maintenance is a direct result of the design of modern plasma torches and the elimination of complex mechanical tool-changing systems found in drilling or sawing operations.
Plasma systems have fewer moving parts in contact with the workpiece. The primary wear items are consumables—nozzles and electrodes—which can be changed in seconds. Modern CNC interfaces track consumable life and alert operators before cut quality degrades, preventing scrap. Furthermore, the dust collection and filtration systems integrated into these lines are designed to handle the high volume of particulates generated by plasma cutting, protecting the linear guides and rack-and-pinion drives from abrasive wear. For a facility operating 24/7 on a major refinery project, the high uptime of a plasma-based line ensures that production schedules are met without the risk of long-term mechanical failure.
Thermal Efficiency and Material Deformation Control
When cutting heavy-section H-beams, thermal management is essential. Excessive heat input can lead to warping, which complicates the assembly of large-diameter tank supports. Plasma cutting systems utilize advanced “pulsed” technology and optimized gas flows to minimize the energy transferred to the workpiece. By increasing the cutting speed and focusing the arc, the system ensures that the majority of the heat is carried away by the kerf material and the shielding gas.
Engineering the production flow involves balancing the feed rate with the plasma power settings. For thick flanges, the line’s software automatically adjusts the torch height and the angle of attack to prevent the dross accumulation that can occur at the bottom of the cut. This results in a dross-free finish that requires little to no grinding, further reducing labor costs and secondary processing time.
Integration with Oil and Gas Digital Workflows
The modern production line does not operate in isolation. It is a node in a larger digital ecosystem. Design data from BIM (Building Information Modeling) or CAD/CAM software is exported as NC files directly to the production line. This eliminates manual data entry and the potential for human error. For oil and gas tank projects, where traceability is mandatory, the system can mark each beam with a unique identification number or barcode using the plasma torch at a low-power setting. This ensures that every component is tracked from the raw material stage through to final installation on the tank farm.
In conclusion, the deployment of an H-beam production line equipped with zero-tailing plasma technology offers a comprehensive solution for the demanding requirements of oil and gas infrastructure. By focusing on intersection accuracy, automated beveling, and a low-maintenance operational model, industrial facilities can achieve a higher level of throughput and structural reliability. The reduction of waste and the precision of the final product are not just operational improvements; they are competitive advantages in a global market that demands efficiency and safety above all else.






