Optimizing Wind Tower Fabrication via Plasma Cutting Systems
Industrial engineering in the renewable energy sector requires a rigorous focus on material throughput and structural integrity. Wind tower production involves the processing of massive cylindrical sections and internal structural supports that must withstand extreme fatigue loads. The integration of Plasma Cutting Machine technology equipped with zero-tailing capabilities represents a significant shift in how manufacturers approach raw material utilization. Unlike traditional mechanical cutting, modern high-definition plasma systems offer the thermal capacity required to penetrate thick-walled carbon steel while maintaining the tight tolerances necessary for automated assembly.
Zero-Tailing Technology: Material Efficiency and Economics
In the context of large-scale fabrication, material waste—specifically the unused ends of pipes or beams known as “tails”—represents a direct hit to the bottom line. Zero-tailing technology utilizes specialized dual-chuck or multi-point feeding mechanisms that allow the plasma torch to operate extremely close to the clamping zone. In standard configurations, a significant portion of the material remains held in the chuck and cannot be reached by the cutting head, leading to scrap rates that can exceed 5-8% per section.
By implementing a synchronized motion control system, the zero-tailing process enables the machine to pass the material through the secondary chuck during the final cutting phase. This ensures that the entire length of the raw stock is utilized. For wind tower internals, such as secondary platforms and ladder supports, the cumulative savings in steel costs over a single production year can offset the capital expenditure of the machinery. From an industrial engineering perspective, this reduces the “scrap-to-finished-product” ratio, streamlining the supply chain and reducing the frequency of raw material procurement.
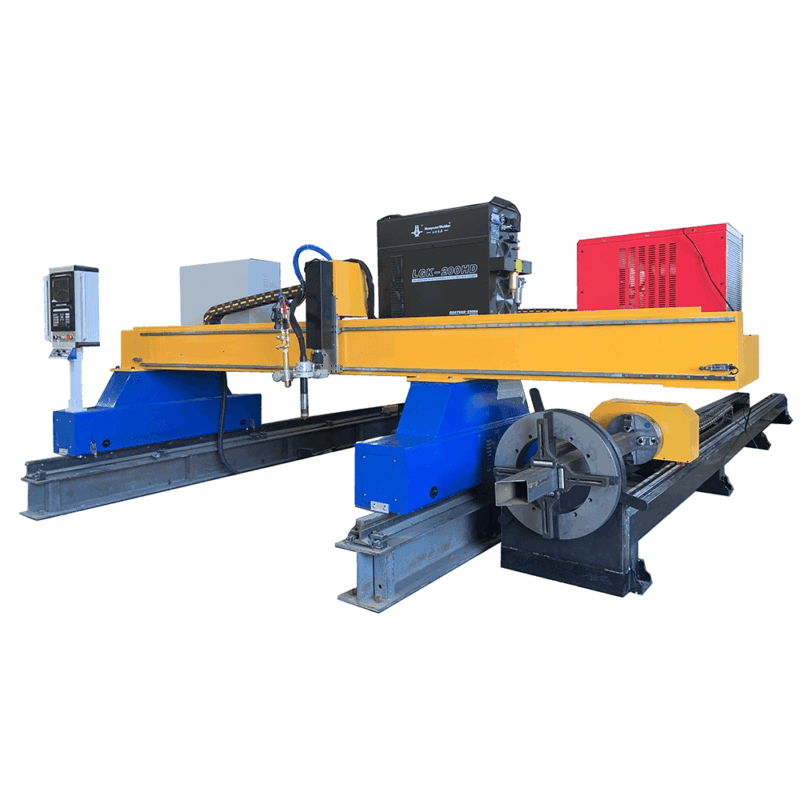
Intersection Accuracy in Tubular Structures
Wind towers are essentially massive tapered tubes that require precise openings for door frames, cable entries, and ventilation ports. The intersection accuracy of these cuts is paramount. When two curved surfaces meet, the resulting geometry is complex; any deviation leads to gaps that require excessive filler metal during the subsequent welding stages.
High-definition plasma systems utilize 5-axis or 6-axis robotic heads governed by advanced inverse kinematics. This allows the torch to maintain a perpendicular or specific beveled orientation relative to the curved surface of the tower section at all times. Intersection accuracy is maintained through real-time sensing and compensation software. By using laser-based surface mapping, the plasma system can detect slight irregularities in the roundness of the tower section and adjust the toolpath in milliseconds. This precision ensures that components fit perfectly upon first assembly, eliminating the need for manual grinding or “fit-up” corrections on the shop floor.
Maintenance Efficiency for H-Beam and Heavy Section Processing
Wind tower manufacturing facilities are harsh environments characterized by high dust levels and heavy vibrations. Equipment reliability is a core KPI for any production manager. Plasma systems designed for H-beam and heavy structural sections are engineered for high duty cycles with minimal downtime.
A key advantage of plasma technology in this sector is the low maintenance requirement of the mechanical delivery system. Unlike mechanical saws that suffer from blade wear and breakage, or more delicate thermal processes that require pristine optical paths, the plasma torch is a robust tool. The primary consumables—electrodes, nozzles, and shields—are easily replaced in minutes without requiring specialized calibration. For H-beam processing specifically, the use of rack-and-pinion drives with hardened ground rails ensures that the system can handle the mass of 30-meter structural members without losing positional accuracy over time. The absence of complex lens assemblies means the machine can operate in non-climate-controlled environments typical of large-scale heavy fabrication yards.
Advanced Beveling for Weld Preparation
Wind towers require deep penetration welds to handle the dynamic loads of the turbine nacelle and blades. Consequently, almost every cut made on the tower shell or the heavy internal flanges must be beveled. Plasma cutting excels in this area by offering integrated beveling capabilities that produce V, Y, X, and K-shaped profiles in a single pass.
Thermal Control and Edge Quality
The heat-affected zone (HAZ) is a critical consideration in wind tower engineering. Modern plasma power sources use sophisticated gas consoles to mix oxygen, nitrogen, and H35 (a hydrogen-argon blend) to produce a narrow, constricted arc. This constriction increases the energy density, allowing for faster travel speeds which, in turn, minimizes the heat input into the base metal. The result is a beveled edge with minimal dross and a metallurgical profile that meets stringent international standards for weldability.
Robotic Beveling Versatility
The flexibility of a multi-axis plasma head allows for “on-the-fly” bevel angle changes. For example, as the torch moves around a circular door cutout on a tapered tower section, the bevel angle must constantly transition to maintain the correct root gap for the door frame installation. This level of geometric complexity is handled automatically by the machine’s post-processor, converting 3D CAD models directly into optimized plasma toolpaths.
Conclusion: Engineering the Future of Wind Infrastructure
The integration of zero-tailing plasma cutting machines into wind tower production lines addresses the three most critical pillars of modern manufacturing: material conservation, geometric precision, and operational uptime. By focusing on beveling quality and intersection accuracy, manufacturers can significantly reduce the labor hours associated with post-cut processing. Furthermore, the robust nature of plasma systems ensures that these machines remain productive in the demanding conditions of a heavy steel shipyard or fabrication plant. As the height and capacity of wind turbines continue to increase, the reliance on high-precision plasma technology will only grow, cementing its role as the backbone of renewable energy infrastructure fabrication.
-


Cantilever Welding Robot solution
-


GF laser cutting machine
-

P3015 plasma cutting machine
-

LFP3015 Fiber Laser Cutter
-

pipe plasma cutting machine
-
LFH 4020 Fiber Laser Cutting Machine
-
LFP4020
-

gantry plasma air cutting machine
-

3D robot cutting machine
-

8 axis plasma cutting machine
-

5 axis plasma cutting machine
-

LT360 tube laser cutting machine
-

robot welding workstation
-

SF6060 fiber laser cutting machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.