Advancing Oil and Gas Fabrication with Zero-Tailing Plasma Technology
In the heavy industrial sector, specifically within Oil and Gas infrastructure, the precision of primary structural components determines the long-term integrity of storage tanks and pressure vessels. The transition toward high-performance Plasma Cutting systems has been driven by the need for processing thick-walled materials with extreme geometric complexity. Zero-tailing technology represents a significant leap in this domain, addressing the historical inefficiency of material waste at the end of structural profiles. By utilizing advanced clamping and modular feeding systems, industrial engineers can now ensure that the entire length of an H-beam or large-diameter pipe is utilized, significantly reducing the cost-per-part in high-volume fabrication cycles.
Kinematics of Intersection Accuracy in 3D Profiles
The structural framework of an oil storage tank often involves complex intersections between H-beams, channels, and cylindrical shells. Achieving high-level intersection accuracy is not merely a matter of aesthetic fit; it is a critical requirement for load distribution and structural safety. Plasma systems equipped with multi-axis robotic heads allow for the execution of complex saddle cuts and pipe-to-pipe intersections with tolerances exceeding standard industry benchmarks.
The accuracy is maintained through real-time feedback loops and laser-based surface sensing. Before the torch ignites, the system maps the actual dimensions of the H-beam, accounting for any mill deviations or twists in the raw material. This ensures that the intersection accuracy of the cut path is mathematically aligned with the center-line of the structural assembly. For the Oil and Gas engineer, this precision translates to a seamless fit-up during the assembly phase, eliminating the need for manual grinding or corrective filling, which are common bottlenecks in tank farm construction.
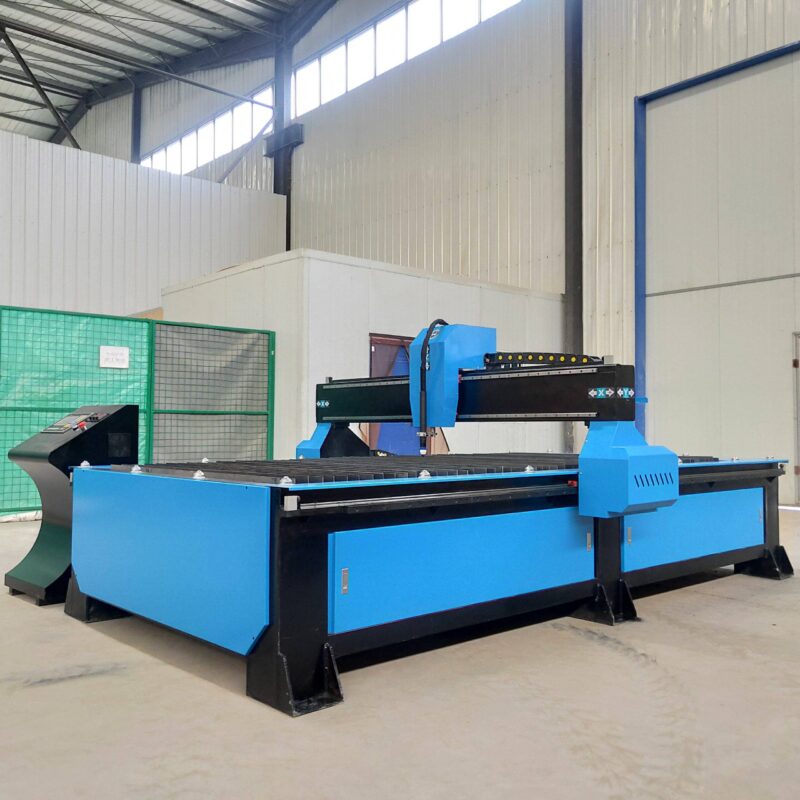
Zero-Tailing Mechanisms and Material Efficiency
Zero-tailing technology is a mechanical innovation designed to eliminate the “remnant” or “tail” typically left behind by traditional chuck-based feeding systems. In standard configurations, the last 300mm to 500mm of a beam cannot be processed because the gripping mechanism requires a minimum surface area to hold the workpiece.
Modern Plasma Cutting Machines for the Oil and Gas sector utilize a dual-chuck or a pass-through clamping system. This allows the torch to reach the absolute end of the profile while the secondary clamp maintains the structural rigidity of the piece. In the context of expensive alloys or heavy-duty structural steel used in tank supports, reducing the scrap rate by even 5% per beam results in substantial annual savings. This efficiency is a core KPI for industrial engineers focused on lean manufacturing principles within the energy sector.
H-Beam Processing and Low Maintenance Requirements
The durability of the cutting hardware is paramount in the harsh environments of fabrication yards. Plasma systems are specifically engineered for high duty cycles, often operating in multi-shift environments. Unlike mechanical drilling or sawing lines, H-beam low maintenance is a primary advantage of plasma technology. The absence of physical contact between the cutting tool and the workpiece eliminates tool wear and the risk of mechanical breakage.
Maintenance protocols for these machines are streamlined to focus on consumable management and rail cleanliness. The plasma torch itself uses standardized electrodes and nozzles that can be swapped in seconds. Furthermore, the robust construction of the gantry and the drive systems—often utilizing helical rack and pinion sets—ensures that the machine remains calibrated despite the vibrations and dust characteristic of heavy steel fabrication. For an industrial engineer, this high uptime is essential for meeting the tight deadlines associated with large-scale petrochemical projects.
Optimizing the Heat Affected Zone (HAZ)
While plasma is a thermal cutting process, modern high-definition systems utilize narrow-constriction nozzles and specialized gas mixtures (such as Oxygen-Oxygen or Argon-Hydrogen) to concentrate the energy beam. This concentration minimizes the Heat Affected Zone (HAZ), preserving the metallurgical properties of the H-beam or tank plate. Maintaining the grain structure of the steel is vital for tanks that will hold pressurized or corrosive fluids, where any weakness in the base metal could lead to stress corrosion cracking over time.
Advanced Beveling for Weld Preparation
In the fabrication of Oil and Gas tanks, the quality of the weld is only as good as the preparation of the edge. Beveling is a critical step that dictates the penetration and strength of the subsequent joins. 5-axis plasma heads enable the creation of V, Y, X, and K-shaped bevels in a single pass. This capability is particularly important for the thick plates used in tank floors and shells.
The software integration allows for “bevel compensation,” where the system automatically adjusts the torch angle and height to account for the kerf (the width of the cut) at different degrees of inclination. This ensures that the root face and the bevel angle remain consistent throughout the entire length of the cut, even on curved surfaces. By automating the beveling process, fabricators eliminate the labor-intensive task of manual edge preparation, which is both time-consuming and prone to human error.
Software Integration and BIM Compatibility
The modern plasma cutting machine does not operate in isolation. It is an extension of the engineering office. Direct integration with Building Information Modeling (BIM) software and CAD/CAM platforms allows for the seamless transfer of complex geometries. The zero-tailing logic is embedded within the nesting software, which calculates the optimal placement of parts on a beam to ensure that the “tail-less” feature is utilized to its maximum potential. This end-to-end digital workflow reduces the “art” of cutting to a precise science, allowing for predictable lead times and standardized quality across global project sites.
Conclusion: The Industrial Engineering Perspective
The implementation of zero-tailing plasma cutting technology represents a strategic investment for firms specializing in Oil and Gas tank fabrication. By focusing on the mechanical advantages of H-beam low maintenance and the technical precision of 3D intersection accuracy, industrial engineers can drastically improve production throughput. The ability to perform complex beveling and utilize every millimeter of raw material through zero-tailing mechanisms ensures that the fabrication process is as lean as it is robust. As the energy sector continues to demand higher safety standards and lower costs, the reliance on high-definition plasma systems for structural integrity will only increase.
-


Cantilever Welding Robot solution
-


GF laser cutting machine
-

P3015 plasma cutting machine
-

LFP3015 Fiber Laser Cutter
-

pipe plasma cutting machine
-
LFH 4020 Fiber Laser Cutting Machine
-
LFP4020
-

gantry plasma air cutting machine
-

3D robot cutting machine
-

8 axis plasma cutting machine
-

5 axis plasma cutting machine
-

LT360 tube laser cutting machine
-

robot welding workstation
-

SF6060 fiber laser cutting machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.