Optimizing Structural Fabrication via Plasma Zero-Tailing Systems
In the heavy construction machinery sector, the efficiency of structural component fabrication is determined by material utilization rates and the precision of secondary processing. Industrial engineers are increasingly turning toward Zero-tailing technology to solve the inherent waste issues associated with traditional profile cutting. In a standard production environment, the final 300mm to 500mm of an H-beam or channel is often discarded because the machine’s feeding mechanism loses its grip on the workpiece. Zero-tailing systems utilize a specialized dual-chuck or synchronized gripper movement that allows the plasma torch to process the entire length of the raw material, effectively reducing scrap rates to near zero.
This leap in material efficiency directly impacts the bottom line, especially when dealing with high-tensile strength steels common in excavator frames, crane booms, and chassis components. By maximizing the nesting density on a single beam, manufacturers can achieve a 5% to 10% increase in total output per ton of raw material. This performance metric is critical in high-volume environments where raw material costs constitute the largest portion of the operating budget.
Achieving Superior Intersection Accuracy in Complex Profiles
Construction machinery demands complex geometric intersections where circular or rectangular tubing meets H-beams at varying angles. Maintaining high intersection accuracy is vital for ensuring the structural integrity of the final assembly. Plasma Cutting Machines equipped with 5-axis or 6-axis robotic heads provide the necessary degrees of freedom to compensate for the natural variances in structural steel profiles.
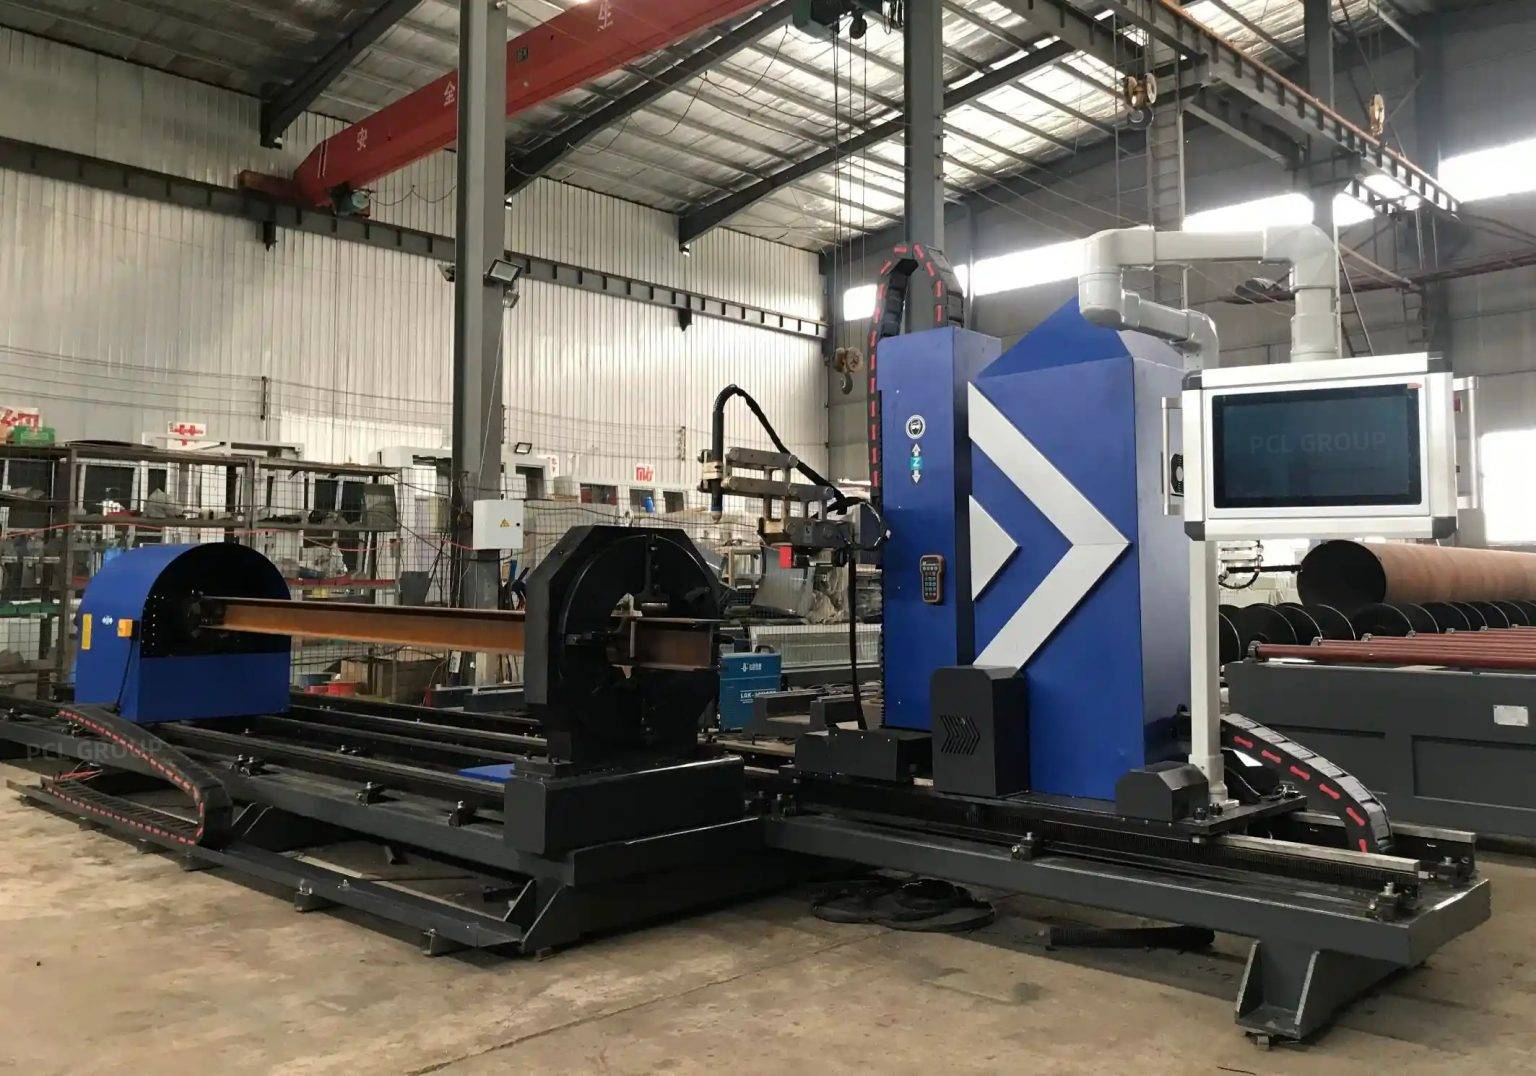
The accuracy of these intersections is managed through real-time sensing and software compensation. As the plasma torch moves across the flanges and web of an H-beam, the system must account for the thickness changes and the radius of the inner corners. High-definition plasma power sources maintain a consistent arc density, ensuring that the kerf remains uniform throughout the cut. This level of precision eliminates the need for manual grinding or fit-up adjustments during the assembly phase, significantly reducing labor hours in the downstream production line.
H-Beam Processing and the Advantage of Low Maintenance
From an operational standpoint, H-beam low maintenance is a primary driver for selecting plasma technology over alternative thermal cutting methods in heavy industry. Construction machinery plants are often harsh environments characterized by metallic dust, vibration, and temperature fluctuations. Plasma systems are inherently robust; the cutting head lacks sensitive optical components that are prone to contamination or misalignment.
The maintenance cycle for a heavy-duty plasma cutter focuses primarily on consumables—nozzles, electrodes, and swirl rings. Modern systems feature “long-life” technology that extends the number of pierces per set of consumables, reducing the frequency of machine downtime. For an industrial engineer, this translates to higher Machine Utilization (MU) rates. Furthermore, the mechanical simplicity of the torch height control (THC) and the rack-and-pinion drive systems means that in-house maintenance teams can perform most repairs without requiring specialized external technicians, keeping the Mean Time To Repair (MTTR) at a minimum.
Advanced Plasma Beveling for Structural Preparation
Preparation for high-strength joints in construction machinery requires precise edge geometries. Plasma beveling allows for the creation of V, Y, X, and K-shaped bevels in a single pass. This is particularly important for the thick plates used in the manufacturing of loader buckets and heavy-duty chassis. By integrating the beveling process directly into the cutting cycle, the need for a secondary beveling operation—such as milling or manual torching—is removed.
The integration of CNC-controlled beveling heads ensures that the angle remains consistent even when the torch is navigating complex contours. Advanced software algorithms calculate the necessary kerf compensation for the tilted arc, ensuring that the dimensional tolerances of the part are maintained. For the industrial engineer, this consolidation of processes reduces work-in-progress (WIP) and simplifies the factory footprint by eliminating dedicated beveling stations.
Thermal Management and Material Integrity
One of the technical challenges in heavy structural cutting is managing the Heat Affected Zone (HAZ). While plasma cutting is a thermal process, the high speed of the plasma arc minimizes the duration of heat exposure to the base material. This is crucial for Construction Machinery that utilizes quenched and tempered steels. By optimizing the cutting speed and gas mixture (typically using Oxygen for carbon steel or H35 for stainless and thick sections), engineers can ensure that the metallurgical properties of the H-beam or plate remain within design specifications.
Data-Driven Optimization and Nesting Efficiency
The implementation of zero-tailing plasma systems is complemented by sophisticated nesting software. This software does not merely arrange parts to fit a shape; it considers the sequence of cuts to maintain the structural rigidity of the beam during the process. For zero-tailing to be effective, the software must communicate perfectly with the machine’s PLC to coordinate the hand-off between grippers. This level of automation ensures that the machine can run “lights-out” or with minimal supervision, further reducing the cost per part.
In summary, the transition to plasma cutting machines with zero-tailing capabilities represents a strategic shift toward lean manufacturing in the construction machinery sector. By focusing on the intersection of high precision, material conservation, and mechanical durability, manufacturers can achieve a more resilient and profitable production flow. The ability to handle H-beams with minimal maintenance and prepare edges with integrated beveling provides a clear competitive advantage in an industry where speed and structural reliability are paramount.
-


Cantilever Welding Robot solution
-


GF laser cutting machine
-

P3015 plasma cutting machine
-

LFP3015 Fiber Laser Cutter
-

pipe plasma cutting machine
-
LFH 4020 Fiber Laser Cutting Machine
-
LFP4020
-

gantry plasma air cutting machine
-

3D robot cutting machine
-

8 axis plasma cutting machine
-

5 axis plasma cutting machine
-

LT360 tube laser cutting machine
-

robot welding workstation
-

SF6060 fiber laser cutting machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.