The Engineering Mandate for Plasma Systems in Wind Energy
Wind tower fabrication demands a rigorous approach to material processing, primarily due to the immense scale and the structural fatigue requirements of the final assembly. In this heavy-industrial context, Plasma Cutting remains the dominant technology for processing carbon steel plates ranging from 20mm to over 100mm in thickness. Unlike thinner gauge applications, wind tower sections require high energy density and significant thermal penetration to maintain cutting speeds that align with global production timelines.
The implementation of plasma cutting wind towers technology allows for the rapid partitioning of large-format plates and the precise cutting of internal access points. From an industrial engineering perspective, the efficiency of the cutting process is not merely defined by the speed of the torch but by the cumulative accuracy of the thermal edge and the minimization of secondary processing. Plasma systems optimized for this sector utilize high-definition power sources that constrict the arc, resulting in a narrower kerf and a reduced heat-affected zone (HAZ), which is vital for preserving the metallurgical properties of the tower shells.
Optimizing Throughput via Offline Programming (OLP)
A significant bottleneck in traditional fabrication is the reliance on “at-machine” programming. For wind tower components, which feature complex geometries and varying diameters, manual G-code entry or basic onboard CAM adjustments lead to excessive machine downtime. The shift toward offline programming software represents a fundamental improvement in the kinematic chain of production.
Digital Twin and Kinematic Simulation
Offline programming allows engineers to create a digital twin of the plasma cutting cell. This environment enables the simulation of torch movements, ensuring that the plasma lead-ins and lead-outs are positioned to prevent gouging or thermal deformation. By generating the cutting paths in a dedicated CAD/CAM suite, the machine remains in constant operation on the shop floor while the next nest is being prepared.
Collision Avoidance and Path Optimization
In the context of curved shell segments, the risk of torch collision is high. OLP software calculates the exact spatial orientation of the plasma head, particularly when dealing with the variable heights of rolled plates. This preemptive calculation eliminates the “trial and error” phase on the production floor, directly increasing the machine’s duty cycle and reducing the risk of damaging expensive consumables or the torch head itself.
Ensuring Intersection Accuracy for Internal Components
The structural integrity of a wind tower depends heavily on the fit-up of internal platforms, door frames, and cable management brackets. These components often intersect with the curved inner surface of the tower at complex angles. Achieving high CNC beveling accuracy at these intersections is a primary requirement for ensuring that the subsequent assembly phases proceed without manual grinding or excessive gap-filling.
True Hole Technology and Geometric Precision
Modern plasma systems utilize specialized software protocols to adjust gas flow and torch height dynamically when cutting bolt holes and small-diameter intersections. This “True Hole” or equivalent technology compensates for the natural taper of the plasma arc. For wind tower door sections, where thick reinforcements must be inserted, the precision of the intersection cut ensures that the load-bearing capacity of the tower is not compromised by poor fit-up.
Tolerance Management in Large-Scale Fabrication
Industrial engineers must account for the accumulation of tolerances. By using plasma cutting systems with high-resolution encoders and rigid gantry designs, the deviation across a 10-meter plate can be kept within sub-millimeter ranges. This level of precision is critical when the shell segments are moved to the fit-up stations, as any deviation in the intersection profile can lead to significant delays during the alignment process.
H-Beam Design and Low Maintenance Requirements
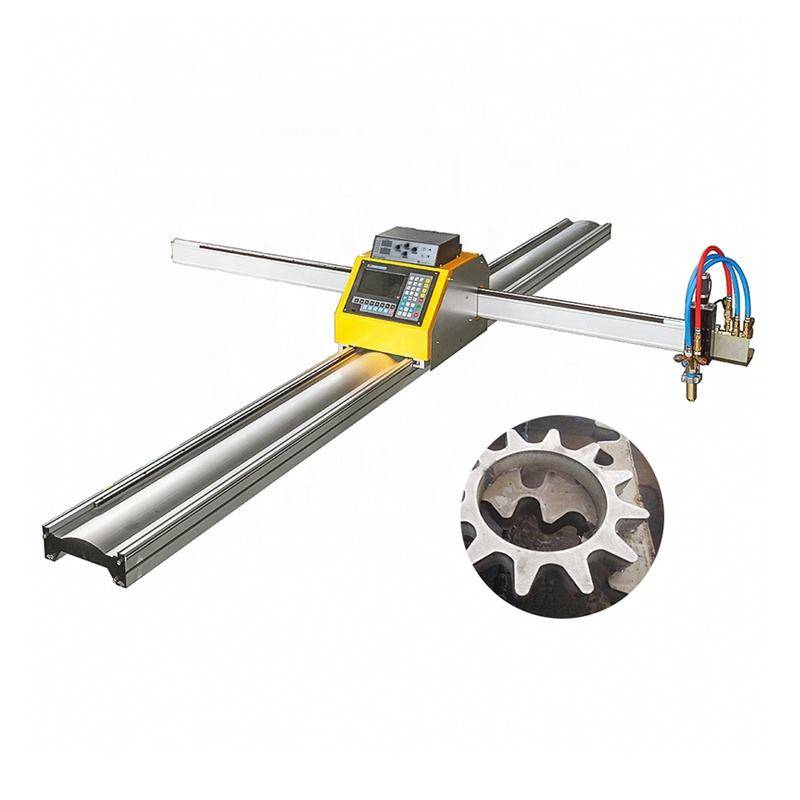
The physical infrastructure of the Plasma Cutting Machine is as important as the electronics. In the harsh environment of a tower fabrication facility—characterized by metallic dust, vibrations, and high temperatures—the mechanical design of the machine’s rail system is a key factor in long-term reliability.
Structural Rigidity of the H-Beam Gantry
Many high-end plasma systems utilize a heavy-duty H-beam fabrication style for the main gantry and rail supports. The use of H-beams provides superior torsional rigidity compared to lighter hollow-section frames. This stiffness is essential for maintaining accuracy during high-speed traverses and when carrying heavy multi-axis bevel heads.
Reduced Maintenance Profiles
From a maintenance engineering standpoint, the simplicity of the H-beam and linear guide combination is a major advantage. Unlike complex enclosed systems that can trap abrasive dust, open H-beam structures are easier to clean and inspect. Coupled with automated lubrication systems and bellows for rack-and-pinion protection, these machines achieve high Mean Time Between Failures (MTBF). Lower maintenance overhead translates directly to a lower total cost of ownership (TCO) and higher availability for multi-shift operations.
Advanced Beveling for Weld Preparation
The most technically demanding aspect of wind tower plasma cutting is the beveling of plate edges. Tower sections are typically joined using submerged arc welding (SAW), which requires specific groove profiles (V, Y, X, or K-cuts) to ensure full-thickness penetration.
Multi-Axis Plasma Head Capabilities
Modern plasma machines are equipped with 5-axis or 6-axis bevel heads that can tilt and rotate in real-time. This allows the machine to cut the bevel angle and the land (the flat vertical portion of the edge) in a single pass. In wind tower production, where wall thicknesses vary as one moves up the tower, the ability to transition from a 30-degree bevel to a 45-degree bevel dynamically is indispensable.
Thermal Control and Edge Quality
Precision beveling requires sophisticated control of the plasma arc’s energy distribution. As the torch tilts, the effective thickness of the material increases, requiring the CNC controller to adjust the amperage and gas pressure instantaneously. OLP software plays a vital role here by calculating the “tilt-lead” and “tilt-side” compensations necessary to maintain a consistent bevel angle across the entire circumference of a shell segment. This precision eliminates the need for manual edge preparation, which is both labor-intensive and prone to human error.
Conclusion: The Integrated Fabrication Strategy
The synergy between high-precision plasma hardware and offline programming software creates a robust foundation for wind tower manufacturing. By focusing on intersection accuracy, the structural reliability of H-beam gantry designs, and the sophisticated requirements of multi-axis beveling, industrial engineers can ensure that the fabrication facility operates at peak efficiency. These systems provide the necessary scalability to meet the increasing dimensions of offshore and onshore wind components while maintaining the strict quality standards required for renewable energy infrastructure.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.