Optimization of Pressure Vessel Fabrication via 5-Axis Plasma Systems
In the industrial engineering landscape of the Oil & Gas sector, the fabrication of storage tanks and high-pressure vessels demands rigorous adherence to geometric tolerances and metallurgical integrity. The transition from manual edge preparation to automated 5-axis plasma beveling represents a fundamental shift in production efficiency. Unlike standard 2D cutting, 5-axis systems facilitate complex weld preparations—including V, X, Y, and K-cuts—directly during the primary profiling stage. This capability eliminates the need for secondary mechanical beveling, which is often the primary bottleneck in heavy-plate fabrication cycles.
Kinematics and the Mechanics of the 5-Axis Bevel Head
The core of the 5-axis system lies in its ability to manipulate the plasma torch across the X, Y, and Z linear axes while simultaneously controlling the tilt (A-axis) and rotation (B-axis). for Oil & Gas Tanks, which often utilize plates exceeding 25mm in thickness, maintaining a consistent torch-to-workpiece distance is critical. Industrial-grade bevel heads utilize high-torque AC servo motors coupled with precision planetary gearboxes to ensure angular repeatability within ±0.1 degrees. This precision is essential when creating the landing zones and bevel angles required for full-penetration submerged arc welding (SAW) processes.
Achieving Precise Pipe and Shell Intersection Accuracy
One of the most complex challenges in tank engineering is the creation of nozzle openings and manways. These require pipe intersection accuracy that accounts for the curvature of the main vessel shell. A 5-axis plasma machine utilizes advanced algorithms to calculate the varying bevel angle along the contoured path of the intersection. As the torch moves around the circumference of a nozzle hole on a cylindrical tank shell, the angle of the cut must constantly transition to maintain a uniform weld prep gap.
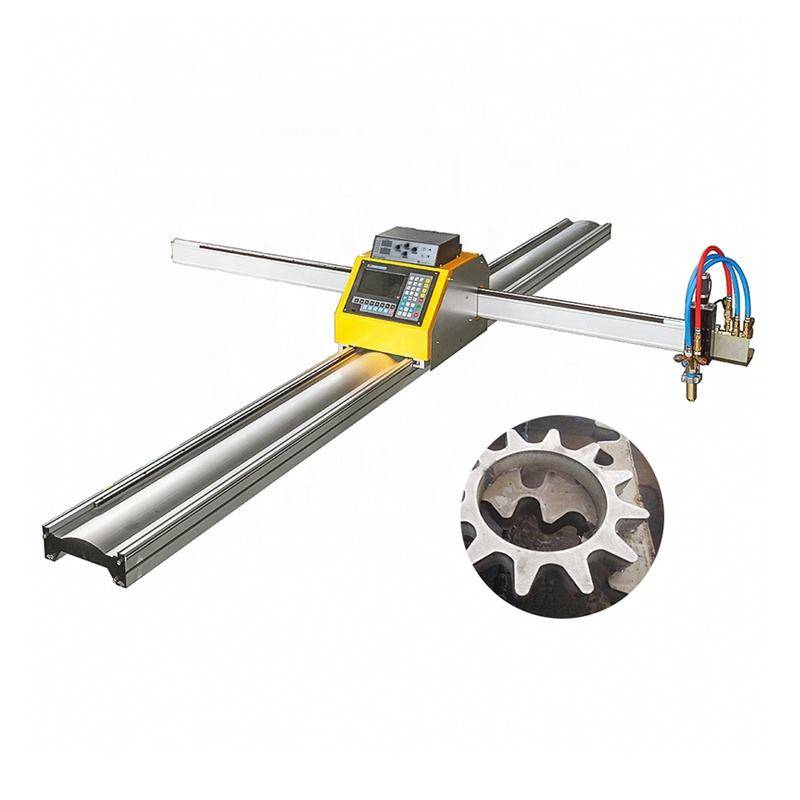
Modern CNC controllers integrate real-time kerf compensation and arc voltage height sensing (AVHC) to adapt to minor plate imperfections or slight variations in the tank’s radius. By automating this geometric calculation, the margin for human error in layout and manual cutting is removed, ensuring that the fit-up between the shell and the nozzle meets the strict 1-2mm tolerance windows specified by engineering blueprints.
Structural Rigidity: The Role of Heavy-Duty H-Beam Construction
Machine stability is the foundation of cutting accuracy. High-definition plasma systems for the Oil & Gas industry are typically built on heavy-duty H-beam construction. From an industrial engineering perspective, the choice of an H-beam gantry and rail support system is driven by the need to dampen the vibrations generated during high-speed rapid traverses. Unlike lighter aluminum extrusions, the mass of a stress-relieved steel H-beam ensures that the inertia of the 5-axis head does not translate into “ghosting” or serrations on the cut surface.
Low Maintenance Design and Long-Term Reliability
The harsh environments of tank farms and shipyards necessitate equipment that minimizes operational downtime. The H-beam structure supports oversized linear guides and helical rack-and-pinion drives, which distribute mechanical loads more effectively than ball screws over long travel distances (often exceeding 12 meters). This structural choice leads to a low maintenance profile, as the rigidity prevents the misalignment of the drive components over thousands of duty cycles. Furthermore, the use of bellows and pressurized lubrication systems protects these critical surfaces from the abrasive metallic dust inherent in the Plasma Cutting process.
Thermal Management and Heat-Affected Zone (HAZ) Control
Plasma cutting is a thermal process, and in the context of Oil & Gas alloys—specifically high-strength carbon steels and stainless steels—minimizing the Heat-Affected Zone is paramount. High-definition plasma technology narrows the arc through oxygen or nitrogen shielding gases, concentrating the energy density. This results in a cleaner cut with a smaller HAZ compared to traditional oxy-fuel methods. For the engineer, this means the metallurgical properties of the tank shell remain within specification, reducing the risk of hydrogen-induced cracking or stress corrosion in the weld zones.
Software Integration and Nesting Efficiency
The efficiency of a 5-axis plasma machine is not solely a function of its hardware but also its integration with CAD/CAM environments. For large-scale tank projects, nesting software must optimize plate utilization while considering the lead-in and lead-out requirements for beveled edges. Beveled cuts require more “real estate” on the plate than vertical cuts due to the tilt of the torch. Advanced software calculates these offsets automatically, ensuring that the 5-axis plasma beveling head does not collide with previously cut parts or the water table slats. This predictive modeling is a key component in reducing scrap rates, which is a major KPI in high-volume industrial projects.
Optimizing the Workflow: From CAD to Weld-Ready Part
The traditional workflow for tank fabrication involved three distinct stages: thermal cutting, mechanical grinding for beveling, and manual fit-up adjustment. By implementing a 5-axis plasma solution, these three stages are condensed into one. The part comes off the table with the pipe intersection accuracy required for immediate assembly. This “one-hit” manufacturing approach reduces the labor hours per ton of steel significantly.
From a maintenance standpoint, the reduction in secondary equipment (such as handheld grinders and portable beveling tools) simplifies the facility’s asset management. The focus shifts to maintaining a single, robust machine center designed for 24/7 operation. The reliability of the heavy-duty H-beam construction ensures that the machine remains calibrated even when subjected to the temperature fluctuations of non-climate-controlled fabrication shops.
Technical Parameters for Oil & Gas Applications
When specifying a plasma system for this sector, several technical benchmarks must be met:
- Angular Range: Minimum +/- 45 degrees to accommodate V and K bevels.
- Positioning Accuracy: Within ±0.05 mm over a 1000 mm span.
- Voltage Control: plasma arc voltage control with a response time under 10ms to prevent torch collisions during beveling.
- Gas Console: Automatic multi-gas consoles for switching between O2, N2, and H35 for different alloy types.
Conclusion of Technical Requirements
The selection of a plasma cutting system for Oil & Gas tank fabrication must prioritize structural integrity and geometric precision. By utilizing 5-axis technology, manufacturers address the core challenges of weld preparation and intersection fit-up. The combination of high-definition plasma sources and a rigid H-beam platform provides the necessary balance of speed, accuracy, and durability. This engineering approach ensures that the final vessels meet the high-pressure safety standards of the energy sector while maintaining a competitive cost-per-part through reduced secondary labor and long-term mechanical reliability.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.