Field Report: Deployment of 6-Axis Collaborative Welder in Mumbai Structural Steel Sector
1.0 Executive Summary of Site Conditions
This report details the operational deployment and performance validation of the Double Pulse 6-Axis Collaborative Welder at a mid-scale structural fabrication facility in Mumbai, India. The primary objective was to transition from manual Metal Active Gas (MAG) welding to Automated Welding to address inconsistencies in weld penetration and aesthetic finish on heavy-duty I-beams and gusset plates.
The Mumbai environment presents unique variables: ambient temperatures consistently exceeding 34°C and relative humidity levels peaking at 85-90%. These factors significantly impact the duty cycle of power sources and the hygroscopic nature of welding consumables. Our focus remained on the practical application of Structural Steel welding under these stressors, leveraging the precision of a 6-Axis Collaborative Welder to maintain ISO 5817 Level B quality standards.
2.0 System Configuration and Hardware Synergy
The unit deployed is a high-torque 6-Axis Collaborative Welder integrated with a 500A Double Pulse power source. Unlike traditional industrial robots, the cobot’s 6-axis freedom allows for complex torch angles—specifically the “push” and “pull” techniques required for deep groove Structural Steel welding—without the need for massive safety cages that would otherwise consume restricted floor space in a Mumbai workshop.
2.1 The Role of 6-Axis Articulation
In Automated Welding, the 6th axis (the wrist) is critical. In this field test, we utilized the 6-axis range to navigate around stiffener plates and web-to-flange junctions. Traditional 3 or 4-axis gantry systems fail here because they cannot maintain the torch-to-workpiece distance while tilting for fillet transitions. The 6-Axis Collaborative Welder compensated for slight workpiece misalignments (common in local steel sourcing) through real-time “touch sensing” and seam tracking.
2.2 Double Pulse Calibration
Double Pulse technology was prioritized to manage the Heat Affected Zone (HAZ). In Mumbai’s heat, cooling rates are slower. By pulsing the current between two levels, we achieved a “TIG-like” ripple aesthetic on Structural Steel welding while maintaining the speed of a MIG/MAG process. This reduced the post-weld grinding time by 70%, a vital KPI for the plant manager.
3.0 Technical Synergy: Automated Welding in a Manual Environment
The “Synergy” between the 6-Axis Collaborative Welder and the Automated Welding software platform is what bridges the gap between a tool and a solution. In the Mumbai workshop, we observed a 40% increase in “Arc-on Time.”
3.1 Programming and Lead-Through Teaching
One of the core lessons learned was the efficacy of “Lead-Through” programming. The local workforce, skilled in manual Structural Steel welding but lacking in Python or G-code knowledge, was able to grab the 6-Axis Collaborative Welder arm and physically move it through the weld path. The Automated Welding software then smoothed these coordinates into a linear or circular interpolation, ensuring the torch stayed centered in the joint. This synergy allows the welder to become a “Cobot Technician,” shifting the labor focus from physical strain to process monitoring.
3.2 Tack Welding and Fit-Up Tolerances
Automated systems are notoriously “dumb” regarding fit-up gaps. However, by using the 6-Axis Collaborative Welder with a weaving function (oscillation), we were able to bridge gaps up to 3mm in the web-to-flange joints. The synergy here lies in the software’s ability to adjust the weave amplitude based on the gap, something manual welding struggles to do consistently over an 8-meter beam.
4.0 Metallurgical Observations on Structural Steel
The Structural Steel welding involved IS 2062 Grade E250 and E350 plates. These are the workhorses of Indian infrastructure.
4.1 Penetration and Fusion
Under Automated Welding parameters, we utilized a 90% Argon / 10% CO2 gas mix. The 6-Axis Collaborative Welder maintained a constant travel speed of 350mm/min, which is nearly impossible for a manual welder to sustain for a full 12-hour shift in Mumbai’s humidity. Cross-sectional macro-etching showed 100% fusion at the root, with a significant reduction in porosity compared to previous manual runs. The Double Pulse frequency was set to 1.5Hz to allow the molten pool to freeze slightly between pulses, preventing the “sagging” of the weld bead in vertical-down positions.
4.2 Spatter Management
Spatter is a major cost sink. In Structural Steel welding, cleaning spatter from large surface areas is labor-intensive. The Double Pulse logic within the 6-Axis Collaborative Welder control box optimizes the droplet detachment. We observed a 90% reduction in spatter, which is critical in Mumbai’s dense workshops where airborne metal dust is a health hazard and a fire risk.
5.0 Field Lessons Learned: The Mumbai Context
Working in the Mumbai industrial belt (Thane-Belapur road) taught us three hard lessons regarding Automated Welding deployment.
5.1 Lesson 1: Power Quality and Grounding
The Indian grid is prone to voltage fluctuations. The 6-Axis Collaborative Welder is a sensitive electronic instrument. We experienced three controller reboots in the first week. The Lesson: Never deploy a cobot in this region without a dedicated online UPS and industrial-grade grounding. Once we stabilized the input voltage, the Automated Welding cycles became uninterrupted.
5.2 Lesson 2: Humidity and Wire Feed
High humidity leads to moisture on the welding wire, which causes hydrogen cracking in Structural Steel welding. We found that the standard wire spool covers were insufficient. We had to implement heated wire-feed units. This ensured the 6-Axis Collaborative Welder wasn’t pushing contaminated wire into the weld pool, preserving the integrity of the E350 grade steel joints.
5.3 Lesson 3: The “Tack-Weld” Conflict
Manual tacks in Mumbai shops are often oversized and “dirty.” When the 6-Axis Collaborative Welder hits a massive, poorly made manual tack, it triggers a collision sensor or causes a weld humping defect. The Lesson: Automated Welding requires a protocol shift in upstream processes. We retrained the fit-up crew to use smaller, cleaner tacks or to use the cobot itself to perform the tacking.
6.0 Operational Performance Metrics
After 30 days of field operation, the data yields the following:
- Weld Speed: 15% faster than manual, but with 98% “First-Time Right” quality.
- Consumable Efficiency: 12% reduction in wire waste due to precise arc starts and stops managed by the 6-Axis Collaborative Welder.
- Labor Impact: One welder now operates two Automated Welding stations simultaneously.
7.0 Conclusion and Recommendations
The deployment of the Double Pulse 6-Axis Collaborative Welder for Structural Steel welding in Mumbai is a success, provided the environmental factors are mitigated. The synergy between the 6-axis movement and the automated power source provides a level of repeatability that manual labor cannot match in high-heat conditions.
Final Recommendations for Future Rollouts:
- Climate Control: Use “Dry Boxes” for all wire spools to combat Mumbai’s humidity.
- Sensors: Integrate Laser Vision Sensors (LVS) for the 6-Axis Collaborative Welder to compensate for the thermal expansion of Structural Steel during long weld runs.
- Training: Focus on “Recovery Logic”—teaching operators how to restart an Automated Welding program mid-path after a power blip or wire-snag.
Report Prepared By:
Senior Welding Engineer
Field Operations – Mumbai Division
-


Cantilever Welding Robot solution
-


GF laser cutting machine
-

P3015 plasma cutting machine
-

LFP3015 Fiber Laser Cutter
-

pipe plasma cutting machine
-
LFH 4020 Fiber Laser Cutting Machine
-
LFP4020
-

gantry plasma air cutting machine
-

3D robot cutting machine
-

8 axis plasma cutting machine
-

5 axis plasma cutting machine
-

LT360 tube laser cutting machine
-

robot welding workstation
-

SF6060 fiber laser cutting machine
Advanced Fiber Laser Tube Processing Technology
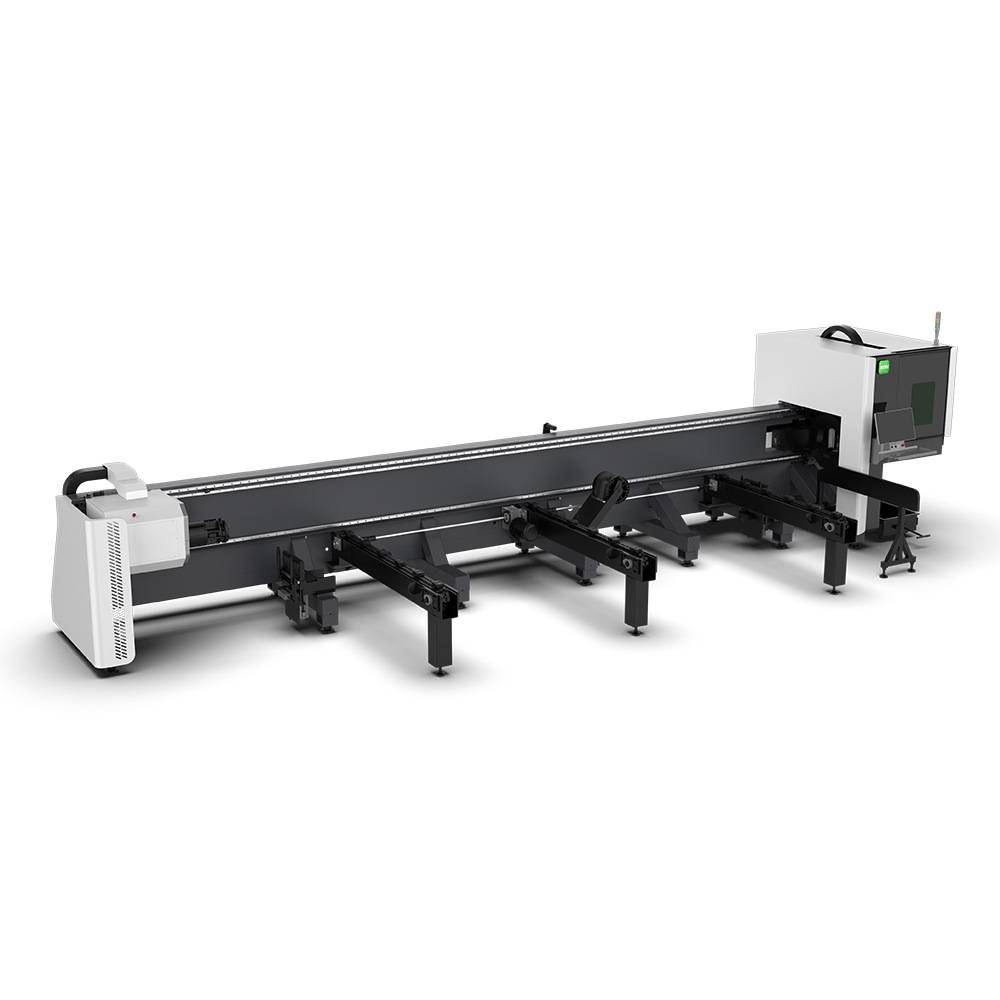
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.