Beam Processing Center with Arc Voltage Control for for Shipbuilding
In this article
- Advanced Structural Fabrication in Shipbuilding
- The Role of Arc Voltage Control (AVC) in Precision Profiling
- Mechanism of Voltage Feedback
- Impact on Cut Quality and Kerf Consistency
- Optimizing Intersection Accuracy for Structural Blocks
- Plasma Beveling and Weld Preparation
- Multi-Axis Robotic Kinematics
- Standardizing the Fit-Up
- Maintenance Efficiency in H-Beam Processing
- Conclusion
Advanced Structural Fabrication in Shipbuilding
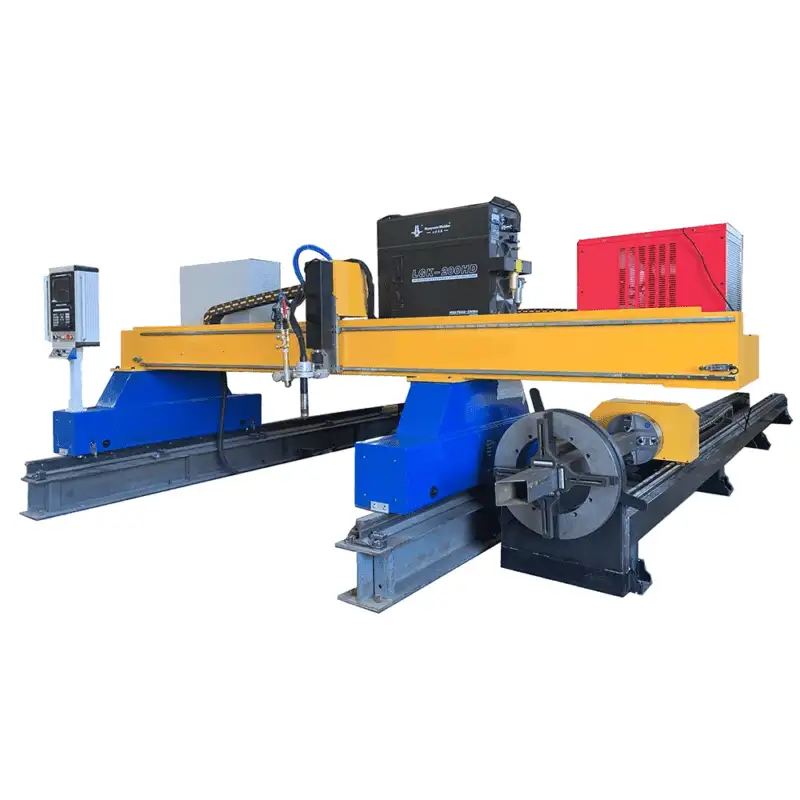
Modern shipbuilding demands extreme precision in the fabrication of structural components such as bulb flats, angles, and H-beams. The primary challenge in the ship block assembly process is the sheer volume of steel combined with the complex geometry required for fluid dynamics and structural stability. A Beam Processing Center (BPC) serves as the core of this fabrication stage. By utilizing Plasma Cutting technology, these centers provide the necessary thermal energy to pierce and profile thick-walled steel sections that comprise the skeletal framework of a vessel.
Unlike traditional manual layout methods, a robotic BPC interprets CAD/CAM data to execute complex cuts with repeatable accuracy. The transition to automated plasma processing is driven by the need to reduce labor costs and increase the duty cycle of the fabrication line. In this industrial context, the focus remains strictly on the thermal profiling and preparation of structural sections to ensure they meet the stringent tolerances required for subsequent assembly phases.
The Role of Arc Voltage Control (AVC) in Precision Profiling
In the maritime industry, steel beams often arrive with surface irregularities, rust, or physical deformations caused by mill cooling processes or storage. Maintaining a consistent distance between the plasma torch nozzle and the workpiece—known as the standoff distance—is critical for cut quality. This is where arc voltage control becomes an indispensable feature of the processing center.
Mechanism of Voltage Feedback
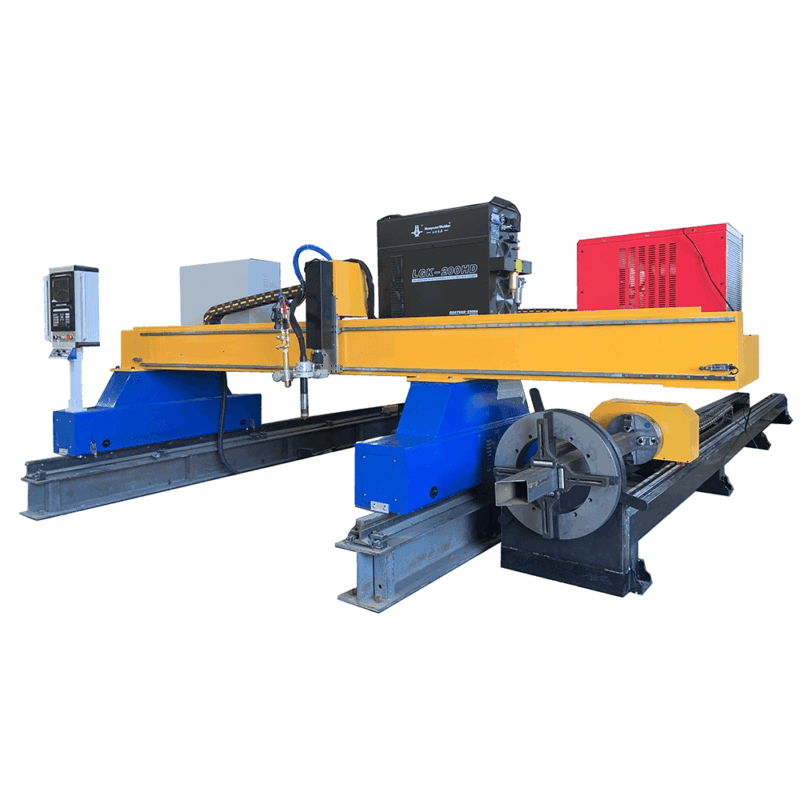
The AVC system operates on the principle that the voltage of the plasma arc is directly proportional to its length. As the distance between the torch and the beam increases, the voltage increases; as it decreases, the voltage drops. The BPC controller monitors this voltage at millisecond intervals. If the system detects a deviation from the setpoint, it triggers a high-speed Z-axis motor to adjust the torch height instantly.
Impact on Cut Quality and Kerf Consistency
Without real-time height adjustment, a warped beam would cause the torch to either crash or move too far away, leading to a loss of the arc or a wide, slanted kerf. By maintaining a constant arc length, the AVC ensures that the plasma stream hits the material at the optimal focal point. This results in a cleaner cut with minimal dross and a narrow Heat-Affected Zone (HAZ), which is vital for maintaining the metallurgical properties of the shipbuilding steel.
Optimizing Intersection Accuracy for Structural Blocks
Shipbuilding involves a high density of intersections where longitudinal stiffeners pass through transverse web frames. Any gap or misalignment at these intersections necessitates costly “filling” or rework during the assembly stage. A Beam Processing Center addresses this through advanced kinematic algorithms that coordinate the movement of the robotic arm and the beam feeding system.
Mitigating Cumulative Error
Precision in intersection cutting relies on the synchronization of the longitudinal feed (X-axis) and the multi-axis movement of the plasma head. High-end BPCs utilize laser scanning or mechanical probing to “locate” the beam’s actual position before the first cut. This compensates for any “camber” or “sweep” in the H-beam, ensuring that cutouts for pipes or other structural members are located exactly where the design specifies, regardless of the raw material’s physical imperfections.
Software-Driven Geometry Compensation
The integration of 3D nesting software allows the BPC to calculate the exact path required for “rat holes” and drainage notches. By ensuring high intersection accuracy, the shipyard can move directly from the BPC to the assembly floor, significantly reducing the lead time for block construction. This precision is what allows for the modular construction techniques currently favored in global naval architecture.
Plasma Beveling and Weld Preparation
For heavy-duty structural steel, a square edge is rarely sufficient for deep penetration welds. Automated beveling is a specialized function of the BPC that allows for the creation of V, Y, X, and K-cross sections in a single pass.
Multi-Axis Robotic Kinematics
The plasma torch is typically mounted on a 5-axis or 6-axis robotic system. This allows the torch to tilt (A-axis) and rotate (B-axis) while traversing the beam. In shipbuilding, where curved sections and angled bulkheads are common, the ability to produce a variable bevel along a single cut path is a significant technological advantage.
Standardizing the Fit-Up
Consistent bevel angles are essential for robotic welding systems used later in the production line. If the bevel angle fluctuates, the volume of the weld groove changes, leading to inconsistent penetration or excessive weld metal deposition. The BPC ensures that every bevel adheres to the ISO or AWS standards specified in the engineering data, providing a predictable environment for the welding engineers.
Maintenance Efficiency in H-Beam Processing
From an industrial engineering perspective, the uptime of the equipment is as important as its precision. Beam Processing Centers designed for plasma cutting are built to withstand the harsh environments of maritime fabrication shops.
Robustness of Thermal Systems
Plasma systems are inherently more robust than alternative thermal cutting technologies when dealing with the heavy dust and vibrations of a shipyard. The H-beam handling systems—usually consisting of heavy-duty conveyors and cross-transfers—are engineered for high-tonnage throughput. Because plasma cutting is a non-contact process, there is no mechanical stress placed on the torch itself, which reduces the frequency of replacement parts compared to mechanical drilling or milling.
Low Maintenance Requirements
The focus on structural integrity extends to the machine design. Modern BPCs use pressurized cabinets for electronics to prevent the ingress of metallic dust. The consumables in a plasma torch (electrodes, nozzles, and shields) are designed for rapid changeover, often taking less than two minutes. This ensures that the machine remains operational for three shifts a day, which is the standard requirement in large-scale shipyard operations.
Fume Extraction and Slag Management
Effective maintenance also involves the management of byproducts. High-capacity downdraft tables or specialized beam-clamping fume extractors remove the particulate matter generated during the plasma process. This protects the precision linear guides and rack-and-pinion drives of the BPC, ensuring that the machine maintains its 0.1mm positioning accuracy over years of operation.
Conclusion
The integration of a Beam Processing Center with Arc Voltage Control represents a critical upgrade for shipyards aiming to enhance their fabrication throughput. By focusing on the precision of plasma intersections and the versatility of robotic beveling, shipbuilders can ensure that every structural component fits perfectly within the larger vessel block. The mechanical reliability of these systems, combined with the real-time height sensing of AVC, provides a high-efficiency solution that minimizes manual intervention and maximizes the utilization of raw steel materials. As maritime engineering continues to push the limits of scale and complexity, the role of automated thermal profiling remains the foundation of structural excellence.





