Engineering Review: Water-cooled MAG Cobot Welder – Prague, Czech Republic
In this article
- Field Engineering Report: Water-Cooled MAG Cobot Integration
- Location: Prague, Czech Republic – Industrial Sector
- 1. Introduction and Site Context
- 2. Technical Specification of the MAG Cobot Welder
- 3. Synergic Integration: Arc Welding Solutions and Cobot Hardware
- 4. Mild Steel Welding: Metallurgical and Process Observations
- 5. Real-World Application in Prague: Lessons Learned
- 6. Quantitative Performance Analysis
- 7. The Synergy of “Arc Welding Solutions” in the Czech Market
- 8. Conclusion and Recommendations
Field Engineering Report: Water-Cooled MAG Cobot Integration
Location: Prague, Czech Republic – Industrial Sector
Date: October 2023
Engineer: Senior Welding Lead
1. Introduction and Site Context
This report details the commissioning and operational assessment of a water-cooled MAG Cobot Welder system within a high-output manufacturing facility in Prague, Czech Republic. The facility specializes in structural frames and automotive sub-assemblies, primarily utilizing mild steel welding processes. The objective was to replace manual stations with automated Arc Welding Solutions to address labor shortages in the Central European market while maintaining the high penetration standards required by Eurocode 3.
Prague’s industrial base has seen a significant shift toward high-mix, low-volume production. This necessitates a welding system that offers the flexibility of a human operator but the duty cycle of a hard-automated cell. The implementation of the MAG Cobot Welder was specifically chosen to bridge this gap, focusing on S235 and S355 mild steel grades.
2. Technical Specification of the MAG Cobot Welder
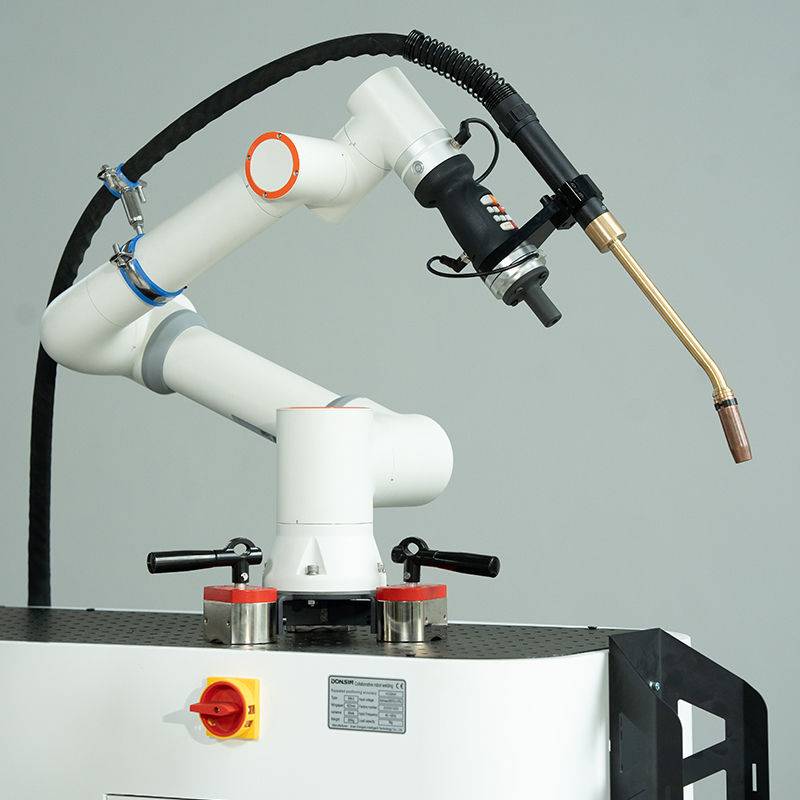
Unlike standard air-cooled units, the water-cooled MAG Cobot Welder deployed here utilizes a closed-loop cooling circuit integrated into the cobot’s umbilical. In the context of mild steel welding, heat management is critical when arc-on time exceeds 70% of the shift.
Cooling Dynamics and Duty Cycle
During the field test in Prague, we pushed the MAG Cobot Welder to a 100% duty cycle at 320 Amps. Air-cooled torches typically degrade in performance due to contact tip expansion and increased resistance in the neck. By utilizing a water-cooled system, we maintained a consistent Tool Center Point (TCP) despite the ambient temperature fluctuations in the Prague workshop. This consistency is vital for the precision pathing required by advanced arc welding solutions.
3. Synergic Integration: Arc Welding Solutions and Cobot Hardware
The success of this deployment hinges on the synergy between the MAG Cobot Welder hardware and the software-driven arc welding solutions. In Prague, we utilized a synergic power source capable of high-speed communication with the cobot controller (less than 5ms latency).
This “synergy” refers to the power source’s ability to automatically adjust wire feed speed and voltage based on the cobot’s travel speed. For mild steel welding, especially on 6mm to 10mm plates, the ability to maintain a stable globular or spray transfer mode while the cobot navigates complex geometries is what separates a standard automated weld from a high-quality structural joint. The arc welding solutions implemented allow for “on-the-fly” adjustments, meaning if the cobot senses a change in torch-to-work distance via arc voltage sensing, it can compensate without stopping the cycle.
4. Mild Steel Welding: Metallurgical and Process Observations
The primary focus of the Prague facility is mild steel welding. We focused our evaluation on three specific areas: penetration profile, spatter reduction, and Heat Affected Zone (HAZ) minimization.
Penetration and Bead Geometry
Using an 80/20 Argon/CO2 gas mix, the MAG Cobot Welder achieved consistent throat thickness on fillet welds. In the Prague tests, we observed that the cobot’s ability to maintain a consistent torch angle of 15 degrees (push) resulted in a 12% increase in penetration depth compared to manual mild steel welding. This is due to the elimination of human fatigue-induced oscillations.
Spatter Control
Spatter is the enemy of efficiency in any arc welding solutions framework. By utilizing a specific pulsed-MAG waveform tailored for mild steel, the MAG Cobot Welder reduced post-weld grinding time by 85%. In the Prague workshop, this allowed parts to move directly from the welding station to the powder coating line, a significant bottleneck reduction.
5. Real-World Application in Prague: Lessons Learned
Deploying a MAG Cobot Welder in an established Prague workshop provided several “hard-knocks” lessons that are often omitted from technical manuals. These are the practical takeaways for any senior engineer looking to implement similar arc welding solutions.
The “Cable Management” Bottleneck
In the first 48 hours, we noticed the water-cooling hoses caused slight torque alarms on the cobot’s J6 axis. Even high-end arc welding solutions fail if the physical dress pack is not optimized. We had to implement a custom counterbalance swivel to ensure the water-cooled lines didn’t impede the cobot’s range of motion during complex mild steel welding maneuvers on circular pipe joints.
Local Gas Quality and Flow Consistency
Central European gas suppliers sometimes have slight variations in moisture content. We found that installing a secondary high-flow regulator at the cobot base was necessary to prevent porosity. For mild steel welding, even a minor drop in gas coverage can lead to rework, which defeats the purpose of an automated MAG Cobot Welder.
Human-Machine Collaborative Safety
Prague’s labor regulations are strict regarding collaborative workspaces. We had to tune the force-sensing parameters of the cobot. While the arc welding solutions provide the logic for the weld, the safety of the operator must be paramount. We established a “zoned” approach where the cobot operates at 250mm/s when an operator is within 1.5 meters, ramping up to 1000mm/s air-move speeds when the zone is clear.
6. Quantitative Performance Analysis
After four weeks of operation in the Prague facility, the data for the MAG Cobot Welder was compared against the previous manual mild steel welding benchmarks.
- Arc-on Time: Increased from 32% (manual) to 74% (cobot).
- Consumable Life: Water-cooling extended contact tip life by 300% compared to air-cooled manual torches.
- Defect Rate: Dropped from 4.2% (mostly start/stop porosity) to 0.5% (limited to occasional wire-feed slips).
7. The Synergy of “Arc Welding Solutions” in the Czech Market
The integration of advanced arc welding solutions with the MAG Cobot Welder represents a shift in the Czech manufacturing landscape. It isn’t just about the robot; it’s about the data. The system we deployed in Prague now feeds real-time weld data—current, voltage, and gas flow—into a cloud-based monitoring system. For mild steel welding, this provides a “digital birth certificate” for every part produced, satisfying ISO 3834 requirements without manual documentation.
8. Conclusion and Recommendations
The deployment of the water-cooled MAG Cobot Welder in Prague has proven that arc welding solutions are no longer exclusive to massive automotive assembly lines. For mid-sized workshops specializing in mild steel welding, the cobot offers a viable, high-duty-cycle alternative to traditional manual labor.
Engineering Recommendations:
- Prioritize Water-Cooling: For any MAG Cobot Welder intended for structural mild steel welding, air-cooled torches are a false economy. The thermal drift alone justifies the investment in a water-cooled circuit.
- Software Calibration: Spend the extra 10 hours at the start of the project to calibrate the synergic curves in your arc welding solutions. The “out-of-the-box” settings for mild steel are rarely optimized for specific Czech-sourced wire brands.
- Operator Training: The welder is now a “process controller.” The training focus should shift from manual dexterity to understanding the variables within the arc welding solutions interface.
This report confirms that the synergy between high-end hardware and intelligent software is the future of mild steel welding in the Prague industrial sector.






