Beam Processing Center with Offline Programming for for Bridge Trusses
In this article
Optimizing Bridge Truss Fabrication via Automated Beam Processing
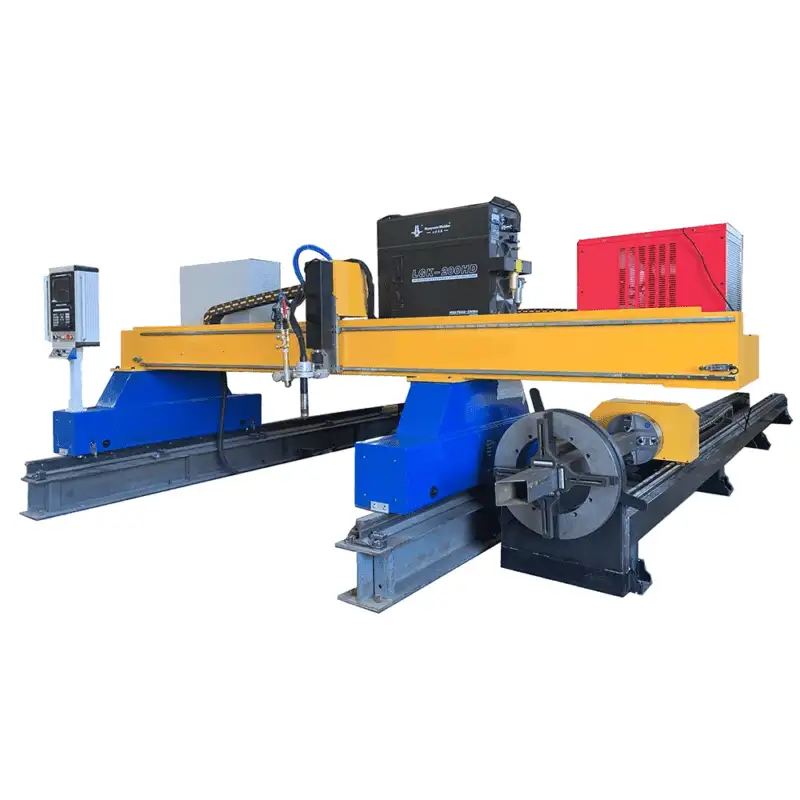
The engineering requirements for modern bridge trusses demand extreme precision and structural reliability. As infrastructure projects scale in complexity, the traditional methods of manual layout, mechanical sawing, and magnetic drilling have become bottlenecks. The transition toward a Beam Processing Center equipped with advanced plasma technology represents a fundamental shift in structural steel throughput. This system integrates multi-axis robotics with sophisticated software to handle H-beams, I-beams, and channels with minimal human intervention.
In the context of bridge construction, where load-bearing calculations depend on the exact fitment of diagonal and vertical members, the margin for error is non-existent. The use of thermal cutting via plasma allows for the creation of complex geometries—such as cope cuts, block-outs, and bolt holes—within a single workstation. This consolidation of processes reduces material handling time and eliminates the compounded tolerances associated with moving a beam between multiple machines.
The Critical Role of Offline Programming
Efficiency in a high-output fabrication shop is measured by machine uptime. Offline Programming (OLP) is the catalyst for this efficiency. Rather than programming the robot or CNC gantry at the machine interface, engineers utilize OLP environments to simulate the entire cutting process in a digital twin scenario. By importing DSTV or STEP files directly from detailing software like Tekla or SDS2, the system generates precise tool paths while the machine is actively processing another workpiece.
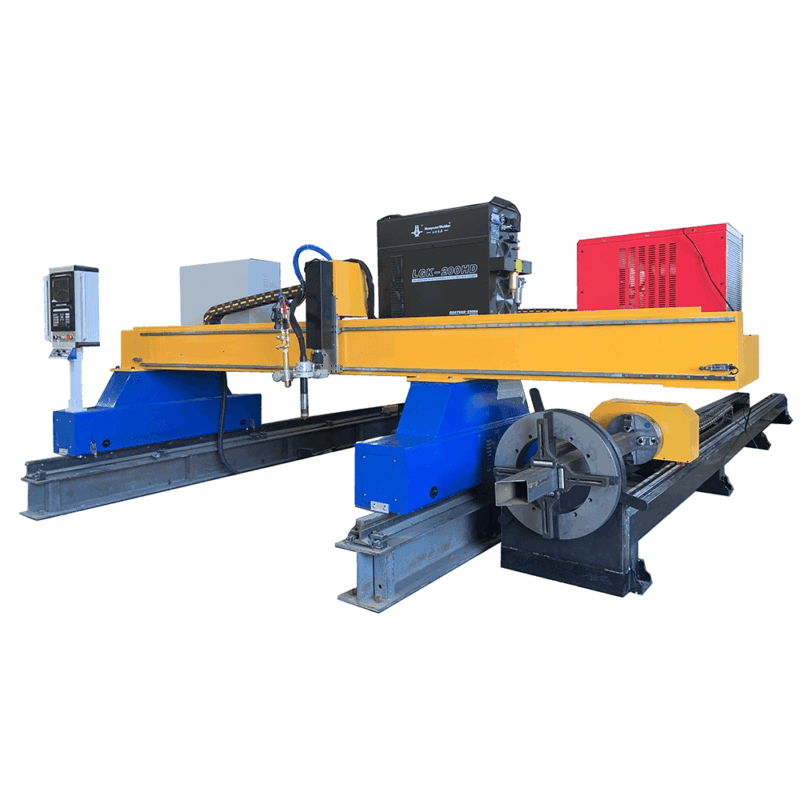
This workflow allows for the early detection of potential collisions and reaches issues. for Bridge Trusses, which often involve massive heavy-wall sections, the OLP software calculates the exact entry and exit points for the plasma torch. It accounts for the thickness of the material and the specific kerf width of the plasma arc. This proactive approach ensures that when the file reaches the Beam Processing Center, the execution is flawless, maximizing the duty cycle of the power supply and the structural integrity of the cut.
Achieving Superior Intersection Accuracy
The geometry of bridge trusses involves numerous intersections where cords meet webs at varying angles. Plasma Cutting Accuracy is paramount here. A multi-axis plasma head can tilt and rotate to follow the calculated intersection line of two structural members, creating a “perfect fit” that requires no additional grinding or shimming. This is particularly vital for H-beams, where the flange-to-web transition often presents challenges for mechanical tools.
Advanced sensors within the processing center perform real-time measurements of the actual beam. Structural steel is rarely perfectly straight; it possesses inherent camber, sweep, and twist from the rolling mill. The automated system probes the beam’s surface to locate the actual centerlines and flange heights. The OLP-generated path is then dynamically adjusted to match the physical reality of the steel. This ensures that bolt holes are perfectly aligned across long spans and that mitered joints meet with the tight tolerances required by AWS D1.5 Bridge Welding Code.
Advanced Beveling for Weld Preparation
Bridge components typically require full penetration or deep partial penetration joints. This necessitates complex beveling on the ends of the beams. A Beam Processing Center utilizes its 3D motion capability to perform V, Y, X, and K-style bevels during the initial cutting phase. Unlike mechanical beveling which is slow and often limited to straight edges, plasma beveling can follow curved profiles and variable angles.
The ability to bevel the web and flanges simultaneously, including transitions through the radius (the “k-area”), is a significant advantage. This precise edge preparation ensures that the subsequent fit-up is seamless. By controlling the torch angle and height via sophisticated algorithms, the system maintains a consistent land and bevel angle across the entire profile of the H-beam, regardless of material thickness variations. This precision directly impacts the volume of filler metal required and the overall time spent on the assembly floor.
H-Beam Maintenance and System Durability
From an industrial engineering perspective, the maintenance profile of a plasma-based Beam Processing Center is highly favorable for structural steel environments. Unlike mechanical systems that rely on high-speed drill bits, saws, and milling cutters—all of which suffer from wear, breakage, and high replacement costs—plasma is a non-contact cutting process. This results in significantly lower consumable costs per foot of cut.
The primary maintenance involves the management of copper consumables (nozzles and electrodes) and the filtration of the fume extraction system. For heavy H-beam processing, where the environment is often dusty and vibrates heavily, plasma systems are notably robust. Modern power sets feature self-diagnostic capabilities that monitor gas flow, coolant temperature, and arc stability. This predictive maintenance data allows facility managers to schedule downtime during off-shifts, ensuring that the bridge truss production line remains continuous and predictable.
Streamlining Throughput and Material Flow
The integration of automated cutting and Offline Programming transforms the fabrication shop into a precision manufacturing cell. By eliminating manual marking and layout—a process traditionally prone to human error—the shop drastically reduces scrap rates. In bridge fabrication, where high-strength steel grades are expensive and lead times for heavy sections are long, minimizing material waste is a critical financial driver.
Furthermore, the data generated during the OLP phase provides accurate time-study metrics. Management can predict exactly how long a specific truss assembly will take to process, allowing for tighter scheduling of downstream activities. The precision of the plasma cut means that parts arrive at the assembly area ready for immediate fit-up. The elimination of secondary cleaning or manual beveling operations shortens the overall production cycle, enabling fabricators to meet the aggressive timelines often associated with infrastructure projects.
Conclusion of Process Advantages
The technical synergy between Plasma Cutting Accuracy and Offline Programming creates a robust framework for bridge truss production. By focusing on the specific needs of H-beam processing—such as multi-axis beveling and high-precision intersections—industrial engineers can ensure that structural components meet the most stringent safety standards while maintaining high throughput. The shift toward these automated centers is not merely an upgrade in machinery; it is a fundamental optimization of the structural steel fabrication lifecycle, prioritizing accuracy, low maintenance, and data-driven production.







