Optimizing LNG Infrastructure with Advanced Plasma Cutting Systems
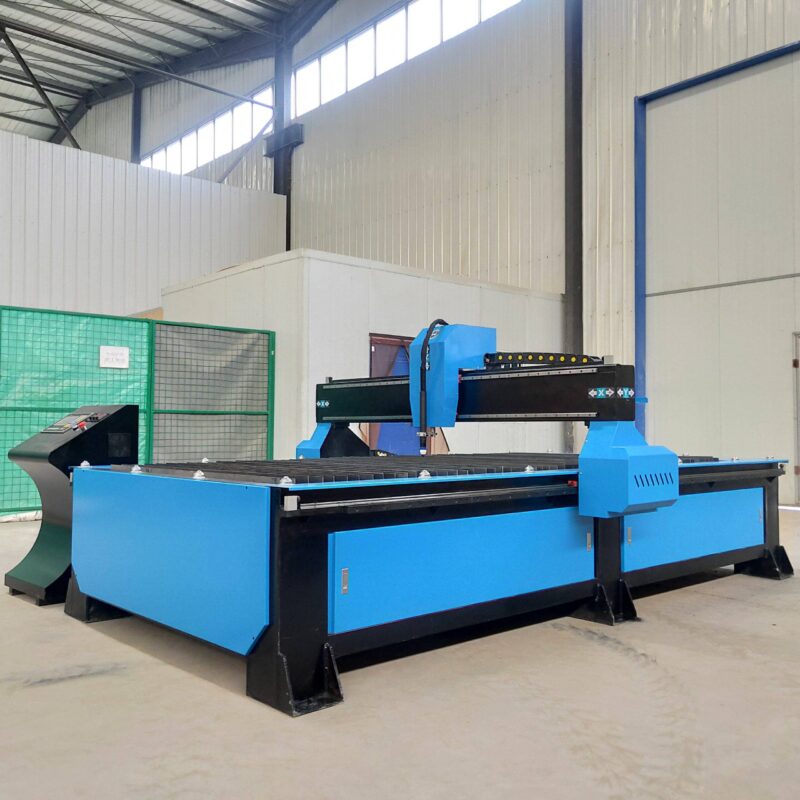
The construction of Liquefied Natural Gas (LNG) facilities demands a level of structural precision that leaves zero margin for error. Given the cryogenic nature of the fluids involved—often stored at temperatures below -160 degrees Celsius—the materials used, typically stainless steel or 9% nickel steel, require sophisticated processing. Plasma Cutting Technology has emerged as the primary standard for fabricating the intricate piping manifolds and heavy-duty structural frames required for regasification units and storage tanks. Unlike mechanical shearing or older thermal methods, plasma systems provide the thermal energy density necessary to penetrate thick alloys while maintaining metallurgical integrity.
The Critical Role of Arc Voltage Control (AVC)
In high-precision industrial environments, the distance between the plasma torch tip and the workpiece is the most significant variable affecting cut quality. Arc Voltage Control (AVC) acts as the real-time feedback mechanism that maintains this distance. As the torch traverses the material, the system monitors the electrical potential of the plasma arc. If the metal plate is warped or if there is a slight deviation in the height of an H-beam, the voltage fluctuates.
The AVC system instantly processes these voltage changes and adjusts the Z-axis motor to compensate. This constant synchronization ensures that the arc remains stable, the kerf width stays consistent, and the dross accumulation is minimized. for LNG Projects, where large plates often exhibit slight deviations due to their sheer surface area, AVC prevents torch collisions and ensures that every linear meter of cutting meets ISO 9013 Grade 2 or 3 standards.
Achieving Superior Intersection Accuracy
LNG facilities utilize massive networks of interconnected piping, ranging from small-diameter instrument lines to large-bore cryogenic headers. The geometry of these intersections—where one pipe meets another at a specific angle—is mathematically complex. Intersection Accuracy is vital because any gap exceeding 1mm can lead to excessive weld volume or structural weaknesses.
Plasma Cutting Machines utilized in this sector employ multi-axis heads capable of articulating around the circumference of a pipe or the web of an H-beam. By integrating AVC with CNC software, the machine can calculate the exact “saddle” or “fishmouth” cut required for a perfect fit-up. The result is a seamless transition between components that allows for uniform heat distribution during the subsequent joining processes, reducing the risk of stress concentrations in the finished assembly.
Structural Processing: H-Beam Low Maintenance Requirements
The skeletal framework of an LNG terminal relies heavily on structural H-beams and I-beams. Traditional methods of processing these members, such as mechanical drilling or sawing, involve high consumables costs and frequent tool replacement. Plasma cutting systems offer a significant advantage through H-beam low maintenance profiles.
Because plasma is a non-contact cutting process, there is no physical force exerted on the machine’s gantry or the cutting head. This absence of mechanical stress translates to a longer lifespan for bearings, rails, and motors. In an industrial engineering context, this reduces the Mean Time To Repair (MTTR) and increases the overall equipment effectiveness (OEE). For LNG contractors working on tight timelines, the reliability of a plasma system ensures that structural fabrication continues 24/7 without the downtime associated with blade changes or hydraulic system failures found in mechanical alternatives.
Automated Beveling for High-Pressure Integrity
Weld preparation is perhaps the most time-consuming aspect of heavy fabrication. In LNG projects, most joints require full penetration welds to handle internal pressures and thermal expansion cycles. This necessitates complex bevel profiles, including V-grooves, Y-grooves, and K-cuts.
Modern plasma systems equipped with 5-axis bevel heads can execute these geometries in a single pass. The AVC system is particularly crucial during beveling; as the torch tilts to an angle, the arc voltage characteristics change. Advanced controllers compensate for this shift, ensuring the bevel angle remains precise throughout the entire length of the cut. This eliminates the need for manual secondary grinding, which is both labor-intensive and prone to human error. A clean, plasma-cut bevel provides the ideal surface for robotic or manual arc welding, ensuring radiographic-quality joints.
Material Efficiency and Heat-Affected Zone Management
One of the primary concerns for engineers in the LNG sector is the Heat-Affected Zone (HAZ). Excessive heat can alter the grain structure of specialized steels, potentially leading to embrittlement at cryogenic temperatures. High-definition plasma systems use constricted arcs and high travel speeds to narrow the HAZ.
By maintaining a high feed rate facilitated by reliable AVC, the thermal input into the base material is localized. This precision not only preserves the material properties but also reduces plate distortion. In large-scale tank construction, where thousands of meters of plate are cut, the reduction in distortion significantly simplifies the fit-up and assembly stages, leading to a faster project completion rate.
Operational ROI in LNG Infrastructure
From a CAPEX and OPEX perspective, the investment in a plasma machine with LNG Infrastructure-grade capabilities is justified by the reduction in labor costs and material waste. The ability to nest complex parts efficiently, combined with the speed of plasma compared to oxy-fuel on stainless alloys, results in a lower cost-per-part. Furthermore, the integration of AVC reduces the scrap rate caused by “diving” torches or inconsistent arc heights, which is a critical factor when working with expensive high-nickel alloys.
Conclusion: Technical Superiority in High-Stakes Fabrication
The technical requirements of LNG projects demand fabrication tools that can deliver consistency under rigorous conditions. Plasma cutting machines, when optimized with Arc Voltage Control, provide the necessary intersection accuracy and beveling precision required for cryogenic safety. By focusing on a low-maintenance structural processing approach, industrial engineers can ensure that the fabrication phase of energy projects remains efficient, safe, and aligned with international engineering standards. The synergy between CNC precision and plasma power remains the benchmark for heavy-duty metal processing in the modern energy landscape.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.