H-Beam Production Line with Laser Seam Tracking for Wind Tower fabrication
In this article
Optimizing Wind Tower Structural Fabrication via Plasma Systems
The fabrication of wind towers demands extreme structural integrity and high-volume throughput. As global energy transitions accelerate, the demand for secondary steel structures and internal H-beam reinforcements has scaled exponentially. Industrial engineers are now prioritizing automated solutions that bridge the gap between raw material processing and final assembly. The core of this evolution lies in the deployment of heavy-duty H-Beam Production Lines equipped with advanced Plasma Cutting accuracy and real-time sensing technologies.
Unlike lighter structural applications, wind tower internals—such as platforms, foundation supports, and ladder brackets—require thick-gauge steel processing. Plasma technology remains the preferred thermal cutting method for these thicknesses due to its balance of speed, cost-efficiency, and metallurgical performance. By integrating laser seam tracking into the plasma gantry, manufacturers can mitigate common issues such as material warping and beam camber, ensuring that every cut aligns with the digital twin model of the tower.
Precision Intersections and Geometric Accuracy
In the context of H-beam production, intersection accuracy is critical. Wind tower components often feature complex interlocking geometries where beams must meet at precise angles to distribute loads evenly. Traditional mechanical measuring often fails to account for the inherent irregularities in hot-rolled H-beams. Laser seam tracking sensors solve this by scanning the profile of the web and flanges in real-time, feeding positional data back to the CNC controller.
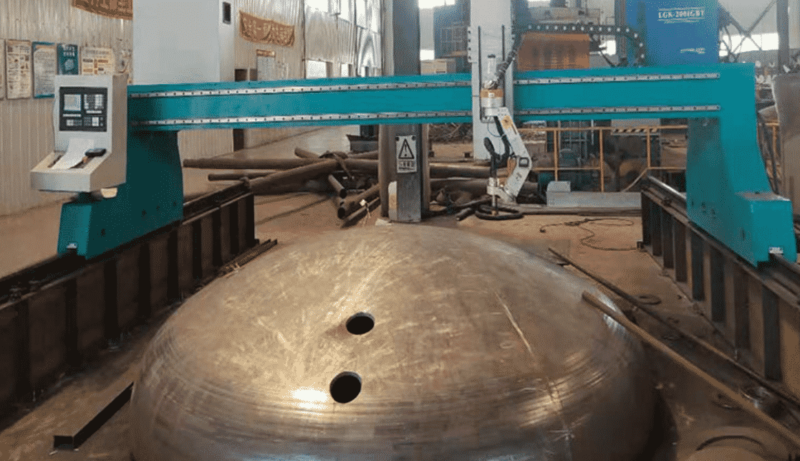
This dynamic adjustment ensures that the plasma torch maintains a constant standoff distance and stays perfectly centered on the intended path. When cutting “fish-mouth” joints or intricate cope cuts for beam-to-beam intersections, the laser seam tracking system accounts for “sweep” or “twist” in the long structural members. This precision eliminates the need for manual fit-up adjustments on the assembly floor, drastically reducing the total man-hours required per tower section.
Advanced Beveling for Structural Integrity
Wind tower components are subject to massive cyclical loads and environmental stress. Consequently, nearly every edge on an H-beam requires specific edge preparation. Automated beveling using multi-axis plasma heads allows for the creation of V, Y, K, and X-type bevels in a single pass. This is particularly important for the heavy-duty flanges used in tower foundations, where deep penetration is mandatory for structural certification.
Modern plasma beveling units utilize high-definition plasma power sources to minimize the heat-affected zone (HAZ). By controlling the gas chemistry and arc voltage, the system produces a clean, dross-free edge that is ready for subsequent processing. The ability to execute a complex bevel on a curved or warped H-beam surface is only possible through the high-speed data acquisition provided by laser sensors, which map the surface topography milliseconds before the arc is struck.
Engineering for Low Maintenance and High Uptime
From an industrial engineering perspective, the “Total Cost of Ownership” (TCO) is a primary KPI. Plasma systems are inherently robust, designed to operate in the dusty, high-vibration environments typical of heavy steel fabrication. One of the standout features of modern H-beam lines is the H-beam production efficiency gained through low-maintenance architectures. Unlike alternative thermal processes that rely on sensitive optics or mirrors, plasma torches are rugged tools.
The primary maintenance requirements for these lines are restricted to consumable replacement—electrodes, nozzles, and shields. Advanced CNC systems now include “consumable life” monitoring, which predicts failure before it occurs, allowing for scheduled downtime rather than emergency stops. Furthermore, the laser tracking sensors used in these environments are typically housed in protective, air-cooled enclosures with splash guards, ensuring they survive the intense ultraviolet light and molten spray associated with heavy plasma cutting.
Throughput Analysis and Process Flow Integration
Integrating a laser-guided plasma line into a wind tower facility transforms the workflow from a batch-process mentality to a continuous flow. In a traditional setup, beams are measured, marked, cut, and then moved to a secondary station for beveling. In a synchronized H-beam production line, these steps are compressed. The beam is loaded onto a conveyor, the laser sensor detects the leading edge, identifies the beam’s orientation, and the plasma head executes all cuts and bevels in one continuous motion.
This integration significantly reduces material handling, which is one of the highest risks for workplace injury and one of the largest “hidden” costs in structural steelwork. By automating the detection of material deviations, the system also reduces scrap rates. In an industry where raw material costs can fluctuate wildly, the ability to get the cut right the first time is a significant competitive advantage.
Thermal Distortion Management
A frequent challenge in plasma cutting thick H-beams is the management of thermal expansion. As the plasma arc introduces heat into the web or flange, the steel expands. Without compensation, a cut that starts accurately may end several millimeters out of tolerance. The laser seam tracking system continuously recalibrates the torch path based on the actual state of the metal during the cut. This closed-loop feedback system is essential for maintaining the tight tolerances required by international wind energy standards, such as EN 1090-2 or AWS D1.1.
Strategic Conclusion for Wind Energy Fabricators
The shift toward larger wind turbines and offshore installations necessitates a more rigorous approach to H-beam fabrication. By focusing on the synergy between plasma cutting and laser sensing, manufacturers can achieve levels of intersection accuracy and beveling consistency that were previously unattainable. The durability and low maintenance requirements of plasma systems ensure that the production line remains a profit center rather than a bottleneck.
Ultimately, the implementation of a laser seam tracking enabled production line represents a shift toward “intelligent” manufacturing. It allows for the processing of lower-tolerance raw materials while producing higher-tolerance finished components, effectively decoupling material cost from final product quality. For the industrial engineer, this is the pinnacle of process optimization: increasing quality, reducing waste, and ensuring the long-term reliability of the world’s renewable energy infrastructure.







