Field Evaluation: 1500W All-in-one Cobot Station Integration
1. Project Scope and Site Environment
This report details the operational deployment of a 1500W All-in-one Cobot Station at a medium-scale structural fabrication facility in Tuas, Singapore. The objective was to transition from manual Metal Active Gas (MAG) welding to an automated laser-based system to address the localized shortage of high-skill welders and to improve throughput on Thick Plate Steel welding applications.
The Singapore workshop environment presents unique challenges, specifically high ambient humidity (averaging 80%+) and constrained floor space. Traditional robotic cells require extensive safety fencing and a footprint that most Jurong-based workshops cannot spare. The deployment of Collaborative Robotics was selected specifically to mitigate these spatial constraints while maintaining high safety standards under the Ministry of Manpower (MOM) guidelines for Class 4 laser operations.
2. The Synergy of Collaborative Robotics and All-in-one Design
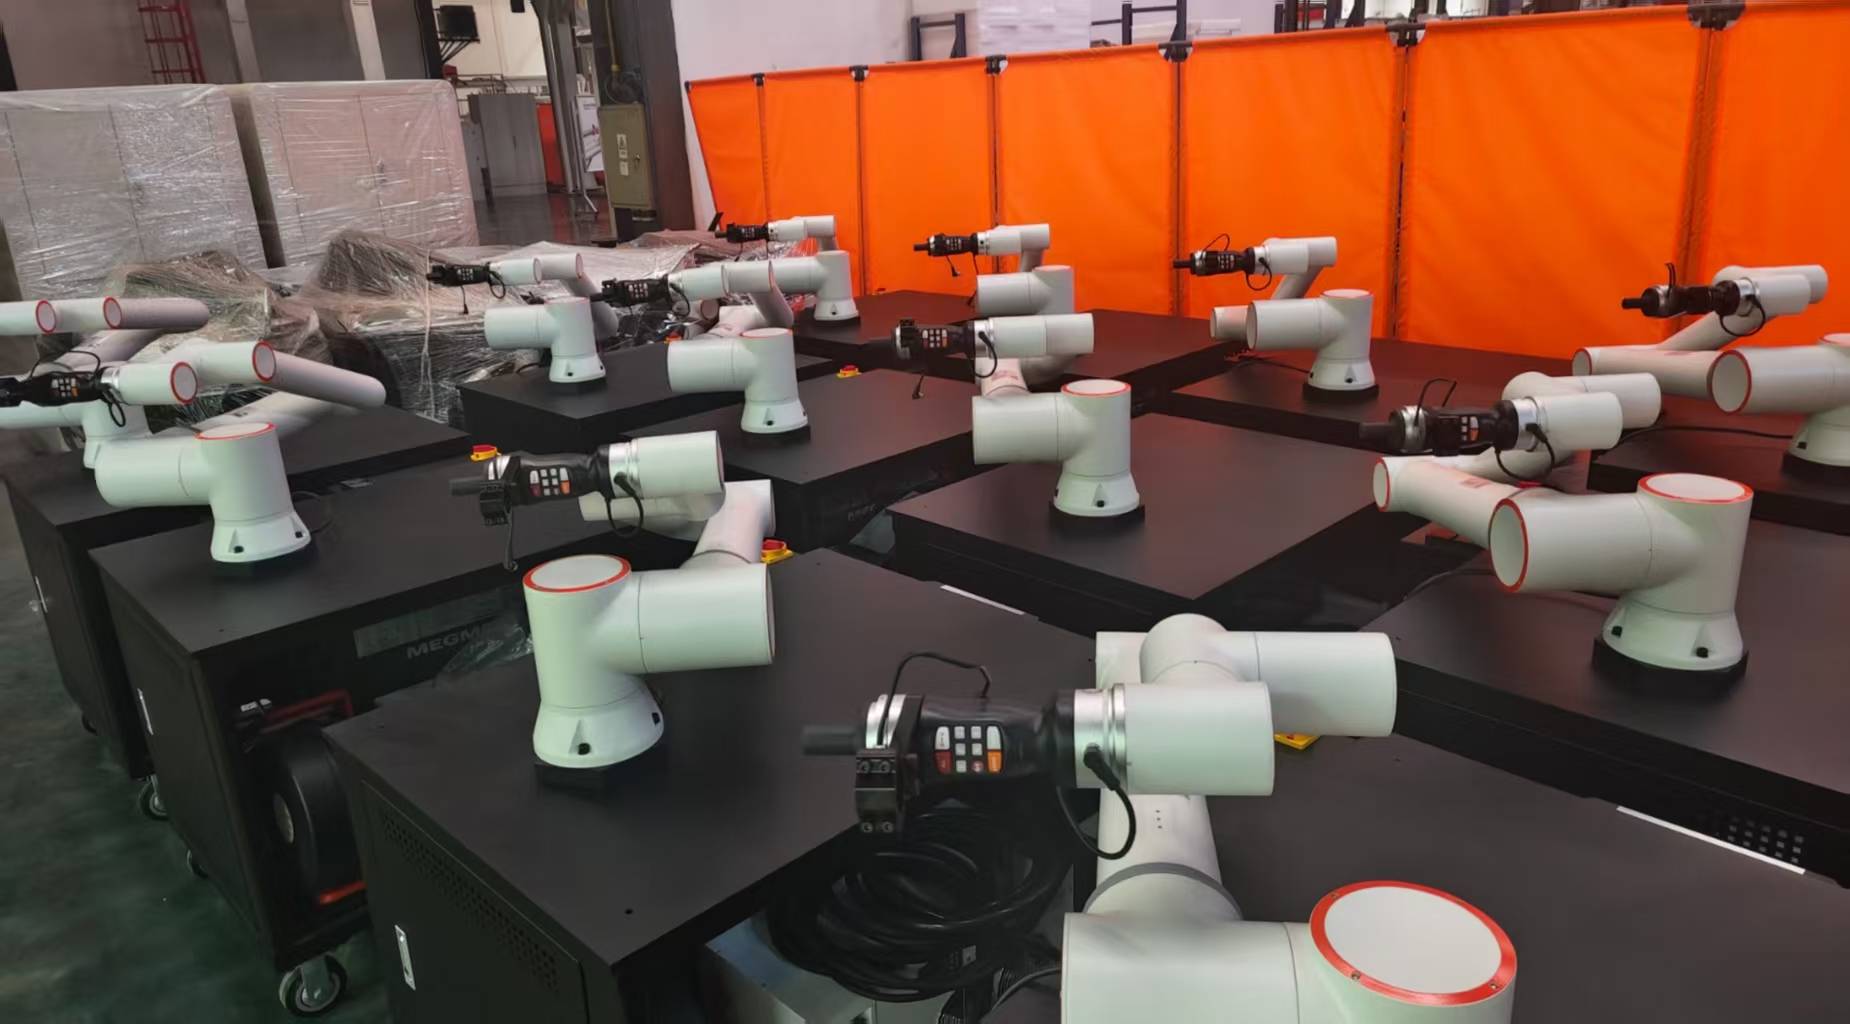
The All-in-one Cobot Station represents a significant shift in welding architecture. In traditional setups, the laser source, water chiller, wire feeder, and robot controller are discrete units connected by a “snake” of cables and hoses. In the Tuas facility, the All-in-one Cobot Station consolidated these components into a single mobile footprint (approx. 1.2m x 0.8m).
Eliminating Integration Lag
The primary synergy between the hardware and Collaborative Robotics is the reduction of “integration lag.” During the field test, we moved the station between three different work cells. Because the chiller and laser source are internal to the station, we only required a single-phase power drop and a gas line. For a Singaporean SME, this mobility allows the cobot to be treated as a tool rather than a fixed asset, moving where the production bottleneck is most acute.
Operator Interface and Hand-Guiding
The “Collaborative” aspect was tested through the lead-through programming feature. Instead of a technician writing lines of G-code, a senior welder—with zero robotics background—physically moved the torch head along the seam of a 10mm T-joint. The software recorded the path. This synergy allows the metallurgical expertise of a veteran welder to be digitized instantly, bypassing the need for a dedicated robotics engineer.
3. Technical Application: Thick Plate Steel Welding
The core of this evaluation focused on Thick Plate Steel welding, specifically S355J2+N structural steel with thicknesses ranging from 8mm to 15mm. Historically, 1500W fiber lasers were considered “thin-gauge only” tools. However, the integration of advanced wobble heads and optimized wire-feed parameters within the All-in-one Cobot Station has pushed the boundaries of what is possible at this power level.
Joint Preparation and Gap Bridging
For 12mm plate welding, we utilized a 60-degree V-groove preparation with a 1.5mm root face. The Collaborative Robotics system was programmed with a “swing” or “wobble” pattern. By oscillating the laser beam at 150Hz with a width of 3.5mm, we successfully bridged fit-up gaps that would typically cause “blow-through” in standard laser setups. This is critical in real-world Singaporean workshops where plate cutting tolerances (often from older plasma tables) are not always perfect.
Heat Input and Metallurgical Integrity
One of the “lessons learned” during the Thick Plate Steel welding trials was the management of the Heat Affected Zone (HAZ). Unlike manual MAG, which dumps significant heat into the plate, the 1500W laser provides a highly concentrated energy source. We observed a 60% reduction in thermal distortion across a 2-meter span. However, the cooling rate is much faster. To prevent the formation of martensite in the S355 steel—which leads to brittleness—we adjusted the cobot’s travel speed to 8mm/s, ensuring a slightly broader heat profile without sacrificing the narrow bead aesthetics.
4. Operational Workflow in a Singapore Context
Singapore’s Workplace Safety and Health (WSH) Act is stringent. Implementing Collaborative Robotics in a welding context requires a dual-layer safety approach. While the cobot itself is “collaborative” (it stops upon contact with a human), the 1500W laser is not.
Safety Interlocks and Housing
The All-in-one Cobot Station was paired with a modular, localized laser-safe curtain. This allowed other workers in the Tuas shop to continue manual grinding and assembly just three meters away from the active laser cell. This “mixed-mode” workshop layout is the only viable way to scale automation in high-rent industrial zones like Ubi or Jurong, where dedicated “robot rooms” are financially unfeasible.
Productivity Metrics
Over a 30-day trial, the following data was captured:
- Setup Time: Reduced from 4 hours (traditional robot) to 25 minutes (All-in-one station).
- Consumable Cost: 30% reduction in shielding gas (Argon/CO2 mix) due to more efficient torch shielding and faster travel speeds.
- Rework Rate: Dropped from 8% (manual) to under 1% (cobot) on repetitive 10mm fillet welds.
5. Lessons Learned and Engineering Recommendations
Fieldwork is never as clean as the brochure. Several technical hurdles were identified and resolved during the commissioning of the All-in-one Cobot Station.
The Humidity Factor
Singapore’s humidity is a silent killer for fiber optics. We noticed “lens fogging” during the early morning shifts. Lesson learned: The All-in-one Cobot Station must be equipped with a high-quality air dryer for the cross-jet air curtain. If you use shop air that hasn’t been properly refrigerated and dried, you will burn through protective windows every 48 hours. We implemented a dedicated point-of-use desiccant dryer, which solved the issue.
Wire Feed Synchronization
When performing Thick Plate Steel welding, the synchronization between the cobot’s acceleration/deceleration and the wire feeder is paramount. On 15mm multi-pass welds, we initially saw “pilling” at the end of the bead. We resolved this by programming a “crater fill” function into the cobot’s end-sequence, where the laser power ramps down over 0.5 seconds while the wire feed continues for an extra 0.2 seconds. This ensures a flush finish and prevents stress cracks.
Grounding and Electrical Noise
Old industrial units in Singapore often have “dirty” power. We experienced intermittent communication drops between the Collaborative Robotics controller and the laser source. Engineering fix: We installed a dedicated isolation transformer and ensured the All-in-one Cobot Station had a direct copper-path ground. Since the modification, 100% uptime was achieved.
6. Summary of Technical Synergy
The deployment proves that the 1500W All-in-one Cobot Station is no longer just a tool for sheet metal. When the metallurgical parameters are correctly tuned for Thick Plate Steel welding, and the flexibility of Collaborative Robotics is leveraged for path teaching, the ROI is realized within 12 to 14 months.
The synergy lies in the fact that the “All-in-one” design handles the logistics of the hardware, while the “Collaborative” software handles the skill gap of the workforce. For the Singaporean fabrication sector, this is the most logical path forward to remain competitive against lower-cost regional neighbors. We recommend a fleet-wide rollout for all S355 structural projects involving plate thicknesses up to 12mm in a single pass and 20mm in multi-pass configurations.
Final Field Notes:
- Check optics weekly: The Singapore salt air (near the coast) accelerates corrosion on non-stainless fittings.
- Staff training: Focus on “torch angle” during the hand-guiding phase; it is the most common variable for porosity in thick plate joints.
- Gas choice: Stick to 100% Argon for the highest penetration, or a 98/2 Argon/CO2 mix if a flatter bead profile is requested by the client.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.