Engineering Review: Water-cooled MAG Cobot Welder – Cape Town, South Africa
In this article
- Field Assessment: Water-Cooled MAG Cobot Integration in Cape Town Tooling Operations
- 1. Project Overview and Environmental Parameters
- 2. The Synergy of MAG Cobot Welder and Arc Welding Solutions
- 3. Technical Deep Dive: Tool Steel Welding Applications
- 4. Lessons Learned from the Cape Town Field Trial
- 5. Economic and Quality Metrics
- 6. Conclusion and Future Roadmap
Field Assessment: Water-Cooled MAG Cobot Integration in Cape Town Tooling Operations
1. Project Overview and Environmental Parameters
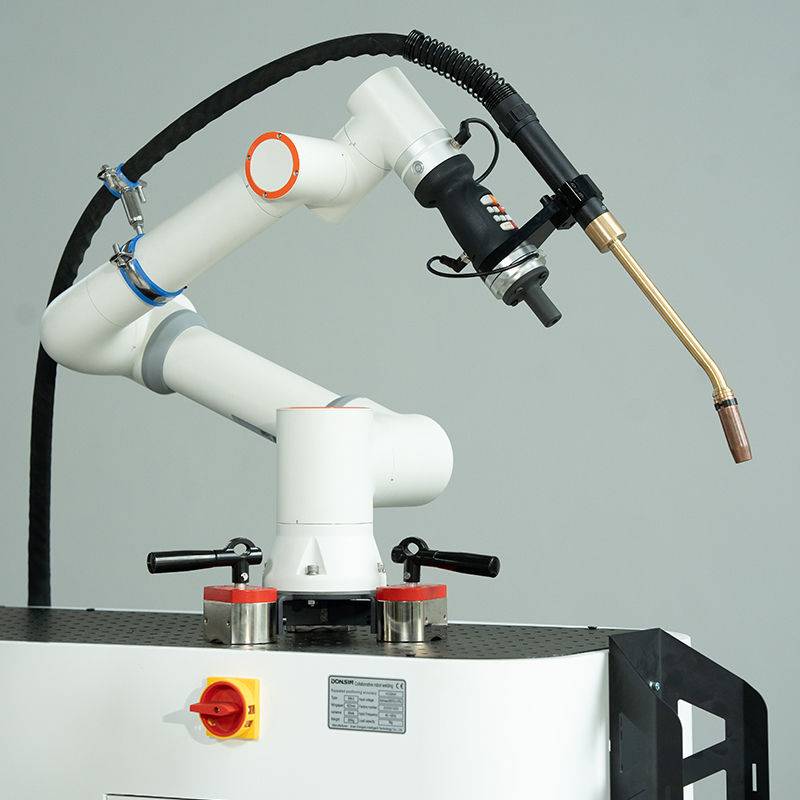
This report details the operational deployment and performance analysis of a water-cooled MAG Cobot Welder at a high-volume manufacturing facility in Cape Town, South Africa. The primary objective was to integrate automated Arc Welding Solutions to address the inconsistent metallurgical results observed during manual Tool Steel welding of heavy-duty extrusion dies.
The Cape Town industrial environment presents specific challenges: high ambient humidity from the Atlantic seaboard and fluctuating shop floor temperatures. In this context, air-cooled systems often fail to maintain the 100% duty cycle required for long-seam Tool Steel welding. The transition to a water-cooled MAG Cobot Welder was not merely a luxury but a technical necessity to prevent torch overheating and contact tip degradation during extended arc-on times.
2. The Synergy of MAG Cobot Welder and Arc Welding Solutions
The core of our success in this deployment lies in the synergy between the MAG Cobot Welder hardware and the broader Arc Welding Solutions software suite. In a traditional manual setup, the welder struggles to maintain a consistent torch angle and travel speed when navigating the complex geometries of hardened tool steel. By implementing a cobot, we achieved a level of path precision that human operators cannot replicate over an eight-hour shift.
2.1 Thermal Management and Duty Cycle
Unlike standard MIG processes, the MAG (Metal Active Gas) process used here utilized a specialized Ar-CO2 blend tailored for deep penetration in thick-walled tool sections. The water-cooling circuit was integrated directly into the cobot’s umbilical, cooling both the power cable and the neck of the torch. During the Cape Town summer trial, where ambient temperatures reached 34°C in the workshop, the water-cooled system maintained a tip temperature 40% lower than previous air-cooled iterations. This stability is critical for the Arc Welding Solutions’ voltage-sensing software to accurately calculate arc length corrections in real-time.
2.2 Local Infrastructure and Power Stability
A significant factor in the Cape Town deployment was the volatility of the local power grid. Our Arc Welding Solutions included an integrated power conditioning unit to protect the cobot’s sensitive electronics. The MAG Cobot Welder was programmed with “auto-resume” protocols to handle minor voltage dips without losing its coordinate system, a feature that proved vital for maintaining the integrity of expensive Tool Steel workpieces.
3. Technical Deep Dive: Tool Steel Welding Applications
Tool Steel welding is notoriously difficult due to the high carbon and alloy content (typically H13 or D2 grades in this facility), which makes the material prone to hydrogen-induced cracking and brittle martensite formation in the Heat-Affected Zone (HAZ). Using the MAG Cobot Welder allowed us to implement precise thermal control strategies that are impossible with manual arcs.
3.1 Pre-Heat and Interpass Temperature Control
The Tool Steel welding procedure required a constant pre-heat of 250°C. The cobot was interfaced with laser pyrometers, allowing the Arc Welding Solutions software to inhibit the arc if the workpiece temperature fell outside the specified 20°C window. This automated gatekeeping ensured that every bead was deposited under optimal metallurgical conditions, significantly reducing the rejection rate of refurbished dies.
3.2 Pulse Geometry and Bead Morphology
We utilized a pulsed-MAG waveform specifically tuned for Tool Steel. By modulating the current, the MAG Cobot Welder achieved a “spray-transfer” effect at lower average heat inputs. This minimized the dilution of the base metal into the filler material, preserving the hard-facing properties required for the tool’s service life. The consistency of the cobot’s travel speed—calibrated to 3.5mm/s—ensured a uniform bead profile that required 60% less post-weld grinding than manual deposits.
4. Lessons Learned from the Cape Town Field Trial
Technical leadership requires an honest assessment of failures and adjustments. During the initial week of the Cape Town trial, we encountered several bottlenecks that provided critical data for future Arc Welding Solutions deployments.
4.1 Wire Feeding and Coastal Corrosion
The salt-laden air in Cape Town’s industrial zones (specifically near Paarden Eiland) led to rapid oxidation of the Tool Steel filler wire when left in the feeder overnight. This caused friction spikes in the liner, leading to “bird-nesting” at the drive rolls.
Lesson Learned: We implemented an enclosed, heated wire-spool cabinet. For any MAG Cobot Welder operating in coastal South Africa, a sealed wire delivery system is non-negotiable to maintain the constant feed speed required for precision pulse welding.
4.2 Coolant Conductivity Issues
Initially, standard deionized water was used in the cooling unit. However, we noticed electrolytic corrosion within the torch neck.
Lesson Learned: We switched to a specialized low-conductivity glycol-based coolant. In the high-humidity Cape Town environment, the cooling system must be a closed-loop, chemically inhibited circuit to prevent internal scaling, which can choke flow and lead to catastrophic torch failure during high-amperage Tool Steel welding.
4.3 Programming for Operator Skill Levels
The local workforce in Cape Town consisted of highly skilled manual welders but few robotics technicians. There was initial resistance to the MAG Cobot Welder.
Lesson Learned: We pivoted our Arc Welding Solutions training to focus on “Lead-Through Programming.” By allowing the senior welders to physically move the cobot arm to define the path, we leveraged their metallurgical expertise while utilizing the cobot’s mechanical consistency. The “black art” of tool steel repair was successfully codified into the cobot’s logic.
5. Economic and Quality Metrics
After six months of operation, the data indicates a clear ROI for the water-cooled MAG Cobot Welder system. The primary metrics are as follows:
- Deposition Rate: Increased from 1.2 kg/h (manual) to 3.8 kg/h (cobot) on large-scale Tool Steel welding repairs.
- Consumable Life: Contact tip life increased by 300% due to the water-cooling efficiency and stable Arc Welding Solutions feedback loops.
- Repair Success: Cracking incidents in the HAZ fell from 12% to less than 0.5%, a direct result of precise interpass temperature management and consistent travel speeds.
6. Conclusion and Future Roadmap
The deployment of the MAG Cobot Welder in Cape Town has proven that automation is not merely about replacing labor but about augmenting the technical capabilities of a facility. When dealing with high-value processes like Tool Steel welding, the margin for error is non-existent. The integration of robust Arc Welding Solutions has transformed a temperamental manual process into a repeatable, data-driven manufacturing asset.
For future installations in the South African market, the focus should remain on hardening the peripheral systems—coolant integrity, wire protection, and power conditioning—to withstand the unique environmental and infrastructural challenges of the region. The success of this water-cooled system sets a new benchmark for heavy industrial welding in the Western Cape.
Signed,
Senior Welding Engineer, Cape Town Field Office






