Beam Processing Center with Narrow Gap welding for for Oil & Gas Tanks
In this article
Optimizing Oil and Gas Tank Fabrication via Beam Processing Centers
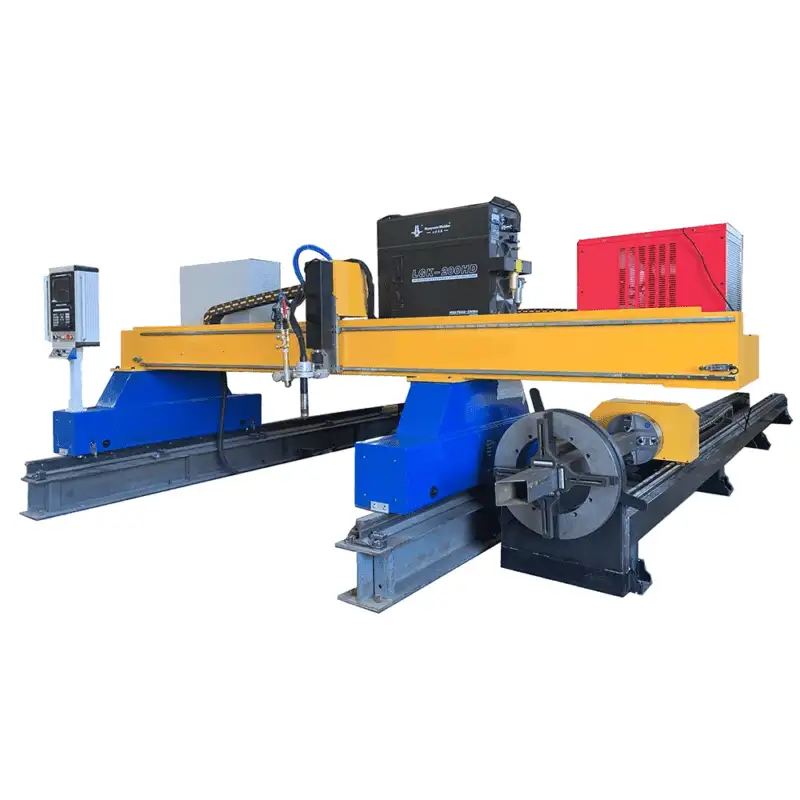
In the Oil and Gas sector, the structural integrity of storage tank foundations and internal support frameworks is non-negotiable. These structures, often utilizing heavy-duty H-beams and thick-walled profiles, require fabrication methods that minimize heat-affected zones while maximizing geometric precision. The transition toward automated structural steel processing has shifted the focus toward beam processing centers (BPC) that leverage high-definition plasma technology. Unlike traditional mechanical sawing or manual oxy-fuel cutting, modern plasma-based BPCs provide the necessary thermal energy to penetrate thick sections while maintaining the tight tolerances essential for downstream narrow gap welding processes.
The Role of Plasma Cutting in Heavy Structural Sections
Plasma cutting remains the industry standard for H-beam processing in energy infrastructure due to its balance of cutting speed and edge quality. When dealing with the heavy gauges common in tank substructures, the plasma arc provides a concentrated energy source capable of severing carbon steel and stainless steel with minimal kerf deviation. For an industrial engineer, the primary metric is the duty cycle and the ability of the system to maintain consistent arc voltage over long cutting paths.
Modern systems utilize oxygen-plasma for carbon steels to achieve a nearly dross-free finish. This is critical because any secondary grinding operation increases the cost per ton of fabricated steel. In a beam processing center, the plasma torch is typically mounted on a multi-axis robotic arm or a high-rigidity gantry, allowing it to move around the stationary or through-feed H-beam. This configuration ensures that the beam’s flanges and web are processed in a single datum environment, eliminating the cumulative errors associated with moving the workpiece between different machines.
Achieving Superior Intersection Accuracy
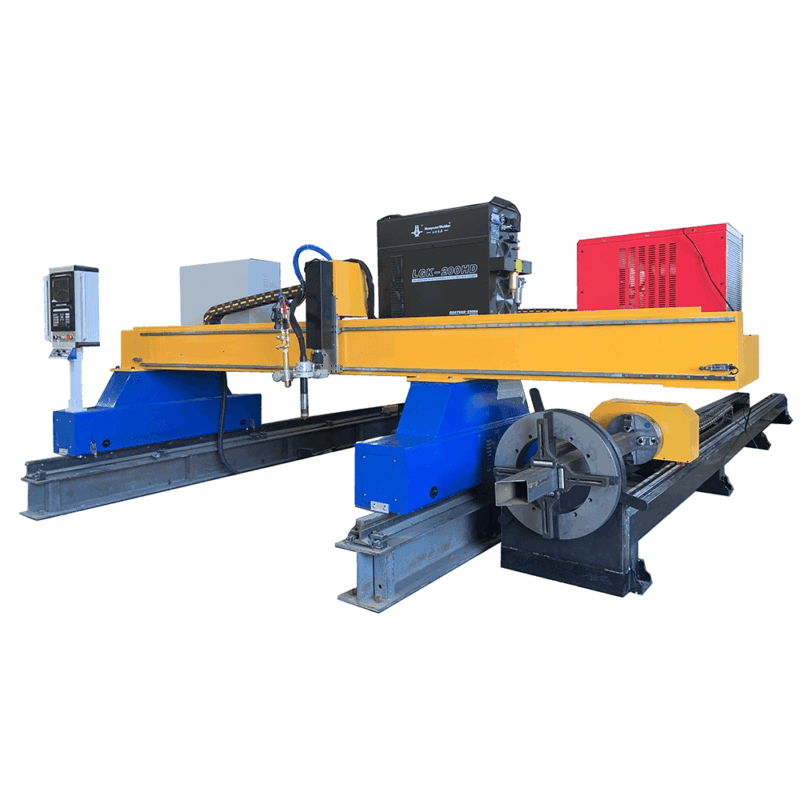
One of the most complex challenges in Oil and Gas tank fabrication is the intersection of structural members. Whether it is a web-to-flange cope or a complex miter cut for a circular support ring, intersection accuracy dictates the success of the assembly phase. High-definition plasma systems integrated with advanced CNC controllers allow for real-time compensation of beam camber and sweep.
Using laser probing or physical touch-sensing, the BPC maps the actual dimensions of the H-beam before the cut begins. This data is fed into the cutting algorithm to adjust the tool path, ensuring that the intersection point matches the 3D model exactly. For narrow gap welding, where the root opening might be as small as 1mm to 3mm, even a slight deviation in the cut profile can lead to excessive weld volume or lack of penetration. High-precision plasma cutting ensures that the structural members fit together like a jigsaw puzzle, reducing the reliance on heavy clamping and hydraulic jacks during fit-up.
Advanced Beveling for Narrow Gap Preparation
Narrow gap welding is increasingly preferred for thick-walled Oil and Gas components because it significantly reduces the amount of filler metal required and minimizes the total heat input into the joint. However, this technique is highly sensitive to groove geometry. Narrow gap welding preparation requires consistent V, Y, or J-groove profiles across the entire length of the structural section.
A 5-axis plasma head on a beam processing center allows for dynamic beveling. As the torch traverses the H-beam, it can change its tilt and rotation angle to create complex bevels that follow the contour of the beam. This is particularly important for “rat hole” cuts and weld access holes where the geometry transitions from a flat surface to a radius. By automating this beveling process, the BPC ensures that the root face and bevel angle remain constant. This consistency is what allows robotic welding systems to operate without manual intervention, as the weld path becomes highly predictable.
H-Beam Processing: Mechanical Stability and Low Maintenance
From a maintenance engineering perspective, the plasma-based BPC offers significant advantages over mechanical cutting systems. Mechanical saws involve high consumable costs in the form of blades and require complex lubrication systems that can contaminate the work area. In contrast, plasma cutting is a non-contact process. There is no mechanical force exerted on the H-beam, which reduces wear on the machine’s drive motors and linear guides.
The maintenance profile of a plasma BPC is primarily centered on the torch consumables—nozzles, electrodes, and swirl rings. Modern “long-life” plasma technologies have extended the number of pierces and arc-on time significantly, allowing for entire shifts of operation without downtime for consumable changes. Furthermore, the absence of heavy vibration (inherent in sawing or milling) means that the structural frame of the BPC retains its alignment for years, ensuring long-term automated beam profiling precision.
Eliminating Secondary Operations
In the traditional workflow, a beam would be cut to length, moved to a layout station for manual marking, and then hand-beveled by an operator with an oxy-fuel torch. Each of these steps introduces potential for human error and material handling damage. By consolidating these tasks into a single plasma-enabled beam processing center, the “art” of fabrication is replaced by the “science” of engineering.
The precision of the plasma arc means that bolt holes can be cut to within 0.1mm of their specified diameter, often negating the need for secondary drilling. While plasma-cut holes were once criticized for their taper, modern high-definition systems utilize specialized gas shielding to produce straight-walled holes that meet the stringent AISC (American Institute of Steel Construction) standards used in O&G projects.
Workflow Integration and SEO Impact on Production
The integration of BIM (Building Information Modeling) data directly into the BPC software further streamlines production. Files exported from platforms like Tekla or SDS/2 are converted into machine code that includes all plasma cutting instructions, bevel angles, and marking locations. This digital thread ensures that what is designed in the engineering office is exactly what is produced on the shop floor.
For companies providing fabrication services for Oil and Gas tanks, the adoption of plasma beam processing is a strategic differentiator. It allows for faster project turnaround times and lower labor costs per unit. More importantly, it provides the level of quality assurance required by global energy firms, where every weld and every structural connection is subject to non-destructive testing (NDT). If the initial plasma cut is perfect, the subsequent welding and inspection processes proceed without the costly rework that plagues traditional fabrication shops.
Summary of Engineering Benefits
The focus on plasma technology within beam processing centers is driven by the need for speed, accuracy, and reliability. By mastering intersection accuracy and beveling for narrow gap welding, fabricators can produce tank supports that are structurally superior and more cost-effective. The low maintenance requirements of these systems, combined with their ability to handle massive H-beams, makes them an essential asset in the modern Oil and Gas industrial landscape.







