Beam Processing Center with Arc Voltage Control for for LNG Projects
In this article
- Precision Fabrication in LNG Infrastructure: The Role of Plasma Beam Processing
- The Mechanics of Arc Voltage Control (AVC) in Thermal Cutting
- Achieving Superior Intersection Accuracy for Complex Nodes
- Plasma Beveling: Preparing the Edge for Cryogenic Loads
- H-Beam Low Maintenance and System Longevity
- Conclusion: The Engineering Imperative
Precision Fabrication in LNG Infrastructure: The Role of Plasma Beam Processing
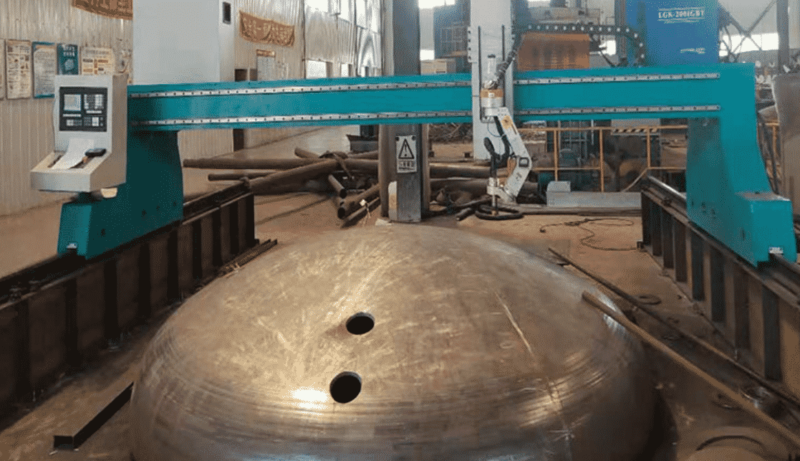
Liquefied Natural Gas (LNG) projects represent some of the most demanding environments for structural steel fabrication. The combination of massive structural loads and the necessity for cryogenic-ready joints requires a level of precision that manual layout and cutting cannot consistently provide. At the center of this fabrication pipeline is the Beam Processing Center, a multi-axis automated system engineered to handle H-beams, channels, and angles with surgical accuracy. For industrial engineers overseeing these projects, the transition from traditional mechanical methods to advanced Plasma Cutting systems equipped with Arc Voltage Control (AVC) is a prerequisite for meeting both tight schedules and stringent safety codes.
The structural integrity of an LNG facility relies heavily on the quality of fit-up between massive steel members. Whether constructing modular pipe racks or the primary support frames for storage tanks, the dimensional tolerances are razor-thin. Plasma cutting technology, when integrated into a robust robotic or CNC gantry system, provides the thermal energy necessary to pierce thick-walled sections while maintaining a narrow kerf. However, the true engineering challenge lies not just in the cut itself, but in maintaining the torch’s relationship to the material surface throughout complex geometries.
The Mechanics of Arc Voltage Control (AVC) in Thermal Cutting
In the context of H-beam processing, material deviations are an inherent reality. Beams are rarely perfectly straight; they often exhibit “camber,” “sweep,” or “twist” resulting from the rolling process at the mill. Traditional fixed-height cutting heads fail in these scenarios, either diving into the workpiece or lifting too far away, which results in poor cut quality, excessive dross, or torch damage. Arc Voltage Control solves this by utilizing the plasma arc itself as a sensor. By measuring the voltage between the electrode and the workpiece, the system can determine the exact distance of the torch tip from the metal surface.
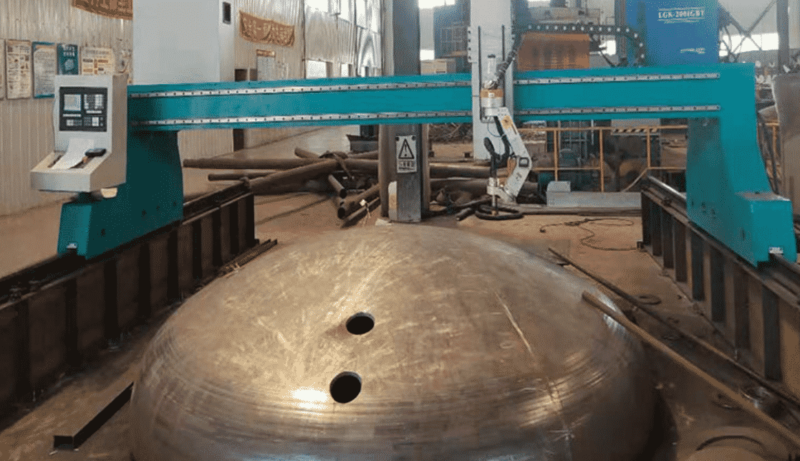
If the voltage increases, the system detects an increase in the arc gap and signals the Z-axis motor to lower the torch. Conversely, a drop in voltage triggers an immediate retraction. In LNG projects, where beams can exceed 12 meters in length, this real-time adjustment ensures that the plasma gas remains at its optimal focal point. For the industrial engineer, this translates to a consistent metallurgical heat-affected zone (HAZ) and a surface finish that often requires zero secondary grinding before entering the assembly phase.
Achieving Superior Intersection Accuracy for Complex Nodes
LNG modules are characterized by complex intersections where multiple beams meet at varying angles. Achieving high intersection accuracy is critical for ensuring that load paths are correctly transferred through the structure. When a secondary beam must cope into the web and flanges of a primary H-beam, the geometry of the cut is three-dimensional and non-linear. Automated beam processing centers utilize sophisticated CAD/CAM interfaces to calculate the exact toolpath required for these “fish-mouth” or “cope” cuts.
By leveraging the AVC, the cutting head maintains its orientation even as it transitions from the flange to the web. This prevents the “rounding” of corners that often occurs with manual oxy-fuel sets. High intersection accuracy means that when the components reach the fit-up table, they slide into place with a gap tolerance of less than 1mm. This precision is not merely an aesthetic requirement; it is a structural necessity. Minimal gaps ensure that the subsequent welding process—often high-deposition submerged arc or gas metal arc welding—can achieve full penetration without the risk of burn-through or excessive internal stress.
Plasma Beveling: Preparing the Edge for Cryogenic Loads
In LNG structural design, simple square cuts are rarely sufficient. To handle the stresses of thermal expansion and contraction, most joints require complex beveling. Plasma beveling modules in a beam processing center allow for the creation of V-grooves, Y-grooves, and K-cuts in a single pass. The ability to tilt the plasma torch up to 45 or 50 degrees while maintaining AVC-regulated height is a significant technological leap over traditional methods.
For an industrial engineer, the advantage of automated beveling is the elimination of “double-handling.” In a traditional workflow, a beam is cut to length, moved to a different station, and then beveled manually using a hand-held grinder or a track burner. A beam processing center performs these operations concurrently. The AVC is particularly vital during beveling because the effective distance the arc must travel increases as the torch tilts. Advanced control algorithms compensate for this “slant distance,” ensuring the bevel angle remains constant across the entire width of the flange, regardless of any beam warping.
H-Beam Low Maintenance and System Longevity
The operational environment of a heavy steel fabrication shop is punishing. Dust, metallic particles, and extreme heat are constants. A primary concern for plant managers is the maintenance cycle of their equipment. Modern beam processing centers are designed with a focus on H-beam low maintenance requirements. This is achieved through the isolation of sensitive electronics and the use of hardened, bellows-protected linear guides.
Furthermore, the use of plasma over mechanical drilling or sawing reduces the physical strain on the machine’s frame. There are no “tool-engagement” forces that lead to bearing wear or spindle fatigue. The AVC also acts as a safety mechanism; by preventing torch collisions with the workpiece, it drastically reduces the replacement frequency of consumables (nozzles and electrodes) and prevents costly damage to the torch body itself. for LNG Projects with multi-year timelines, the reliability of these machines ensures that the fabrication schedule remains insulated from unexpected mechanical downtime.
Optimizing Throughput through Automated Material Handling
Beyond the cutting head, the efficiency of a beam processing center is measured by its material handling capabilities. Automated conveyors and cross-transfers move heavy profiles into the cutting zone with minimal operator intervention. Integration with Building Information Modeling (BIM) software allows the machine to pull cutting data directly from the structural model, eliminating manual data entry errors. In the context of an LNG project, where thousands of unique parts must be tracked and labeled, integrated inkjet marking or plasma marking systems are used to scribe part numbers and weld symbols directly onto the steel. This ensures traceability, a non-negotiable requirement for high-stakes energy infrastructure.
Conclusion: The Engineering Imperative
For the industrial engineer tasked with delivering an LNG project on time and within budget, the adoption of a beam processing center with integrated Arc Voltage Control is a strategic necessity. By focusing on the precision of plasma cutting, the system addresses the three most significant bottlenecks in structural fabrication: fit-up rework due to poor intersection accuracy, the labor-intensive nature of manual beveling, and the high overhead associated with machine maintenance. As global demand for LNG continues to drive the scale of modular construction upward, the reliance on automated thermal cutting will only increase, making AVC-equipped systems the gold standard for structural steel excellence.
Technical Specifications Summary for Engineering Planning
When specifying a system for LNG-grade H-beam processing, engineers should prioritize a high-speed Z-axis response time (typically >3000mm/min) for the AVC to ensure it can react to rapid changes in profile geometry. Additionally, the plasma power source should be rated for a 100% duty cycle to match the continuous output required for large-scale industrial projects. By aligning these technical capabilities with the project’s specific metallurgical requirements, fabrication facilities can ensure a seamless transition from raw mill sections to precision-engineered structural components.





