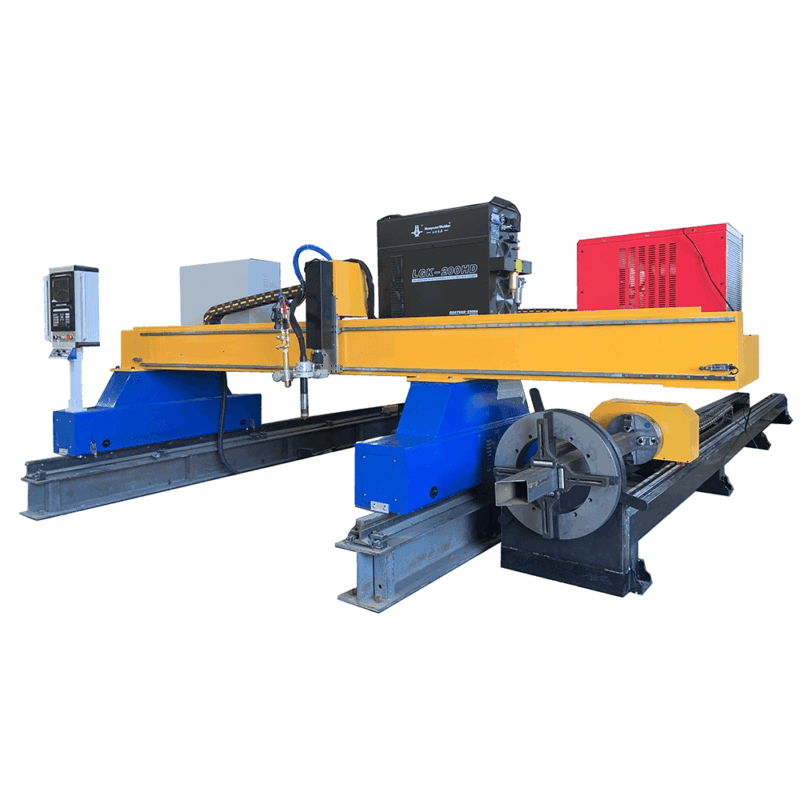
Beam Processing Center with Arc Voltage Control for for Oil & Gas Tanks
In this article
Optimizing Oil and Gas Tank Fabrication via Plasma Beam Processing
The fabrication of large-scale storage tanks and pressure vessels for the oil and gas sector demands rigorous adherence to dimensional tolerances and structural integrity. Central to this process is the Plasma Beam Processing Center, a multi-axis system designed to handle the heavy-duty profiles required for tank supports, nozzle intersections, and shell reinforcements. Unlike traditional manual layouts, these automated centers integrate high-definition plasma power sources with sophisticated motion control to execute complex cuts on H-beams, channels, and cylindrical sections.
For industrial engineers, the primary challenge in tank fabrication is managing the scale of the workpieces. Material irregularities, such as slight bows in H-beams or eccentricity in large-diameter shells, can lead to catastrophic fit-up failures. The integration of Arc Voltage Control (AVC) serves as the critical feedback loop necessary to maintain torch height parity, ensuring that the plasma arc remains stable regardless of surface deviations.
The Mechanics of Arc Voltage Control (AVC) in Plasma Systems
Arc Voltage Control is not merely a height sensor; it is a dynamic regulation system that measures the electrical potential between the plasma torch electrode and the workpiece. In Plasma Cutting, the voltage is directly proportional to the arc length. As the distance between the torch and the material increases, the voltage rises; as it decreases, the voltage drops.
In the context of Arc Voltage Control, the system’s CNC continuously monitors these fluctuations at microsecond intervals. If the material being processed—such as a large tank head or an H-beam flange—is not perfectly flat, the AVC adjusts the Z-axis motor to maintain a constant standoff distance. This constancy is vital for maintaining the “sweet spot” of the plasma plume, which dictates the kerf width and the angularity of the cut. Without AVC, variations in material height would result in inconsistent cut widths, leading to poor intersection fit-up and increased secondary grinding.
Achieving Precision in Intersection Accuracy
One of the most complex tasks in oil and gas tank construction is the cutting of nozzle openings and pipe-to-shell intersections. These “saddle cuts” or “fish-mouth” profiles require 3D spatial accuracy. A Plasma Beam Processing Center utilizes 5-axis or 6-axis robotic arms or gantry systems to navigate these geometries.
Intersection Accuracy is achieved through the synchronization of the rotational axis of the beam or pipe with the lateral and vertical movement of the plasma torch. Because the surface of a tank shell is curved, the torch must constantly change its orientation to remain perpendicular (or at a specific bevel angle) to the surface. AVC ensures that as the torch travels over the curvature, it does not collide with the workpiece nor drift too far away, which would cause the arc to extinguish or “lag,” ruining the tolerance of the hole. For engineers, this translates to a “drop-in” fit for nozzles, significantly reducing the man-hours previously spent on manual trimming and gap-filling during assembly.
H-Beam Processing and Low Maintenance Operations
Structural supports for tanks often utilize heavy H-beams (Universal Beams) that require coping, slotting, and bolt-hole piercing. In a plasma-based processing center, these operations are consolidated into a single pass. A major advantage of using plasma for H-beam processing is the H-beam low maintenance profile compared to mechanical alternatives like sawing or drilling.
Mechanical systems suffer from tool wear, requiring frequent blade replacements or drill bit sharpening, especially when dealing with high-tensile steels common in the energy sector. Plasma cutting is a non-contact process. The only wear parts are consumables—electrodes, nozzles, and shields—which can be monitored via the CNC software and replaced in minutes. Furthermore, the absence of mechanical force on the beam eliminates the need for massive hydraulic clamping systems that often fail under the grit and scale environment of a heavy fabrication shop. The streamlined motion control of a plasma center reduces the total number of moving parts subject to friction, thereby increasing the Mean Time Between Failures (MTBF).
Advanced Beveling for Weld Preparation
In oil and gas applications, simple 90-degree cuts are rarely sufficient. Most structural and pressure-retaining joints require specific edge preparations, including V-grooves, Y-grooves, or K-bevels, to ensure full-penetration welds. A Structural Beveling head on a plasma center allows for the automation of these profiles.
The AVC plays a secondary, yet equally important, role during beveling. When the torch is tilted at an angle (e.g., 45 degrees for a V-bevel), the effective distance the arc must travel to the plate changes. The control system must calculate the “effective voltage” to maintain the correct tip-to-work distance while the torch is in a non-vertical orientation. This automated beveling eliminates the need for a secondary process using hand-held oxy-fuel torches or track burners. By executing the bevel during the primary cutting phase, the center ensures that the bevel angle is consistent along the entire length of the cut, which is essential for automated welding robots that may follow the cutting process.
Thermal Management and Kerf Compensation
Industrial engineers must also account for the thermal input of the plasma arc. While plasma is faster than oxy-fuel, it still introduces heat into the workpiece. High-end beam processing centers incorporate kerf compensation algorithms that adjust the torch path in real-time based on the thickness of the material and the amperage used.
When combined with AVC, the system can compensate for the slight lifting or “potato chipping” of thin-gauge tank plates caused by thermal expansion. The AVC detects the rise in the plate and adjusts the Z-axis instantly, preventing the torch from dragging and ensuring that the programmed dimensions are maintained within sub-millimeter tolerances. This level of control is what allows plasma systems to compete with higher-cost technologies while maintaining the robust throughput required for heavy industrial sectors.
Operational Efficiency and Data Integration
Modern processing centers are integrated into the facility’s PLM (Product Lifecycle Management) and BIM (Building Information Modeling) workflows. The NC files generated from 3D models of the oil tanks are fed directly into the plasma center. Because the system utilizes AVC to handle real-world material imperfections, the “digital twin” of the tank component is realized with high fidelity.
The reduction in manual intervention leads to a significant decrease in the Total Cost of Ownership (TCO). By focusing on plasma’s strengths—speed, versatility in beveling, and low mechanical maintenance—fabricators can achieve a higher tonnage throughput per month. The reliance on AVC mitigates the risks associated with operator error, as the system automatically handles the nuances of torch height and arc stability that would otherwise require a highly skilled technician to manage manually.
Conclusion for Engineering Implementation
The transition to an automated Plasma Beam Processing Center for oil and gas tank fabrication represents a strategic shift toward high-precision, low-maintenance manufacturing. By leveraging Arc Voltage Control, engineers can guarantee Intersection Accuracy on complex geometries and produce weld-ready Structural Beveling profiles without the overhead of mechanical tooling or the inconsistency of manual labor. As the industry moves toward tighter regulatory codes and more aggressive production schedules, the integration of these high-definition plasma systems becomes not just an advantage, but a logistical necessity.