Beam Processing Center with Arc Voltage Control for for Oil & Gas Tanks
In this article
Optimizing Structural Integrity with Arc Voltage Control
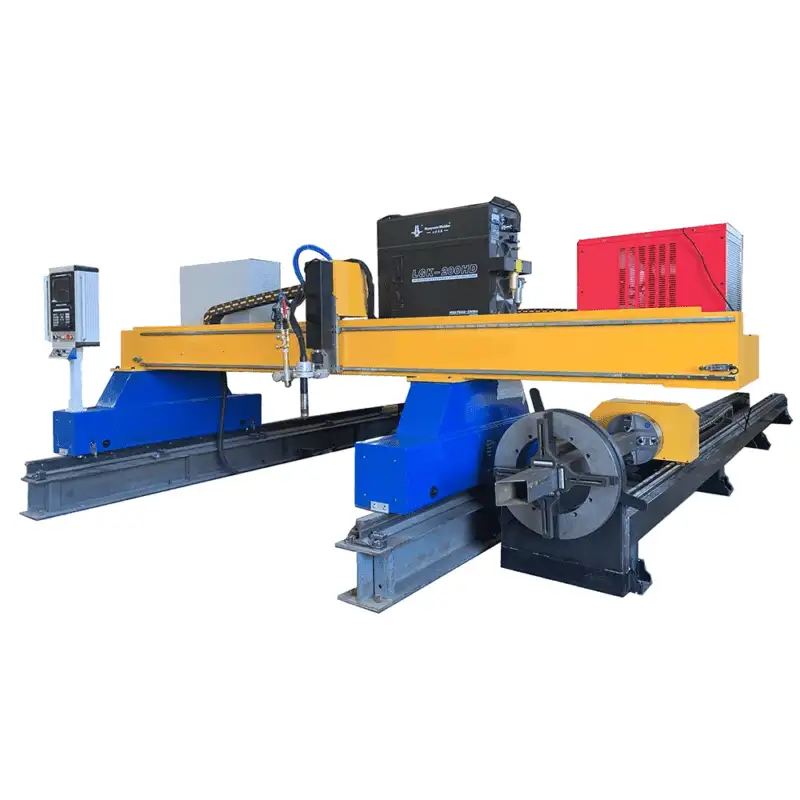
In the fabrication of large-scale storage tanks for the Oil and Gas industry, the structural framework—primarily composed of H-beams, channels, and heavy plate—demands rigorous adherence to dimensional tolerances. A Beam Processing Center equipped with Plasma Cutting technology serves as the primary engine for this production. The most critical component in maintaining cut quality over long structural members is the Arc Voltage Control (AVC) system. Unlike basic height sensors, AVC monitors the electrical potential between the plasma electrode and the workpiece in real-time. As the distance between the torch and the beam fluctuates due to material crowning, twisting, or thermal expansion, the AVC adjusts the Z-axis position instantaneously to maintain a constant voltage.
For an industrial engineer, the value of AVC lies in the consistency of the kerf width. In plasma cutting, any variation in torch height alters the shape of the plasma arc, leading to “top rounding” or excessive dross. In Oil and Gas applications, where structural beams must support thousands of tons of liquid pressure, even minor deviations in cut geometry can lead to stress concentrations. By stabilizing the arc gap, AVC ensures that every penetration and profile cut meets the intersection accuracy required for seamless assembly.
Precision Intersection Cutting for Tank Support Systems
Oil and Gas tanks require complex support structures where beams must intersect at various angles to distribute load effectively. Traditional methods involved manual layout and hand-held plasma torches, which introduced significant human error. Modern beam processing centers utilize multi-axis robotic arms or gantry systems to execute these intersections with mathematical precision. The intersection accuracy provided by CNC-controlled plasma systems allows for the creation of “coped” joints where one beam fits perfectly into the profile of another.
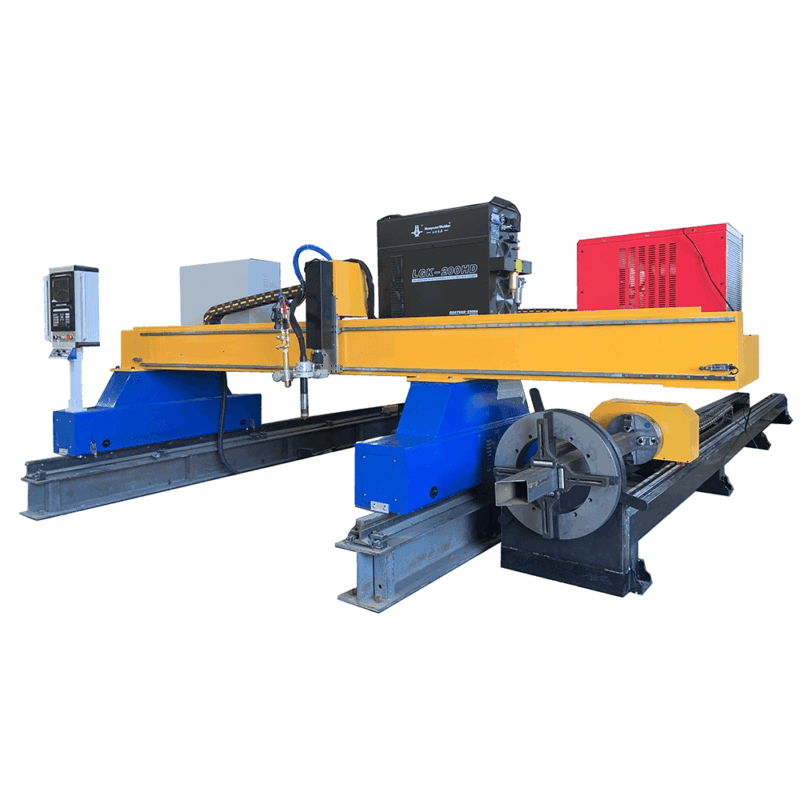
When cutting openings for piping or manways into structural beams, the plasma system must calculate the tool path based on the true 3D profile of the steel. This involves complex interpolation where the torch must rotate and tilt while simultaneously moving along the X, Y, and Z axes. Because the AVC maintains the optimal standoff distance during these complex maneuvers, the resulting edges are clean and free of taper, which is essential for the structural integrity of the tank’s secondary containment and support rings.
Mechanical Efficiency and H-Beam Low Maintenance
From an operational standpoint, the choice of plasma over other thermal cutting methods is driven by the rugged nature of the environment. Structural steel for the Oil and Gas sector is often stored outdoors and may have surface rust, mill scale, or primer coatings. Plasma cutting excels in these conditions because the high-temperature ionized gas easily penetrates surface contaminants. Furthermore, a H-beam low maintenance profile is a primary requirement for high-throughput facilities.
Plasma systems are designed for high duty cycles. The maintenance requirements are localized to consumables—electrodes, nozzles, and swirl rings—which can be replaced in minutes without specialized optical calibration. Unlike systems that require high-purity environments or delicate mirrors, a plasma beam center operates reliably in dusty, non-climate-controlled fabrication shops. For the industrial engineer, this translates to higher Machine Utilization Effectiveness (MUE) and lower Total Cost of Ownership (TCO). The mechanical components of the beam center, such as the rack-and-pinion drives and hardened linear guides, are built to withstand the vibration and thermal load generated during continuous cutting operations.
Automated Beveling for Heavy Wall Weld Preparation
One of the most time-consuming tasks in tank fabrication is the preparation of weld joints. Oil and Gas standards, such as API 650 or ASME Section VIII, require specific bevel angles for full-penetration joints to ensure the safety of pressurized vessels. A beam processing center with an integrated tilting plasma head allows for automated plasma beveling. This eliminates the need for secondary grinding or manual beveling processes.
The system can execute V, Y, X, and K-cuts on the fly. As the torch tilts to the required angle, the AVC system continues to function, adjusting for any slight bow in the beam web or flange. This is a critical distinction: if the height were fixed, a tilted torch would be at a different distance from the metal than a vertical one. The AVC compensates for this trigonometric offset, ensuring the bevel face remains uniform across the entire length of the cut. This uniformity is vital for subsequent joining processes, as it allows for consistent root openings and reduces the volume of filler metal required.
Material Handling and Throughput Optimization
The efficiency of a Beam Processing Center is not limited to the cut itself but extends to the movement of the material. In Oil and Gas tank projects, beams can reach lengths of 12 to 18 meters. Integrated conveyor systems with hydraulic clamping ensure that the beam is indexed accurately through the cutting zone. When combined with plasma cutting technology, these systems can process multiple features—bolt holes, copes, and bevels—in a single pass.
Industrial engineers focus on reducing “air-cut time.” By utilizing advanced nesting software, the beam center can calculate the most efficient sequence of cuts to minimize torch travel and material waste. The software accounts for the plasma kerf (the width of the cut) and the specific arc characteristics of the gas mixture being used (typically Oxygen or Nitrogen/Water-injection for stainless applications). This level of control ensures that the final structural components are ready for immediate assembly, bypassing the bottleneck of manual rework.
System Reliability in Harsh Fabrication Environments
The final consideration for Oil and Gas fabrication is the durability of the cutting equipment. Plasma torches are designed to be “collision-aware.” In the event of a tip-up or a piece of scrap interfering with the path, modern torch holders feature breakaway mechanisms that prevent damage to the Z-axis drive. This resilience, paired with the H-beam low maintenance design, ensures that the fabrication schedule remains on track even when working with “B-grade” structural steel that may have unpredictable internal stresses.
In summary, the integration of Arc Voltage Control within a plasma beam processing center provides the precision, adaptability, and speed required for the demanding Oil and Gas sector. By focusing on intersection accuracy and automated plasma beveling, fabricators can produce high-quality structural components that meet stringent safety standards while maintaining a lean, low-maintenance production line. The technology effectively bridges the gap between raw structural steel and the high-precision engineering required for modern energy infrastructure.






