Technical Integration of Plasma Cutting in LNG Infrastructure
The construction of Liquefied Natural Gas (LNG) facilities demands a level of structural precision that leaves no room for error. Industrial engineers tasked with overseeing these projects face unique challenges: high-pressure environments, cryogenic temperatures, and massive structural requirements. At the center of this fabrication ecosystem is the Plasma Cutting Systems technology, specifically configured with 5-Axis Beveling capabilities. Unlike standard 2D cutting, the 5-axis configuration allows for complex geometry management, which is essential for the intricate piping networks and heavy-duty H-beams that form the skeleton of an LNG plant.
From an engineering perspective, the transition to 5-axis plasma cutting is driven by the need for automated weld preparation. In LNG projects, thick-walled pipes and pressure vessel plates require precise grooves—V, X, Y, or K shapes—to ensure full penetration during the welding process. The plasma arc, when controlled by a high-precision 5-axis head, provides the necessary thermal energy to sever thick alloy steels while simultaneously creating the bevel angle. This eliminates secondary machining processes, effectively reducing the manufacturing cycle time and minimizing the handling of heavy materials.
The Mechanics of 5-Axis Beveling and Weld Preparation
The core advantage of 5-Axis Beveling lies in its ability to rotate and tilt the plasma torch dynamically during the cutting path. In the context of LNG tank construction, where large diameter plates must meet at specific angles to form a spherical or cylindrical vessel, the bevel must be consistent across the entire edge. A 5-axis head utilizes sophisticated CNC algorithms to compensate for the kerf width and arc voltage variations in real-time.
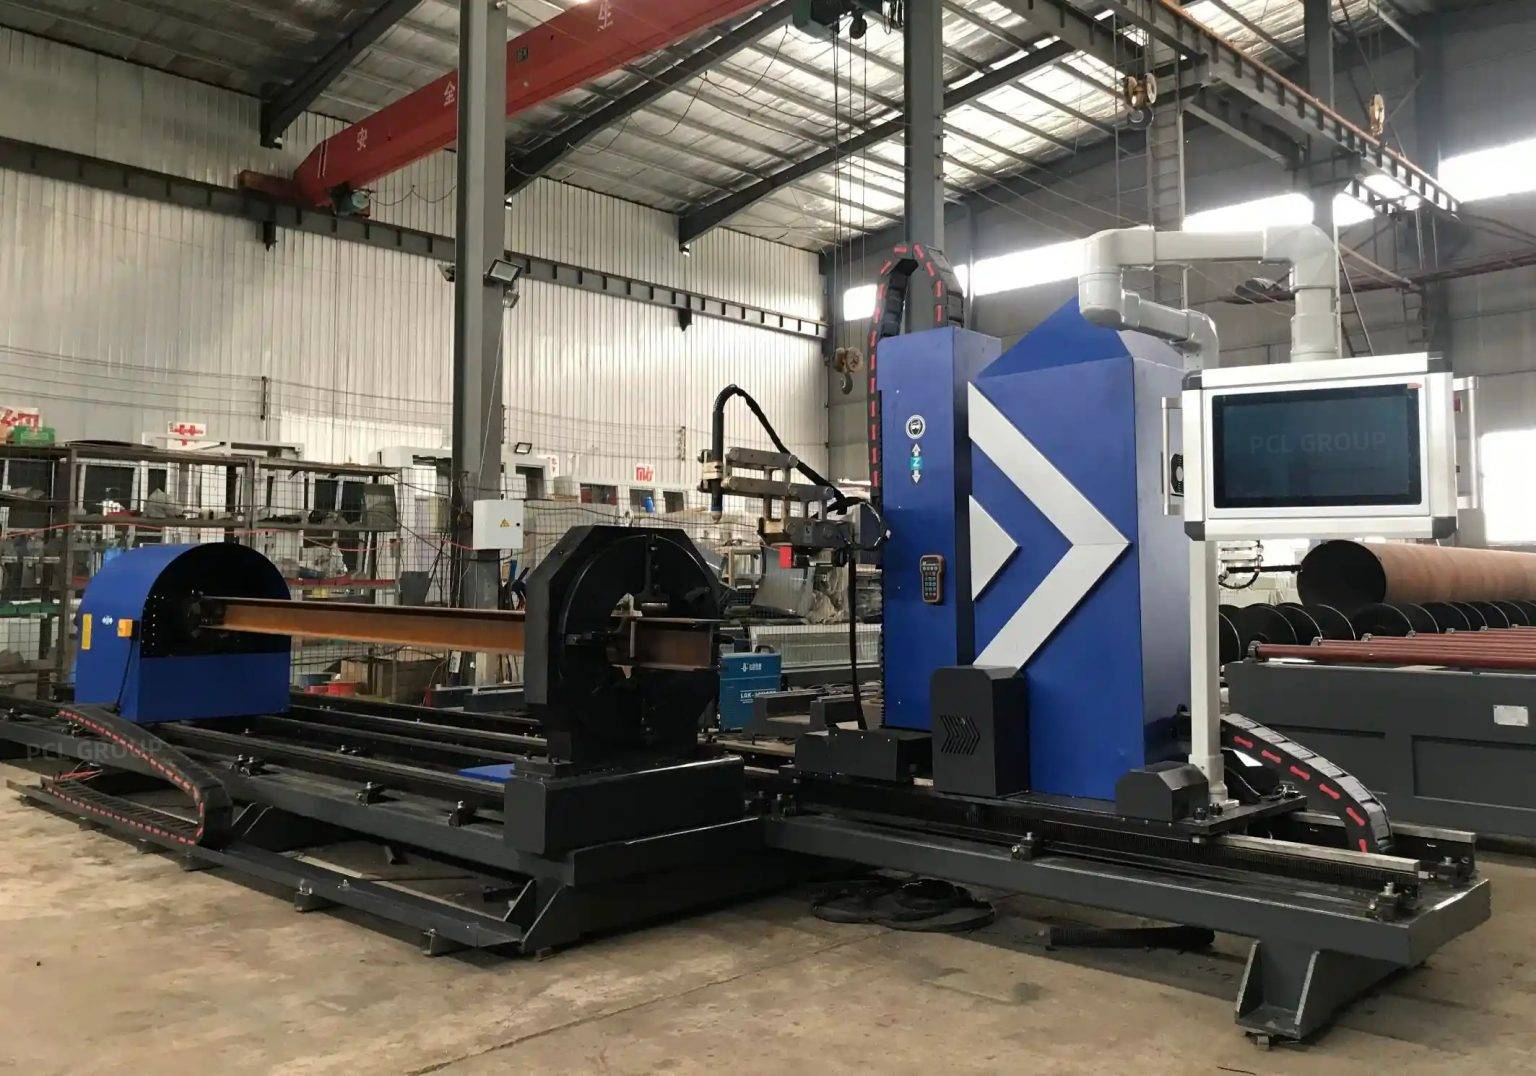
By employing a continuous rotation head, the system avoids the “cable twist” limitations that plagued older generations of plasma machines. This allows for long, uninterrupted cuts on large-format plates. For industrial engineers, the focus is on the Heat Affected Zone (HAZ). Modern high-definition plasma systems use constricted arc technology to narrow the HAZ, ensuring that the metallurgical properties of the specialized steels used in LNG—often containing high nickel content—remain within the specified tolerances for cryogenic service. This precision ensures that the subsequent welding stages are faster and more reliable, as the fit-up tolerances are kept within fractions of a millimeter.
Achieving Critical Intersection Accuracy in Pipe Profiling
LNG facilities rely on complex manifolds and piping headers where multiple pipes intersect at various angles. Achieving Intersection Accuracy is the most difficult aspect of pipe profiling. When a branch pipe meets a header pipe, the cut must account for both the curvature of the cylinders and the bevel angle required for the joint. A 5-axis plasma machine solves this through advanced mathematical modeling integrated into the nesting software.
The software calculates the “saddle” cut, providing a seamless fit that requires minimal gap bridging. In high-pressure LNG lines, any deviation in the intersection leads to stress concentrations that could jeopardize the system under thermal expansion or contraction. Plasma cutting provides a non-contact method to execute these profiles on hardened or treated steels without the tool wear associated with mechanical sawing or milling. The result is a repeatable, high-speed production line that maintains geometric fidelity across thousands of unique pipe segments.
H-Beam Processing: Efficiency and Maintenance Protocols
The structural framework of LNG terminals involves massive quantities of H-beams and I-beams. Traditional methods of processing these—such as drilling and mechanical shearing—are labor-intensive and require frequent tool replacement. Plasma cutting systems designed for structural steel offer a low-maintenance alternative that handles multi-surface cutting in a single pass.
Industrial engineers favor plasma for H-beam processing due to the lack of physical force applied to the workpiece. Because plasma is a thermal process, there is no vibration or mechanical stress, which extends the lifespan of the machine’s gantry and drive systems. The maintenance cycle is primarily focused on consumables—nozzles, electrodes, and shields—which can be replaced in minutes. This is a critical factor in maintaining a high OEE (Overall Equipment Effectiveness) on the shop floor. Furthermore, the ability to cut bolt holes, web penetrations, and flange bevels with the same torch reduces the footprint of the fabrication line, as one 5-axis plasma station replaces multiple dedicated machines.
Optimizing Gas Selection for LNG Grade Steels
In the LNG sector, the material of choice is often stainless steel or 9% nickel steel due to their ductility at extremely low temperatures. The plasma cutting process must be tuned to these alloys. Industrial engineers must select the appropriate plasma and shielding gases to prevent oxidation and ensure a clean cut surface. For instance, using H35 (a mixture of hydrogen and argon) for thick stainless steel provides a clean, dross-free edge that is ready for welding without grinding.
The 5-axis system’s ability to adjust gas flow and pressure dynamically based on the torch angle is vital. When the torch is tilted for a 45-degree bevel, the effective thickness of the material increases. The CNC controller must automatically compensate by increasing power and adjusting gas flow to maintain the arc’s stability. This level of automation is what separates industrial-grade plasma systems from general-purpose cutting tools, providing the consistency required for international LNG safety standards.
Data-Driven Production and Quality Control
The modern plasma cutting environment is deeply integrated with LNG Infrastructure project management software. Every cut, bevel, and hole is logged, providing a digital twin of the fabrication process. This traceability is essential for quality assurance in LNG projects, where every component must be tracked from the mill to the final assembly.
By monitoring the consumables’ life and the arc-on time, industrial engineers can predict maintenance needs before failures occur, preventing costly downtime during tight construction windows. The accuracy of the 5-axis plasma machine directly impacts the downstream assembly. When the intersection accuracy is high, the “fit-up” time on site is reduced by up to 40%, as field crews are not required to perform manual corrections. This systemic efficiency is why 5-axis plasma cutting remains the gold standard for heavy-duty energy projects worldwide.
Conclusion: Maximizing Throughput in Heavy Fabrication
For the industrial engineer, the decision to implement a 5-axis plasma cutting system is a balance of precision, speed, and long-term operational costs. In the LNG sector, where the complexity of the geometry is matched only by the strictness of the safety codes, the ability of plasma to deliver high-quality bevels and accurate pipe intersections is unmatched. By focusing on low-maintenance H-beam processing and high-definition arc control, fabrication facilities can meet the aggressive timelines of global energy infrastructure projects while maintaining the highest levels of structural integrity.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.